Choosing the best abrasion resistant steel plate suppliers in 2026 requires more than comparing prices or browsing polished websites. Buyers need evidence from real projects, clear mill documentation, and practical service records. A reliable supplier should explain plate grades, hardness ranges, impact performance, thickness tolerances, and suitable processing methods. Those details matter when plates face loaders, crushers, dump bodies, or mining chutes.
Look for suppliers that provide heat numbers, inspection certificates, chemical analysis, and traceable production records. Independent laboratory reports can strengthen confidence, especially for demanding construction and mining applications. Experienced suppliers should also discuss welding procedures, cutting limits, delivery protection, and replacement planning. Technical advice matters. So does honesty.
This guide will compare leading suppliers through measurable criteria, including product consistency, certifications, customization, logistics, technical support, and customer feedback. It will distinguish actual manufacturing capability from simple trading activity. A supplier may offer fast delivery but limited grade options. Another may provide excellent steel but weak after-sales communication. No supplier is perfect.
The 2026 market may also expose weaknesses that product brochures hide. Delivery estimates can change. Batch performance can vary. Even a respected company deserves verification before a major purchase. Readers should request recent documents, inspect sample plates when possible, and match each offer with the working environment. Price remains important, but premature savings can create costly downtime. This introduction sets a practical framework for finding a dependable abrasion resistant steel plate supplier, without treating rankings as permanent or unquestionable.
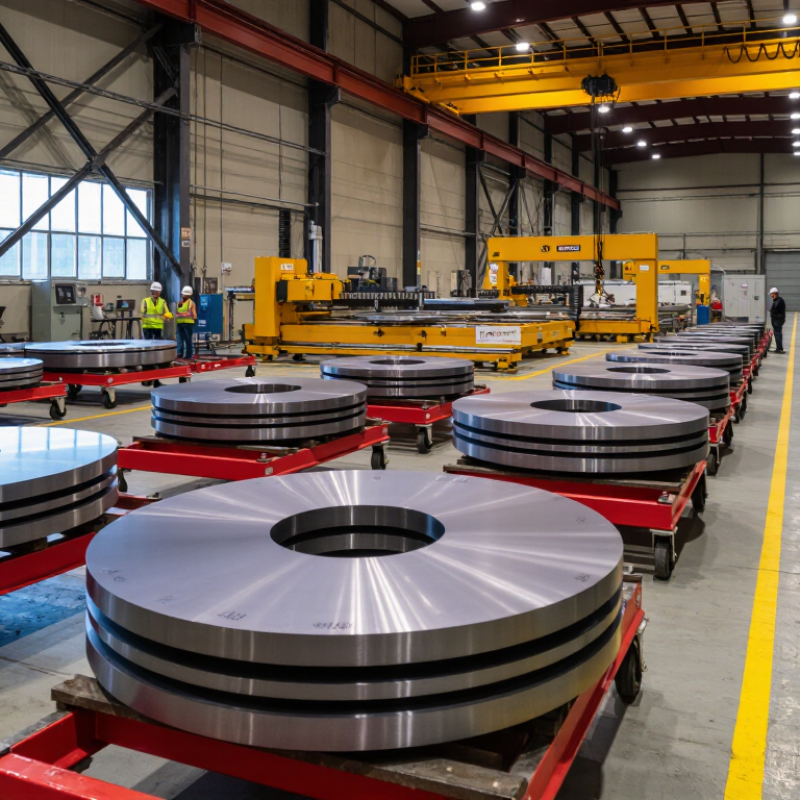
Choosing the best abrasion-resistant steel plate supplier in 2026 requires more than comparing prices. AR400, AR500, and AR600 grades describe nominal hardness levels, commonly measured in HBW. Higher hardness can extend service life in quarry liners, dump bodies, chutes, and mining screens. However, hardness alone does not guarantee better performance. Plate thickness, impact conditions, steel chemistry, and cutting quality also matter.
In practical projects, AR400 often balances wear resistance and easier fabrication. AR500 suits severe sliding abrasion, while AR600 handles aggressive wear with stricter processing requirements. Welding and drilling become less forgiving as hardness rises. A reliable supplier should provide heat numbers, mill test certificates, dimensional records, and verified hardness results. I have seen plates fail early because the selected grade was too hard for repeated impact. That choice looked efficient on paper, but field conditions proved otherwise.
Tips: Ask for hardness mapping across the plate, not one test point. Confirm the actual HBW range and thickness tolerance. Request cutting and welding guidance before production begins. Check whether the supplier can trace every plate to its original heat. Keep samples for independent testing when the application is costly. AR600 may impress during a wear test, yet AR400 can perform better where impact and fabrication dominate. There is no perfect grade.

When comparing abrasion resistant steel plate suppliers in 2026, check the stated ASTM grade carefully. The reference “ASTM A磨” is incomplete and should not appear on a purchase order. ASTM A128 mainly covers high-manganese austenitic steel castings, not conventional rolled plate. A capable supplier should explain this difference before offering material. It should also provide the full grade, heat number, thickness, delivery condition, and applicable test documents.
EN 10025 covers structural steel products, including grades such as S355. It does not automatically certify abrasion resistance. If a supplier links EN 10025 steel to wear service, request supporting hardness and impact data. Ask where the hardness was measured. Plate edges, surfaces, and cut zones can produce different results. The material certificate should identify the test method and sampling location clearly.
ISO 6506 defines Brinell hardness testing with a controlled indenter, load, and measurement procedure. A reliable supplier should show HBW results, test equipment calibration, and traceability to the supplied heat. Do not judge wear life from hardness alone. Impact, sliding distance, load, moisture, and particle shape matter too. This is where many comparisons become too simple. A higher number may look convincing, yet poor welding practice can reduce service performance. In practical sourcing, trial samples and site records often reveal more than a polished certificate. Mistakes still happen, especially when standards are mixed without technical review.
| Standard or Checkpoint | Primary Scope | Relevant Material or Test | Key Technical Requirement | Evidence to Request from a Supplier | Purchasing Relevance |
|---|---|---|---|---|---|
| ASTM A128/A128M | Steel castings with austenitic manganese properties. | Cast Hadfield manganese steel, commonly used for severe impact and impact-abrasion service. | Grade-specific chemical composition, casting quality, heat treatment, and mechanical requirements must be verified against the ordered grade. | Material test certificate, chemical analysis, heat-treatment records, casting identification, and dimensional inspection report. | Suitable for cast wear components such as liners, jaws, mantles, and impact parts; it is not a general hot-rolled abrasion-resistant plate specification. |
| EN 10025-2 | Hot-rolled products made from non-alloy structural steels. | Structural steel grades such as S235JR, S275JR, and S355JR. | Grade designation covers yield strength, tensile strength, elongation, delivery condition, and impact toughness class. | Inspection certificate compliant with EN 10204, heat number, chemical composition, tensile-test results, impact-test results where applicable, and dimensional data. | Useful for structural support frames and fabrication around wear systems, but it does not by itself classify a plate as abrasion-resistant. |
| ISO 6506-1 | Method for determining Brinell hardness of metallic materials. | Brinell hardness testing using a tungsten-carbide ball indenter. | Results are reported in HBW and must identify the test force and ball diameter, for example HBW 10/3000. | Hardness-test report showing test location, surface preparation, equipment identification, test force, ball diameter, individual readings, and average value. | Provides a standardized hardness verification method; it does not define the chemical composition or wear grade of the steel plate. |
| Plate Hardness Verification | Confirms whether the delivered plate matches the ordered wear-grade requirement. | Brinell hardness, typically supplemented by tensile or impact testing when specified by the material standard. | Acceptance limits must be stated in the purchase order because ISO 6506-1 defines the test method rather than a universal hardness range. | Test map covering representative locations, calibrated equipment records, and traceability from test coupon to plate heat number. | Important for assessing expected wear life, weldability planning, and consistency between production batches. |
| Chemical-Composition Control | Verifies alloying elements and identifies material grade. | Carbon, manganese, silicon, chromium, nickel, molybdenum, boron, and other elements as applicable to the ordered grade. | Values must remain within the limits specified by the applicable product standard or manufacturer’s technical specification. | Heat-specific mill test certificate, spectrometer analysis, and a clear link between the certificate, plate marking, and packing list. | Helps prevent substitution of structural steel for wear-resistant material and supports welding procedure selection. |
| Dimensional and Surface Inspection | Checks plate geometry and surface condition before shipment or fabrication. | Thickness, length, width, flatness, edge condition, surface defects, and plate identification. | Tolerances should be agreed according to the applicable product standard, order specification, or approved drawing. | Dimensional inspection report, surface-inspection record, photographs, packing list, and plate-marking details. | Reduces cutting loss, fit-up problems, rework, and disputes related to visible defects or incorrect dimensions. |
| Weldability Documentation | Assesses fabrication risks when wear plate is welded to structures or components. | Carbon-equivalent information, recommended consumables, preheating guidance, interpass-temperature limits, and post-weld instructions. | Welding requirements depend on grade, thickness, chemical composition, restraint, hydrogen control, and service conditions. | Welding guide, welding procedure specification, carbon-equivalent calculation, consumable recommendations, and qualified procedure records where required. | Essential for avoiding cold cracking, excessive heat-affected-zone hardness, distortion, and premature service failure. |
| Traceability and Certification | Maintains a documented link between supplied products and manufacturing records. | Heat number, plate number, batch number, production date, and inspection documentation. | Markings on the plate should correspond with the certificate and shipping documents without gaps in identification. | EN 10204 inspection certificate, certificate of conformity, packing list, heat-treatment record, and independent inspection report when contracted. | A core supplier qualification indicator for projects requiring audits, warranty support, or regulated quality documentation. |
| Application Matching | Matches the material selection to the dominant wear mechanism. | Sliding abrasion, impact abrasion, gouging abrasion, erosion, corrosion, or combined wear. | No single steel grade is optimal for every wear condition; hardness, toughness, thickness, geometry, and operating temperature must be considered together. | Technical recommendation based on operating data, sample application history, wear mechanism analysis, and clearly stated limitations. | Helps avoid selecting a harder but less tough material where impact loading or fabrication requirements are dominant. |
Choosing the best abrasion-resistant steel plate supplier requires more than comparing price lists. Mill capacity should match your order pattern, not only the supplier’s maximum output. Ask whether the mill produces plate internally or relies on subcontracting. A stable mill can usually confirm rolling schedules, furnace capacity, and monthly availability. Request recent production records, not vague capacity claims. Small details matter. A delayed heat can stop fabrication for days.
Plate thickness is equally important. Confirm the available range, tolerance, flatness, and cutting limits for your design. A supplier may offer 6–100 mm plates, yet struggle with consistent quality at extreme thicknesses. Ask for test reports linked to heat numbers. These reports should show hardness, chemical composition, impact performance, and ultrasonic testing when required. Thickness variation can affect welding preparation and replacement costs.
Certifications also reveal operational discipline. Look for a current quality-management certificate and material documents such as EN 10204 3.1, when applicable. Verify certificate validity independently. Lead time deserves practical questioning. Request separate estimates for production, inspection, cutting, packing, and ocean transport. A quoted four-week delivery may exclude testing. That is a common gap. In my experience, suppliers who explain delays honestly are often more dependable than those promising impossible speed. Still, no evaluation is perfect; capacity figures can change after maintenance, energy shortages, or sudden demand. Build a small schedule buffer.
Choosing a 2026 abrasion resistant steel plate supplier requires more than comparing hardness values.
Field experience shows that impact toughness often decides whether a plate survives sudden loading. Ask for Charpy V-notch results at the intended service temperature. A high hardness number can still hide brittle behavior.
Wear loss should be measured under realistic conditions. Request the test method, abrasive type, load, sliding distance, and reported volume loss.
Laboratory results are useful, but they may not match crushed stone, coal, or recycled metal in service. Small differences in test setup can change the ranking. Numbers matter.
Yield strength indicates resistance to permanent deformation during heavy loading. Confirm the minimum value, testing direction, plate thickness, and heat number.
Weldability also needs practical evidence. Review carbon equivalent, recommended preheat, consumable selection, interpass temperature, and heat-affected-zone hardness.
Supplier engineers should provide welding procedures, inspection records, and traceable mill certificates. A useful supplier can explain limitations without hiding behind a data sheet.
Perfect comparisons are unrealistic. Some suppliers publish impressive wear results but omit impact conditions or weld repair guidance. That omission deserves questions, not assumptions.
Before purchasing, compare complete test records with the actual bucket edge, chute liner, or structural panel application. A few minutes with an independent inspector may prevent expensive cracking later.
Choosing the best abrasion resistant steel plate supplier in 2026 requires more than comparing the lowest quoted price. A reliable comparison starts with grade, thickness, plate weight, testing, and delivery terms. Price should be measured per usable tonne, not only per tonne quoted. Cutting waste, packaging, and inland transport can change the final cost significantly. The cheapest quote can still be expensive.
Global logistics deserve close attention. Ask whether the supplier can provide mill certificates, heat numbers, inspection records, and accurate export documents. Confirm production schedules and port options before placing an order. A strong logistics team should explain lead times clearly, including possible delays caused by vessel changes or customs checks. These details are easy to overlook.
Custom cutting can reduce workshop labor, but precision depends on plate hardness, thickness, and cutting method. Plasma cutting may leave a heat-affected edge, while other methods may improve finish but increase cost. Specify dimensions, tolerances, hole locations, and edge requirements in writing. Support matters after delivery, too. Useful suppliers respond quickly to technical questions and help resolve shortages or dimensional issues with evidence. Still, no supplier is perfect. Cutting plans may need revision, and delivery estimates can shift. Independent inspection is sensible for critical projects, especially when downtime would be costly.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







