2026 Best Burr Oak Fin Press Types for Global Buyers
Choosing a Burr Oak Fin Press in 2026 requires more than comparing tonnage, speed, and price. Global buyers must examine production goals, fin geometry, material thickness, energy use, service access, and operator training. A compact press may suit prototypes and short runs. A servo-driven production line may perform better beside automated coil feeding and inspection equipment.
David A. Burr, a recognized leader associated with Burr Oak Tool, has stated, “The best tooling solution begins with understanding the customer’s complete manufacturing process.” That principle remains practical. A press should not be judged alone. Its payoff depends on die change time, alignment stability, scrap control, and available technical support. Ask difficult questions early.
This guide compares major Burr Oak Fin Press types for buyers across HVAC, refrigeration, automotive, and industrial heat-transfer markets. It considers mechanical presses, hydraulic systems, servo presses, and integrated forming lines. Each section connects machine design with real workshop conditions, including noisy floors, limited space, changing alloy batches, and demanding delivery schedules. No model wins everywhere. That assumption deserves scrutiny.
Some recommendations may remain conditional. Published specifications do not always predict daily performance. A machine that looks efficient on paper may require costly tooling adjustments or specialized maintenance. Buyers should request sample-part trials, reference installations, warranty details, and total ownership estimates. Regional voltage, import requirements, spare-parts logistics, and technician availability also matter. Careful selection reduces avoidable downtime and supports safer, more consistent production.
Burr Oak Fin Presses: Definition, Purpose, and Core Functions
Burr Oak Fin Presses: Definition, Purpose, and Core Functions
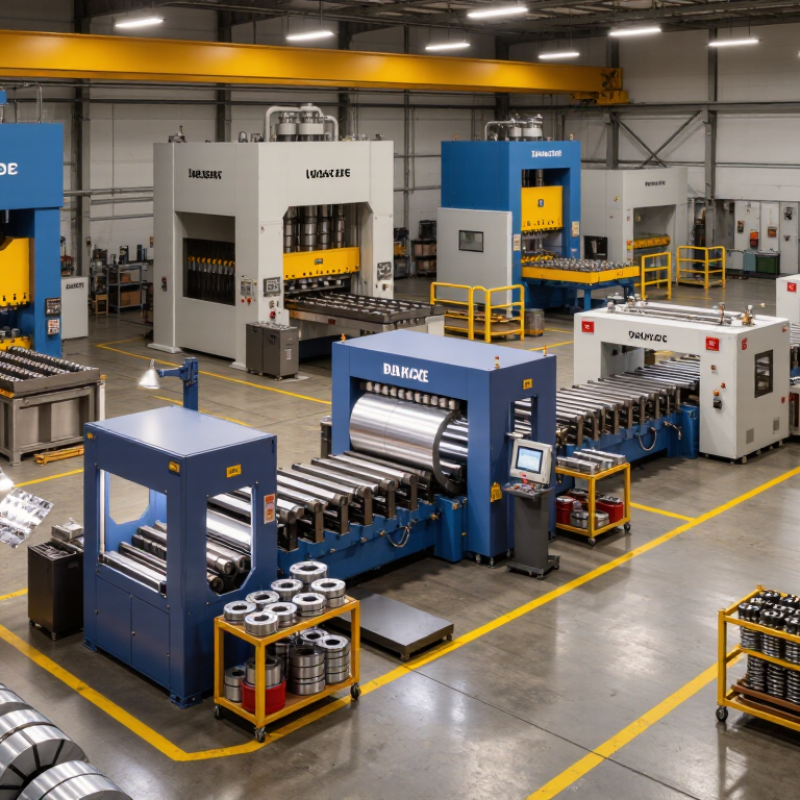
Burr oak fin presses are industrial machines that form thin metal strips into heat-transfer fins. They commonly process aluminum coils for evaporators, condensers, radiators, and other heat-exchange equipment. The press feeds, pierces, louver-cuts, and separates the strip at controlled intervals. Some systems also stack finished fins automatically.
The purpose is practical: increase surface area while keeping airflow resistance manageable.
The International Energy Agency’s Future of Cooling report states that cooling already uses about 10% of global electricity. It also projects cooling demand could more than triple by 2050. That pressure makes consistent fin production increasingly important for global buyers.
Core functions include coil feeding, progressive stamping, fin-height control, pitch adjustment, scrap removal, and output counting. A stable feed system protects delicate aluminum from buckling. Small errors matter. A slight pitch variation can affect coil performance and assembly fit.
I would not judge a press by speed alone. Tooling life, changeover time, sensor accuracy, and operator access deserve equal attention. The International Energy Agency’s Energy Efficiency 2023 report also emphasizes efficiency improvements across industrial systems, so buyers should examine motor consumption and idle-time controls. A faster machine is not always the better machine.
Key Specifications for Comparing Fin Press Performance
2026 Best Burr Oak Fin Press Types for Global Buyers
When comparing fin press performance, start with measurable specifications, not catalog claims. Check rated force, stroke length, strokes per minute, feed accuracy, and supported strip thickness. For heat-exchanger fins, a practical press often needs stable feeding within ±0.05 mm. Small errors can distort louvers, holes, or burr-oak profile details. Press speed also matters, but only when the die remains consistent.
Energy deserves equal attention. The U.S. Department of Energy’s Industrial Assessment Centers report that participating plants often identify energy-saving opportunities worth 8% to 12% of annual consumption. Therefore, compare motor power, idle consumption, and energy per thousand parts. A higher-speed machine may waste energy during setup or frequent stoppages. That part is easy to overlook.
Safety and maintenance reveal real performance. ISO 12100 recommends documented risk assessment, while ISO 13849 supports evaluating control-system reliability. Ask for guarding details, emergency-stop response, lubrication intervals, and measured noise levels. In my experience, a press with 98% theoretical uptime can deliver less than 85% in a dusty workshop. That gap needs honest testing. Request production samples, scrap-rate records, and a two-shift trial before purchasing.
Material, Tooling, and Automation Options for Global Buyers
For global buyers, fin press selection should begin with material, not speed. Aluminum remains the practical choice for lightweight heat-transfer fins, while copper supports higher thermal conductivity but increases material cost. The International Aluminium Institute reported global primary aluminum production above 70 million tonnes in 2023, confirming a deep supply base for international sourcing.
Material changes the tooling decision. Thin aluminum strip needs polished guides, controlled roll forming, and accurate fin collars. Copper demands stronger cutting edges and closer wear monitoring. Progressive dies suit stable, high-volume production. Modular tooling works better when fin height, pitch, or louver patterns change frequently. Small errors become visible quickly.
Automation affects more than labor. The International Federation of Robotics recorded 541,302 industrial robot installations worldwide in 2023. A fin press with automatic feeding, vision inspection, and coil monitoring can reduce handling variation. It can also create expensive downtime when sensors are poorly calibrated. That part is often underestimated. Buyers should request cycle-time evidence, scrap data, spare-part lead times, and maintenance records.
The heat exchanger market context is also relevant. MarketsandMarkets projected strong global growth through 2028, driven by energy, transport, and industrial cooling demand. However, that forecast covers heat exchangers broadly, not fin presses alone. Treat it as directional evidence, not a purchasing guarantee. A reliable comparison should test actual strip samples under production-speed conditions. Fancy automation may fail without disciplined tooling maintenance.
Safety Standards, Maintenance Needs, and Purchasing Considerations
For global buyers, fin press selection should match material thickness, coil width, stroke rate, and production volume. Mechanical presses suit high-speed lines with stable tooling. Hydraulic presses offer adjustable force for thicker or fragile fin stock. Pneumatic models work well for lighter-duty forming, but compressed-air quality matters. An undersized press may create uneven pitch, burrs, and premature die wear.
Safety needs documented proof, not attractive specifications. The International Labour Organization reported nearly three million work-related deaths globally in 2023. OSHA 29 CFR 1910.212 requires guarding at machine points of operation. Buyers should request interlocked doors, emergency stops, two-hand controls, and verified safeguarding tests. ISO 12100 risk assessment and ISO 13849-1 control-system validation provide useful benchmarks. Ask for noise readings, electrical schematics, and operator training records. Small omissions become expensive later.
Maintenance should be visible and measurable. Check lubrication points, guide clearance, die alignment, and pneumatic leaks during scheduled inspections. Keep spare seals, sensors, cutting inserts, and critical fasteners locally available. The U.S. Department of Energy’s 2022 compressed-air assessment guidance notes that leaks can waste a significant share of generated air, although actual losses depend on system condition. A lower purchase price can therefore hide higher operating costs. I would also verify service response times, voltage compatibility, installation space, and documentation language. These details are easy to overlook. They deserve a written comparison.