A modern Edi Water System can produce high-purity water continuously, but the “best” unit depends on the feed water, required quality, and operating conditions. EDI, or electrodeionization, is commonly installed after reverse osmosis. It combines ion-exchange resins with selective membranes and a direct-current field to remove dissolved ions. The EDI Water System Working Principle is straightforward: ions move through membranes into concentrate channels, while the resin helps them travel through the dilute chamber. The electric field also regenerates the resin during operation.
The details matter. In a typical plant, operators check feed conductivity, pressure, flow, and product-water resistivity. If pretreatment is poor, hardness or suspended solids can foul components and shorten service life. A stable reading is useful, but it does not explain every change in performance; trends and alarm history matter too. EDI reduces the need for routine chemical regeneration, yet it is not a maintenance-free box. Feed-water limits, sanitization procedures, and monitoring requirements vary by manufacturer and system design.
For buyers comparing 2026 models, capacity, recovery, energy use, controls, and service access deserve close attention. Ask for performance data at your actual feed-water conditions, not just a headline specification. Small details, such as space to replace a module or reach a sample valve, can affect daily operation. “Best” is a moving target. A carefully sized system may outperform a larger, costlier one, though that decision still needs verification with qualified water-treatment professionals.
2026 Best EDI Water System How Does It Work?
An EDI water system uses electricity, ion-exchange membranes, and resin to reduce dissolved ions in water. EDI means electrodeionization. In many treatment plants, reverse osmosis removes much of the dissolved material first. The EDI stage then draws remaining charged ions through selective membranes into a separate concentrate stream. The resin helps ions move through the unit, while the electric field continually regenerates it. No routine chemical regeneration is needed, but the system still needs suitable feed water and regular checks.
That matters. EDI is one step in a treatment train, not a complete water-treatment solution. Feed-water quality, pressure, temperature, and flow can affect product quality. Operators often monitor conductivity or resistivity and watch for changing trends. EDI also does not reliably remove every uncharged contaminant or guarantee microbial control. One practical detail is easy to miss: a neat process diagram cannot show every site-specific issue, such as a fouled pretreatment filter. Real systems need real monitoring.
Tips: Check the reverse-osmosis water before it enters EDI, and follow the equipment maker’s operating limits. Record conductivity or resistivity consistently. If readings drift, investigate the feed and operating conditions before assuming the EDI unit itself has failed.
| System Dimension | How It Works | Typical Feed or Output | Role in Water Treatment | Key Selection or Operating Consideration |
|---|---|---|---|---|
| Feed-water quality | EDI receives low-ion water, most commonly permeate produced by reverse osmosis (RO). | RO permeate; actual limits for conductivity, hardness, silica, carbon dioxide, and other constituents depend on the EDI module. | Provides the controlled feed needed for effective continuous deionization. | Check the module’s feed-water specification and the complete pretreatment design. EDI is generally not intended to treat untreated source water directly. |
| Ion-exchange resin | Resin beads temporarily capture dissolved cations and anions, helping transport ions through the dilute compartment. | Dissolved ionic contaminants in the RO permeate. | Supports ion removal between the membrane barriers. | Feed quality and flow distribution affect performance. Resin does not make EDI a general-purpose filter for suspended solids or organic contaminants. |
| Ion-exchange membranes | Alternating cation- and anion-selective membranes guide positively and negatively charged ions toward concentrate compartments. | Ions migrate out of the product-water stream into a separate concentrate stream. | Separates ionic contaminants from the water being purified. | Membranes are selective for charged species; they do not replace particle filtration or organic-contaminant treatment. |
| Direct-current field | An applied DC electric field drives ion migration through the resin and across the selective membranes. | Electrical power and properly conditioned feed water. | Enables continuous ion removal and helps regenerate the resin during operation. | Voltage, current, temperature, and flow must remain within the equipment manufacturer’s operating limits. |
| Continuous resin regeneration | The electric field splits a small amount of water into hydrogen and hydroxide ions, which help restore the resin’s ion-exchange capacity. | Hydrogen and hydroxide ions are formed within the EDI stack. | Allows the unit to operate continuously without routine chemical regeneration of the EDI resin. | “Chemical-free regeneration” applies to the EDI process itself; the wider water-treatment plant may still use chemicals for pretreatment or cleaning. |
| Dilute and concentrate streams | The dilute stream becomes the purified product, while the concentrate stream carries removed ions away from the stack. | Separate product-water and concentrate-water outlets. | Provides a continuous route for removing contaminants rather than storing them in the product stream. | Concentrate flow, recovery, and disposal or reuse arrangements are system-specific and should be confirmed during design. |
| Product-water quality | EDI reduces dissolved ionic species after RO; performance is monitored using suitable water-quality instruments. | High-purity water; some well-designed systems can produce water approaching 18.2 MΩ·cm resistivity at 25°C under appropriate conditions. | Provides a polishing step for applications requiring low ionic contamination. | Resistivity alone does not establish overall water purity. Silica, boron, dissolved gases, organics, particles, and microbiological quality may require separate monitoring or treatment. |
| Typical process sequence | Common arrangement: pretreatment → RO → EDI → storage and distribution, with additional polishing where the application requires it. | Each stage is selected for the source water and the final quality requirement. | Places EDI after RO as a polishing technology rather than as a standalone treatment train. | Final design depends on source-water analysis, required product-water quality, demand, sanitization needs, and applicable regulations. |
| Monitoring and maintenance | Operators track feed and product quality, flow, pressure, temperature, and electrical readings; pretreatment and instrumentation are maintained. | Routine operating data and water-quality measurements. | Helps identify feed-water changes, scaling or fouling risks, and declining performance. | Use the supplier’s operating and maintenance guidance, and verify product quality with calibrated instruments and appropriate sampling practices. |
Note: EDI performance and operating limits vary by system design, feed-water composition, and application. Confirm specifications with the selected equipment documentation and a qualified water-treatment designer.
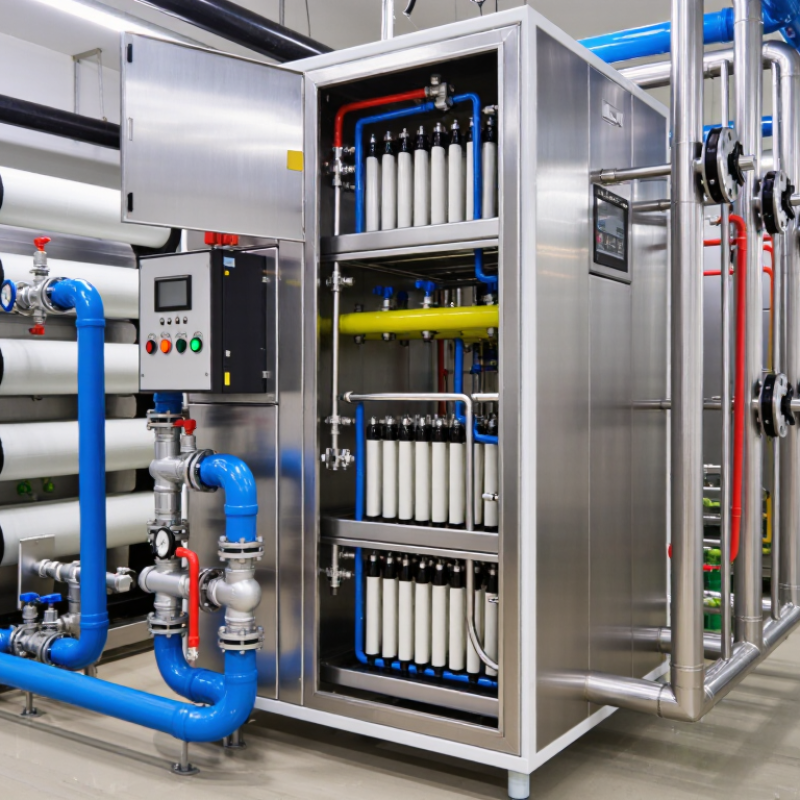
A practical EDI water system is built around several connected components, each protecting the next. Pretreatment filters remove suspended solids and reduce scale-forming minerals. A reverse osmosis unit then lowers the dissolved-ion load before water reaches the EDI module. That step matters. EDI performs best with consistent, low-salinity feed water, not untreated source water.
Inside the EDI module, alternating ion-exchange membranes form dilute and concentrate channels. Ion-exchange resins fill the dilute channels, where they capture remaining charged particles. A direct-current power supply drives those ions through the membranes and into the concentrate stream. Water molecules split into hydrogen and hydroxide ions, helping regenerate the resin during operation. The process is continuous, but it still depends on stable flow and suitable feed quality.
The system also needs pumps, valves, a concentrate drain, and monitoring instruments. Conductivity sensors track product-water quality, while pressure and flow readings can reveal a blocked filter or an uneven channel. Small changes matter. Operators should check readings over time, not rely on one attractive number on a display. In practice, controls may be overlooked during system planning; that can make troubleshooting harder later. The EDI module is the centerpiece, but reliable performance comes from the whole treatment train.
This illustrative example shows conductivity falling from 10 µS/cm in reverse-osmosis permeate to 0.1 µS/cm in EDI product water. Actual results depend on feedwater quality and system operating conditions.
How it works: RO permeate enters resin-filled dilute chambers. Cation- and anion-exchange membranes separate these chambers from concentrate channels. A direct-current electric field moves dissolved ions through the membranes into the concentrate stream, while the resin supports continuous ion removal and regeneration. The purified water exits as EDI product.
Pretreated water, usually reverse-osmosis permeate, enters the dilute channels of an electrodeionization (EDI) module. Inside, ion-exchange resin helps dissolved ions move toward charged membranes under direct current. Cations and anions pass through selective membranes into separate concentrate channels; purified water continues to the product outlet. The electric field also splits water molecules, continually regenerating the resin. No chemical regeneration is normally needed. The concentrate stream carries rejected ions away.
Feed quality matters. Hardness, carbon dioxide, silica, and sudden flow changes can affect product quality or performance. Operators typically track conductivity, resistivity, temperature, pressure drop, and product flow. Small details count.
A USGS Circular 1441 report estimated U.S. thermoelectric withdrawals at about 133 billion gallons per day in 2015; most was cooling water, not EDI feed. Still, it illustrates the scale of water handling in power generation. EDI treats only a small, high-purity stream within that larger system.
A neat process diagram can make operation look effortless. It isn’t always: fluctuating pretreatment can push readings off target, so actual feed limits and product specifications must be checked against the system design and application.
2026 Best EDI Water System How Does It Work?
How Ion-Exchange Resins and Electricity Remove Dissolved Ions
An electrodeionization (EDI) system uses ion-exchange resin, selective membranes, and direct current to reduce dissolved ions in water. Feed water passes through narrow channels packed with cation and anion resins. These resins capture positively and negatively charged ions. Think of them as tiny exchange sites along the water’s path. The process is continuous.
Here is the key interaction. An electric field pulls cations toward the cathode and anions toward the anode. Selective membranes guide these ions into separate concentrate channels, away from the purified-water stream. Meanwhile, the field splits some water molecules into hydrogen and hydroxide ions. These help restore the resin’s exchange capacity as it operates. No chemical regeneration is normally needed.
In practice, the picture is less tidy. Feed-water quality, flow rate, and electrical conditions all affect performance. Too much hardness or other troublesome ions can cause scaling or reduce output, so pretreatment matters. Small details count. Operators monitor conductivity and pressure, not just the display’s product-water reading. EDI is not a substitute for good system design, and its performance should be checked against the intended water-quality requirements. One point worth questioning: a low conductivity reading alone does not describe every impurity in the water.
How to Choose an EDI System for Your Water Quality Needs in 2026
Choosing an EDI system starts with the water your process actually needs, not the largest capacity on a specification sheet. List target conductivity or resistivity, silica, boron, and organic-carbon limits, then identify where samples will be taken.
ASTM D1193-19 sets a minimum resistivity of 18 megohm-centimeters at 25°C for Type I reagent water. That is a useful benchmark, not a promise that an EDI unit alone will deliver it. High-purity systems commonly pair reverse osmosis with EDI and, where needed, final polishing.
Small details matter: a long pipe run or a poorly placed sample point can distort readings.
For pharmaceutical applications, compare the design with the relevant compendial tests. USP General Chapter <645> gives a Stage 1 conductivity limit of 1.3 microsiemens per centimeter at 25°C for applicable purified water and water for injection testing. Confirm the required test method and limits with your quality team.
Check feed-water variation, temperature range, recovery, and alarms; ask for performance data under conditions close to your own. EDI mainly removes ionized contaminants. Nonionic organics and microbes may need separate treatment.
Not always obvious.
I would also verify service access and routine monitoring plans before purchase. A system can meet a factory test and still struggle when feedwater shifts seasonally.
That gap deserves attention.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru