Choosing the right High Quality Pipe Machine Equipment in 2026 requires more than comparing prices and production speed. Manufacturers must examine pipe materials, diameter ranges, wall thickness, tolerance requirements, and expected output. A machine built for HDPE may not suit PVC, PPR, steel, or multilayer applications. The wrong match can create uneven walls, unstable dimensions, and costly material waste.
This guide introduces key equipment types, including pipe extrusion machines, injection molding systems, spiral pipe machines, corrugation lines, and precision cutting units. Each category serves a different production purpose. Extrusion lines support continuous manufacturing, while injection systems produce shaped fittings with repeatable accuracy. Corrugation equipment creates flexible drainage pipes with defined profiles. Small details matter. Cooling tanks, haul-off units, die design, and automatic control systems can influence final quality as much as the main machine.
Reliable selection should combine practical experience with supplier documentation, factory testing, and verified customer feedback. Look for clear specifications, accessible spare parts, operator training, and responsive technical support. A polished brochure is not enough. Ask how the machine performs after years of daily operation. Review energy use, maintenance intervals, safety functions, and control-system stability before making a decision.
No machine is perfect.
Even advanced equipment may require adjustment when raw materials change or production conditions shift. This article compares leading machine types through a practical, evidence-based perspective. It also highlights limitations that buyers may overlook, helping manufacturers choose dependable equipment with realistic expectations and stronger long-term value.
Pipe Machine Equipment: Definition, Purpose, and Industrial Applications
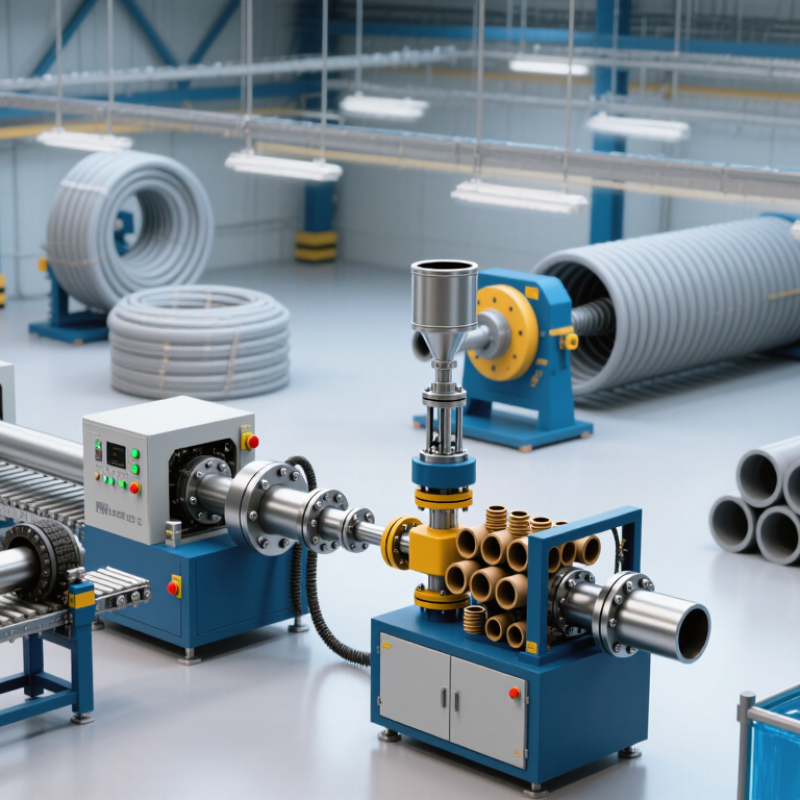
Pipe machine equipment includes the tools and systems used to form, cut, weld, bend, and finish pipes. Common types include tube mills, pipe bending machines, threading machines, and automated cutting units. Their main purpose is to produce accurate pipes with consistent dimensions and reliable surface quality. In practical operations, equipment selection depends on pipe material, diameter, wall thickness, and production volume. Not every machine fits every workshop.
These machines support construction, water management, energy, transportation, and general manufacturing. A tube mill can shape steel strips into continuous welded pipes. A bending machine creates smooth curves for fluid lines and structural frames. Cutting and end-finishing equipment prepares clean connections for later assembly. On a production floor, sensors help control speed, pressure, and alignment. Small errors matter. A slight bend can affect installation, sealing, or long-term safety.
Tips: Check material compatibility before purchasing equipment. Review motor power, tooling range, maintenance access, and operator safety features. Keep calibration records and inspect welds regularly. A specification may look perfect on paper, yet real production conditions can expose weaknesses. Trial runs are useful, although they can reveal issues that planning missed. Clear training and practical maintenance routines often improve results more than extra automation.
High-quality pipe manufacturing begins with choosing the right machine for the material, diameter, and production target. Extrusion lines form plastic pipes by pushing heated polymer through a calibrated die. They usually include a cooling tank, haul-off unit, and automatic cutting system. Small temperature errors can create uneven walls. That detail is easy to underestimate.
For steel and stainless applications, tube mills shape strip into round sections before welding the seam. High-frequency welding machines create continuous joints, while laser systems can offer narrow, precise weld zones. Roll-forming stations must stay aligned; otherwise, pipes may twist or show unstable dimensions.
Seamless pipe equipment works differently. It uses piercing, elongation, and sizing processes to produce pipes without a longitudinal weld. These systems require stronger process control and careful inspection.
Other important machine types include pipe straighteners, end-facing units, threading machines, hydrostatic testers, and surface treatment lines. A reliable production cell connects these stages with sensors, traceable records, and regular calibration. In practical machine evaluations, testing equipment deserves the same attention as forming equipment. A beautiful surface cannot hide weak pressure performance. Energy use, changeover time, maintenance access, and operator safety also affect real quality. The fastest line is not always the best choice. Sometimes, a simpler system produces more consistent results. That trade-off deserves honest review.
2026 Best High Quality Pipe Machine Equipment Types
Key Components and Operating Principles of Pipe Machines
Choosing high-quality pipe equipment in 2026 requires more than comparing output rates. Each machine must match the material, diameter, wall thickness, and production target. Common types include extrusion lines, spiral forming machines, and seamless pipe systems. Their essential components include a rigid frame, drive motor, gearbox, forming unit, cooling section, haul-off unit, and cutter. A programmable controller coordinates these parts. Sensors monitor temperature, speed, pressure, and alignment.
In an extrusion machine, heated material moves through a rotating screw inside a barrel. The screw melts, mixes, and pushes the material through a die. The die shapes the pipe continuously. Vacuum sizing then controls its outside diameter, while cooling stabilizes the structure. Haul-off rollers maintain consistent speed. Cutting equipment produces fixed lengths. Even a small temperature drift can create uneven walls. That assumption is often wrong.
Reliable operation depends on calibration, maintenance, and operator judgment. Experienced technicians inspect screw wear, die surfaces, roller pressure, and cooling flow before production. They also compare sensor readings with physical measurements. A clean control panel cannot correct poor mechanical alignment. No setup is perfect. Operators may overlook vibration because the pipe still looks acceptable. However, vibration can signal bearing wear or unstable feeding. Regular checks reduce waste and support repeatable quality, although real production is less tidy than technical manuals suggest.
Key components, operating principles, and representative pipe diameter capabilities
The chart shows representative outside-diameter ranges commonly associated with different pipe-processing equipment. Actual capability depends on material, die design, tooling, cooling capacity, wall thickness, and production speed.
A heated barrel melts thermoplastic resin, while a rotating screw conveys and pressurizes the melt through a forming die. Main components include the hopper, screw, barrel, die, vacuum sizing tank, cooling tank, haul-off, and cutter.
Intermeshing screws provide intensive mixing and controlled melting for PVC compounds. Typical components include gravimetric feeders, twin screws, temperature zones, a die head, sizing equipment, cooling sections, and a haul-off.
A continuous extruder forms the pipe while paired molding blocks create the corrugated profile. The system normally includes an extruder, corrugator, forming molds, cooling system, haul-off, and cutting unit.
Pipe ends are faced, heated with a plate, and pressed together under controlled pressure to form a joint. Key components are the clamping frame, hydraulic unit, facing tool, heating plate, and control system.
2026 Best High Quality Pipe Machine Equipment Types
High-quality pipe equipment must prove more than production speed. It should protect operators, maintain dimensional accuracy, and support stable output. ISO 12100 recommends structured risk assessment and risk reduction during machine design. ISO 13849 also guides safety-related control systems. These standards matter beside the machine, not only inside manuals.
Performance deserves measurable evidence. The International Energy Agency reported that industry consumed about 37% of global final energy in 2022. Efficient drives, controlled heating, and reduced scrap can therefore influence operating costs and emissions. The World Steel Association recorded approximately 1.89 billion tonnes of crude steel production in 2023. That scale increases pressure on forming, cutting, welding, and testing equipment. In practice, a strong pipe line should hold diameter tolerance, weld consistency, and surface quality across long production runs. Real factories are less perfect. Material variation, worn tooling, and rushed maintenance still create failures.
Tips: Check emergency stops, guarding, interlocks, and noise levels during a live demonstration. Request test data using your actual pipe grade and dimensions. Measure scrap rates, changeover time, and energy use, rather than trusting brochure claims. Keep calibration records and inspect rollers before visible defects appear. A useful purchase decision includes operator feedback. Engineers may overlook awkward access points, and operators often notice them first.
| Equipment Type | Primary Application | Typical Pipe Materials | Key Quality Indicators | Relevant Standards and References | Important Safety Features | Performance Evaluation Criteria |
|---|---|---|---|---|---|---|
| Plastic Pipe Extrusion Line | Continuous production of solid-wall thermoplastic pipes and tubes. | PE, PP, PVC, ABS, and multilayer thermoplastics. | Outside diameter, wall thickness, ovality, surface finish, melt homogeneity, and dimensional stability. | ISO 4427 for PE water pipes; ISO 1452 for PVC-U pressure pipes; ISO 12100 for machinery risk assessment. | Guarded rotating parts, emergency stops, temperature and pressure alarms, electrical protection, and controlled access to heaters. | Stable melt pressure, consistent haul-off speed, accurate temperature control, low scrap rate, and repeatable dimensions. |
| Twin-Wall and Corrugated Pipe Line | Production of structured-wall pipes for drainage, sewerage, cable protection, and non-pressure applications. | HDPE, PP, and PVC. | Profile geometry, ring stiffness, joint integrity, inner-wall smoothness, length accuracy, and layer bonding. | ISO 9969 for ring stiffness; ISO 21138 for structured-wall thermoplastics pipes; ISO 12100 for machinery safety. | Interlocked guards, mold-zone protection, pinch-point protection, emergency stops, and cooling-water monitoring. | Uniform corrugation pitch, stable vacuum forming, consistent wall structure, and reliable socket dimensions. |
| Pipe Belling and Socketing Machine | Forms sockets for push-fit joints on cut thermoplastic pipe sections. | PVC-U, PVC-O, ABS, PP, and PE-based systems where specified. | Socket diameter, insertion depth, roundness, sealing-groove accuracy, and material integrity. | Applicable product standards such as ISO 1452 and ISO 16135, depending on pipe material and application. | Heater shielding, guarded clamping areas, over-temperature protection, emergency stops, and safe tool-change procedures. | Repeatable heating cycle, controlled forming force, short changeover time, and accurate socket dimensions. |
| Butt Fusion Welding Machine | Joins thermoplastic pipe ends by heating and pressing aligned faces together. | PE, PP, and other compatible thermoplastics. | Pipe alignment, heating temperature, bead formation, fusion pressure, joining time, and cooling time. | ISO 21307; ASTM F2620; ISO 12100; ISO 13849-1 for safety-related control systems where applicable. | Guarded heating plate, anti-crush controls, pressure relief, electrical grounding, emergency stop, and secure pipe clamps. | Accurate pressure control, low misalignment, repeatable fusion cycles, reliable data logging, and uniform weld beads. |
| Electrofusion Control Unit | Supplies controlled electrical energy to electrofusion fittings for pipe joining. | PE and compatible polyethylene systems. | Voltage and current stability, barcode or parameter accuracy, fusion time, cooling control, and joint traceability. | ISO 12176-2; ISO 12176-3; ISO 12176-4; ISO 21307 where applicable to the joining system. | Overcurrent protection, earth-leakage protection, insulated connectors, overheating alarms, and automatic cycle interruption. | Stable output, accurate fusion parameters, automatic fault detection, data recording, and compatibility with specified fittings. |
| CNC Pipe Cutting and Chamfering Machine | Cuts pipe to length and prepares ends for sockets, welding, threading, or mechanical connections. | Steel, stainless steel, ductile iron, PVC, PE, and other specified materials. | Cut-length accuracy, perpendicularity, burr level, chamfer angle, surface condition, and repeatability. | ISO 12100; IEC 60204-1; applicable dimensional tolerances specified by the pipe product standard. | Blade guarding, interlocked doors, chip containment, two-hand or safeguarded controls, emergency stops, and lockout provisions. | Cutting repeatability, tool life, spindle stability, automatic measurement, low vibration, and efficient material handling. |
| Pipe Threading and Grooving Machine | Produces threaded or grooved ends for detachable pipe connections. | Carbon steel, stainless steel, galvanized steel, and other machinable metals. | Thread profile, pitch, groove width, groove depth, concentricity, burr control, and dimensional conformity. | ASME B1.20.1 for inch pipe threads; ISO 7-1 for pipe threads where applicable; ISO 12100. | Chuck guarding, overload protection, coolant management, foot or emergency stop, and protection from rotating workpieces. | Threading accuracy, groove consistency, tool-change time, spindle torque, chip evacuation, and surface quality. |
| Pipe Coating and Lining Equipment | Applies corrosion protection, insulation, abrasion resistance, or internal lining to pipe surfaces. | Steel, ductile iron, concrete, and compatible thermoplastic or composite systems. | Coating thickness, adhesion, holiday detection, surface cleanliness, cure level, coverage, and uniformity. | ISO 21809 series for pipeline coatings; ISO 8501-1 for surface preparation; ISO 12944 for corrosion protection principles. | Ventilation, dust and vapor extraction, grounding, explosion-risk controls where required, temperature monitoring, and PPE provisions. | Controlled application speed, stable coating thickness, efficient curing, low overspray, and repeatable surface preparation. |
| Hydrostatic Pressure Test Bench | Verifies pressure resistance and leakage performance of pipes and fittings using water. | Plastic, steel, copper, ductile iron, and other pressure-rated pipe products. | Pressure stability, test duration, pressure decay, leak detection, end-load control, and calibrated measurement. | ISO 1167 for thermoplastics; ISO 9080 for long-term hydrostatic strength evaluation; applicable product standards. | Physical barriers, pressure relief valves, interlocked access doors, automatic depressurization, remote operation, and protected hose connections. | Pressure-control accuracy, stable water temperature, calibrated sensors, automated test records, and safe cycle completion. |
| Air and Vacuum Leak Tester | Detects leaks, porosity, or inadequate sealing in pipes, fittings, and assembled systems. | Thermoplastics, elastomers, metals, and assembled pipe systems. | Leak rate, pressure decay, test repeatability, sealing quality, temperature compensation, and calibrated instrumentation. | ISO 20485 for leak testing principles; ISO 12100; product-specific pressure and leakage requirements. | Pressure limitation, guarded test chambers, automatic venting, sensor fault detection, emergency stop, and safe fixture locking. | Detection sensitivity, cycle time, pressure stability, false-reject rate, calibration traceability, and digital reporting. |
| Pipe Inspection and Measurement System | Measures pipe geometry and identifies surface or dimensional defects during production or final inspection. | Thermoplastics, metals, composites, and lined pipes. | Diameter, wall thickness, ovality, surface defects, length, straightness, and defect classification. | ISO 3126 for thermoplastics pipe dimensions; ISO 4630 and applicable product-specific measurement standards. | Enclosed optical paths, laser safety controls, guarded moving components, electrical isolation, and clear status indication. | Measurement repeatability, calibration interval, sampling rate, defect-detection reliability, data traceability, and integration with line controls. |
Note: Applicable requirements depend on pipe material, pressure class, diameter range, joining method, installation environment, and the governing local regulations.
Selecting the best pipe machine equipment in 2026 requires more than comparing purchase prices.
Start with the pipe material, diameter range, wall thickness, and expected production volume. A machine designed for small irrigation pipes may struggle with heavy industrial tubing. Check these limits carefully.
During equipment trials, inspect the extrusion or forming line at operating speed, not only during an empty demonstration. Watch the temperature display, motor vibration, cooling stability, and cutting accuracy. Ask for measured output data from similar materials. Independent test records are more useful than polished sales claims. Also examine control access, emergency stops, guarding, and maintenance space. A cramped layout can turn a simple repair into hours of downtime.
Energy use matters in 2026. Select systems with stable heating zones, efficient drives, and clear power-monitoring functions. Confirm whether spare parts, technical training, and remote support are realistically available in your region. I once focused too heavily on maximum speed and overlooked changeover time. That decision looked efficient on paper but increased daily losses. Allow operators to test the controls. Their practical feedback may reveal problems that specifications hide. Choose equipment that delivers consistent quality, not impressive numbers alone.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru