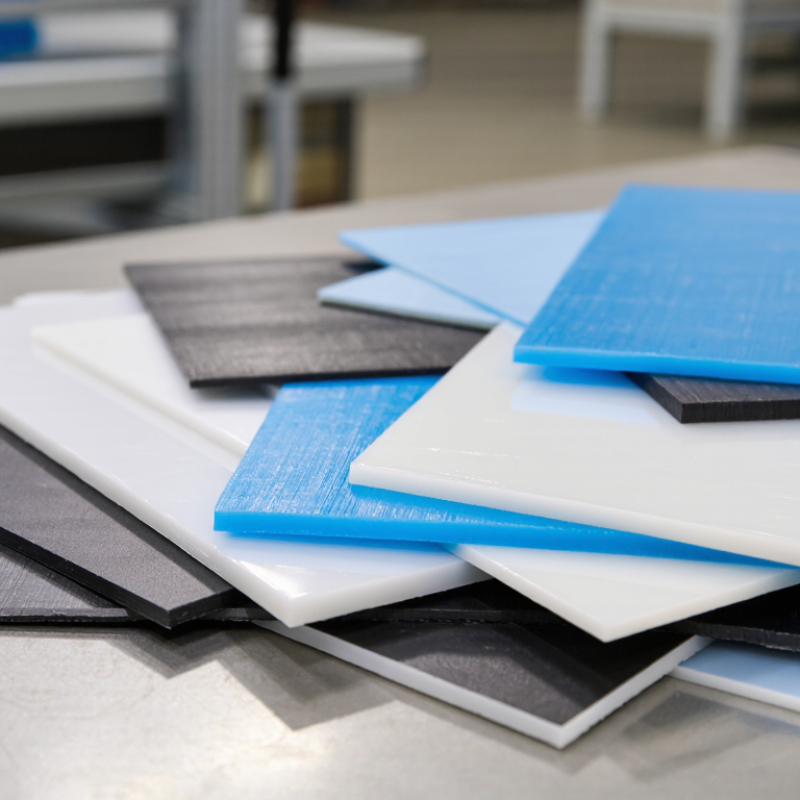
For global buyers, choosing the right Polyethylene Boards in 2026 requires more than comparing prices. Material grade, thickness, density, surface finish, and fabrication quality can change performance significantly. A board used for marine fendering faces different demands than one used for food-processing tables or warehouse liners. The best option depends on load, moisture, temperature, impact, and cleaning conditions.
This guide examines leading polyethylene board options through practical purchasing criteria. It considers virgin and recycled materials, HDPE and UHMW-PE properties, dimensional stability, wear resistance, and machining behavior. It also reviews supplier transparency, production consistency, testing documents, and export experience. Buyers should request technical data sheets, sample pieces, tolerances, and batch information before placing large orders. Small details matter.
Real-world sourcing is rarely perfect. Product descriptions may use similar terms while hiding meaningful differences in density or formulation. Some suppliers provide impressive samples but inconsistent production batches. That risk deserves attention. This overview therefore balances performance claims with verification steps, helping procurement teams compare suppliers more fairly. It does not assume one board fits every application. Cost, service life, delivery reliability, and technical support must be evaluated together. Experienced buyers may still need independent testing for demanding projects, especially when boards face continuous abrasion, heavy loads, or repeated temperature changes. The goal is practical confidence, not exaggerated certainty.
Polyethylene Boards: Definition, Structure, and Main Types
Polyethylene boards are solid thermoplastic sheets made from polyethylene resin. They resist moisture, many chemicals, and repeated impacts. In practical use, their smooth surfaces are easy to clean. They also avoid splintering, unlike many wooden boards. A board’s performance depends on density, molecular weight, thickness, and processing quality.
The main types include LDPE, HDPE, and UHMWPE. LDPE feels softer and bends more easily, making it suitable for flexible liners and light-duty protection. HDPE offers better stiffness and wear resistance for cutting surfaces, machine guards, and fabricated parts. UHMWPE contains extremely long molecular chains. This structure improves abrasion resistance and sliding performance, though machining can require careful tool control. I have found that a thicker board is not always stronger in service. Poor support can still cause bending.
Tips: Check the technical datasheet before purchasing. Confirm density, impact strength, working temperature, and chemical compatibility. Ask for sample testing when friction, food contact, or outdoor exposure matters. Measure flatness after storage, especially with large sheets. Some buyers overlook thermal expansion. That can create gaps, warped panels, or installation stress. A small trial often reveals problems that specifications miss.
2026 Top Polyethylene Boards for Global Buyers
Key Performance Factors for Comparing Polyethylene Boards
Choosing a polyethylene board starts with the working environment, not the catalogue photograph. A board used for marine guides faces different stress than one used for food-processing tables. Compare thickness tolerance, density, surface hardness, and impact resistance. Small variations can affect cutting accuracy and service life.
Temperature deserves close attention. Some grades remain tough in cold storage, while others become less forgiving below freezing. Ask for test data at the temperatures your operation actually reaches. Do not rely on room-temperature results alone. That shortcut can be costly.
Moisture absorption is usually low, but installation details still matter. Check expansion rates before fixing a large sheet to a metal frame. Allowing no movement may cause bowing or stressed fasteners. I have seen material perform well while the design around it failed. The board was blamed first.
Abrasion resistance should match contact pressure and movement speed. A sliding chute needs different evidence than a protective wall liner. Request wear-test methods, sample dimensions, and conditioning details. Without that information, numbers may look precise but remain difficult to compare.
For global purchasing, review lot traceability, dimensional inspection records, and consistent color or surface finish. Obtain samples from the intended production lot when possible. Verify certificates for the final application and destination market. A general statement of compliance is not enough.
No board wins every test. Cost, stiffness, machinability, and replacement intervals must be considered together. My own comparisons sometimes favor a less expensive grade, though only after its weak points are documented and accepted.
A practical comparison of common polyethylene board material options. Values are typical industry ranges and may vary according to resin grade, additives, processing method, thickness, and test standard.
| Comparison Factor | HDPE Board | UHMW-PE Board | LDPE Board | Recycled HDPE Board |
|---|---|---|---|---|
| Material Description | High-density polyethylene with a balanced combination of stiffness, toughness, chemical resistance, and processability. | Ultra-high-molecular-weight polyethylene designed for exceptional abrasion resistance and low-friction performance. | Low-density polyethylene with higher flexibility and impact absorption than standard HDPE. | HDPE manufactured partly or mainly from recovered polyethylene feedstock; properties depend strongly on feedstock sorting and formulation. |
| Typical Density | 0.94–0.97 g/cm³ | 0.93–0.94 g/cm³ | 0.91–0.94 g/cm³ | Approximately 0.93–0.97 g/cm³ |
| Typical Tensile Strength at Yield | 20–35 MPa | 20–35 MPa | 8–15 MPa | 18–32 MPa, depending on recycled content and quality control |
| Typical Flexural Modulus | 700–1,500 MPa | 500–1,000 MPa | 100–300 MPa | 600–1,400 MPa |
| Impact Performance | Very good; remains tough in many demanding handling applications. | Excellent resistance to impact and repeated mechanical loading. | Excellent impact absorption and flexibility. | Good to very good; variation is greater than with virgin material. |
| Abrasion Resistance | Good for general industrial and fabrication use. | Excellent; typically selected for chutes, liners, wear strips, and sliding components. | Moderate; softer surfaces can wear faster under abrasive contact. | Moderate to good, depending on formulation and surface quality. |
| Coefficient of Friction | Low to moderate; suitable for many sliding and conveying applications. | Very low; advantageous where low drag and material release are important. | Low to moderate. | Low to moderate, with possible batch-to-batch variation. |
| Operating Temperature Range | Approximately −50°C to +80°C for many general-purpose grades. | Approximately −150°C to +80°C for many grades; verify the specific grade and load conditions. | Approximately −50°C to +60°C for many general-purpose grades. | Approximately −40°C to +70°C in typical applications; verify the actual formulation. |
| Heat Deflection Temperature | Typically about 65–85°C under common test loads. | Typically about 60–85°C under common test loads. | Typically about 35–50°C under common test loads. | Typically about 60–85°C, depending on recycled content and grade. |
| Chemical Resistance | Excellent resistance to many acids, alkalis, salts, and aqueous chemicals. | Excellent resistance to many corrosive chemicals; check compatibility with strong oxidizers and solvents. | Good resistance to many aqueous chemicals; less suitable for some solvents and elevated-temperature exposure. | Good in general, but contaminants and composition variability should be evaluated for critical service. |
| Moisture Absorption | Very low, generally below 0.01% by weight at 23°C and 50% relative humidity. | Very low, generally below 0.01% by weight. | Very low, generally below 0.01% by weight. | Very low; surface contamination and porosity may affect practical performance. |
| UV and Weathering Performance | Good when stabilized with carbon black or approved UV additives. | Good when UV-stabilized; unstabilized material may degrade during long outdoor exposure. | Moderate unless specifically UV-stabilized. | Variable; request outdoor-weathering data and UV-stabilizer information for exterior use. |
| Machinability and Fabrication | Easy to saw, drill, route, weld, and thermoform with suitable equipment. | Machinable, but its toughness and low thermal conductivity require controlled cutting conditions. | Easy to cut and fabricate; flexibility may reduce dimensional stability during machining. | Generally machinable, although inclusions and property variation can affect surface finish. |
| Dimensional Stability | Good for normal service; thermal expansion should be considered in precision installations. | Good in wear applications, but thermal expansion and creep must be considered under sustained loads. | Lower stiffness can lead to greater deflection and dimensional change under load. | Moderate to good; verify tolerance capability for precision components. |
| Long-Term Load Performance | Good when designed for creep and temperature effects. | Good wear life, but sustained structural loads require careful design against creep. | Limited for rigid load-bearing applications because of lower stiffness. | Suitable for non-critical loads when performance consistency is confirmed. |
| Common Thickness Availability | Approximately 1–100 mm; thicker custom plates are available from some processors. | Approximately 3–100 mm; thicker or machined formats may require special production. | Approximately 1–50 mm, subject to manufacturing method and application. | Approximately 3–50 mm, depending on recycled feedstock and production process. |
| Typical Applications | Fabricated tanks, cutting boards, machine guards, wear pads, marine components, and industrial liners. | Chute liners, hopper liners, guide rails, wear strips, sliding pads, and high-abrasion components. | Flexible liners, impact pads, packaging-related components, seals, and low-load protective surfaces. | Construction protection boards, pallets, temporary flooring, agricultural products, and general-purpose fabricated parts. |
| Food-Contact Suitability | Potentially suitable when manufactured from compliant grades and processed under applicable regulations. | Potentially suitable for certain applications when the specific grade is compliant; do not assume compliance from the material name alone. | Potentially suitable for compliant grades used within their approved temperature and application limits. | Often restricted for direct food contact unless the recycled feedstock and manufacturing process meet the relevant regulations. |
| Recyclability | Widely recyclable as polyethylene when collected and sorted correctly. | Recyclable as polyethylene, although collection and separation may be less common. | Recyclable as polyethylene, subject to local collection infrastructure. | Already incorporates recovered polyethylene; end-of-life recyclability depends on sorting and contamination. |
| Best Selection Priority | Balanced performance, broad availability, fabrication ease, and general industrial use. | Maximum wear life, low friction, and demanding sliding or abrasion service. | Flexibility, cushioning, and impact absorption at relatively low loads. | Lower material footprint or cost for applications where tight property consistency is not essential. |
| Key Buyer Verification Documents | Technical data sheet, lot certificate, dimensional tolerance, UV-stabilization details, and applicable compliance declaration. | Technical data sheet, wear-test method, coefficient-of-friction data, impact data, and dimensional tolerance. | Technical data sheet, hardness, tensile data, temperature limits, and flexibility or elongation information. | Recycled-content declaration, batch traceability, contamination controls, technical data sheet, and application-specific test results. |

Note: Tensile strength, flexural modulus, impact resistance, wear rate, and temperature limits are test-method- and grade-dependent. Global buyers should request current technical data sheets, certificates of analysis, regulatory declarations, and representative samples before approving a polyethylene board for production use.
For 2026 procurement, polyethylene boards should be selected by application, not by a single “best” grade. High-density polyethylene suits cutting surfaces, tank liners, and general fabrication because it offers low moisture absorption and reliable impact resistance. UHMW-PE works better where sliding wear is severe, such as conveyor guides, chute liners, and material handling points. Low-density polyethylene remains useful for flexible pads, seals, and protective layers. Each option solves a different problem.
Food processors often choose smooth, non-porous HDPE boards for tables and cutting areas. Confirm the required food-contact documentation for the destination market. Marine fabricators may prefer UV-stabilized sheets for fender strips, dock components, and boat interiors. Outdoor signs and agricultural guards need color stability, thickness control, and suitable fastening plans. A board that performs indoors may warp or fade outdoors. That detail is easy to miss.
For heavy industry, thickness, density, friction, and operating temperature deserve practical testing. Ask for batch data, tolerances, and machining guidance before placing a large order. CNC routing can leave rough edges if feeds are poorly adjusted. A recurring purchasing lesson is simple: low price can create higher replacement costs. It happens. No polyethylene board is perfect; creep under constant load remains a concern. Review load duration, support spacing, cleaning chemicals, and local recycling rules. Global buyers should also compare packaging, export protection, and technical support, not only the quoted sheet price.
Top polyethylene board options for different global applications
The chart compares representative typical tensile strength and flexural modulus values for common polyethylene and related thermoplastic board options. UHMWPE is generally selected for high-wear applications, HDPE for balanced chemical and impact resistance, LDPE for flexibility and impact absorption, and polypropylene for higher stiffness and process-temperature requirements. Values are typical material ranges represented by midpoint estimates; actual performance depends on grade, thickness, processing, temperature, and regulatory requirements.
International buyers should treat certification as evidence, not decoration. A reliable supplier provides current ISO 9001 records, material certificates, and batch-level inspection reports. The documents should identify polyethylene grade, density, thickness tolerance, and production date. Generic certificates create uncertainty.
Food-contact applications require region-specific compliance evidence. Buyers may request migration testing, a declaration of conformity, and supporting laboratory data. REACH and RoHS documentation can matter for industrial projects, but their relevance depends on the destination and application. Always check the importing market’s current requirements. Rules change.
Physical quality is equally important. Inspectors should measure thickness at several points, examine cut edges, and check warpage on a flat table. Impact strength, tensile performance, temperature resistance, and UV stability should match the intended use. A board can look smooth yet fail under repeated loading. That detail is easy to miss.
Traceability strengthens trust. Each shipment should connect to a production batch, test record, and packing list. Independent testing is useful when volumes are large or specifications are unfamiliar. Still, no certificate replaces careful sampling. Some purchasing checklists remain too general. They should include storage conditions, surface protection, allowable color variation, and corrective-action procedures. A small gap can become an expensive dispute.
Polyethylene boards remain a practical choice for industrial liners, fabrication, packaging, and marine projects. For 2026 buyers, price should be judged against the complete delivered cost. Budget by specification, not thickness alone. Board density, virgin or recycled content, surface finish, color, and cutting tolerance can change quotations significantly. A low ex-works price may become expensive after tooling, export packing, insurance, and inland transport.
Ask suppliers for a dated quotation with clear trade terms, minimum order quantity, production lead time, and payment conditions. Request a small sample before placing a large order. Check its actual thickness at several points. Inspect the edges, surface marks, warping, and flexibility under moderate pressure. Keep test records. They make later claims easier to verify. One overlooked detail is packaging. Thin boards can arrive with corner damage when stacked without rigid protection.
Supplier evaluation needs more than a polished website. Review factory capacity, quality procedures, material traceability, and recent export experience. Ask whether the supplier can provide dimensional reports and batch records. Confirm how rejected boards are handled. Communication speed matters, but technical accuracy matters more. An unclear answer about density is a warning sign. I have found that buyers sometimes compare quotations too early, before fixing specifications. That creates false savings and repeated revisions. Even careful inspections are imperfect. Weather, storage time, and transport conditions can affect board performance after delivery. Build reasonable tolerance into the purchasing plan, and document every agreed detail before production.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru