Choosing the right bolt in 2026 requires more than comparing prices, thread sizes, or polished product photos. Global buyers must evaluate strength, material, coating, dimensions, traceability, and service conditions together. A bolt used inside a dry warehouse faces different risks from one exposed to salt spray, vibration, or repeated temperature changes.
John H. Bickford, a respected fastening engineer and author, offered a useful reminder: “A bolt is a spring.” This short statement explains why preload, tightening control, and joint design matter. A high-strength bolt can still fail when installation is careless, friction changes, or the connected materials behave differently. Real-world experience often reveals details that catalogs hide.
This Bolt Guide examines common bolt types, including hex bolts, flange bolts, carriage bolts, eye bolts, socket head bolts, and structural fasteners. It connects their designs with practical applications across construction, machinery, automotive production, energy, and maintenance. Buyers should also review standards such as ISO 898-1, ASTM F3125, and relevant regional specifications. Certification and test reports deserve attention.
Small details matter.
For example, a zinc-plated bolt may suit an indoor frame but perform poorly near coastal equipment. A stainless steel option may resist corrosion better, yet it can create galling during installation. These choices are not always simple. No guide can replace engineering judgment, supplier verification, or field inspection. That limitation should remain visible. This 2026 overview aims to make comparisons clearer, while acknowledging that the best bolt depends on the complete joint, not the bolt alone.
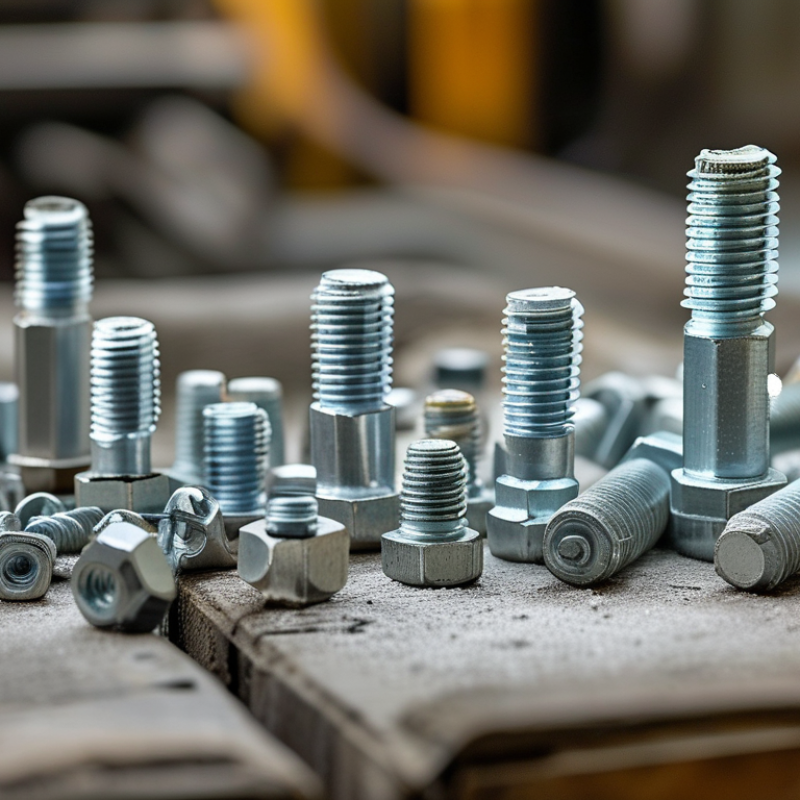
Bolts are small components with a major structural responsibility. They connect steel frames, bridge plates, equipment bases, and modular building sections. Their performance depends on more than diameter. Thread form, material strength, coating, length, and installation torque all influence the joint.
A hex-head bolt suits many general connections. High-strength structural bolts support heavily loaded steel assemblies. Anchor bolts secure columns to concrete foundations, while flange bolts help distribute pressure around connected surfaces. Stainless and coated options can reduce corrosion in coastal or humid environments. However, no bolt works everywhere. A marine site, a cold warehouse, and a dry interior project require different assessments.
Proper selection begins with the joint design. Engineers should check tension, shear, vibration, temperature, and access for tools. The washer, nut, hole size, and tightening method must match the assembly. A clean thread matters. So does calibrated equipment. On a real site, dust and rushed installation can change the final preload, even when the specification looks perfect.
Global construction also demands traceable documentation. Buyers should request material certificates, dimensional records, coating details, and inspection results from qualified suppliers. Digital project models can identify bolt locations before delivery, reducing missing parts and rework. Yet digital control is not enough. I have seen accurate schedules fail when field conditions changed. A short site review can prevent a costly correction.
Bolt selection becomes clearer when buyers classify three features: head shape, thread design, and intended function. Hex-head bolts suit general structural and machinery work. Socket-head bolts fit recessed spaces where a wrench cannot turn easily. Carriage bolts use a rounded head and square neck, limiting rotation through timber or thin metal.
Shape matters, but it is not the whole decision. U-bolts clamp pipes, cables, and curved supports. Eye bolts provide lifting or anchoring points, but their rated use must be verified carefully. Stud bolts have threads at both ends and often serve flanged connections. In field inspections, mismatched head clearance causes many avoidable delays. Measure the installation space before ordering.
Thread choice affects assembly, vibration resistance, and replacement. Coarse threads usually tolerate dirty conditions and offer faster installation. Fine threads can provide better adjustment and stronger engagement in some applications. Full-thread bolts distribute engagement along the joint, while partial-thread designs may offer useful shear positioning. Metric and inch-based systems must never be mixed casually. Check diameter, pitch, length, strength grade, material, and coating against the drawing.
Function should guide the final choice. A fastening bolt for a steel frame differs from one used in equipment maintenance. Washers, nuts, tightening method, and corrosion exposure also change performance. A neat catalog table can still mislead. Recheck the real load, joint movement, and service temperature before approval. Overspecification is not always safer; poor fit remains poor engineering.
2026 Top Bolt Types Guide for Global Buyers
Bolt selection starts with the load, environment, and installation method. ISO 898-1 classifies carbon and alloy steel bolts by mechanical performance. Class 8.8 provides about 800 MPa tensile strength and 640 MPa yield strength. Class 10.9 reaches approximately 1,000 MPa tensile strength. Higher grade is not automatically safer. It can increase brittleness, tightening sensitivity, and hydrogen embrittlement risk after plating.
Match the material to the service conditions. Use carbon steel for protected structural joints and controlled indoor equipment. Choose stainless steel for moisture, food-processing areas, or frequent washing. Austenitic stainless grades resist corrosion well, but they may gall during installation. Apply suitable lubrication and control torque. For elevated temperatures, verify creep resistance and strength retention. ASTM F3125 covers structural heavy hex bolts, while ASTM F593 covers stainless steel fasteners.
Corrosion planning deserves equal attention. The World Steel Association reported 1,888.2 million tonnes of crude steel production in 2023. This scale supports broad steel availability, but it does not guarantee traceable bolt quality. Require mill certificates, lot identification, hardness results, and coating details. A recurring field mistake is mixing metric property classes with inch-based strength grades. They are not interchangeable. I would also question blindly choosing the strongest bolt. Joint design, washer fit, thread engagement, and actual torque control often matter more. Small details decide failure.
Minimum mechanical properties of commonly specified metric bolt grades. Carbon and alloy steel values are based on ISO 898-1 property classes; stainless-steel values are based on ISO 3506-1 property classes. Select the grade according to load, corrosion exposure, temperature, and installation requirements.
Tensile strength indicates the minimum stress required to break the fastener. Yield strength or 0.2% proof stress indicates the minimum stress before significant permanent deformation. Stainless grades improve corrosion resistance, while higher carbon/alloy-steel classes generally provide greater load capacity.
Global bolt buying in 2026 requires more than matching diameter and length. The World Steel Association reported 1.888 billion tonnes of crude steel production in 2023. That scale supports broad supply, but it also creates inconsistent specifications across markets. ISO 4014 defines dimensions for partially threaded hexagon head bolts. ISO 898-1 covers mechanical properties for carbon and alloy steel fasteners. Inch-based products follow different dimensional systems, such as ASME B18.2.1. A 20 mm bolt is not automatically compatible with a 3/4-inch bolt. Thread pitch, flank form, head size, and length measurement can differ.
During practical inspections, I check the mating nut, thread gauge, washer clearance, and marked property class. The marking matters. A class 8.8 bolt should not be replaced casually with a stainless product of similar appearance. ASTM F3125 also separates structural bolt grades and assemblies, so project drawings must control the purchase. Check the standard edition.
A useful buyer record includes nominal diameter, pitch, thread length, head dimensions, material, coating, strength class, and test certificate. The International Organization for Standardization states that ISO 898-1 applies specific tensile and hardness requirements, not merely visual identification. Metric coarse threads often suit general assembly, while fine threads may improve adjustment but demand closer inspection. I have seen drawings omit pitch. That small gap caused reordering, wasted time, and uncertain fit. Supplier data should be verified against calibrated gauges and the receiving inspection plan. Temperature, corrosion exposure, and preload requirements may also change the correct selection.
| Bolt Type | Common Standards | Typical Nominal Sizes | Thread Dimensions | Head or Drive Dimensions | Common Strength or Material Options | Compatibility Checks |
|---|---|---|---|---|---|---|
| Metric Hexagon Head Bolt | ISO 4014 partially threaded; ISO 4017 fully threaded; DIN 931 and DIN 933 equivalents | M6–M24 commonly stocked; larger sizes available for engineered applications | Coarse pitch: M6 × 1.0, M8 × 1.25, M10 × 1.5, M12 × 1.75, M16 × 2.0, M20 × 2.5, M24 × 3.0 | Across-flats examples: M6 10 mm, M8 13 mm, M10 16 mm, M12 18 mm, M16 24 mm, M20 30 mm, M24 36 mm | Carbon or alloy steel property classes 8.8, 10.9, and 12.9; stainless steel A2-70 or A4-70 under ISO 3506-1 | Match metric nut thread, pitch, length, property class, coating, and required head clearance. Do not substitute for inch threads. |
| Unified Inch Hexagon Head Bolt | ASME B18.2.1; Unified National Coarse (UNC) and Unified National Fine (UNF) | 1/4–1 in commonly stocked; larger diameters used in heavy-duty applications | Examples: 1/4-20 UNC or 1/4-28 UNF; 3/8-16 UNC or 3/8-24 UNF; 1/2-13 UNC or 1/2-20 UNF; 3/4-10 UNC or 3/4-16 UNF | Across-flats examples: 1/4 in 7/16 in, 3/8 in 9/16 in, 1/2 in 3/4 in, 3/4 in 1-1/8 in, 1 in 1-1/2 in | SAE Grade 5, SAE Grade 8, and corrosion-resistant stainless steel grades selected according to the applicable specification | Confirm nominal diameter, UNC or UNF pitch, thread class, head dimensions, strength grade, and inch-based measuring requirements. |
| Flange Head Bolt | ISO 4162; DIN 6921; ASME B18.2.1 for applicable inch designs | M5–M20 commonly used in machinery, vehicle assemblies, and equipment frames | Metric coarse pitches such as M6 × 1.0, M8 × 1.25, M10 × 1.5, and M12 × 1.75; fine pitches are application-specific | Integral circular flange distributes clamp load; flange diameter depends on nominal size and standard series | Steel property classes 8.8 and 10.9 are common; stainless options are available for lower or corrosion-focused loads | Check flange diameter, bearing-surface design, wrench size, thread pitch, washer requirement, and clearance around the flange. |
| Socket Head Cap Screw | ISO 4762; DIN 912; ASME B18.3 for inch versions | M3–M20 commonly used; larger sizes require application-specific verification | Typical metric coarse pitches: M4 × 0.7, M5 × 0.8, M6 × 1.0, M8 × 1.25, M10 × 1.5, M12 × 1.75 | Internal hex drive; common key sizes include 3 mm for M4, 4 mm for M5, 5 mm for M6, 6 mm for M8, 8 mm for M10, and 10 mm for M12 | Alloy steel property classes 8.8, 10.9, and 12.9; stainless steel versions available under relevant material specifications | Verify socket depth, tool access, recess engagement, minimum edge distance, thread engagement, and material strength. |
| Countersunk Hex Socket Screw | ISO 10642; DIN 7991; ASME B18.3 for inch versions | M3–M16 commonly used in flush-mount assemblies | Metric coarse pitches such as M4 × 0.7, M5 × 0.8, M6 × 1.0, M8 × 1.25, and M10 × 1.5 | 90° countersunk head; internal hex drive; countersink diameter and depth must match the selected screw size | Alloy steel classes commonly include 10.9 and 12.9; stainless alternatives are used where corrosion resistance is prioritized | The mating hole must have the correct 90° countersink, sufficient material thickness, and adequate head seating area. |
| Carriage Bolt | DIN 603; ASME B18.5 | Metric M5–M16; inch sizes commonly range from 1/4 to 5/8 in | Metric coarse threads or UNC threads; thread length varies by product configuration | Rounded or domed head with a square neck; square-neck dimensions must match the prepared hole | Low-carbon steel, zinc-coated steel, stainless steel, and higher-strength versions depending on the specification | Check square-neck width and depth, panel thickness, head clearance, thread system, and resistance to rotation during tightening. |
| Eye Bolt | DIN 580 for lifting eye bolts; ASME B18.15 for selected inch designs | M6–M64 depending on lifting capacity and design configuration | Metric thread sizes are commonly used; pitch and thread length must be taken from the exact standard and size | Circular eye dimensions and shoulder geometry vary by nominal size; shoulder type is important for angular loading | Forged steel or stainless steel; lifting-rated products require marked working load limits | Use only for loads permitted by the applicable standard. Verify working load limit, load direction, shoulder seating, and thread engagement. |
| U-Bolt | Dimensions are often application-specific; selected designs follow ASME B18.31.5 or project standards | Rod diameters commonly 6–24 mm; larger sizes are engineered for specific pipe or structural systems | Metric coarse or UNC/UNF threads; both legs must use the same specified thread | Inside width and inside height are critical; bent radius and leg length vary by application | Mild steel, high-strength steel, hot-dip galvanized steel, and stainless steel | Match pipe outside diameter or member width, inside height, plate thickness, nut system, coating, and allowable clamp load. |
| Structural Hex Bolt | ISO 7412; EN 14399 high-strength structural bolting assemblies; ASTM F3125 for selected inch structural systems | Metric M12–M36 commonly used in steel structures; larger sizes require project approval | Usually metric coarse pitch; thread length and grip length are specified for the structural assembly | Large hex head and bearing surface; dimensions depend on the relevant structural product standard | High-strength steel assemblies such as property class 8.8 or 10.9, with matching nuts and washers | Use a complete compatible assembly. Verify preload method, tightening procedure, nut class, washer type, coating, and inspection requirements. |
| T-Bolt | Application-specific; commonly designed for T-slots, aluminum profiles, and machine tables | M4–M12 are common; slot-compatible sizes depend on the profile or table system | Metric coarse pitches such as M5 × 0.8, M6 × 1.0, M8 × 1.25, and M10 × 1.5 | T-head width and thickness must fit the slot; head may rotate or slide into position depending on the design | Zinc-plated or stainless steel; strength selection depends on the clamping application | Confirm slot width, slot depth, neck geometry, insertion method, thread pitch, and maximum permissible clamping force. |
| Buyer verification note: Before ordering, confirm the complete designation: nominal diameter, thread system, pitch or TPI, thread length, total length, head style, strength or material grade, coating, applicable standard, nut and washer compatibility, and required inspection or certification documents. Metric and inch threads are not interchangeable even when their nominal diameters appear similar. | ||||||
Choosing the right bolt starts with the joint, not the catalog. Define load, material, temperature, vibration, and available installation space. Hex bolts suit many general connections, while flange bolts spread pressure under the head. Socket bolts help in tight spaces. Carriage bolts offer a smooth visible side, but their neck must fit the hole correctly.
Write a clear purchase specification. Include diameter, length, thread pitch, bolt type, strength class, surface treatment, and quantity. State whether measurements follow metric or inch-based standards. Ask suppliers for drawings, material certificates, coating details, and lot traceability. Samples should represent the actual production batch. A polished sample proves little.
Inspect the shipment before installation. Measure diameter, length, thread profile, head dimensions, and coating thickness. Check for burrs, cracks, rust, damaged threads, and mixed lots. A simple thread gauge can reveal problems quickly. For critical joints, use hardness testing and review test reports from a qualified laboratory. Do not rely on appearance alone.
I once treated matching labels as enough evidence. That was a poor assumption. Packaging can hide inconsistent batches. Recheck random cartons, record photographs, and compare results with the approved specification. If a bolt feels unusually soft or the thread binds, stop assembly and investigate the cause. Small deviations can become expensive failures.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru