Choosing welding equipment in 2026 requires more than comparing amperage, price, and brand names. A Mig Tig Welder can support fabrication, automotive repair, stainless steel work, and light industrial production. However, MIG and TIG solve different problems. MIG offers faster deposition and easier continuous welding. TIG provides cleaner control, sharper heat management, and better results on thin or visible joints.
Industry data supports careful equipment selection. The American Welding Society estimates that the United States may need 330,000 new welding professionals by 2028. This labor shortage increases interest in machines that reduce setup time and simplify operator training. Fortune Business Insights also projects continued growth in the global welding equipment market through the early 2030s. These trends encourage manufacturers to develop inverter machines, dual-process platforms, pulse controls, and more efficient power systems. Yet market growth does not make every machine suitable for every workshop.
Standards still matter. ISO 4063 identifies MIG and TIG processes as distinct welding methods, while OSHA guidance emphasizes ventilation, electrical safety, eye protection, and fire prevention. A reliable choice should match material thickness, duty cycle, wire or tungsten requirements, input power, and service support. A small garage may value portability and a 120-volt option. A fabrication shop may need stable three-phase output and a higher duty cycle. I would not claim one machine is universally best. That is where many buying guides become too confident. The right decision comes from real workpieces, measured power needs, operator skill, and the quality of the manufacturer’s technical support.
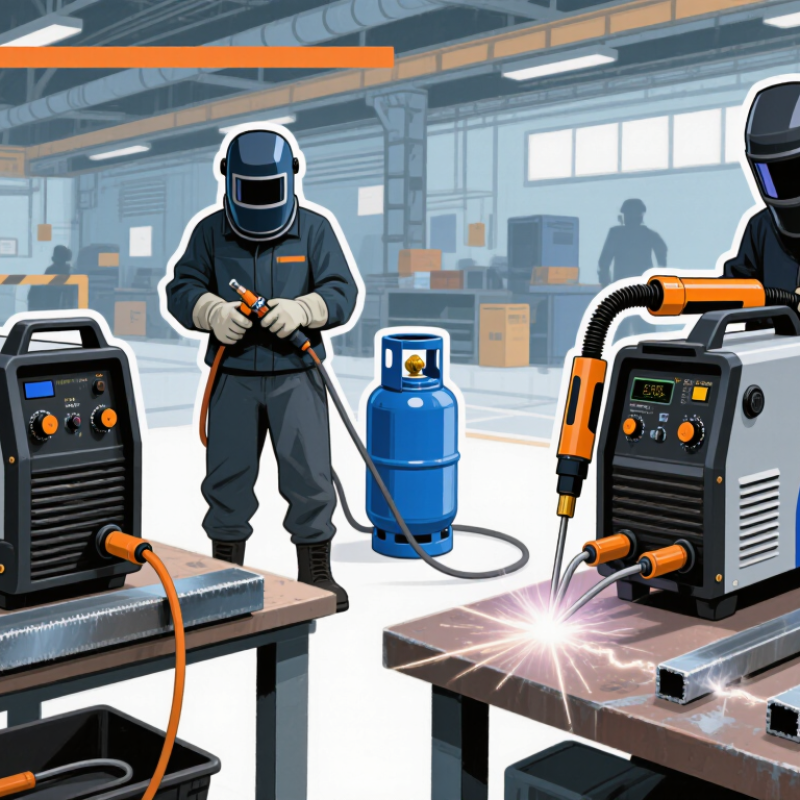
MIG and TIG welders create strong joints, but they work in noticeably different ways. MIG welding uses a continuously fed wire electrode. The wire melts into the joint while shielding gas protects the hot weld pool. This method is fast, practical, and easier for many beginners.
TIG welding uses a non-consumable tungsten electrode. The operator controls the arc with a torch and adds separate filler metal when needed. This gives excellent control over heat, bead shape, and appearance. TIG suits thin stainless steel, aluminum, and detailed repair work. It is slower, though. The process also demands steadier hands and cleaner surfaces.
A practical comparison makes the difference clearer. MIG feels like guiding a small, controlled stream of metal along the joint. TIG feels more like drawing with heat. MIG often handles production work and thicker steel efficiently. TIG rewards patience on delicate parts. Material thickness, joint position, surface cleanliness, and required appearance should guide the choice.
I have found that speed can hide poor preparation. A fast weld is not automatically a reliable weld. Beginners may also underestimate gas flow and torch angle. Small setting changes can affect penetration, spatter, and distortion. Checking a test piece first remains a sensible habit.
Good ventilation, suitable protective equipment, and correct machine settings are essential for every welding process.
In 2026, MIG and TIG welders are available in several practical configurations. MIG welders commonly use solid wire with shielding gas for clean steel, stainless steel, and aluminum work. Flux-cored MIG machines work without external gas, making them useful outdoors or in windy conditions. Some models support both wire systems, although changing settings takes patience.
TIG welders include DC, AC/DC, pulsed, and inverter types. DC TIG suits steel, stainless steel, and copper. AC/DC TIG is better for aluminum because alternating current helps break through surface oxide. Pulse control reduces heat input and can improve thin-sheet welds. High-frequency starts provide cleaner arc ignition, while lift starts are simpler and often more affordable. Small machines may support foot pedals, remote controls, or torch-mounted amperage adjustment.
The best type depends on material, thickness, workplace, and operator experience. For repair work, a dual-process machine can save space and handle varied jobs. For precise visible welds, TIG offers excellent control, but it demands slower hand movement and cleaner preparation. MIG is usually faster for frames and repeated joints. I would not call one process universally superior. In real workshops, the “best” choice can change after one awkward repair, a long extension cable, or unexpected aluminum contamination. Check duty cycle, amperage range, input power, gas compatibility, and service documentation before buying. Safety testing and proper ventilation remain essential.
Choosing between MIG and TIG welding starts with the material, not the machine’s appearance. MIG welding suits carbon steel and thicker sections because its continuous wire feeds quickly and supports productive fabrication. TIG welding offers finer control for stainless steel, aluminum, and thin sheet metal. It can produce clean, precise beads, but it demands steadier hand movement and better surface preparation.
Material thickness changes the decision. Thick steel frames may need MIG’s higher deposition rate, while a thin aluminum panel can benefit from TIG’s controlled heat. Joint position matters too. Overhead or awkward repairs may require adjustable current, stable arc control, and a manageable torch. I have found that higher amperage is not always better. Excess heat can warp sheet metal or weaken the surrounding area. A test weld often reveals mistakes that specifications cannot.
Tips: Match the wire or filler rod to the base metal. Clean oil, rust, and oxide layers before welding. Check shielding gas selection and flow, especially with aluminum. For frequent production work, consider duty cycle and wire-feed stability. For detailed repair work, prioritize low-current control and pedal response. Record the settings that work. Your first choice may need revision after testing. That is normal. A practical welder should fit the material, joint design, workspace, and operator’s real skill level.
Choosing between MIG and TIG welding in 2026 requires more than comparing amperage. Performance depends on arc stability, duty cycle, control accuracy, and material compatibility. MIG welders should offer steady wire feeding and adjustable voltage. TIG machines need precise amperage control and a reliable high-frequency start. Pulse settings can reduce heat distortion on thin stainless steel or aluminum. However, advanced controls cannot fix poor preparation or incorrect shielding gas.
Safety features deserve equal attention. Thermal overload protection helps prevent damage during demanding work. A stable ground connection reduces arc interruptions and shock risks. Clear warnings, insulated handles, and a balanced torch improve daily confidence. In a busy workshop, an easy-to-read display matters more than decorative functions. Test every control with gloves on. Small buttons can become frustrating.
Ease of use also affects weld quality. A lightweight machine is easier to move, but extreme lightness may suggest limited cooling capacity. Check the rated duty cycle under realistic conditions, not only the highest advertised setting. I have found that simple machines often produce better results when operators understand them fully. Still, this view is imperfect. A beginner may benefit from preset programs, while an experienced welder may prefer manual control. Inspect cable length, connector strength, fan noise, and replacement consumable access before buying. Practical details often decide whether a welder performs well after months of use.
Choosing the best MIG or TIG welder in 2026 starts with the material, not the machine’s advertised power. MIG welding suits steel fabrication, repairs, and longer seams. It uses a continuous wire, so beginners often gain stable results sooner. TIG welding gives cleaner control on stainless steel, aluminum, and thin sheet. The process is slower, but the weld bead can look precise and refined.
Check the required amperage, duty cycle, and input voltage before buying. A welder rated for 200 amps may not deliver that output continuously. In a workshop test, a 160-amp unit handled 3 mm steel comfortably, but it struggled during repeated long welds. That detail matters. Look for adjustable wire speed, inductance control, and clear voltage settings on a MIG model. For TIG, high-frequency start, a foot pedal, and AC capability are valuable when working with aluminum.
Your power supply and workspace also shape the decision. A compact machine may fit a home garage, yet its short cables can become frustrating around large frames. Gas choice, torch quality, and replacement consumables affect long-term cost. Do not ignore operator comfort. I once selected a powerful welder with awkward controls and used it less than expected. That was a poor decision. Test the controls, inspect the manual, and match the machine to your actual projects, not imagined ones.
Typical operating-current ranges help match a welding process to the material thickness, heat control, and project speed you need.
MIG welding commonly covers approximately 30–300 A and is generally faster for fabrication and thicker materials. TIG welding commonly starts at lower currents, around 5–250 A, providing finer heat control for thin stainless steel, aluminum, and precision work. Actual ranges depend on the welder, electrode or wire size, shielding gas, material, joint design, and duty cycle.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru