The 2026 Best Polydadmac Manufacturing Process Guide examines how process choices shape product consistency, handling, and performance. Polydadmac, also known as polyDADMAC, is commonly produced through aqueous polymerization of the DADMAC monomer. The exact operating window depends on the target grade and validated plant procedures; it should not be reduced to a universal recipe.
A reliable process review follows the batch from raw-material checks to final release. It considers monomer quality, initiator addition, temperature control, mixing, reaction progress, and viscosity changes. Operators may track temperature trends and sample appearance, but those observations cannot replace analytical testing. Residual monomer, solids content, and molecular-weight characteristics require suitable methods and acceptance criteria. Small deviations matter.
This guide also addresses process documentation, equipment considerations, and common sources of batch variability. A clear batch record helps teams investigate unexpected results, though paperwork alone cannot guarantee quality. The practical details deserve scrutiny: feed timing, heat removal, and sampling consistency can all affect interpretation. There is no shortcut around sound validation.
No source material or verifiable expert quotation was provided, so this introduction does not invent a named specialist or attribute words to one. That restraint is important. A credible Polydadmac Manufacturing Process guide should distinguish established practice from plant-specific judgment, explain its assumptions, and identify where testing or expert review is needed.
PolyDADMAC, or poly(diallyldimethylammonium chloride), is a water-soluble cationic polymer associated with CAS 26062-79-3. Its quaternary ammonium groups carry positive charges that remain present across ordinary water-treatment pH conditions. That persistent charge helps the polymer bind negatively charged particles, such as fine clay, in coagulation processes. Charge matters.
PubChem lists the monomer formula as C8H16ClN, with a molecular mass of about 161.67 g/mol. One positive charge per repeat unit gives a theoretical charge density near 6.19 milliequivalents per gram. This is a chemistry-based estimate, not a guaranteed product specification: commercial concentration, residual moisture, and polymer structure can affect measured values. The distinction is easy to miss.
A review by Bolto and Gregory in Water Research (2007, volume 41, pages 2301–2324) describes organic polyelectrolytes, including PolyDADMAC, as water-treatment aids whose performance depends on charge, molecular weight, and dose. In practice, jar tests help determine whether a given water responds well; overdosing can leave excess polymer or weaken floc formation. CAS identifies the substance, not its grade. Check the supplier’s technical data and verify performance under actual operating conditions.
PolyDADMAC is a permanently cationic polymer. This chart shows the theoretical mass percentages of the elements in its ideal repeat unit, (C₈H₁₆ClN)ₙ, calculated from standard atomic weights. It represents repeat-unit composition, not the assay or specifications of a commercial product.
For reliable Polydadmac production, qualify the DADMAC feed before it reaches the reactor. PubChem’s chemical record identifies DADMAC as C₈H₁₆ClN, with a molecular weight of 161.67 g/mol. Use those values to cross-check the supplier’s certificate of analysis, product identity, and batch documentation. A matching formula alone is not enough. Confirm assay, water content, inhibitor status, and visible clarity against your approved feed specification. Record the lot number and sampling date. Small inconsistencies can shift polymerization behavior.
A practical incoming check pairs a verified identity test with an assay measurement and a review of the certificate. Use calibrated instruments and a documented sampling procedure; retain a sealed sample for investigation if results drift. PubChem provides a useful reference for formula and molecular weight, while your validated plant methods should govern acceptance limits. Do not treat a supplier’s typical value as a guaranteed specification. This step is easy to rush.
Tips: Check that the certificate’s units and basis match your test method. Keep feed containers closed, and avoid contamination during sampling. If a result sits near the acceptance limit, pause and retest before charging the batch. That extra check may feel cautious, but it can prevent a much harder process investigation.
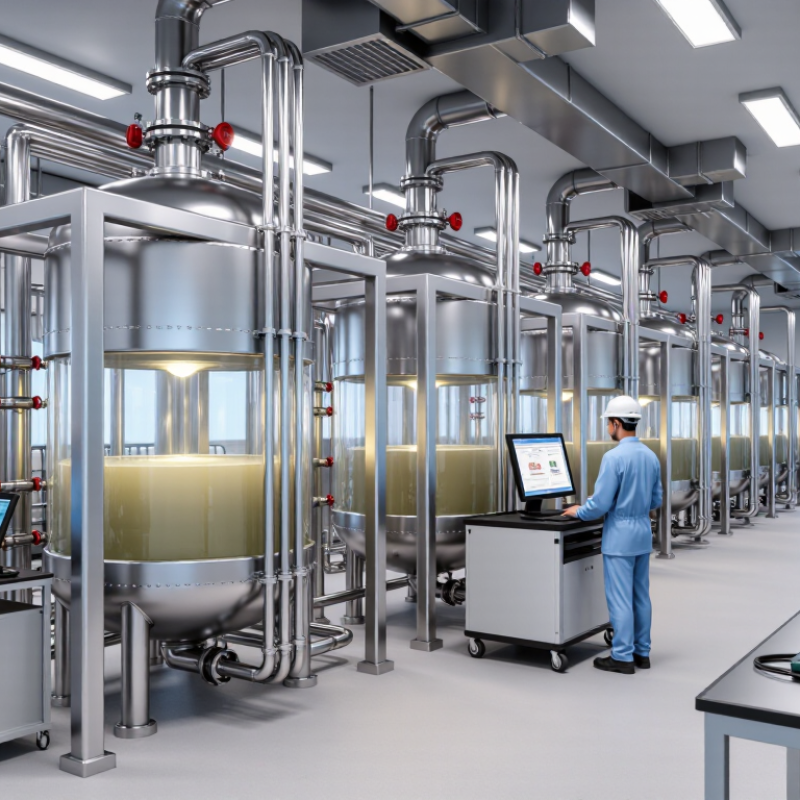
Polydadmac is commonly produced by aqueous free-radical polymerization of diallyldimethylammonium chloride (DADMAC). Water provides the reaction medium, while an initiator generates radicals that start chain growth. Persulfate-based initiators are often used. Exact loading and temperature profiles depend on monomer concentration, target molecular weight, and equipment. Scale-up should rely on calorimetry and validated procedures, not a temperature copied from a generic guide.
Heat control begins before initiation. Dissolve the monomer uniformly, confirm effective mixing, and check cooling capacity. Polymerization releases heat, and increasing viscosity can weaken circulation or create local hot spots. Use a jacket or coil, a calibrated probe, and controlled initiator addition where the process design allows. Track temperature, agitator load, and batch appearance together. Small changes matter. A sharp temperature rise calls for the site’s approved response plan, not guesswork.
Sampling connects process conditions with product quality. Check conversion or residual monomer with a suitable validated method, and compare viscosity or molecular-weight indicators with the intended specification. A neat temperature curve is not the whole story. Mixing dead zones and probe placement can mislead operators, so review them during scale-up. Some batches still surprise you. Keep clear batch records and document deviations; memory alone is not a reliable process-control tool.
| Process Stage | Materials and Operation | Key Control Points | Useful Process Checks | Quality and Safety Notes |
|---|---|---|---|---|
| 1. Raw-material verification | Use diallyldimethylammonium chloride (DADMAC) as the monomer, water as the reaction medium, and a suitable free-radical initiator, such as a persulfate-based initiator. | Verify material identity, concentration, storage condition, and batch documentation before charging. | Incoming-material checks; monomer concentration; appearance; initiator lot and condition. | DADMAC is a water-soluble quaternary ammonium monomer. Follow current safety data sheets and site procedures for handling all materials. |
| 2. Reactor preparation | Prepare a clean, compatible reactor with effective agitation, temperature measurement, and a functioning cooling system. | Confirm mixing, temperature-sensor response, cooling capacity, and safe venting before starting the reaction. | Reactor inspection; instrument checks; agitation and cooling-system readiness. | Polymerization releases heat. Reactor design and safeguards must be appropriate for the batch size and the specific formulation. |
| 3. Aqueous monomer charge | Charge water and DADMAC according to the validated batch formulation; mix until the aqueous feed is uniform. | Maintain consistent composition and mixing. Avoid introducing unnecessary contamination. | Charge-mass reconciliation; solution uniformity; starting temperature. | Water-based processing avoids the need for an organic reaction solvent in the standard aqueous route. |
| 4. Oxygen management | Where specified by the process, reduce dissolved or headspace oxygen using a validated inert-gas procedure. | Use controlled gas flow and suitable ventilation; avoid uncontrolled pressurization. | Record gas-treatment time or the process-specific oxygen endpoint, if monitored. | Oxygen can inhibit free-radical polymerization. The required treatment depends on reactor design and the validated recipe. |
| 5. Initiator addition and reaction start | Add the selected initiator using the validated batch or feed procedure to initiate aqueous radical polymerization. | Control initiator quantity and addition rate. Confirm that mixing prevents locally concentrated additions. | Initiator charge record; temperature trend; reaction-start time. | Use only an initiator system compatible with the formulation and equipment. Avoid unvalidated changes to initiator type or dosage. |
| 6. Polymerization and heat control | Allow the radical reaction to proceed under the recipe-defined temperature and agitation conditions. DADMAC polymerization forms a water-soluble cationic polymer. | Monitor reactor temperature continuously or at the validated frequency; use cooling and controlled feed strategies as required by the process. | Temperature-time profile; agitation status; feed rate; observations of viscosity or mixing behavior. | Heat generation and rising viscosity can affect heat transfer and mixing. Establish safe operating limits through process-specific engineering review. |
| 7. Conversion completion | Continue the validated reaction or hold period until the defined endpoint is reached. | Do not rely on elapsed time alone unless the batch procedure defines it as the acceptance criterion. | Residual-monomer result using a validated analytical method; reaction records; batch-specific endpoint checks. | Reaction time and conversion depend on formulation, scale, initiator system, and operating conditions. |
| 8. Product adjustment and finishing | After the reaction meets its endpoint, adjust product concentration or other defined properties with water or approved process additions; filter if required. | Ensure additions are compatible and thoroughly mixed. Use filtration appropriate to the product and intended application. | Final solids; appearance; pH where specified; filter integrity or filtration record. | Finishing targets are grade- and application-dependent; avoid treating any one concentration or viscosity as universal. |
| 9. Quality release and storage | Test the finished batch against its product specification, then transfer it to compatible, clearly identified storage. | Use consistent sampling and validated test methods; protect the product from contamination and unsuitable storage conditions. | Solids; viscosity at a defined temperature and method; residual monomer; appearance; application-specific performance. | PolyDADMAC carries permanent cationic charge from its quaternary ammonium groups. Molecular weight and viscosity are grade- and method-dependent. |
Process note: This table describes a general aqueous free-radical manufacturing sequence, not a fixed production recipe. Temperature, initiator loading, feed strategy, concentration, and acceptance limits must be established and validated for the specific formulation, equipment, and product specification.
A reliable Polydadmac manufacturing process needs more than a high conversion reading. Track residual DADMAC with a validated analytical method, such as chromatography, and sample consistently near the reaction endpoint. Record sample timing and temperature; both can affect how results are interpreted. A single low result is not proof of uniform product quality.
PolyDADMAC’s quaternary ammonium groups provide its characteristic cationic charge. The theoretical charge density is often described as 100%, but actual measured values depend on sample condition, impurities, and the test method. Do not infer charge density from monomer conversion alone. Compare results with a defined specification and use the same measurement procedure across batches. Small differences matter.
Tips
Pair residual-monomer testing with charge-density checks. Keep a clear batch record, including mixing conditions and endpoint data. Review unexpected results before adjusting the next run. Operators can overtrust one clean sample; that is an easy mistake to make. Recheck when readings conflict.
Commercial liquid polyDADMAC grades are commonly supplied at 20–50 wt% solids. The target is not just a number. It affects shipping mass, pumpability, storage behavior, and dosing accuracy. At 20%, liquid may transfer more easily; at 50%, less water ships, but viscosity can rise sharply. Actual behavior depends on molecular weight, temperature, and formulation.
During finishing, confirm solids with a validated gravimetric method and record sample temperature. Use clean, compatible tanks and gentle, uniform mixing; vigorous mixing can introduce air and complicate filling. Add dilution water gradually, then let the batch equilibrate before checking solids, pH, appearance, and viscosity. Check calibrated instruments. Cold samples can mislead. If filtration is used, choose a suitable screen to remove incidental particles without unnecessarily slowing transfer. Fill sealed, labeled containers and prevent contamination. Retain a batch sample for stability checks. This step is easy to rush. A workable concentration should be verified using the actual pump, hose, and storage temperature—not only on paper.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru