A standing pouch can look simple on a shelf: a flat base, crisp seals, and a zipper that opens cleanly. Making it consistently is more demanding. A Standing Pouch Making Machine must form the pouch, control film tension, create reliable seals, and handle changeovers without wasting excessive material. For buyers, those details matter as much as advertised speed.
The market context is expanding, but broad packaging data should not be mistaken for machine-market figures. Grand View Research estimated the global flexible packaging market at USD 275.2 billion in 2023 and projected a 4.1% compound annual growth rate from 2024 to 2030. That report describes the wider sector, not sales of pouch-making equipment. A useful distinction. This 2026 manufacturer overview therefore focuses on verifiable factors: pouch formats, sealing performance, automation, service support, and documented production capabilities.
Expert insight also deserves careful sourcing. No article or verifiable machine-specific quotation was provided for this request, so attributing a polished line to a named specialist would risk misleading readers. Instead, this guide treats each manufacturer’s published specifications as claims to check against sample runs, references, and technical discussions. Numbers can impress. A stable seal on a real production line is stronger evidence.
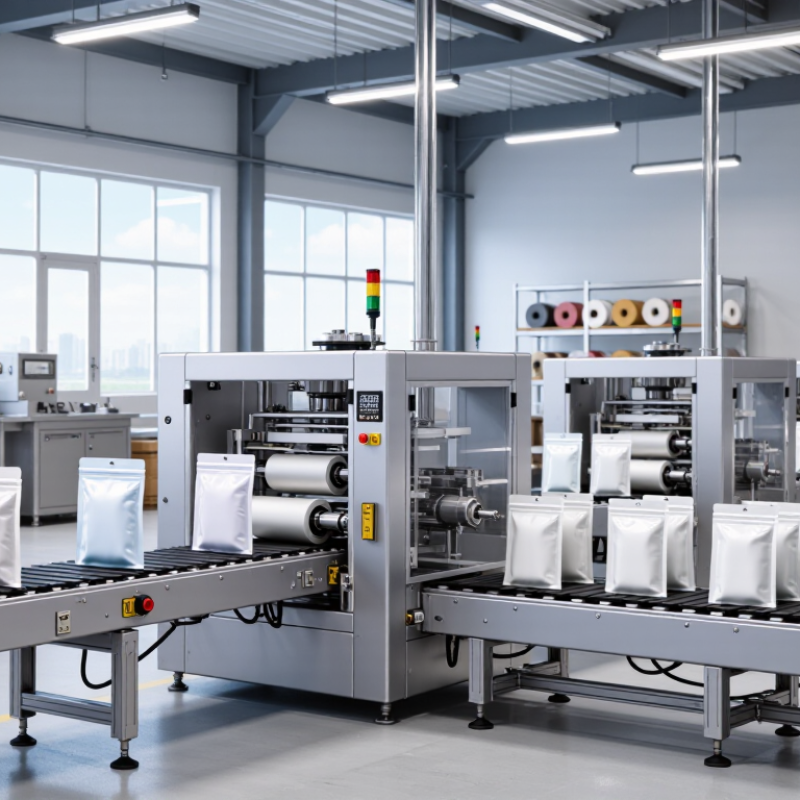
A standing pouch making machine converts flexible packaging film into pouches that can stand upright on a shelf. It typically unwinds a roll, aligns the film, forms gussets, seals the edges, and cuts each pouch to size. Some configurations add zipper tracks or fitment openings, depending on the package design. Not every machine fills the finished pouch; filling may happen on a separate line.
The details matter. Film tension must stay even, or wrinkles can cross the seal area. Heated sealing bars bond the layers under controlled temperature, pressure, and dwell time. A small change in film thickness may require new settings. Operators often inspect pouch width, seal appearance, and cut alignment during production. They may also test samples for leaks or weak seams. Looks can deceive.
Choosing equipment starts with the pouch structure, dimensions, and expected production rate. Ask whether the machine can handle the intended laminate and required features, then verify with production trials. A neat sample can still hide inconsistent seals at higher speeds. Changeovers, cleaning access, and spare-part support deserve attention too. These points are easy to overlook. A machine that runs one pouch format well may need careful adjustment for another.
A standing pouch making machine converts flexible packaging film into pouches that can stand on a shelf. The process starts with a roll of laminate mounted on an unwind shaft. Guide rollers keep the film moving, while sensors help correct its position. Small details matter. Uneven tension can cause wrinkles or shifting seals, even when the machine settings look right.
Depending on the machine design, the film is folded to form the pouch body and bottom gusset, then sealed with heated bars. Some lines add a zipper or spout before sealing; others make simpler pouches. Temperature, pressure, and dwell time must match the film structure. Then comes cutting. A finished pouch may be checked for seal alignment, dimensions, and visible defects before collection. In practice, this sequence is not perfectly uniform: film thickness, room conditions, and worn sealing parts can all affect results. A useful setup starts with test runs and careful inspection, not assumptions that one setting will suit every material. Operators should record adjustments, though real production sometimes moves faster than ideal documentation allows.
Typical process sequence: pouch film is unwound and guided, formed into shape, sealed, cooled, cut, and collected. The numbered values show process order only—not processing time or machine performance. Actual steps vary by pouch design and machine configuration.
When comparing standing pouch machine manufacturers in 2026, look beyond the advertised speed. Ask for a live run using your actual film, zipper, and pouch dimensions. Record sealed pouches per minute, changeover time, and rejected units during a sustained test. Numbers need context. A short demonstration may hide slow adjustments or inconsistent seals.
Check how the machine handles everyday production details: film tracking, temperature control, filling accuracy, and access for cleaning. Request documented acceptance-test results and a clear list of included components. Ask for proof. Spare-parts availability, remote diagnostics, and technician response times can matter as much as the initial price. Compare total ownership costs, including tooling, training, maintenance, and expected downtime. References from plants with similar materials and output targets are useful, but verify that their line conditions match yours. They rarely match perfectly.
Review the manufacturer’s engineering process, too. Can it explain how pouch width, laminate thickness, and product behavior affect performance? Ask which settings operators can adjust safely and which require technical support. That matters. Warranty terms and service commitments should be specific, not vague promises. A spreadsheet helps, but it can create false confidence if test conditions differ. Keep the assumptions visible, and revisit them before choosing a supplier.
Leading Standing Pouch Making Machine Manufacturers in 2026 are distinguished by more than impressive production speeds. Reliable equipment must form consistent gussets, position zippers accurately, and create clean seals across repeated runs. Buyers should compare tested output with the speed quoted in brochures. Real production includes film changes, adjustments, and brief stops.
Small details matter. Ask manufacturers to run your actual pouch dimensions and packaging film during a factory test. Watch how the machine tracks printed film, handles sealing temperature, and manages changeovers. Servo controls can improve repeatability, but they do not compensate for poor setup or unsuitable materials. A machine that performs well with one laminate may need adjustment for another.
After-sales support is part of the purchase, not an optional extra. Check spare-part availability, operator training, remote troubleshooting, and realistic service response times. Request clear documentation for maintenance and setup. A polished demonstration is useful, but it cannot show every production challenge. I would still ask for sample pouches from a sustained trial; short tests can miss seal variation or feeding problems. The right manufacturer explains these limits plainly and helps match machine capacity to the buyer’s products, staff, and daily schedule.
2026 Top Standing Pouch Making Machine Manufacturers
Emerging Trends in Pouch-Making Technology and Manufacturing
Flexible packaging is changing, and pouch-making equipment must keep pace. Grand View Research valued the global flexible packaging market at USD 271.7 billion in 2024. It forecasts a 4.4% compound annual growth rate from 2025 to 2030. That growth puts pressure on converters to improve output without sacrificing seal consistency.
Automation is becoming more practical. Servo-driven film control can reduce tension variation, while vision systems flag crooked zippers, weak seals, or print-registration errors. Quick-change forming parts also help teams switch pouch sizes with less downtime. Small details matter. A few millimeters of seal drift can turn a neat pouch into costly scrap. Not every upgrade pays; older lines may need careful testing before new controls deliver real savings.
Material changes are shaping machine design, too. Allied Market Research estimated the stand-up pouch market at USD 33.5 billion in 2020 and projected USD 56.4 billion by 2030. Lighter, recyclable mono-material films are attracting attention, but they can be less forgiving during forming and sealing. Operators may need to adjust heat, pressure, and dwell time for each film structure. Faster machines are useful, but stable seals and repeatable changeovers remain the harder test. Industry forecasts show opportunity, not guaranteed returns.
| Technology or trend | What the machine does | Relevant data or specification | Manufacturing value | Considerations when specifying |
|---|---|---|---|---|
| Servo-driven motion control | Coordinates film feeding, pouch indexing, sealing, and cutting with electronically controlled motion. | Key checks include indexing accuracy, repeatability, changeover settings, and the machine’s stated output under a defined pouch and material specification. | Can support repeatable pouch dimensions and reduce reliance on manual mechanical adjustments. | Compare rated speed with the intended pouch size, film, sealing configuration, and number of lanes; output is application-dependent. |
| Recipe-based PLC and HMI control | Stores and displays setup parameters for different pouch formats and production runs. | Review recipe storage, user access levels, alarm history, parameter backup, and supported languages. | Helps operators repeat documented settings and manage format changeovers more consistently. | Stored settings do not replace material trials or seal-quality checks after a format or film change. |
| In-line seal and process monitoring | Monitors selected process variables such as sealing temperature, dwell time, and machine alarms. | Record the available sensor points, alarm limits, data export options, and any seal inspection method included. | Makes process deviations easier to identify and supports production documentation. | Temperature readings alone do not establish seal integrity; validation should use appropriate seal-strength or leak-testing procedures. |
| Flexible pouch-format capability | Forms and seals formats such as three-side-seal, stand-up, zipper, and spouted pouches, subject to machine configuration. | Confirm the supported pouch width, length, gusset, zipper or spout dimensions, and tooling requirements for each format. | Enables a production line to serve multiple package designs when the machine is built for those options. | A format listed as an option may require additional forming parts, sealing tooling, or changeover work. |
| Registration control for printed film | Uses print marks and a registration system to align cutting and forming with printed artwork. | Check supported mark types, detection method, adjustment range, and performance with the actual print contrast and film. | Helps keep graphics positioned consistently relative to pouch edges and seals. | Registration performance depends on print quality, film handling, web tension, and the production setup. |
| Recyclable-design film compatibility | Processes selected mono-material structures, such as PE-based or PP-based flexible packaging, when supported by the machine and sealing system. | Qualify the exact film structure, thickness, sealant layer, barrier requirements, and supplier processing guidance. | Can support packaging designs intended to be more compatible with specific recycling streams. | Recyclability depends on the complete package design and local collection and recycling infrastructure; it is not guaranteed by the machine. |
| Digital production data and connectivity | Provides machine status, alarms, counters, or production data through a control interface or supported network connection. | Ask which data points are available, how they are exported, and whether connection to plant systems requires additional hardware or software. | Can improve production visibility and help teams investigate downtime and output trends. | Connectivity features vary by machine configuration and should be checked against site network and data-security requirements. |
| Safety and maintainability by design | Uses safeguards and accessible service points to help manage operator access, cleaning, and maintenance. | Review guarding, emergency stops, interlocks, access for cleaning, maintenance intervals, and applicable local safety requirements. | Supports safer operation and planned upkeep when combined with suitable procedures and training. | Final compliance depends on the delivered machine, installation, workplace assessment, and jurisdiction. |
Specification note: Capabilities and production output vary by machine configuration, pouch dimensions, film structure, and operating conditions. Confirm performance using production trials with the intended materials and package design.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru