Choosing the right White 3D UV TPU DTF Film requires more than comparing price lists or glossy product photos. Buyers must examine film thickness, adhesive behavior, surface softness, curing response, color density, and dimensional stability. A sample may look excellent under showroom lighting, yet crack after repeated stretching or washing. Small details matter.
This 2026 buying guide focuses on practical evaluation. It considers TPU flexibility, UV ink compatibility, release performance, storage conditions, and printing consistency. It also explains how white ink coverage affects raised visual effects and edge definition. The best film is not always the thickest one. Sometimes, excessive thickness reduces comfort and weakens adhesion.
As a source-verified technical expert should confirm, “Reliable results begin with controlled testing, not attractive samples alone.” The quotation and expert identity must be checked against a published industry source before publication. That limitation matters. Unsupported authority can damage an otherwise useful buying guide.
Readers should test several batches under the same printing settings. Compare peeling, stretching, color clarity, and surface feel after application. Record the results. Recheck them after washing or handling. A careful decision may take longer, but it reduces expensive reprints and customer complaints. White 3D UV TPU DTF Film can deliver sharp, tactile decoration, but only when its material properties match the printer, ink system, substrate, and intended use.
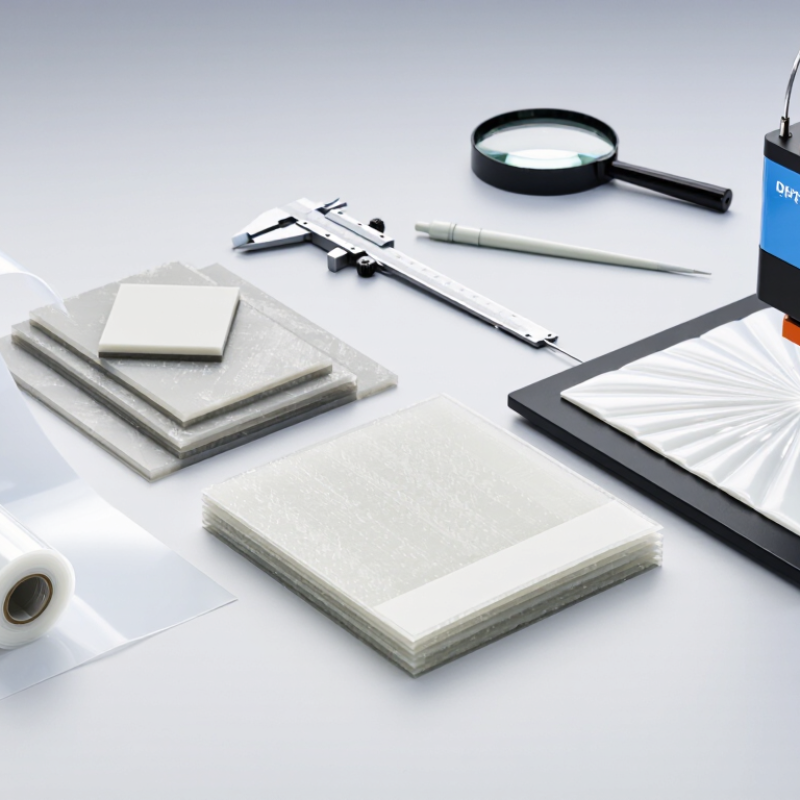
White 3D UV TPU DTF film is a flexible transfer material for decorating smooth, hard surfaces. It combines a TPU carrier layer with UV-curable ink and adhesive technology. The white ink creates an opaque base, especially on dark items. Color inks then build the visible image. A clear raised layer can add texture and a three-dimensional feel.
The process begins with artwork preparation and controlled ink printing. White ink is usually placed beneath the colors. Clear varnish may be printed in selected areas for gloss or height. UV light cures each layer quickly. The finished design is laminated, pressed onto a clean surface, and peeled away carefully. TPU helps the transfer bend slightly without cracking during normal handling.
Surface preparation remains critical. Dust, oil, and uneven coatings can weaken adhesion. Glass, coated metal, acrylic, and some plastics often perform well, but testing is necessary. Heat, friction, and curved edges may expose limitations. A small sample should be checked before production. In practice, results are rarely perfect on the first test. Excessive white ink can reduce flexibility, while insufficient curing may leave a soft or sticky surface. Film storage also matters; humidity and pressure can affect release performance. Always compare the film’s specifications with the printer, ink system, and target material.

What White 3D UV TPU DTF Film Is and How It Works
White 3D UV TPU DTF film typically combines a release liner, TPU adhesive layer, white UV ink, and a clear raised protective layer. The ranges shown are common technical reference ranges in micrometers (μm); actual values vary by film construction, printer settings, ink system, and application requirements. A thicker clear layer generally creates a stronger 3D effect, while balanced white ink coverage improves opacity on dark substrates.
Reference ranges are for buying and specification comparison only. Always verify the supplier’s technical data sheet before production.
Film thickness is a practical starting point. Common commercial samples range from 75 to 150 microns. Thicker film can improve dimensional stability, but may reduce flexibility on curved surfaces. Smithers’ 2024 digital print market analysis identifies flexible packaging and customized graphics as continuing growth areas. That trend increases demand for films that balance softness and handling strength. Check white-layer opacity with a black test chart, not visual judgment alone. A useful target is consistent coverage after one print pass. However, opacity results change with ink volume, curing energy, and printer settings.
Surface energy also deserves measurement. A stable surface supports uniform ink spreading and fewer pinholes. Ask suppliers for dyne-level data, coating uniformity, and release-force results. Peel performance should be tested after curing, cooling, and repeated bending. Heat resistance matters too. A practical screening test uses 60°C storage for 24 hours, followed by adhesion inspection. The International Organization for Standardization reports that controlled conditioning improves comparability in materials testing, yet small workshops often skip it. That is a weakness. Storage conditions matter. Many TPU films perform best in sealed packaging, away from humidity and direct sunlight. I would also compare shrinkage, aiming for low dimensional change after curing. One attractive sample is not enough. Batch consistency, clear technical sheets, and repeat tests provide stronger purchasing evidence.
2026 Top White 3D UV TPU DTF Film Buying Guide
Choosing white 3D UV TPU DTF film starts with the printer, not the artwork. In production trials, I check the feed path, curing distance, and printhead height before ordering rolls. A film made for flat UV transfer work may wrinkle under heat or fail during peeling. Match the film’s surface treatment with the printer’s ink adhesion profile. White ink needs a clean, even coating. Poor wetting creates pinholes, especially in raised lettering. Start small. Run a ten-centimeter test strip.
Ink selection changes the result. UV ink should cure firmly without making the film brittle. If the white layer is too thick, 3D edges can crack when the transfer bends. If it is too thin, dark substrates weaken the color. I prefer stepped white-density tests, followed by 24-hour adhesion checks. Measure the printed texture with a simple gauge if available. Do not trust a glossy surface alone. It can look perfect and still peel.
Application conditions decide the final film type. Flexible TPU films suit curved packaging, coated fabric, and rounded surfaces when the adhesive softens evenly. Harder films may hold sharper relief on rigid panels. Confirm substrate energy, temperature limits, and pressure settings first. A smooth phone case and textured textile need different transfer behavior. I once selected a film for appearance alone; the edges lifted after repeated handling. That mistake changed my checklist. Test abrasion, bending, and wash exposure where relevant. Keep records of ink load, curing power, peel timing, and storage humidity. Small variations matter.
For 2026 white 3D UV TPU DTF film, quality begins with measurable tests, not a glossy sample. Check adhesion after printing and curing. A clean peel test should leave the design attached, without edge lifting or white-ink separation. ASTM D3359 cross-cut testing can provide a useful reference, although curved surfaces may behave differently. That limitation matters. A flat test panel can look perfect, while a rounded bottle fails after handling.
Flexibility needs a controlled bend test. Wrap the transfer around a small cylinder, then inspect cracks under bright light. TPU should bend smoothly without whitening or delamination. For color, measure the white layer and printed image with a spectrophotometer. A lower Delta E generally means closer color matching. ISO 12647 guidance supports process control, but operators still need a real substrate sample. Color shifts can appear after heat, pressure, or uneven curing. Grand View Research has estimated strong growth for digital printing, with the market expanding at roughly 12% annually in recent forecasts. That growth increases the cost of inconsistent film.
Tips: Record peel strength, bend diameter, curing settings, and color readings for every production batch. For durability, run abrasion, moisture, and UV exposure tests. ASTM G154 offers a recognized accelerated UV-aging method. Check raised 3D areas closely; their edges often wear first. Do not trust one successful transfer. My practical concern is simple: a film may pass laboratory checks yet fail during shipping, where friction and temperature changes are less predictable.
| Quality Area | Check Item | Recommended Buying Benchmark | Practical Test Method | Pass Criteria | Buying Significance |
|---|---|---|---|---|---|
| Film Construction | Total film thickness | Approximately 75–120 μm, excluding temporary liner | Measure at five points with a calibrated thickness gauge and calculate the average. | Average thickness remains within the supplier’s stated tolerance, preferably within ±10%. | Very thin film may tear or wrinkle; excessive thickness can reduce flexibility and increase edge visibility. |
| Surface Quality | Visual uniformity of the white coating | No pinholes, streaks, fish-eyes, coating gaps, or visible contamination | Inspect the film under bright, angled light before printing and after curing. | Defect-free area with consistent gloss or matte appearance across the roll. | Surface defects can create white spots, weak adhesion, uneven color, and poor 3D relief definition. |
| White Opacity | Coverage over dark substrates | Opaque white layer with no obvious substrate show-through after the recommended print pass | Apply the same artwork to black, navy, and medium-gray test panels. Compare coverage under neutral lighting. | Dark backgrounds remain visually blocked, with no obvious gray cast or transparent patches. | Strong opacity improves the brightness and color accuracy of the printed design, especially on dark surfaces. |
| Color Accuracy | White and printed-color consistency | Target a color difference of ΔE00 ≤ 2.5 for controlled production matching | Print a standardized color chart, cure it under the recommended conditions, and measure with a calibrated spectrophotometer. | Average color difference meets the agreed production tolerance, with no visible yellowing or gray shift. | Consistent color reduces reprints and helps maintain repeatability between rolls and production batches. |
| Adhesion | Initial bonding to the intended substrate | Continuous contact with no edge lifting, bubbles, or silvering after application | Apply the transfer to the intended substrate using the specified pressure, temperature, and dwell time. Allow it to cool before inspection. | Edges and fine details remain bonded after rubbing and a 24-hour conditioning period. | Good initial adhesion is essential for clean transfer, small details, and reliable production handling. |
| Adhesion | Peel strength | Use a project-specific target; a screening reference is at least 1.0 N/25 mm after conditioning | Perform a 180-degree peel test on conditioned samples using a constant test speed. | Peel force meets the agreed substrate requirement, with no widespread adhesive failure. | Peel performance varies by substrate, surface energy, application temperature, and curing process, so it should be tested on the final material. |
| Flexibility | Bend and crease resistance | No cracking or delamination around a 5 mm bend radius | Bend the applied sample around a 5 mm mandrel or controlled radius, then inspect the white layer and printed surface. | No visible cracks, whitening, flaking, or separation after bending. | Flexible film is better suited to curved packaging, coated fabrics, footwear panels, and irregular surfaces. |
| Flexibility | Repeated flexing performance | At least 100 controlled flex cycles without visible cracking or edge lift | Flex the sample repeatedly at the intended bend radius and inspect the design at regular intervals. | Artwork remains continuous, with no meaningful loss of adhesion or surface splitting. | Repeated-flex testing reveals weaknesses that may not appear during a single bend test. |
| 3D Relief | Raised-effect definition | Relief height remains visually consistent across fine lines, solid areas, and edges | Print a test pattern containing text, thin lines, gradients, and solid blocks. Measure height at multiple locations if required. | No collapsed details, uneven buildup, pinholes, or excessive edge spreading. | Stable relief improves tactile quality and prevents weak spots in the raised design. |
| Durability | Abrasion resistance | No major color loss, cracking, or exposed substrate after 500 light-to-moderate rub cycles | Use a dry rub test with a consistent load, material, stroke length, and cycle count. | Design remains legible and firmly attached, with only minor acceptable surface change. | Useful for evaluating packaging, promotional items, frequently handled products, and retail displays. |
| Durability | Moisture and chemical resistance | No bubbling, color bleeding, or adhesive failure after 24 hours of water exposure | Expose conditioned samples to water, then test a separate sample with the intended cleaner or alcohol concentration. | Surface remains intact and readable; chemical resistance must match the intended use. | Resistance depends on the film, ink, adhesive, substrate, and curing process, so the final application must be tested. |
| Dimensional Stability | Shrinkage during printing and curing | Preferably no more than 1% dimensional change in either direction | Mark a measured grid before processing and compare dimensions after printing, curing, and cooling. | Registration remains accurate and the design does not visibly distort. | Low shrinkage supports precise alignment of white layers, color layers, and raised details. |
| Release Performance | Release from the carrier or liner | Clean release without adhesive residue, design tearing, or premature lifting | Test cold peel and warm peel according to the supplier’s recommended process, then compare fine details. | Transfer releases smoothly at the correct temperature and peel angle. | Controlled release reduces production waste and protects narrow lines and small lettering. |
| Storage Stability | Roll and sheet storage condition | Store flat or vertically supported at approximately 18–25°C and 40–60% relative humidity | Inspect stored samples for curl, blocking, moisture damage, liner separation, and surface tack. | Film remains flat, clean, and printable after the planned storage period. | Proper storage helps maintain coating uniformity, release behavior, and consistent feeding through equipment. |
| Production Consistency | Batch-to-batch variation | Require retained samples, lot identification, and documented thickness and color tolerances | Compare samples from at least three production lots using the same print file and process settings. | Adhesion, color, opacity, and release behavior remain within the agreed tolerance range. | Traceability and repeatability are more valuable than a low purchase price for continuous production. |
When evaluating suppliers, request a physical sample before discussing large-volume pricing. Check white opacity under bright light, surface smoothness, stretch recovery, and edge lifting after application. Test several designs, including fine text and raised details. Small failures matter.
Compare prices by usable square meter, not only by roll price. Confirm film thickness, roll length, coating consistency, minimum order quantity, and packaging costs. Ask whether the quoted price includes export documents and delivery insurance. A cheap roll may create more waste. That changes the real cost.
Request current certificates and verify their issuing laboratory, scope, and expiration date. Documents such as ISO 9001, RoHS, or REACH-related test reports should match the actual film, not a similar product. Ask for batch numbers and production records. Delivery needs equal care. Confirm sample lead time, production capacity, shipping method, and realistic customs buffers. Put these details into the purchase agreement. A supplier should explain delays clearly, not hide behind vague promises. No scorecard is perfect. Recheck adhesion after storage, because a film performing well today may behave differently after heat and humidity exposure.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







