Buying a Chemical Anchor for international projects involves more than comparing cartridge prices. Performance depends on concrete strength, crack conditions, hole diameter, embedment depth, and installation temperature. A product that works in a warm warehouse may fail during a cold winter installation.
Structural fastening specialist Dr. Günther Seidl has emphasized, “Reliable anchoring begins with understanding the base material, not with choosing a brand.” This principle should guide every global purchasing decision. Buyers should request verified technical data, European Technical Assessment documentation where applicable, fire-performance classifications, and clear batch traceability. Check the resin type, shelf life, curing time, and storage requirements before approving a shipment. Small details matter.
Installation quality is equally important. Dust left inside a drilled hole can reduce bond strength. A trained installer should use the specified brush, air-cleaning method, injection nozzle, and curing interval. Do not treat these steps as optional. They are not.
Global buyers should also examine supplier experience, quality-control systems, packaging protection, and after-sales support. Ask whether technical documents match the exact product being shipped. Sometimes they do not. That uncomfortable gap deserves attention.
A lower unit price may hide higher project risk. Freight delays, damaged cartridges, unclear instructions, or inconsistent batches can create expensive rework. Compare complete delivered cost, not just the catalogue figure. The strongest purchase decision combines tested performance, dependable supply, documented installation guidance, and honest technical communication. That standard is demanding, but chemical anchoring leaves little room for convenient assumptions.
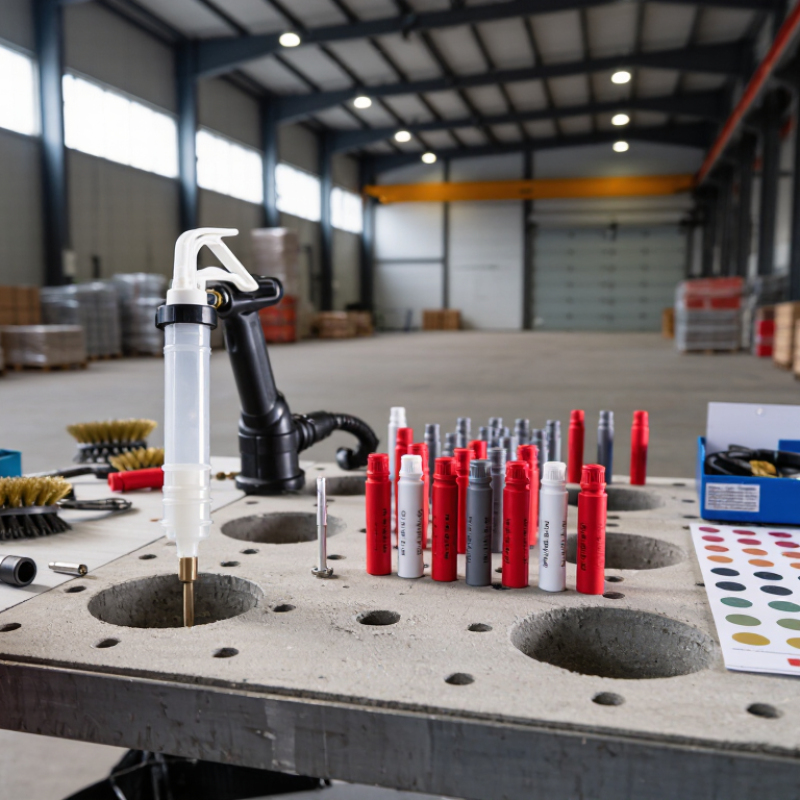
Chemical anchor selection starts with the structure, not the product catalogue. Record the base material, hole diameter, embedment depth, edge distance, and expected load. Concrete may be cracked, damp, aged, or contaminated with dust. Each condition changes installation performance.
Tip 1: Describe the application precisely. Is it a handrail, machinery frame, façade support, or overhead fixture? Note tension, shear, vibration, temperature, and fire exposure. A small bracket may need different testing than a heavily loaded steel column. Measure twice. Guessing creates expensive rework.
Tip 2: Check the installation environment before comparing prices. Outdoor anchors may face rain, salt air, or repeated freeze-thaw cycles. Indoor installations can still involve moisture, chemicals, or poor ventilation. Confirm curing time at the actual site temperature. A resin that cures quickly in a warm warehouse may behave differently on a cold morning.
Global buyers should request technical datasheets, installation instructions, safety information, and independent performance evidence. Verify suitability for the specific substrate and design load. Also confirm packaging dates, storage limits, language requirements, and local building rules. These details are easy to overlook. They should not be.
Tip 3: Ask for traceable batch information and practical installation guidance. Trial holes can reveal weak concrete or unexpected reinforcement. That step may feel slow, but it often prevents failure. I have seen project teams focus on unit cost and underestimate drilling tools, cleaning equipment, and installer training. The cheaper option was not cheaper after correction work.

7 Chemical Anchor Buying Tips for Global Buyers
Compare Resin Types, Load Ratings, and Installation Conditions
Global buyers should compare resin chemistry before comparing price. Epoxy usually provides strong bonding and reliable performance in demanding concrete applications. Vinyl ester can suit damp areas and higher chemical exposure. Polyester may work for lighter loads and less demanding conditions. Resin choice depends on the base material, not preference. Check technical data carefully.
Review tension and shear ratings for the exact concrete condition. Values for cracked concrete may differ greatly from uncracked concrete. Check embedment depth, anchor spacing, edge distance, and design safety factors. A high load rating can mislead when the installation geometry is poor. Ask for independent test reports and clear design values. The spreadsheet is not enough.
Installation conditions often decide real performance. Confirm whether the hole is dry, damp, or water-filled. Measure concrete and air temperatures before dispensing the resin. Follow the specified mixing nozzle and discard the initial material. Hole cleaning requires brushing and oil-free air. Small errors matter. Respect the full curing time before applying loads. Keep batch records and installation photographs for quality checks. Even experienced teams can miss a dusty hole or shorten curing time. That weakness deserves honest review. Request instructions suited to local site conditions and trained installers.
Global buyers should verify standards before comparing chemical anchor prices. Product labels alone are not enough. Ask for current technical data sheets, safety data sheets, and documented performance ratings. Confirm that the tested product matches the exact resin, mixing nozzle, cartridge size, and curing conditions you will receive.
Request test reports from qualified laboratories, not only internal quality statements. Check bond strength, curing time, temperature limits, moisture performance, and shelf life. The report should show test methods, sample numbers, production dates, and acceptance criteria. A certificate without traceability can mislead. Inspect whether the manufacturer tests every batch or relies on periodic sampling.
Factory quality deserves equal attention. Review raw material controls, calibration records, batch coding, storage temperatures, and complaint procedures. A remote audit can reveal gaps that documents hide. Ask how rejected cartridges are isolated and how corrective actions are recorded. Small details matter.
Do not trust perfect paperwork blindly. No checklist is perfect. I have seen buyers focus heavily on laboratory results while overlooking damaged packaging and unclear expiration marks. That mistake can affect installation quality. Request sealed samples, compare them with production batches, and arrange independent testing for high-volume orders. Keep written records of every approval, change notice, and shipment inspection. Supplier transparency is useful, but consistent evidence is stronger.
For global chemical anchor buyers, the lowest quotation rarely represents the lowest landed cost. I compare unit price, resin or steel surcharges, export packing, insurance, duties, and destination handling. The World Bank Commodity Markets Outlook tracks sharp commodity-price movements, so every quotation needs a validity period. Ask for the pricing formula. Otherwise, a cheap offer can age badly. This is not elegant, but it happens.
Packaging deserves a line-by-line check. Confirm cartridge dimensions, closure integrity, batch coding, pallet height, moisture protection, and multilingual safety documentation. The UN Globally Harmonized System supports consistent hazard communication, yet local implementation still varies. A damaged nozzle can turn usable stock into waste. Request drop-test evidence and photographs from an actual shipment, not only catalogue images. I have learned that “standard packaging” means little without measurements.
Logistics planning should follow the jobsite date, not the supplier’s optimistic promise. UNCTAD’s Review of Maritime Transport reports that about 80% of world trade by volume moves by sea. Port congestion can still disrupt schedules. Compare factory lead time, booking time, transit range, customs clearance, and buffer days. The World Bank’s 2023 Logistics Performance Index assessed 139 economies and showed major differences in speed and reliability. Build two scenarios: normal movement and disruption. Then test whether the installation team can wait. Lead time is a commercial risk, not just a calendar entry. Some buyers still ignore this.
Practical comparison framework for procurement teams sourcing injectable or cartridge-based chemical anchoring systems for concrete and masonry applications.
| Buying Tip | Key Evaluation Dimension | Indicative Market Data | What Global Buyers Should Verify | Commercial and Operational Impact |
|---|---|---|---|---|
| 1. Compare the Full Landed Cost | Unit price, order quantity, and total cost of ownership | Common cartridge sizes include 300 ml, 360 ml, 410 ml, and 585 ml. Indicative export pricing for standard chemical anchor cartridges can vary broadly from approximately US$3–12 per cartridge, depending on resin chemistry, performance class, packaging, order volume, and destination. | Request pricing on the same cartridge volume, resin type, nozzle configuration, currency, and Incoterm. Add static mixer nozzles, adapter parts, inland transport, ocean or air freight, insurance, duties, taxes, and local handling charges. | A lower ex-works price may become more expensive after freight, customs, accessories, and import charges. Compare landed cost per usable anchoring point rather than price per cartridge alone. |
| 2. Match Resin Chemistry to the Application | Performance, substrate, temperature, and installation conditions | Common systems include polyester, vinyl ester, and epoxy-based formulations. Typical cured-service temperature ranges may be approximately -40°C to +80°C, but the allowable range depends on the specific formulation, load case, and approval documentation. | Check suitability for cracked or uncracked concrete, masonry, dry or water-saturated holes, overhead installation, seismic conditions, sustained loads, and the required curing temperature. Review the technical data sheet and approval reports. | Choosing the wrong chemistry can reduce bond strength, extend curing time, or invalidate the design. A technically suitable product can reduce rework and installation risk even when its unit price is higher. |
| 3. Audit Packaging and Shelf Life | Cartridge format, protection, labeling, and remaining shelf life | Typical unopened shelf-life claims for chemical anchoring products are commonly around 12–24 months when stored under the manufacturer’s specified conditions. Many products require storage in a cool, dry area, often within approximately 5°C–25°C. | Confirm production date, minimum remaining shelf life at shipment, batch traceability, tamper evidence, multilingual labels, barcode requirements, compatibility with dispensing guns, and inclusion or pricing of static mixer nozzles. | Short remaining shelf life increases inventory write-off risk. Damaged cartridges, missing nozzles, or incompatible dispensing equipment can stop work and create hidden project costs. |
| 4. Plan Dangerous-Goods and Transport Requirements | Classification, freight mode, temperature exposure, and customs documents | Transport classification is formulation-specific. Some adhesive components may be regulated as dangerous goods while others may not be. Air freight is generally more restrictive and more expensive than sea or road transport. | Obtain the current Safety Data Sheet, transport classification, UN information where applicable, packing instructions, emergency contact details, and export documents before booking freight. Confirm whether temperature-controlled handling is required. | Incorrect classification can cause shipment refusal, customs delays, storage fees, or regulatory penalties. Sea freight is usually more economical for larger replenishment orders, while air freight is faster but less flexible. |
| 5. Benchmark Lead Times and Supply Capacity | Production schedule, order confirmation, and replenishment reliability | A practical planning range is approximately 2–6 weeks for standard production after order confirmation, plus transit time. Custom labels, special packaging, testing, or peak-season demand may extend the schedule. | Ask for confirmed production capacity, minimum order quantity, forecast requirements, holiday shutdown dates, batch-release timing, and the supplier’s historical on-time delivery performance. Separate manufacturing lead time from transit lead time. | A supplier with a slightly higher price but reliable capacity may reduce project delays and emergency freight. Establish a reorder point based on consumption, transit time, customs clearance, and safety stock. |
| 6. Validate Quality Documents and Compliance | Testing, approvals, traceability, and regional requirements | Product documentation should normally identify mix ratio, installation temperature, curing time, hole-cleaning method, bond or load data, storage conditions, and batch information. Required approvals vary by country, structure type, and project specification. | Request the technical data sheet, Safety Data Sheet, installation instructions, certificate of analysis where applicable, quality-management evidence, and relevant third-party test or approval reports. Confirm that documents apply to the exact product and cartridge size. | Complete documentation supports engineering approval, customs review, worker safety, and project audits. Generic or outdated documents can delay approval even when the physical product is available. |
| 7. Test Installation Economics Before Scaling | Yield, curing time, labor, waste, and dispensing efficiency | Usable output depends on hole diameter, embedment depth, rebar or threaded-rod size, cartridge volume, dispensing pressure, nozzle design, and purge waste. Initial purge material is normally discarded until the adhesive is properly mixed. | Conduct a site trial using the intended dispensing gun and mixer nozzle. Measure holes completed per cartridge, curing time at actual site temperature, installation speed, rejected holes, nozzle consumption, and cleaning requirements. | Labor and waste can exceed the difference in cartridge price. A product with consistent dispensing and predictable curing may deliver a lower installed cost and more reliable daily output. |
Data note: Price, shelf-life, storage, transport classification, performance, and lead-time ranges are indicative planning benchmarks rather than quotations or product certifications. Always confirm the current technical data sheet, Safety Data Sheet, local regulations, and project-specific approval requirements before purchase.
Reliable chemical anchor purchasing starts with complete documentation. Request the SDS, technical data sheet, certificate of analysis, batch number, and expiry date. Check whether documents match the exact formulation and shipment. Storage instructions should state temperature, humidity, and shelf-life limits. A clear label helps warehouse staff avoid costly mistakes. Translated documents may also prevent confusion at the job site.
Safety details deserve practical attention. Confirm hazard classifications, required gloves, eye protection, ventilation, and disposal procedures. Ask for curing times under cold, hot, dry, and damp conditions. Never assume one installation method suits every site. A small sample test can reveal poor adhesion or unexpected curing behavior.
I have seen buyers focus on price and overlook storage damage. That decision rarely stays cheap.
Compatibility must match the substrate, threaded rod, hole diameter, embedment depth, and expected load. Request independent test evidence where projects demand it. Confirm performance on cracked concrete, wet holes, or seismic applications only when documented. After-sales support should include installation guidance, troubleshooting, complaint handling, and reasonable response times. Ask who provides technical help across time zones. Keep batch records and site photos. They make investigations faster, although records are often incomplete when problems appear.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







