Choosing the right Ppr Heater Machine can determine whether a pipe joint stays reliable or fails under pressure. In real workshop conditions, the difference often appears in small details: uneven heating, a loose thermostat, or a plate that cools too quickly. A machine may look powerful on paper, yet perform poorly during repeated installation work.
This guide shares seven practical tips for evaluating heating power, temperature control, socket quality, portability, safety features, and after-sales support. These points reflect common concerns faced by plumbers, contractors, and maintenance teams. A dependable unit should heat PPR pipes evenly, hold a stable temperature, and make each connection easier to inspect. Clear indicators and heat-resistant handles also matter when the workspace is crowded or dusty.
Small details matter.
Experience has taught many installers not to choose by wattage alone. A higher rating does not automatically mean better control or longer service life. Some machines feel solid during a short test but become difficult to handle after hours of work. That weakness is easy to overlook. No checklist is perfect, either. Pipe size, job frequency, local voltage, and operator skill can change the best choice. By examining these factors carefully, buyers can reduce wasted material, improve joint consistency, and select a Ppr Heater Machine that fits real working conditions rather than marketing promises.
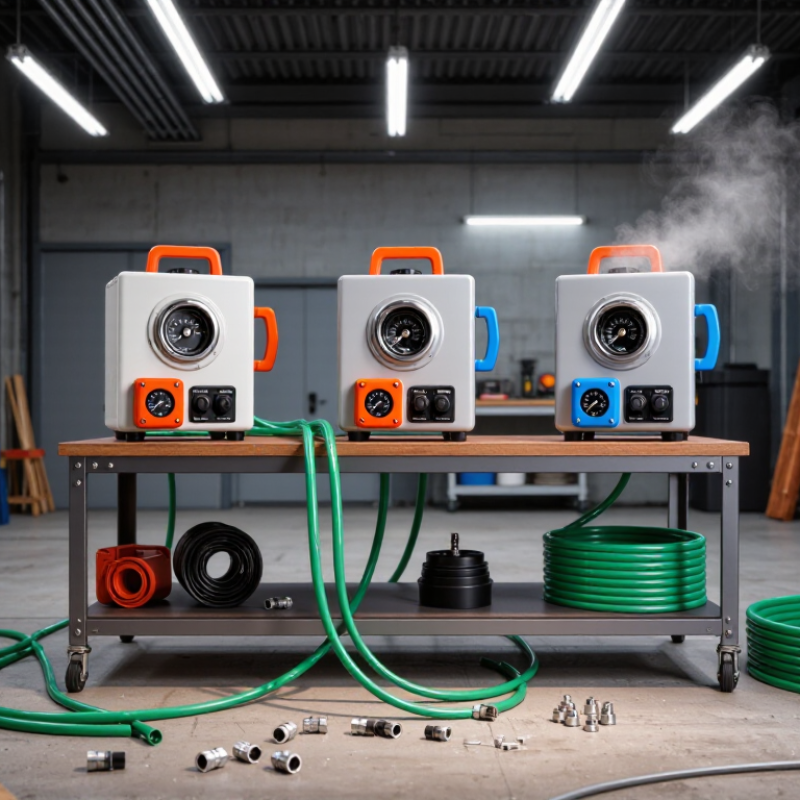
A PPR heater machine softens polypropylene random copolymer pipe and fittings for socket fusion. It uses an electrically heated plate with matching male and female dies. The pipe end melts around the fitting socket, then both parts join under controlled pressure. After cooling, the joint becomes one continuous plastic connection.
ISO 15874 sets performance requirements for polypropylene piping systems. DVS 2207-11 also provides practical guidance for heating and joining thermoplastics. The 2023 PlasticsEurope report recorded 400.3 million tonnes of global plastics production in 2022. This scale shows why stable processing matters. Still, a higher temperature is not automatically better. Excess heat can create an internal bead and restrict water flow.
Tip 1: Check temperature accuracy with an independent thermometer.
Tip 2: Choose dies that match the pipe size.
Tip 3: Confirm the machine reaches its rated temperature quickly.
Tip 4: Select a firm frame and non-slip base.
Tip 5: Keep heating surfaces clean and undamaged.
Tip 6: Follow the pipe maker’s heating time, insertion depth, and cooling period.
Tip 7: Inspect the finished joint for even fusion, alignment, and excessive internal swelling.
Small errors matter. A cheap temperature display may look professional but still drift during repeated work. Calibration is often overlooked, and that is a weakness worth correcting.
PPR projects need the right heater machine, not simply the hottest one. ISO 15874 defines performance requirements for polypropylene piping systems, while DVS 2207-11 emphasizes controlled heating and clean joint preparation. In field work, socket fusion is usually suitable for small indoor pipes. Butt-fusion equipment fits larger diameters and workshop fabrication. Electrothermal tools are different and should not be confused with standard heater plates.
Tip 1: Match the machine to the pipe diameter. A 20 mm pipe needs a different socket set than a 110 mm line. Tip 2: Check the temperature range. Many PPR socket-fusion procedures use about 260°C, but the machine must hold that temperature steadily. Tip 3: Choose interchangeable dies for mixed project sizes. Fixed tooling can become expensive and inconvenient.
Tip 4: Prefer a calibrated thermostat and clear temperature indicators. DVS guidance stresses process control, not guesswork. Tip 5: Inspect heating-plate coating and die alignment before every job. Tip 6: Select a portable unit for repair work, but use a stable frame for long production runs. Tip 7: Confirm electrical protection and local operating requirements. The OECD Global Plastics Outlook reported global plastic waste reached 353 million tonnes in 2019, so reducing failed joints and discarded pipe matters. I still find temperature readings can be misleading near dusty sites. Record heating times, ambient conditions, and joint results; small notes often reveal the real machine problem.
| Tip | Selection Dimension | Recommended Machine Type | Typical Working Range or Specification | Why It Matters | Practical Check Before Purchase |
|---|---|---|---|---|---|
| 1 | Pipe Diameter Range | Socket fusion heater for small diameters; butt fusion machine for larger diameters | Socket fusion is commonly used for approximately 20–110 mm pipes. Butt fusion equipment is commonly selected for pipes from about 63 mm upward, depending on the model. | The heater, clamps, dies, and heating plate must match the outside diameter and wall thickness of the pipe system. | List the smallest and largest pipe diameters used on the project and confirm that the machine includes compatible heating sockets, inserts, or tooling. |
| 2 | Connection Method | Socket fusion, butt fusion, or electrofusion equipment | Socket fusion heats the pipe outside and fitting inside. Butt fusion heats and joins matching pipe ends. Electrofusion uses fittings with embedded electrical heating wires. | Each method requires different equipment, operator procedures, and installation space. | Choose the method specified by the pipe and fitting manufacturer, local installation standard, and project design. |
| 3 | Heating Temperature Control | Thermostatically controlled heating plate or electronically controlled system | PPR fusion is generally performed with a heating surface near 260°C, while the exact value and heating time should follow the applicable standard and manufacturer instructions. | Stable temperature helps create a uniform melt layer and reduces the risk of cold joints, overheating, or material degradation. | Check the temperature adjustment range, display readability, sensor response, and whether the heating surface maintains an even temperature. |
| 4 | Power Supply and Heating Speed | Portable single-phase unit for field work; higher-power unit for continuous workshop use | Many portable heaters operate on 110–120 V or 220–240 V AC. Typical power ratings vary from approximately 600 W to more than 2,000 W, depending on size and design. | Insufficient power can lengthen warm-up time and reduce productivity, especially in cold environments or during repeated joints. | Compare the machine voltage and wattage with the available supply, generator capacity, extension-cord rating, and expected daily workload. |
| 5 | Portability and Installation Space | Handheld or compact bench-mounted heater for confined locations; hydraulic or powered frame for large pipes | Compact socket-fusion tools are suitable for repair work and indoor installations. Framed butt-fusion machines provide controlled alignment but require more working clearance. | A machine that is difficult to position can cause pipe misalignment, uneven pressure, or unsafe handling. | Measure access openings, trench width, wall clearance, and available workspace before selecting the machine format. |
| 6 | Clamping, Alignment, and Pressure Control | Guided socket tool for basic joints; clamping and hydraulic systems for repeatable butt fusion | Butt-fusion machines normally use fixed or adjustable clamps, a facing tool, a heating plate, and a controlled joining mechanism. Pressure requirements depend on pipe size, SDR, material, and procedure. | Accurate alignment and controlled joining force are essential for a consistent fusion bead and reliable joint strength. | Inspect clamp rigidity, alignment adjustment, facing-tool quality, pressure control, and the availability of pipe supports. |
| 7 | Safety, Maintenance, and Verification | Machine with insulated handles, stable support, replaceable non-stick coatings, and accessible service parts | The heating plate should have electrical protection and a durable non-stick surface. Operators should use heat-resistant gloves and follow documented heating, insertion, cooling, and inspection procedures. | Good safety features and maintenance access reduce burns, electrical risks, contamination, and inconsistent weld quality. | Confirm electrical protection, grounding requirements, calibration or temperature verification options, spare-part availability, cleaning instructions, and training documentation. |
Important: Temperature, heating time, insertion depth, cooling time, and joining pressure vary with pipe diameter, wall thickness, material grade, ambient conditions, and the applicable installation standard. Always follow the approved fusion procedure for the specific PPR pipe and fitting system.
Choosing the best PPR heater machine starts with the pipe sizes you actually install. Check heating power against socket capacity and daily workload. Higher wattage can shorten warm-up time, but it may waste energy on small fittings. Look for stable output, not impressive numbers alone. A practical test is simple: measure the time needed to heat a cold die and a loaded die.
Temperature control deserves close attention. Choose a machine with a clear display, adjustable settings, and a responsive thermostat. Confirm that the reading remains steady while several joints are prepared. Uneven heat can soften one side of a pipe and weaken the joint. Check whether the heating plate distributes heat evenly across its surface. Verify the recommended temperature range in the technical manual. Some controls look precise but react slowly. That matters.
Heating speed is useful only when temperature stability follows it. Compare warm-up time, recovery time, and performance after repeated cycles. Select durable, well-insulated handles and a plate that resists surface damage. Inspect calibration records or request a practical demonstration before purchase. Keep spare dies available for common pipe diameters. I once favored speed over control; the first joints looked fine, but later alignment exposed the mistake. A slower, steadier machine is often easier to trust on site.
Choosing a PPR heater machine starts with pipe compatibility, not the lowest price. Check the pipe diameter range and included socket sizes. The machine should heat your actual PPR materials evenly. Review its temperature range, heating time, and fitting instructions. A loose socket can produce an uneven joint. That mistake is easy to miss.
Construction quality affects daily work. Look for a thick heating plate and firmly attached sockets. Stainless steel surfaces usually resist workshop wear and cleaning. A stable base prevents the hot tool from tipping. Insulated handles reduce discomfort during repeated installation. Check the power cord, plug, and housing for signs of weakness. Small details matter. However, a heavy body does not always mean better performance. I once treated weight as proof of quality, but that assumption was incomplete.
Safety features deserve careful attention. Choose adjustable temperature control with a clear indicator light. Overheat protection can reduce damage during long jobs. A grounded plug and heat-resistant cable are important for safer operation. Confirm that the electrical design suits your workplace and local requirements. Keep the heater on a dry, stable surface. Use protective gloves and eye protection when handling heated pipes. Read the technical sheet, not only the sales description. Test one sample joint before starting a large installation. The result should show even melting, proper alignment, and no visible gaps. Temperature settings may need small adjustments. That is normal.
7 Tips to Choose the Best PPR Heater Machine
Tip 1: Check portability before comparing heater power. A compact machine with a handle, protective case, and a two-meter cable moves easily between floors. It should remain stable on a narrow workbench. Excessive weight becomes tiring during repeated pipe joints. Practical site checks often reveal this weakness.
Tip 2: Compare maintenance needs, not only the purchase price. Look for replaceable heating plates, clear temperature controls, and accessible electrical components. PPR welding commonly requires controlled heating near 260°C, consistent with guidance used around ISO 15874 piping systems. A damaged coating can affect joint quality. That detail is easy to miss.
Tip 3: Calculate operating cost from real measurements. Record rated watts, warm-up time, working hours, and local electricity tariffs. The IEA Electricity 2024 report forecasts global electricity demand to grow by about 3.4% annually through 2026. Energy prices may therefore deserve more attention. A 1,500-watt heater running four hours consumes roughly 6 kWh, before cycling losses.
Tip 4: Inspect thermostat accuracy and temperature recovery. A machine that reheats slowly can delay crews and increase idle consumption. Choose models with readable displays and stable thermal control. Keep spare fuses and inspect cables regularly. Small failures create large interruptions.
Tip 5: Evaluate the full operating cost. Include transport, calibration, replacement plates, downtime, and technician training. The cheapest unit is not always economical. I have seen buyers overlook storage damage and regret it later. That judgment may sound obvious, yet it remains common.
Estimated annual operating cost by selection factor for a generic PPR heater machine
This planning model uses a 2,000-hour annual workload, an electricity rate of $0.15/kWh, labor at $25/hour, and routine maintenance based on typical inspection and replacement tasks. Prioritize portability, stable temperature control, durable heating elements, easy cleaning, accessible spare parts, safe operation, and total operating cost rather than purchase price alone.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru