Buying Auto Pipe Welding equipment is not only a price comparison. It is a production decision involving pipe material, diameter, wall thickness, joint design, and factory conditions. A machine that performs well on stainless steel may struggle with carbon steel or narrow root gaps. Small differences matter.
John C. Lippold, a respected welding-metallurgy expert, explains a central principle: “Weldability is not simply a material property; it depends on the welding process and procedure.” This idea guides the ten tips in this article. Global buyers should examine welding current stability, torch alignment, wire feeding, shielding-gas control, and automated travel speed. They should also request sample welds, procedure records, inspection results, and clear maintenance terms from suppliers.
Look closely at the bead.
A polished brochure proves little. Ask how the system handles real pipe sections, changing wall thicknesses, imperfect fit-up, and repeated production cycles. Check whether operators can adjust parameters without creating inconsistent results. Remote support, spare-part access, training, and installation assistance also affect long-term value.
Some buyers focus too heavily on automation speed. That can be a mistake. A faster cycle is not useful if repairs increase or weld quality varies between shifts. Even experienced teams may overlook cable routing, fixture rigidity, or workshop temperature. These details deserve practical testing.
The following guide offers a buyer-focused framework for comparing Auto Pipe Welding systems. It does not promise one universal solution. Instead, it encourages careful questions, documented trials, and honest evaluation before purchase.
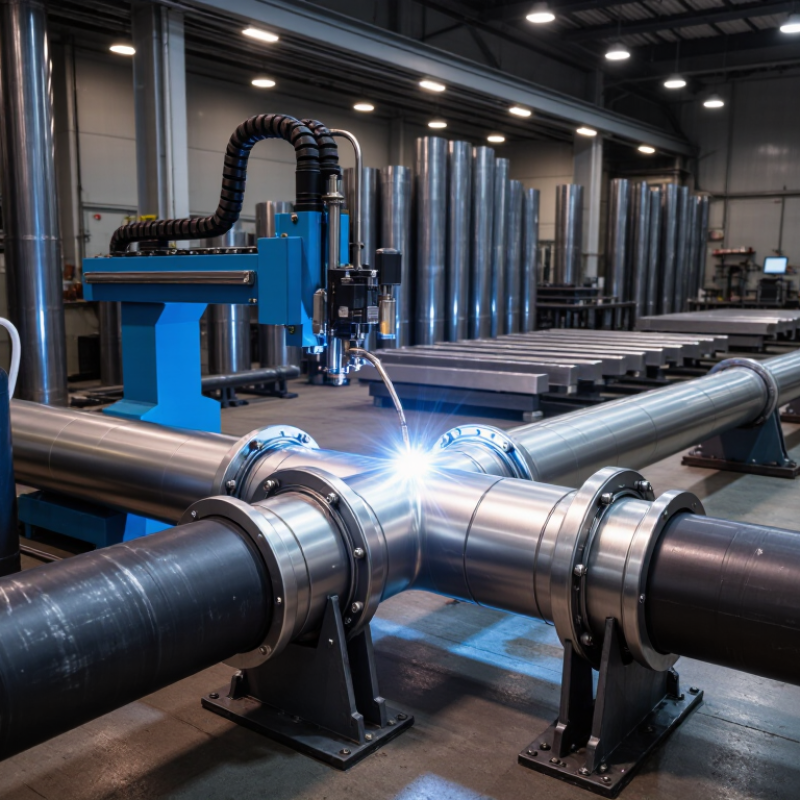
Tip 1: Define the pipe OD and wall thickness before requesting an automatic welding system. A 273 mm outside diameter pipe with a 12.7 mm wall needs different tooling than a 508 mm pipe with a 6 mm wall. These dimensions affect clamping, torch travel, heat input, and weld access. Specify tolerances, ovality, joint preparation, and root gap. Do not rely on nominal size alone. ISO 15614-1 requires welding procedure qualification against defined essential variables, including thickness ranges and joint details. A rushed dimensional sheet can still mislead suppliers.
Tip 2: State the material grade and require an ISO 15614-1 qualified WPS. Carbon steel, stainless steel, duplex, and nickel alloys respond differently to heat, shielding gas, and interpass temperature. Include the exact standard, grade, delivery condition, filler classification, and preheat limits. Ask for the supporting PQR, test method, and acceptance criteria. The International Institute of Welding highlights procedure control as a major factor in repeatable weld quality. That matters when automation removes some operator correction. It does not remove engineering responsibility.
The American Welding Society’s 2023 workforce report projected a need for about 330,000 new welding professionals in the United States by 2028. Consistent documentation helps reduce dependence on scarce expert judgment. In practice, buyers should compare the proposed machine settings with the qualified WPS, then run a representative trial using real pipe dimensions. Small deviations expose weaknesses early.
Auto pipe welding rewards disciplined preparation, not faster torch movement. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. Automation is growing, but accurate joint fit-up still controls weld quality.
Tip 3: Match ASME B16.25 bevels with AWS D10.10 preparation guidance. B16.25 defines butt-welding-end geometry, including bevel angle, root face, and transition details. Do not assume every pipe uses one standard angle. Confirm the project drawing, wall thickness, WPS, and material grade. AWS D10.10 emphasizes controlled heating and practical preparation for pipe welding. A 1–2 mm root-face error can alter penetration and increase repair risk. Measure each end with a bevel gauge. Check ovality, misalignment, and burrs before tacking.
Tip 4: Treat fit-up as a repeatable inspection point. I have seen clean bevels fail because the internal mismatch was ignored. Keep tack welds compatible with the qualified procedure. Remove cracked or contaminated tacks. Use calibrated gap gauges, not visual judgment alone. Record bevel angle, root opening, and alignment on the inspection sheet. This matters when production moves across countries or shifts. The American Welding Society projected a shortage exceeding 330,000 welding professionals in the United States by 2028. Consistent measurements reduce dependence on individual memory, although the checklist itself still needs review. A perfect record cannot rescue a poorly chosen joint design.
Orbital welding quality depends on matching current, travel speed, arc gap, and wall thickness. Use a qualified welding procedure, then confirm it with a test coupon. A small change in travel speed can affect penetration and bead shape. Record the settings for every pipe size and joint position. Keep the numbers visible near the welding station. This reduces guesswork during global production.
Do not trust preset values blindly. They may suit one alloy but fail on another. A practical review is still necessary. Check the weld profile under proper lighting. Look for undercut, uneven width, or incomplete fusion. In my experience, rushed parameter changes often create defects that appear only after inspection.
For stainless steel, maintain oxygen below 50 ppm during root welding and until the hot section cools sufficiently. Use an oxygen monitor, not appearance alone. Brown or blue discoloration can signal inadequate shielding. Seal both ends with suitable purge dams, and check for leaks before introducing argon. Keep gas flow steady rather than excessively high, because turbulence can draw room air into the joint.
Measure oxygen near the weld zone when possible. Readings from a distant outlet may be misleading. A short purge may save gas, but it can damage corrosion resistance and increase rework. I have seen operators rely on a single reading, then discover oxidation inside the root. That mistake deserves a second thought. Reliable records should include purge time, oxygen readings, gas flow, and weld identification.
Before accepting an automated pipe welding line, confirm each welder’s qualification for the actual procedure. The certificate should match the welding process, pipe material, thickness, position, and filler metal. Check the qualification date and supporting test records. Keep records together. A certificate alone may not prove current competence. Observe whether operators understand parameter limits, joint preparation, and weld acceptance criteria.
Traceability should follow every weld from material receipt to final inspection. Record the heat number, pipe identification, welder ID, machine setting, filler batch, and joint location. A clear weld map makes missing information easier to find. Small gaps matter. In field audits, unidentified repairs often create more risk than visible defects. Do not guess. Require controlled repair records, including the reason, method, and reinspection result. Digital records can help, but only when operators enter accurate data at the right time.
Perform a 100% visual inspection before painting, insulation, or shipment. Use clean lighting and inspect the complete weld circumference. Check alignment, bead shape, undercut, overlap, cracks, arc strikes, spatter, surface pores, and incomplete tie-ins. Measure reinforcement with a suitable weld gauge when required. A second qualified inspector should review unclear findings. Visual inspection cannot detect every internal defect, so the approved inspection plan may require additional testing. That point is easy to overlook. An incomplete checklist can look professional while hiding rushed work. Have inspectors sign only after examining the physical weld and matching it with the traceability record.
Cycle time must be measured at the joint, not in a sales demonstration. Record fit-up, purge, arc time, cooling, repositioning, and inspection. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. That growth shows automation matters, but speed alone does not prove value. A shorter arc time may increase rework if heat input, alignment, or penetration becomes unstable.
Measure the arc.
Consumables can quietly control operating cost. Compare wire usage, shielding-gas flow, tungsten life, purge volume, and nozzle replacement frequency. The American Welding Society has projected a U.S. welding workforce shortage exceeding 300,000 people by 2028. Better automation may reduce labor pressure, yet consumable waste still damages cost per joint. Use this calculation: total purchase, labor, energy, consumables, maintenance, and rework divided by accepted joints. Do not divide by completed welds only.
Warranty terms deserve the same scrutiny. Request coverage periods, response times, spare-parts availability, and exclusions for fixtures, software, and operator error. ISO 12100 risk-management principles support documenting foreseeable operating risks before equipment acceptance. A generous warranty may still be weak if downtime is excluded. Ask for a live acceptance test using your pipe diameter, wall thickness, joint design, and production speed. My practical concern is simple: one impressive trial can hide a difficult week on the factory floor. Keep the comparison imperfect but honest.
| Welding Configuration | Typical Cycle Time (min/joint) | Consumables Used | Consumable Cost (USD/joint) | Typical Warranty Offered (months) | Estimated Operating Cost (USD/joint) | Best-Fit Purchasing Scenario |
|---|---|---|---|---|---|---|
| Manual GTAW with filler wire | 90–150 | Shielding gas, stainless filler wire, tungsten electrodes, cups, and occasional abrasives | $8–$18 | 12–24 | $85–$165 | Low-volume work, frequent design changes, difficult access, or projects with limited automation budget |
| Orbital GTAW with closed welding head | 35–60 | Shielding gas, filler wire when required, tungsten electrodes, inserts, and purge accessories | $10–$24 | 12–24 | $55–$115 | Repeatable tube and pipe production where consistent penetration, low rework, and documented parameters are priorities |
| Mechanized GMAW with positioner | 25–45 | Solid wire, shielding gas, contact tips, nozzles, liners, and anti-spatter compound | $7–$16 | 12–24 | $45–$95 | Medium- to high-volume fabrication with suitable joint access and a strong focus on throughput |
| Mechanized FCAW or pulsed GMAW | 30–55 | Flux-cored wire or solid wire, shielding gas where applicable, contact tips, liners, and cleaning tools | $9–$22 | 12–24 | $50–$105 | Carbon-steel or low-alloy pipe fabrication where deposition rate is more important than a minimal heat input |
| Automated multi-process pipe cell | 20–40 | Process-specific wire or filler, shielding gas, contact parts, tungsten or torch components, and fixtures | $10–$25 | 18–36 | $55–$110 | High-volume projects that can justify dedicated tooling, qualification, programming, and preventive maintenance |
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru