Choosing the 2026 best Acrylic Impact Modifier for PVC is not a brand-name exercise. It is a fit-for-purpose decision. Buyers should compare impact performance, processing behavior, consistency, and total formulation cost. A modifier that performs well in a rigid window profile may not suit a pipe compound or a thin molded part. The details matter: resin grade, extrusion temperature, fusion time, and the part’s expected service conditions can all change the result.
Ask suppliers for current technical data, recommended dosage ranges, and application-specific test results. Then validate shortlisted grades in your own formulation. A room-temperature impact result alone may not predict performance after cold storage or outdoor exposure. Small lab samples can also behave differently from a production run. That gap deserves attention. Acrylic Impact Modifier selection is a balance, not a shortcut; higher impact values may come with processing or cost trade-offs. This guide examines practical criteria for comparing options, while noting where published data may leave questions unanswered. No named expert quotation is included because no source was provided; inventing one would make the advice less trustworthy.
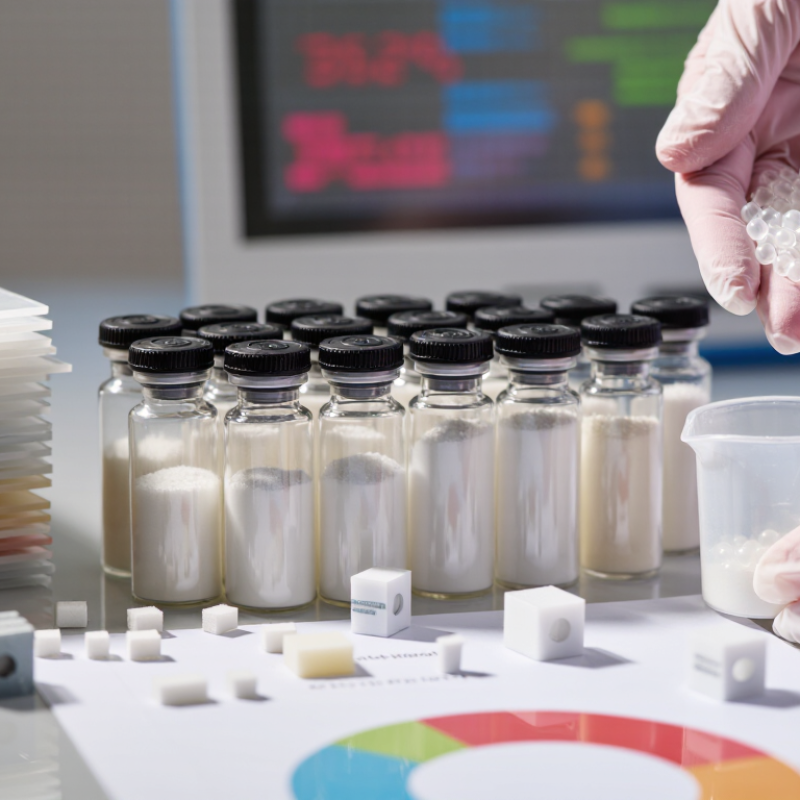
Acrylic impact modifiers (AIMs) are typically core-shell particles added to rigid PVC. Their rubbery cores deform under sudden stress, absorbing energy and helping slow crack growth. The acrylic shells support dispersion and bonding within the PVC matrix. When particles are poorly dispersed, protection can be uneven. Small details matter.
During impact, well-dispersed particles can encourage localized deformation instead of a brittle fracture. This helps explain why AIMs are used in products such as PVC profiles and pipes. Plastics Europe’s Plastics – the Fast Facts 2023 report estimates that PVC represented about 12.6% of global plastics production in 2022, underscoring its industrial scale. Tips: Test finished parts, not just resin samples. Compare impact results at relevant temperatures using consistent specimen preparation, such as ASTM D256 or ISO 179 methods. Also track stiffness and processing behavior. A strong impact result may come with trade-offs, and a test number alone can hide them.
Acrylic impact modifiers (AIMs) are polymer additives used mainly in rigid PVC to improve resistance to impact and brittle failure. Many are made with a flexible acrylic-rubber phase and a harder acrylic phase. The flexible phase helps absorb impact energy; the surrounding phase helps the modifier disperse in the PVC matrix. Actual performance depends on the modifier grade, PVC formulation, processing conditions, and test method.
| Buyer dimension | What an acrylic impact modifier does | What to evaluate in PVC | Relevant test or check |
|---|---|---|---|
| Impact modification | Adds a flexible phase that can deform and help dissipate energy when rigid PVC is struck. | Impact performance at the product’s service temperature, wall thickness, and expected loading conditions. | Notched impact testing, such as ASTM D256 or ISO 180; compare results only when specimen preparation and test conditions match. |
| Weathering suitability | Acrylic-based modifiers are commonly selected for outdoor rigid-PVC applications where weatherability is important. | Color change, surface appearance, and retention of impact performance after exposure; the complete PVC formulation also affects results. | Accelerated weathering using a defined method, such as ASTM G154 or ASTM G155, followed by relevant appearance and mechanical tests. |
| Processing and fusion | Can influence PVC fusion behavior, melt flow, and the balance between processability and finished-part performance. | Extruder output, melt temperature, torque or motor load, surface finish, and consistency at the intended production rate. | Run a controlled processing trial using the same PVC compound, equipment settings, and production conditions. |
| Surface and appearance | A suitable grade can help maintain the surface quality required in rigid-PVC products, but the result depends on dispersion and processing. | Gloss, color, visible defects, and surface consistency in the actual molded or extruded part. | Inspect finished production samples and define acceptance criteria for the application. |
| Typical application fit | Often considered for rigid-PVC building and construction products where impact resistance and outdoor durability are key requirements. | Match the modifier to the product specification, such as profiles, siding, or other rigid-PVC components; do not assume one grade suits every process. | Check the end-product specification and validate performance on production-representative samples. |
| Comparison with other modifier families | AIMs are one option among PVC impact modifiers. CPE and MBS are other established families, each with different performance and formulation trade-offs. | Acrylic grades are often considered when outdoor weatherability matters; MBS grades are commonly used when transparency is important, while CPE grades are used in a range of rigid-PVC formulations. Confirm suitability for the specific product. | Compare equivalent formulations and test conditions rather than relying on modifier-family labels alone. |
| Selection and validation | The “best” modifier is the grade that meets the application’s performance requirements and runs reliably in the buyer’s PVC formulation and process. | Review technical data, recommended handling and processing guidance, formulation compatibility, and lot-to-lot quality controls. | Request current technical documentation and conduct a controlled laboratory evaluation followed by a production trial. |
Note: The table describes general material-selection considerations, not guaranteed performance values. Test results are meaningful only when formulation, specimen preparation, conditioning, and test conditions are reported and comparable.
Acrylic impact modifier performance in PVC depends on more than dosage. Particle size and distribution affect how evenly stress spreads through the compound. A well-dispersed modifier can help blunt cracks; poor dispersion may leave weak spots. Core-shell structure and compatibility with the PVC matrix also influence impact strength, surface finish, and processing behavior. Small details matter. Heat stability matters too, especially during long extrusion runs.
Measure performance using controlled tests, not supplier claims alone. ASTM D256 reports notched Izod impact resistance, typically in J/m; ISO 179-1 reports Charpy impact strength, commonly in kJ/m². These results are not directly interchangeable. Record temperature, notch, specimen thickness, and conditioning alongside every result. The standards define test methods, not a universal pass value, so compare formulations under identical conditions. A single room-temperature result can miss brittle behavior in cold service.
Tips: Test at both room temperature and the lowest expected use temperature. Check impact strength alongside fusion, melt flow, and surface appearance. If impact improves but extrusion becomes unstable, revisit dosage and dispersion. That trade-off is easy to overlook. Cite ASTM D256 and ISO 179-1 in your test records for traceable comparisons.
2026 Best Acrylic Impact Modifier for PVC Buyers
Choosing an acrylic impact modifier means matching the grade to the part, not chasing the highest impact figure. PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023, underscoring the scale of performance demands across applications. For PVC, compare impact strength alongside stiffness, fusion behavior, melt flow, and surface finish. A pipe fitting and an outdoor profile may need different balances. Check the supplier’s test method and specimen conditions; values from different methods are not directly comparable.
Review particle-size data, recommended loading, and compatibility with your PVC formulation. Then test candidate grades in the actual compound and processing window. Use notched impact testing, such as ISO 179 or ASTM D256, and record results at the temperatures your product will face. Track extrusion torque, die buildup, and color after heat exposure. These details can expose trade-offs that a single datasheet value hides. A lab result is useful, but it may not predict every production line.
Tips: Keep resin, stabilizer, lubricant, and test conditions constant during trials. Change one factor at a time. Also compare more than one modifier level; the best result may not occur at the highest loading. One limitation is easy to miss: repeated testing takes time, but skipping it can leave a grade that looks good on paper and disappoints in the mold.
2026 Best Acrylic Impact Modifier for PVC Buyers
Choosing a Modifier for Processing Conditions and End-Use Needs
Choosing an acrylic impact modifier starts with your actual processing conditions, not a headline impact value. A rigid profile running at high line speed may need a different balance than a thick, injection-molded fitting. Check fusion behavior, melt stability, and dispersion at your usual equipment settings. Small changes matter. If a modifier slows fusion, adjusting temperature or screw speed may affect surface finish and cycle time.
Match testing to the product’s service conditions. For outdoor profiles, compare impact performance before and after weathering; for parts used in cold areas, test impact at relevant temperatures. A neat laboratory result can still mislead if the trial uses a different filler level or stabilizer package. One catch: there is no universal best loading. Run a controlled production trial, record torque, output, appearance, and impact results, then review the trade-offs. I would not choose from one strong impact figure alone.
Choose a modifier for processing conditions and end-use needs
Illustrative qualitative screening scores (1 = lower, 5 = higher), not measured or guaranteed product performance. Acrylic impact modifiers are commonly selected for impact improvement and outdoor weatherability. Confirm the specific grade, loading, PVC formulation, processing conditions, and end-use requirements with supplier data and testing.
For PVC buyers, supplier selection should start with reproducible evidence, not a low price per kilogram. The VinylPlus Progress Report 2024 records 737,645 tonnes of PVC recycled in Europe during 2023, highlighting the growing importance of consistent material performance across PVC applications. Ask suppliers for current technical data, batch certificates, traceability, and test conditions. Compare impact strength using the same method, such as ASTM D256 or ISO 179, and test samples in your own formulation. A number without test conditions is hard to judge.
Total cost includes modifier dosage, processing time, rejected parts, and delivery reliability. Run trials on the same equipment and record impact results, fusion behavior, and scrap rates. PlasticsEurope’s 2024 report estimates global plastics production at 413.8 million tonnes in 2023; broad market growth does not guarantee stable supply or suitable quality. Request samples from more than one batch, then check whether results stay within agreed limits. Small details matter. I still find spreadsheets miss a real production variable now and then, so keep trial notes and review them with operators before approving a supplier.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru