Choosing the right Carbon Graphite Rods can determine whether an industrial process runs smoothly or fails under pressure. Heat, electrical current, chemical exposure, and repeated handling all affect rod performance. A workshop furnace may expose rods to intense heat, while an electrochemical system demands stable conductivity and clean surfaces.
Andrew Miller, an energy materials analyst at Benchmark Mineral Intelligence, has described graphite as “the largest component in a lithium-ion battery by weight.” This observation also reflects graphite’s wider industrial importance. Material selection should consider purity, density, grain structure, machining accuracy, and oxidation resistance. A dense rod may perform well in a high-temperature furnace. A more porous grade may suit a different application, but it can wear faster.
Small details matter.
This guide reviews ten Carbon Graphite Rods for industrial use. It compares conductivity, thermal stability, chemical resistance, dimensional consistency, and practical durability. The focus is not only on laboratory specifications. Real operating conditions often expose weaknesses that product sheets overlook. A rod that appears suitable on paper may crack after repeated heating and cooling. Another may remain stable but require careful surface protection.
There is no universal best choice. That is worth remembering. Engineers should verify supplier test data, operating temperatures, tolerances, and application history before purchasing. Some comparisons may remain imperfect because manufacturers use different testing methods. Still, the shortlist offers a practical starting point for maintenance teams, furnace operators, and materials engineers seeking dependable graphite performance.
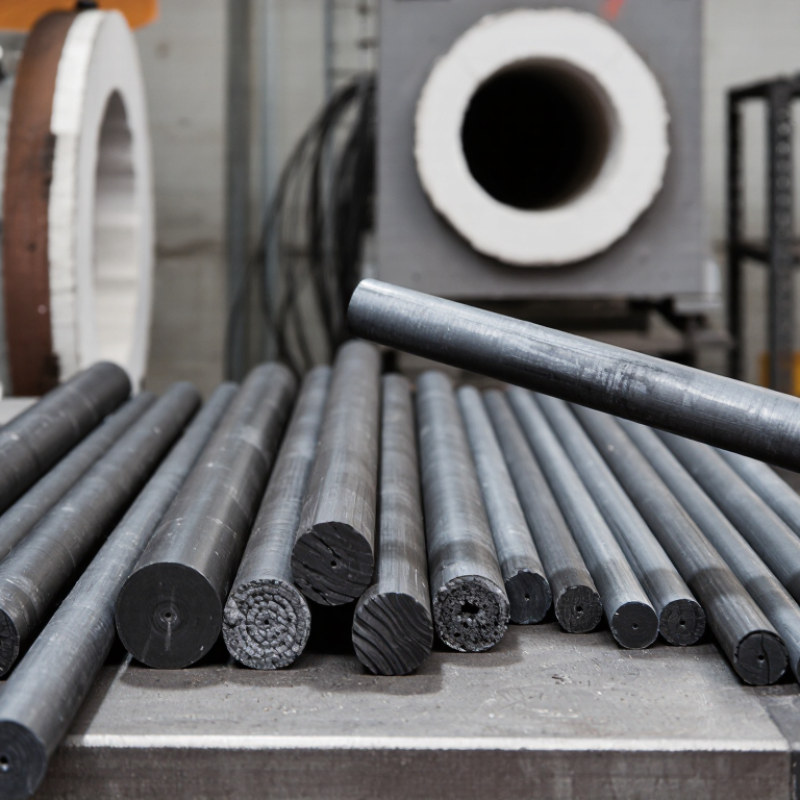
Carbon graphite rods are solid, cylindrical components made from carbon-rich graphite. Their layered crystal structure allows atoms to slide across basal planes. This creates low friction, good electrical conductivity, and strong heat resistance. The rods also tolerate thermal shock better than many ordinary ceramics. However, graphite remains brittle. A small edge impact can create a crack that grows during heating.
Industrial performance depends on density, grain size, and impregnation quality. Fine-grained rods usually provide smoother surfaces and better dimensional control. High-density grades resist gas penetration and mechanical wear. Porous grades may perform acceptably in less demanding fixtures. In furnace zones, technicians often inspect rod ends for oxidation, chips, and uneven heating. These details matter more than appearance. Machining accuracy also affects electrical contact and current distribution.
Industrial functions include electrodes, heating elements, furnace supports, glass-processing fixtures, and electrochemical components. The USGS Mineral Commodity Summaries 2025 estimated global natural graphite production at about 1.6 million metric tons in 2024. Demand pressure is increasing. The International Energy Agency’s Global Critical Minerals Outlook 2024 projected clean-energy graphite demand could rise roughly fourfold by 2040 under its stated policy scenario. That forecast supports wider industrial use, but it does not make every rod suitable. A perfect ranking is unrealistic. Selection should consider temperature, atmosphere, current density, load, and replacement access. Oxidizing conditions remain a weakness, even when the rod appears oversized.
| No. | Generic Rod Type | Typical Structure | Typical Density (g/cm³) | Electrical Resistivity (µΩ·m) | Thermal Conductivity (W/m·K) | Recommended Industrial Function | Key Selection Advantage |
|---|---|---|---|---|---|---|---|
| 1 | Fine-Grain Isostatic Graphite Rod | Uniform, isotropic, fine-grained carbon matrix | 1.75–1.90 | 8–15 | 80–140 | Semiconductor processing, high-temperature fixtures, precision electrodes | Low porosity and consistent properties in multiple directions |
| 2 | High-Purity Graphite Rod | Purified graphite with very low metallic and ash content | 1.70–1.85 | 8–16 | 70–130 | Crystal growth, vacuum furnaces, analytical and laboratory equipment | Minimizes contamination during high-temperature processing |
| 3 | Electrode-Grade Graphite Rod | Medium-to-coarse grain with good electrical conductivity | 1.60–1.75 | 4.5–8.0 | 90–160 | Electric arc heating, resistance furnaces, electrochemical equipment | Low electrical resistance and good thermal-shock tolerance |
| 4 | EDM Graphite Rod | Fine, homogeneous particles optimized for machining | 1.70–1.85 | 8–14 | 80–120 | Electrical-discharge machining electrodes and intricate molds | Excellent machinability and stable dimensional accuracy |
| 5 | Vibration-Molded Graphite Rod | Pressed grain structure with practical mechanical strength | 1.55–1.75 | 10–20 | 60–110 | Furnace supports, thermal shields, crucible components and tooling | Cost-effective for large cross-sections and general furnace service |
| 6 | Resin-Impregnated Graphite Rod | Open-pore graphite sealed with a resin impregnant | 1.65–1.85 | 10–25 | 20–80 | Corrosive chemical handling, heat exchangers and process equipment | Reduced permeability and improved resistance to liquid chemicals |
| 7 | Carbon-Graphite Composite Rod | Graphite combined with carbon reinforcement or a carbonized binder | 1.55–1.80 | 10–30 | 30–100 | Mechanical wear parts, sliding contacts and custom thermal tooling | Balances electrical conductivity, strength and wear resistance |
| 8 | Pyrolytic Graphite Rod | Highly oriented layered carbon deposited by chemical vapor processes | 2.05–2.25 | 0.5–8 parallel to layers | 500–1,500 parallel to layers | Thermal management, high-temperature research and specialized aerospace components | Exceptional in-plane thermal conductivity and anisotropic behavior |
| 9 | Flexible Graphite Rod | Expanded natural graphite compressed into a flexible form | 1.0–1.6 | 10–30 | 5–30 | Packing, sealing, valve stems and thermal expansion joints | Conforms to irregular surfaces and tolerates thermal cycling |
| 10 | Antioxidation-Coated Graphite Rod | Graphite substrate protected by a ceramic or refractory coating | 1.65–2.20 | 8–25 | 30–150 | High-temperature fixtures where limited air exposure may occur | Slows oxidation compared with uncoated graphite in suitable atmospheres |
| Technical note: Values are representative ranges for industrial carbon and graphite materials. Actual properties depend on raw material, grain size, forming method, heat treatment, impregnation, coating, measurement direction and test standard. Graphite can oxidize rapidly in air at elevated temperatures; high-temperature use is generally performed in vacuum or an inert atmosphere. | |||||||

10 Best Carbon Graphite Rods for Industrial Use?
Key Properties for Evaluating Industrial Graphite Rods
Choosing an industrial graphite rod requires more than checking diameter and price. Start with purity, bulk density, grain size, and electrical resistivity. ASTM C559 supports density testing, while ASTM C611 measures resistivity. These values reveal whether a rod can handle heating elements, electrodes, or high-temperature fixtures. A dense rod usually offers better strength, but it may machine less easily. That trade-off matters.
Thermal expansion is another practical concern. Ask for the coefficient of thermal expansion, flexural strength, and oxidation resistance. A rod exposed to repeated heating can crack if expansion is uneven. The International Energy Agency reported in its Global Critical Minerals Outlook 2024 that graphite demand for clean-energy technologies may increase several times by 2040. This wider demand can pressure quality control and supply consistency. Certification alone is not enough.
Inspect the surface under bright light. Look for open pores, edge chips, and visible laminations. Request a batch-specific certificate, not only a general product sheet. The USGS Mineral Commodity Summaries 2024 reported approximately 1.6 million metric tons of global natural graphite production in 2023, yet material grades still vary widely. In my experience, small density differences can change service life. I would also test a sample before approving a large order. It feels slower. It often prevents expensive replacement work.
Typical nominal values for common industrial graphite rod forms. Actual performance varies with grain size, purity, impregnation, machining, and operating atmosphere.
Evaluation guide: Higher density and flexural strength generally improve dimensional stability and mechanical durability, while lower electrical resistivity improves current-carrying performance. Maximum service temperature applies to inert or vacuum environments; oxidation can begin at much lower temperatures in air.
Ten leading carbon graphite rod types serve different industrial demands. Standard electrode rods support electric arc furnace operations. Ultra-high-power rods tolerate intense current and thermal shock. High-purity rods suit semiconductor and laboratory furnace environments. Fine-grain isostatic rods deliver tight tolerances and smooth machining. Vibration-molded rods offer economical structural support. Extruded rods provide consistent lengths for heating systems. Impregnated rods resist oxidation and reduce porosity. Silicon-carbide-coated rods improve surface protection at elevated temperatures. Spectrographic rods support controlled analytical testing. Heating-element rods transfer heat efficiently in vacuum or inert atmospheres.
The World Steel Association reported that electric arc furnaces produced roughly 28% of global crude steel in 2023. That figure shows why electrode reliability matters. The U.S. Geological Survey estimated 2023 global natural graphite mine production at about 1.6 million metric tons. The International Energy Agency also identifies graphite as a major growth material for energy technologies. These reports describe demand pressure, not automatic product quality. A rod may still fail from poor storage, incorrect current density, or uneven furnace loading. I would not treat purity alone as the best buying measure.
Tips: Check ash content, electrical resistivity, bulk density, flexural strength, and maximum service temperature. Match rod diameter to current and heat distribution. Inspect for hairline cracks under bright, angled light. Store rods dry and supported. A practical mistake remains common: choosing the longest rod instead of the most stable grade.
Selecting a graphite rod starts with the operating environment, not the catalogue diameter. Temperature, atmosphere, electrical load, mechanical stress, and contamination risk should be recorded together. In air, oxidation can weaken graphite rapidly above approximately 500°C, while inert or vacuum service allows much higher working temperatures. The exact limit depends on grade, density, and exposure time.
A dense, fine-grained rod usually offers better strength and lower gas permeability. High-purity grades suit molten-metal contact, furnace fixtures, and electrochemical equipment. Measure resistance at the actual temperature, because graphite’s electrical behavior changes as it heats. ASTM C559 provides a recognized method for measuring bulk density and apparent porosity. These values help compare suppliers beyond polished surface appearance.
Market data also supports careful qualification. The U.S. Geological Survey reported about 1.6 million metric tons of natural graphite mine production in 2023, showing a large but variable feedstock base. The International Energy Agency has identified graphite as a major growth material for clean-energy supply chains through 2030. That growth may increase grade variability and lead times.
Request a certificate covering purity, density, ash, dimensions, and thermal-shock testing. Check the rod inside the furnace, not only on paper. A small diameter error can create uneven heating, yet many selection sheets overlook it. Rechecking after thermal cycling is wiser.
Installation begins with the actual process, not a catalog ranking. Check rod diameter, length, density, porosity, and electrical resistance before acceptance. Small cracks can widen during heating. Handle each rod with clean gloves and padded supports. Never clamp graphite against a sharp metal edge. Align the rod carefully, because bending stress often causes early failure. Use compliant fixtures and tighten connections evenly. Allow gradual heating to reduce thermal shock.
Maintenance records should include operating hours, temperature, atmosphere, current, and visible wear. Inspect for pitting, thinning, surface flaking, and loose contacts during scheduled shutdowns. Keep graphite dust away from bearings, sensors, and electrical cabinets. Use local ventilation and suitable respiratory protection when dry brushing or machining is unavoidable. Hot graphite can oxidize quickly in air. Avoid spraying water onto a heated rod. Confirm isolation and stored energy control before inspection.
Service life depends heavily on current density and furnace atmosphere. A rod that looks acceptable may contain an internal crack. Measure resistance trends when practical, rather than relying only on appearance. Replace components after verified wear, unstable output, or dimensional loss. Calendar-based replacement can waste useful material. It can also miss sudden damage. In real maintenance work, records are not always complete, and that weakness affects predictions. Review failures honestly, including installation mistakes, uneven heating, and unsuitable support design. That evidence usually improves the next selection.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







