10 Best CNC Vertical Turning Lathes for Global Buyers
Choosing the right Cnc Vertical Turning Lathe can influence productivity, accuracy, and long-term operating costs. Global buyers face many variables, including workpiece diameter, maximum turning height, spindle torque, ram rigidity, and thermal stability. A machine that looks powerful on paper may struggle with heavy interrupted cuts or unstable shop-floor conditions.
Professor Yusuf Altintas, a respected authority in machining and machine-tool dynamics, describes the machine tool as “a complex mechatronic system.” That view matters here. A vertical turning lathe is not merely a large spindle with a cutting tool. Its control system, drive motors, guideways, lubrication, and structural design must work together. Small weaknesses can appear as vibration marks, poor surface finish, or repeated setup adjustments.
This guide reviews ten leading models for international buyers. The comparison considers real production needs, not only brochure specifications. It examines chuck capacity, motor power, axis travel, live tooling, control compatibility, operator access, and after-sales support. Service response also matters. A technically excellent machine may become expensive when spare parts take weeks to arrive.
No ranking can fit every factory. That is worth admitting. A compact machine may outperform a larger model in flexible batch production. A heavy-duty lathe may be excessive for lighter components. Buyers should verify test-cut results, installation requirements, electrical standards, and local technician support before ordering. The following selection offers a practical starting point, although careful engineering review remains essential.
What Is a CNC Vertical Turning Lathe?
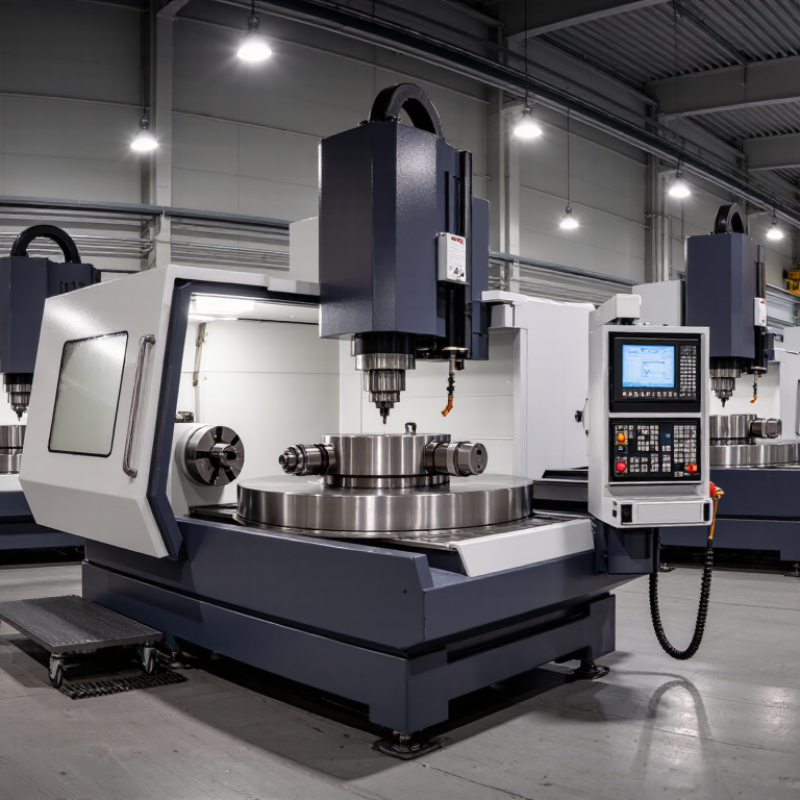
A CNC vertical turning lathe is a computer-controlled machine for rotating workpieces on a vertical spindle. Its chuck sits horizontally, while the workpiece stands upright. This layout uses gravity to improve stability, especially when machining heavy or wide components. Cutting tools move along programmed paths to perform turning, facing, boring, threading, and grooving operations. Operators usually load a digital program, secure the workpiece, and verify tool offsets before cutting.
Compared with horizontal lathes, vertical models often need less floor space for large diameters. They can also reduce deflection during heavy cutting. This makes them suitable for wheels, flanges, rings, housings, and other disk-shaped parts. Accuracy still depends on spindle condition, machine rigidity, thermal control, and operator setup. A high spindle speed does not automatically mean better results. I have seen small alignment errors create visible marks on a finished surface. That detail is easy to underestimate.
Tips: Check the maximum turning diameter, workpiece height, spindle load, chuck size, and tool capacity. Ask for repeatability data from real production conditions, not only showroom figures. Confirm whether the control system supports your programming workflow. Test chip evacuation with your material. Cast iron and stainless steel behave differently. Leave room for inspection access. A machine may look powerful, but poor access can slow every setup. Also review training, maintenance response, and spare-part availability before purchasing. Some specifications appear impressive, yet practical usability can be less convincing.
10 Best CNC Vertical Turning Lathes for Global Buyers
What Is a CNC Vertical Turning Lathe?
A CNC vertical turning lathe is a computer-controlled machine that rotates a workpiece on a horizontal table while cutting tools move vertically and radially. The following chart presents realistic, non-brand-specific market benchmarks for maximum turning diameter across common VTL size classes.
Values are representative maximum turning diameters commonly specified for compact, medium-duty, and heavy-duty CNC vertical turning configurations. Actual capacity depends on machine design, chuck size, tool system, and workpiece geometry.
Key Criteria for Evaluating CNC Vertical Turning Lathes
Choosing a CNC vertical turning lathe requires more than comparing price and maximum diameter. Global buyers should examine workpiece size, table load, spindle torque, and cutting-tool capacity. These figures must match real production demands, not occasional workshop tasks. A machine rated for a large diameter may still struggle with heavy, unbalanced components.
Accuracy deserves practical verification. Ask for positioning and repeatability data under controlled conditions. Thermal drift can change results after several hours of cutting. Request sample parts, inspection records, and a clear explanation of testing methods. A polished brochure is not proof. I have learned that coolant flow, chip removal, and operator access often affect output more than expected.
Control functions should support the team’s skill level. Simple probing, tool monitoring, and collision protection can reduce setup errors. Check the electrical system, safety guards, documentation, and training materials for your operating region. Service response also matters. Confirm spare-part availability, remote diagnostics, installation support, and technician coverage. Ask difficult questions early.
Energy use and maintenance should enter the calculation. A rigid machine with stable guides may preserve accuracy over years, but only with proper lubrication and alignment checks. Buyers should compare total ownership cost, not only purchase cost. Even experienced engineers can overlook foundation requirements or door clearance. That mistake is expensive. Supplier references from similar industries provide stronger evidence than generic testimonials.
10 Best CNC Vertical Turning Lathes for Global Buyers - Key Criteria for Evaluating CNC Vertical Turning Lathes
Comparative benchmark based on commonly available CNC vertical turning-lathe configurations and international buyer requirements
| Rank | Recommended Configuration | Best For | Maximum Turning Diameter
(mm) | Maximum Workpiece Height
(mm) | Chuck / Faceplate
(mm) | Spindle Speed
(rpm) | Main Motor
(kW) | Positioning Accuracy
(mm) | Automation Readiness
(1–5) | Heavy-Cutting Capability
(1–5) | Typical Application |
| 1 | High-Precision Two-Axis VTL | Precision-focused production | 500–800 | 500–700 | 400–630 | 1,500–3,000 | 22–45 | ±0.005–0.010 | 4 | 3 | Flanges, hydraulic components and precision rings |
| 2 | Heavy-Duty Single-Column VTL | Large, heavy workpieces | 800–1,600 | 800–1,200 | 800–1,250 | 400–1,200 | 45–90 | ±0.010–0.020 | 3 | 5 | Energy, mining, construction and industrial gear components |
| 3 | Compact Production VTL | Small-batch and repeat production | 400–630 | 350–500 | 315–500 | 2,000–4,000 | 15–30 | ±0.005–0.010 | 4 | 3 | Automotive hubs, brake discs and general machining |
| 4 | Two-Column Heavy Machining VTL | Maximum rigidity and stability | 1,600–3,200 | 1,200–2,000 | 1,600–2,500 | 100–600 | 75–160 | ±0.020–0.050 | 2 | 5 | Power-generation rotors, large bearings and pressure vessels |
| 5 | C-Axis Live-Tool VTL | Milling and turning in one setup | 630–1,000 | 600–900 | 500–800 | 800–2,500 | 30–60 | ±0.010–0.020 | 5 | 4 | Valve bodies, gear blanks and complex flanged parts |
| 6 | High-Speed Aluminum VTL | Non-ferrous metals and short cycle times | 400–800 | 350–600 | 315–630 | 2,500–6,000 | 18–37 | ±0.005–0.010 | 4 | 2 | Aluminum wheels, pulleys, housings and light-alloy parts |
| 7 | Y-Axis Multifunction VTL | Complex multi-face machining | 630–1,250 | 600–1,000 | 500–1,000 | 600–2,000 | 30–75 | ±0.010–0.020 | 5 | 4 | Aerospace discs, pump components and offset-hole parts |
| 8 | Dual-Spindle Production VTL | High-volume parallel production | 500–800 | 450–700 | 400–630 per spindle | 1,500–3,500 | 22–45 per spindle | ±0.010–0.020 | 5 | 3 | Automotive and industrial components requiring balanced throughput |
| 9 | Hydrostatic-Bearing VTL | Ultra-stable precision machining | 800–2,000 | 700–1,500 | 800–1,600 | 300–1,500 | 45–110 | ±0.005–0.015 | 3 | 4 | Bearing races, optical components and high-value precision parts |
| 10 | Large-Diameter Ring VTL | Oversized rings and thin-wall parts | 1,250–2,500 | 700–1,200 | 1,250–2,000 | 200–800 | 55–132 | ±0.015–0.030 | 3 | 5 | Wind-turbine rings, slewing bearings and large-diameter flanges |
Evaluation notes: The specifications shown are practical market ranges for comparable CNC vertical turning-lathe configurations, not guaranteed specifications for a particular machine. Actual capacity depends on spindle design, chuck type, tooling, workpiece material, thermal conditions, control system and machine options. Positioning accuracy values are commonly stated machine-tool benchmarks and should be confirmed through the supplier’s inspection report and applicable ISO 230 or equivalent test documentation.
Ten Leading CNC Vertical Turning Lathes for Global Buyers
Ten Leading CNC Vertical Turning Lathes for Global Buyers
Selecting among ten leading CNC vertical turning lathes requires more than comparing spindle speed and table diameter. In real workshops, rigidity often matters more than impressive brochure figures. A stable machine should hold tolerances during heavy interrupted cuts. Its cast structure must resist vibration when turning large steel rings. Buyers should check table load, chuck size, ram travel, and maximum workpiece height. These details affect daily production.
A practical evaluation starts with test cuts using similar material. Measure surface finish after roughing and finishing cycles. Review chip control around the chuck, especially with stainless steel or cast iron. A responsive CNC control can shorten setup time, but operators still need clear menus and reliable tool offsets. Automatic tool changers should position repeatably. Thermal compensation is valuable during long shifts. It is not magic.
Service capability can separate a suitable lathe from a costly mistake. Confirm spare-part availability, remote diagnostics, installation support, and local technician coverage before purchase. Electrical standards and safety requirements also vary by market. A machine may perform well in testing yet disappoint when training is weak. That risk deserves attention. Buyers should request documented accuracy tests, maintenance schedules, and references from comparable workshops. The best choice is not always the fastest lathe. It is the machine that matches the work envelope, operator skill, production rhythm, and expected support over many years.
Comparison of Performance, Features, and Applications
10 Best CNC Vertical Turning Lathes for Global Buyers
Choosing among the ten best CNC vertical turning lathes requires more than checking spindle speed. Real performance depends on rigidity, cutting stability, thermal control, and operator access. During shop-floor evaluations, heavy cast structures usually reduce vibration on large steel parts. High-torque spindles also maintain cutting force during interrupted operations. However, maximum speed can mislead buyers. A slower spindle may deliver better surface quality on oversized workpieces.
Features should match the application. Dual-column designs suit large flanges, rings, and energy-sector components. Compact single-column machines often fit automotive parts and general job-shop production. Look for automatic tool changers, live tooling, probing systems, and clear control interfaces. These features can reduce setup time and improve repeatability. Yet more automation increases training demands and maintenance points. That trade-off deserves honest review. No ranking is universal.
Tips: Compare usable swing, not only advertised swing. Request test cuts using your actual material and tooling. Check chip evacuation around the worktable. Ask about service response, spare-part availability, and operator training in your region. Measure power consumption during typical cycles, not idle operation. Keep records.
Application fit remains decisive. A machine for stainless-steel rings needs different torque and coolant control than one for aluminum housings. Buyers should review accuracy reports, installation conditions, and long-term workload. Small details matter, sometimes more than headline specifications.
How to Choose the Right CNC Vertical Turning Lathe
Choosing a CNC vertical turning lathe starts with the workpiece, not the catalog. Measure maximum diameter, height, weight, and chucking surface. Leave clearance for jaws, tools, and chip flow. A machine with impressive swing may still lack usable height. Confirm spindle torque at your real cutting speed, especially for cast iron, steel, or interrupted cuts. Torque matters more than a headline rpm.
Evaluate rigidity through the table, column, ram, and guideways. Heavy structural sections reduce vibration, but they do not replace correct fixturing. Request sample cuts using your material, insert geometry, and target tolerance.
Test the real cut. Check surface finish after warm-up, not only during a short demonstration. Thermal drift can change bore size by several microns. That detail is easy to miss.
Control functions should match operator skill and production needs. Look for probing, tool measurement, collision protection, remote diagnostics, and clear alarm history. Verify local power requirements, foundation loading, coolant capacity, and chip removal before delivery. Ask for documented accuracy tests and a realistic service response time. Spare parts availability affects uptime more than a low purchase price. Be skeptical of perfect payback claims. Your own cycle data may expose optimistic assumptions. A smaller machine with stable service can outperform a larger one that waits for support.






