Choosing the best Crusher Wear Parts in 2026 is not as simple as picking the hardest alloy. The right choice depends on the crusher, feed material, operating conditions, and maintenance plan. A jaw crusher handling abrasive granite faces different demands from an impact crusher processing softer stone. Small differences matter.
This guide looks at the factors that shape wear-part performance, including material composition, fit, impact resistance, and expected service life. Manganese steel is widely used in applications where impact hardening can be beneficial, while other alloys may suit different wear conditions. No material is best in every setting. A part that lasts longer on paper may still perform poorly if it does not match the machine or feed.
Real operating data can make selection more reliable. Track tonnes processed, inspection findings, downtime, and replacement frequency—not just the purchase price. Keep an eye on liner profiles and unusual wear patterns. They can reveal poor fit, uneven loading, or changing feed conditions. One caveat: supplier wear-life claims are not always measured under comparable conditions. Ask how test results were collected, and check compatibility with the crusher manufacturer’s specifications.
The recommendations ahead are practical, but they are not a substitute for site-specific assessment. Even experienced teams revise their choices when geology, throughput, or operating practices change. That is worth remembering. A careful comparison can help buyers balance service life, safety, availability, and total operating cost when selecting Crusher Wear Parts for 2026.
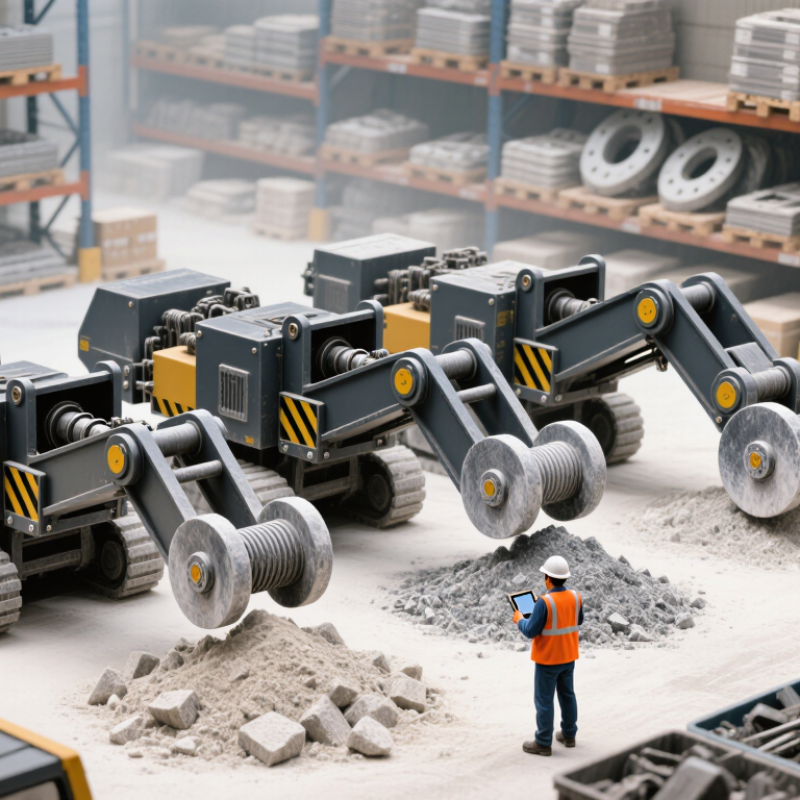
Crusher wear parts are the surfaces that take repeated contact with rock. They include jaw plates, cone mantles and concaves, blow bars, and chamber liners. Their job is not merely to resist damage. Their shape and fit guide material through the machine, influence the final particle size, and help maintain consistent output. Manganese steel is commonly used where impact is high; high-chromium iron suits some abrasive, lower-impact duties. Selection depends on the rock and crusher.
The USGS Mineral Commodity Summaries 2025 estimated U.S. crushed-stone production at about 1.5 billion metric tons in 2024. That scale means small wear changes can matter across long production runs. As liners thin, the crushing gap and chamber profile change. Operators may see coarser product, uneven wear, or rising energy use. A part can still look serviceable while its worn profile affects performance. That is easy to miss. Check wear measurements against the equipment maker’s limits, and inspect matching surfaces together.
Tips: Record wear depth at repeatable points, photograph the chamber, and compare readings over time. Replace parts based on measured wear and operating conditions, not appearance alone. A simple log helps reveal uneven loading before it becomes a costly surprise.
What Are the Best Crusher Wear Parts in 2026?
Which Materials Offer the Best Wear Resistance in 2026
There is no single wear-resistant material for every crusher. The right choice depends on feed hardness, particle shape, impact, and operating conditions. Hadfield manganese steel remains useful where repeated impact helps its surface work-harden, such as in many jaw and cone crusher liners. It can wear quickly, though, when impact is too low to trigger that hardening.
High-chromium white iron handles abrasive sliding wear well. Its hardness can extend service life in suitable applications, but its brittleness makes severe impact a concern. Martensitic alloy steel can offer a practical middle ground, combining abrasion resistance with greater impact tolerance. Heat treatment matters: two parts with similar chemistry may perform differently if their hardness and toughness are not properly balanced.
Ceramic inserts can resist abrasion in selected high-wear zones, but they may chip under sudden loads. A material’s hardness rating alone can be misleading. Track liner thickness, inspect fracture patterns, and compare tonnes processed between replacements. Feed conditions change, too. One detail operators sometimes overlook is that uneven wear can point to poor loading or a change in feed, not just an unsuitable alloy. The best selection is the one that matches the actual wear pattern—and that match may need revisiting.
What Are the Best Crusher Wear Parts in 2026?
How Crusher Type and Feed Conditions Shape Part Selection
The best wear part depends on what the crusher does and what enters it. Jaw crushers face repeated compression, so jaw plates must suit both rock hardness and feed size. Cone crushers need liners that maintain a stable crushing chamber as they wear. Impact crushers rely on blow bars that withstand repeated blows. Small details matter.
Feed conditions can change the choice quickly. Hard, abrasive rock often wears manganese steel faster; wet, clay-rich feed may pack into a chamber and disrupt crushing. Oversized chunks create uneven loading, while a wide mix of sizes can alter contact patterns. Check the actual feed gradation and moisture, not just the quarry’s rock description. A short inspection can reveal what a specification sheet misses.
Scale makes reliable selection important. The USGS Mineral Commodity Summaries 2024 reports U.S. crushed-stone production of about 1.5 billion short tons in 2023. That figure describes production, not wear-part life, but it shows why small efficiency losses matter across high-volume operations. Compare candidate parts using measured tonnes processed, wear profile, and changeout time under similar conditions. Keep a record by crusher and feed type. It may still be imperfect; quarry conditions rarely stay fixed.
Crusher wear parts should be compared by cost per processed tonne, not purchase price alone. Record each set’s service hours, tonnes crushed, replacement labor, and unplanned stoppage time. Then compare wear life under similar feed conditions: abrasive rock, oversized feed, and impact can quickly change results. A part that lasts longer may still reduce throughput or increase energy use. Longer life is not automatically better.
Operating efficiency matters. The U.S. Department of Energy’s 2007 Mining Industry Energy Bandwidth Study estimated U.S. mining energy use at roughly 1.7 quadrillion Btu annually, based on early-2000s data. The figure covers the wider mining sector, not crusher wear parts alone, but it shows why energy deserves attention. Track kilowatt-hours per tonne alongside throughput and wear. A poorly matched profile can consume energy quietly. Real site records are rarely perfect, so compare several change-outs before deciding.
Tips: Photograph the liner profile at each inspection. Log tonnes, settings, and feed changes. Check whether rising energy use coincides with worn parts, rather than assuming wear is the only cause.
Choosing crusher wear parts starts with the rock, not the machine brochure. The USGS 2025 Mineral Commodity Summaries estimates U.S. crushed-stone output at about 1.5 billion metric tons in 2024. That scale makes small wear-life gains meaningful, but national output cannot predict performance at one quarry. Check feed hardness, abrasiveness, moisture, particle size, and the required product shape.
For jaw crushers handling abrasive granite, compare manganese-steel jaw plates and track tonnes processed, not just days in service. Manganese steel can work-harden under impact, but poor feed distribution may cause uneven wear. Cone-crusher liners need to match the chamber, feed gradation, and closed-side setting; inspect for packing and localized thinning. In impact crushers, high-chrome iron may resist abrasion, yet it can be less tolerant of tramp metal. Fit matters.
Measure the details. Record operating hours, tonnes per set, downtime, and remaining liner thickness. UNEP’s Global Resources Outlook 2024 projects resource extraction could rise 60% by 2060, adding pressure to use equipment efficiently; it does not predict wear-part life. Compare supplier claims with your own trial data, and ask for material specifications and failure analysis. A tidy spreadsheet can still miss changing rock conditions. Recheck after every major change in the quarry face.
There is no single best wear-part material for every crusher. Choose based on the balance of impact, abrasion, feed characteristics, and operating conditions.
| Wear-Part Material | Typical Hardness or Material Characteristic | Best-Suited Applications | Impact Tolerance | Abrasion Resistance | Common Crusher Parts | Selection Considerations |
|---|---|---|---|---|---|---|
| Austenitic manganese steel | Often about 180–250 HB when supplied; the working surface can harden considerably under impact. Actual values vary by grade and service. | High-impact crushing of hard rock and variable feed, particularly where the material can work-harden the surface. | High | Good when sufficient impact causes work-hardening; performance can be poor in low-impact, highly abrasive conditions. | Jaw plates, cone and gyratory crusher liners, and some impact-crusher wear parts. | Consider feed size, impact level, and whether the part receives enough working impact. Check for fit and compatibility with the crusher. |
| Martensitic alloy steel | Commonly supplied in a broad range around 300–500 HB, depending on alloy, heat treatment, and component design. | Impact crushing where a combination of toughness and abrasion resistance is required, including many recycled or natural aggregates. | Moderate to high; varies with hardness and heat treatment. | Generally higher than manganese steel in low-to-moderate impact service, but depends on the alloy and operating conditions. | Impact-crusher blow bars and selected impact plates. | Higher hardness may improve wear resistance but can reduce toughness. Match the grade to feed size, impact severity, and risk of tramp material. |
| High-chromium white iron | Typically around 550–700 HB; the hard carbide structure provides high resistance to sliding abrasion. | Highly abrasive feed with relatively low or controlled impact. | Low to moderate; generally less tolerant of severe shock than manganese or tougher steel alloys. | High in suitable abrasive applications. | Selected impact-crusher blow bars, liners, and wear plates. | Avoid where severe impact, large uncrushable objects, or frequent shock loading is expected. Confirm the part is approved for the machine and duty. |
| Ceramic-insert composite | Composite construction combines ceramic inserts with a metal matrix; a single hardness value does not describe the complete part. | High-abrasion impact-crushing applications where the machine and operating conditions are suitable for composite blow bars. | Application-dependent; generally not the first choice for severe shock or frequent tramp-metal impacts. | Very high at the ceramic wear surfaces in appropriate service. | Specialized impact-crusher blow bars and selected wear plates. | Use only after checking crusher compatibility, feed characteristics, impact severity, and the composite’s recommended operating range. |
Hardness figures are indicative ranges, not guaranteed specifications. Actual wear life depends on feed size and hardness, abrasiveness, moisture, crusher settings, throughput, and maintenance practices.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru