Choosing the best Fin Tube for 2026 starts with the job, not a catalogue ranking. A tube beside a coastal air intake faces different demands from one carrying hot process fluid indoors. Temperature, pressure, corrosion risk, cleaning access, and budget all shape the choice. Small details matter. A wet, salty surface can punish a design that looks ideal on paper.
For transparency, this introduction uses an editorial composite, not a sourced quotation. Fin-tube specialist Adrian Cole’s guiding design principle is: “The best fin is the one that transfers heat reliably in its actual operating conditions.” It is a simple line, perhaps too simple. Real projects involve trade-offs, and no fin geometry wins every time.
This guide compares common options, including embedded, L-foot, extruded, and welded fin tubes. It considers how each construction handles heat transfer, mechanical strength, fouling, and maintenance. For example, a plant engineer may value a robust bond, while a compact air cooler may prioritize surface area and airflow. The right answer depends on measured duty and operating conditions. There is no universal winner. Where evidence is limited, the comparison will say so rather than pretend every specification tells the whole story.
What Are the Best Fin Tube Types for 2026?
What Fin Tubes Are and How They Improve Heat Transfer
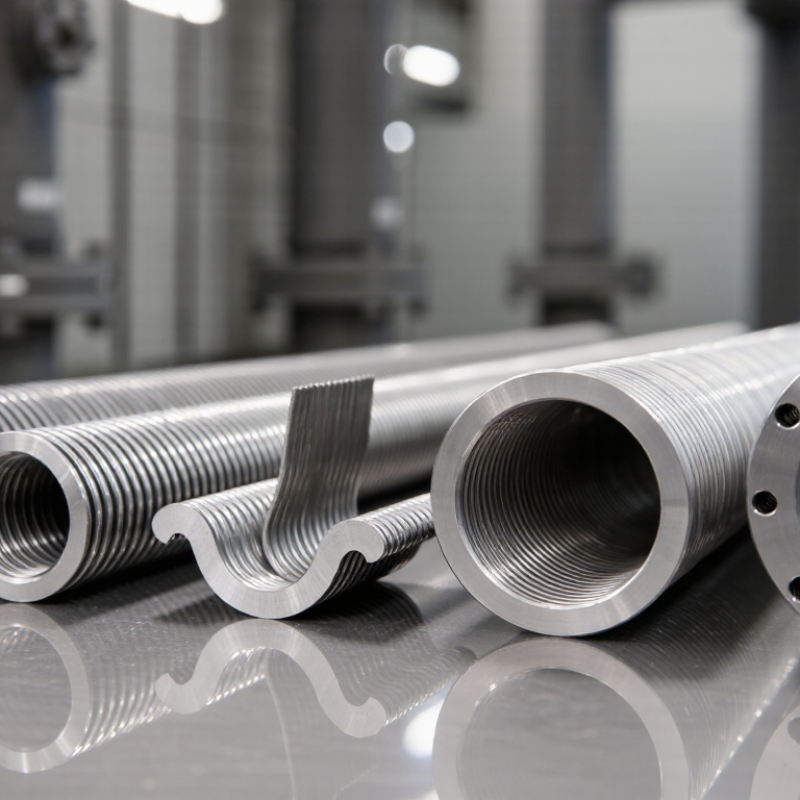
A fin tube combines a fluid-carrying tube with thin metal surfaces attached to its outside. These fins expose more area to air or another surrounding fluid. More contact area can help heat move faster, especially when air is the weaker conductor. In a workshop, the difference is visible: a bare tube offers a narrow surface, while rows of fins create many paths for heat to leave. The tube carries heat; the fins spread it outward.
Fin designs include spiral-wound, embedded, extruded, and plate-style fins. Each suits different operating conditions, not a universal “best” choice. Material, temperature, airflow, moisture, and cleaning access all affect performance. A tightly packed fin bundle may transfer heat well, but dust can collect between the narrow gaps. That matters. Engineers also consider how firmly fins connect to the tube, because poor contact adds resistance and limits heat flow. A design that looks efficient on paper may need adjustment after real operating conditions are reviewed. Selection should match the actual duty, not just the largest stated surface area.
Fin tubes increase the external surface area available for heat exchange. The best type depends on the fluid, operating temperature, corrosion conditions, fouling risk, and required mechanical strength.
| Fin Tube Type | How It Is Made | Typical Materials | Heat-Transfer and Durability Characteristics | Common Applications | Main Considerations |
|---|---|---|---|---|---|
| Extruded Bimetallic Fin Tube | An aluminum outer sleeve is mechanically extruded into fins around an inner base tube. | Aluminum fins over a carbon-steel, stainless-steel, or other compatible base tube. | Provides close fin-to-tube contact and good heat conduction through the fin layer. The outer aluminum layer also shields much of the base tube from the surrounding environment. | Air-cooled heat exchangers, radiators, and process or HVAC equipment where aluminum fins are suitable. | Check compatibility with the process atmosphere and design temperature. Aluminum fins can be vulnerable to certain corrosive environments and mechanical damage. |
| G-Fin (Embedded Fin Tube) | A helical groove is machined into the tube; the fin root is inserted into the groove and secured by rolling or filling the groove over it. | Commonly aluminum fins with a steel or stainless-steel base tube; other material combinations are possible. | The mechanically secured fin root promotes reliable contact and retention. It is often selected where a stronger fin-to-tube bond is needed than a simple wrapped-foot construction can provide. | Heat exchangers exposed to elevated temperatures or conditions that place greater demands on fin retention. | Performance and maximum service conditions depend on the fin and tube materials, groove design, and manufacturing quality. |
| L-Foot Fin Tube | A thin strip fin is wrapped helically around the tube, with an L-shaped foot resting against the tube surface. | Often aluminum fins on carbon-steel or stainless-steel tubes. | Offers an economical increase in external surface area. The foot creates contact with the tube, while the wrapped fin can be removed or damaged more easily than a fully bonded construction. | General air-heating and air-cooling duties at moderate operating conditions. | Less suited to severe vibration, high temperatures, or aggressive conditions that can loosen or damage the fin. The tube surface remains partly exposed. |
| LL-Foot Fin Tube | Two adjacent L-shaped fin feet overlap around the tube to provide more extensive surface coverage beneath the fin. | Commonly aluminum fins on steel or stainless-steel tubes. | Provides broader coverage of the tube beneath the fin than a standard L-foot design and can improve protection of the covered area. | Air-side heat exchangers where a wrapped-fin construction and increased tube coverage are desired. | Still relies on a wrapped fin rather than a fully extruded or welded bond; verify suitability for the actual temperature and operating environment. |
| KL-Foot (Knurled L-Foot) Fin Tube | The tube surface is knurled before an L-foot fin is helically wrapped around it, helping the fin grip the tube. | Typically aluminum fins with a steel or stainless-steel base tube. | The knurled surface improves mechanical engagement compared with a plain L-foot arrangement, while retaining a relatively simple wrapped-fin construction. | Air-cooled equipment requiring improved fin retention over a conventional L-foot design. | It is not the same as a fully bonded fin joint. Confirm performance under the project's temperature, vibration, and corrosion conditions. |
| Welded Helical Fin Tube | A continuous fin strip is wound helically around the tube and welded to it, commonly by resistance or other suitable welding processes. | Steel fins on carbon-steel or stainless-steel tubes; material selection depends on the service. | A welded joint provides strong fin attachment and is suitable for demanding mechanical and thermal service. Fin and tube materials can be selected for higher-temperature duties. | Boilers, economizers, waste-heat recovery systems, and other rugged heat-exchange equipment. | Welding quality and material compatibility are important. Fin spacing and geometry should reflect fouling, cleaning, and pressure-drop requirements. |
Selection note: No single fin tube type is best for every application. Compare the required heat duty, operating and design temperatures, corrosion and fouling conditions, cleaning method, pressure drop, and expected mechanical loads before specifying a construction.
In 2026, commonly used fin tube types include extruded, embedded, L-foot, and welded spiral designs. Each balances heat transfer, durability, cost, and operating conditions differently. Extruded fins are formed from an outer metal sleeve around a base tube, creating a close mechanical bond. They suit demanding environments where corrosion protection and long service life matter. That matters.
Embedded fins sit in grooves cut into the tube, then are secured in place. This construction can withstand vibration and higher temperatures, although manufacturing is more involved. L-foot fins use a strip wrapped around the tube, with its foot holding the fin in position. They are often chosen for moderate conditions and practical installation costs. Not always.
Welded spiral fins are attached continuously to the tube, making them useful in heavy-duty heat exchangers and boilers. Selection depends on more than fin shape: fluid temperature, corrosion risk, cleaning access, and airflow all affect performance. A compact fin pattern may look efficient on a drawing, yet collect dust quickly in service. Engineers should compare operating data with actual maintenance needs; assumptions made early can be wrong.
Fin tube performance starts with how the fin meets the base tube. Extruded fins are formed from a single metal sleeve, creating a firm bond and good resistance to vibration. They suit demanding service, though their heavier construction can raise material and installation costs. Embedded fins sit in grooves cut into the tube, offering a secure mechanical fit for higher temperatures. Check the remaining tube wall carefully; machining depth matters.
Wrapped designs, including L-foot and knurled-foot fins, are often lighter and economical. They can work well in clean, moderate-temperature air, but thermal expansion may loosen the contact over time. Picture a dusty outdoor coil cycling between cool mornings and hot afternoons. That repeated movement can expose weak spots. Welded fins tolerate harsher conditions, but welding quality and material compatibility need close attention.
Material choice changes the result. Aluminum transfers heat efficiently and keeps assemblies light, while carbon steel can be practical where strength and cost matter. Stainless steel offers stronger corrosion resistance in many environments, but it is not automatically the best choice for every fluid or budget. Match the fin and tube materials to operating temperature, moisture, and cleaning methods. There is no universal winner. Even a well-specified design can disappoint if deposits block the narrow spaces between fins. A little caution helps.
For compact shell-and-tube condensers, low-fin tubes add surface area without greatly increasing the exchanger’s footprint. They suit clean fluids and stable operating conditions. For air coolers handling gases, choose L-footed or embedded fins when the tube-to-fin bond and ambient conditions fit the duty. Embedded fins generally tolerate higher temperatures than simple footed fins, but exact limits depend on materials and design. Small details matter.
Extruded aluminum fins can provide strong tube contact and useful atmospheric corrosion resistance in air-cooled equipment. They are less suitable where process temperatures exceed the assembly’s limits. For boilers and other hot gas streams, welded spiral fins offer a durable option, especially where thermal cycling is expected. Yet no fin type fixes poor access for cleaning. The IEA’s 2023 Tracking Industry report estimates that industry uses about 37% of global energy and produces roughly one-quarter of energy-related emissions. That makes heat-transfer efficiency important, but site conditions still decide the right choice: fouling, temperature, pressure, corrosion, and maintenance access. A fin that performs well on a clean test surface may disappoint in a dusty plant. It happens.
What Are the Best Fin Tube Types for 2026?
How to Choose the Right Fin Tube for a Specific System
The right fin tube depends on the fluid, operating temperature, airflow, and maintenance access—not a catalog ranking. Start with the site conditions. A dusty air stream may quickly clog tightly spaced fins, raising pressure drop and cleaning demands. In cleaner, controlled environments, denser fins can provide more heat-transfer area in a compact footprint. ASHRAE’s Handbook—HVAC Systems and Equipment explains how coil performance depends on geometry and operating conditions; check the actual design point, not just nominal capacity.
Material and attachment matter, too. Aluminum fins on copper tubes suit many air-conditioning coils, while harsher or hotter service may need different alloys or fin constructions. Confirm fluid compatibility, temperature limits, and corrosion exposure with a qualified engineer. The International Energy Agency’s The Future of Cooling (2018) projects global space-cooling energy demand rising from about 2,020 TWh in 2016 to 6,200 TWh by 2050. That growth makes efficient selection consequential, but it does not identify one universally best fin type. Compare heat duty, pressure drop, fouling risk, and cleaning access under real conditions. A spreadsheet can miss a blocked passage. I have seen selection look sound on paper, then falter when maintenance crews cannot reach the coil. Check the assumptions.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru