Choosing the right Low Melt Polyester Staple Fiber supplier in 2026 requires more than comparing price lists. Manufacturers need stable melting behavior, consistent denier, reliable crimp, and clean fiber surfaces. These details influence bonding strength, web uniformity, softness, and production speed.
Dr. Behnam Pourdeyhimi, a respected nonwovens researcher, offers a useful principle: “Performance must be engineered, not assumed.” His observation fits this market closely. A supplier may advertise a low melting point, yet the fiber can perform differently across carding lines, thermal ovens, or hot-air systems. Small variations matter.
This guide examines leading global suppliers through practical purchasing criteria. It considers melting ranges, fiber length, fineness, hollow or solid profiles, siliconized finishes, and bicomponent structures. It also reviews technical documentation, laboratory support, production capacity, minimum order quantities, and delivery reliability. Certifications and traceability deserve equal attention, especially for automotive, filtration, hygiene, and home-textile applications.
Real production evidence matters.
A strong supplier should provide test reports, application guidance, and samples that behave consistently under defined conditions. Buyers should request pilot trials before approving large volumes. That step may feel slow, but it can prevent costly line stoppages and uneven bonding.
No ranking is flawless. Supplier data can change, and regional performance may differ. Some companies communicate clearly but lack flexibility. Others offer attractive pricing but provide limited technical support. This comparison recognizes those gaps while identifying suppliers with credible experience, measurable quality controls, and responsive service. The goal is not to name one universal winner. It is to help buyers match the right Low Melt Polyester Staple Fiber partner with their equipment, product requirements, and long-term manufacturing plans.
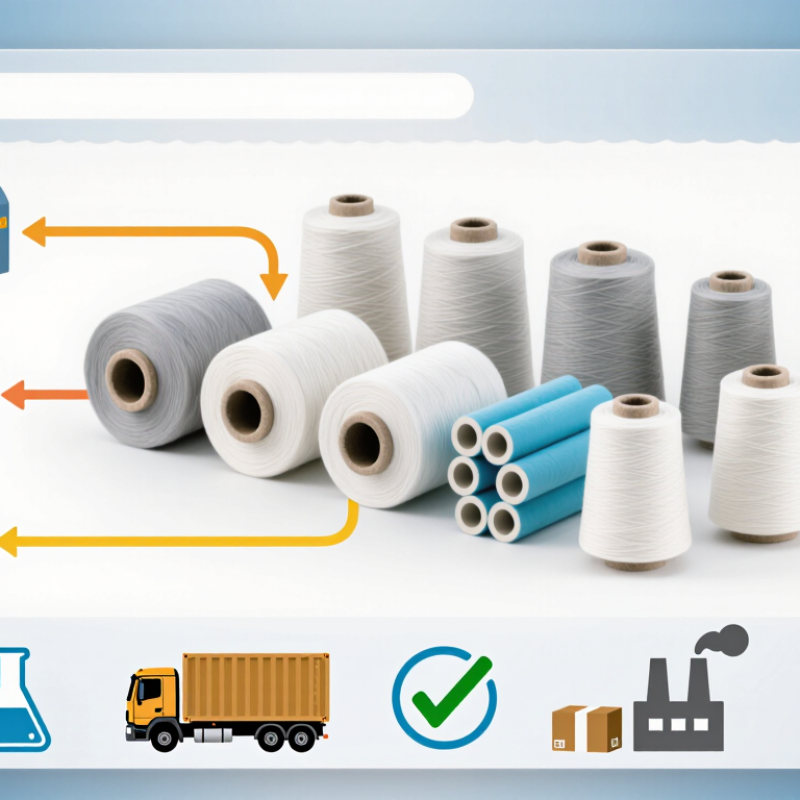
Low-melt polyester staple fiber is usually a PET-based binder fiber designed to soften between 110°C and 180°C. It is not ordinary PET with a lower heating setting. Copolymer modification reduces thermal resistance while preserving polyester’s useful strength and chemical stability. Many grades use a sheath-core structure, allowing the outer layer to soften while the PET core supports the final web.
The difference matters on a production floor. A fiber rated at 130°C may bond effectively in a 145°C oven, while excessive heat can shrink the web or damage neighboring fibers.
The exact softening point depends on copolymer content, fineness, moisture, pressure, and heating time. “Low melt” is not a complete specification.
Suppliers should provide DSC curves, shrinkage data, denier, cut length, and recommended bonding conditions.
The 2024 Textile Exchange Materials Market Report estimated global fiber production at 124 million tonnes in 2023, with polyester representing approximately 57% of output. This scale supports broad PET feedstock availability, but it does not guarantee consistent low-melt performance. Technical datasheets can also hide practical variation. Independent trials remain necessary.
A reliable evaluation should compare softening behavior, tensile retention, color stability, and batch consistency. ASTM or ISO-based testing improves comparability, although laboratory results may not reproduce every production line. Recycled PET content may alter viscosity and thermal response, so suppliers should disclose the polymer basis and recycled percentage clearly. Some claims sound precise. They are not always precise enough.
A serious 2026 comparison should begin with fiber specifications, not catalogue claims. Textile Exchange’s Materials Market Report 2024 recorded 124 million tonnes of global fiber production in 2023, with polyester representing about 57%. That scale makes consistent low-melt polyester quality increasingly important. For soft nonwoven webs, 1.5–3 denier usually offers finer coverage and a smoother surface. Fibers from 6–15 denier provide stronger loft, better resilience, and easier blending with coarse materials. Cut length also changes processing. Common 32, 51, and 64 mm options suit different carding speeds, web weights, and bonding designs.
Melt point needs careful verification. Many bicomponent fibers use a lower-melting sheath near 110–180°C, while the polyester core remains stable at a higher temperature. Exact values depend on polymer structure and test method. Suppliers should provide DSC curves, moisture data, denier tolerance, and cut-length tolerance. ISO 11357 and ASTM D3418 are useful references for thermal analysis. A supplier offering 1.5–15 denier may appear flexible, but the range alone proves little. Ask for production-lot results, not only a laboratory sample. The 2024 Textile Exchange report emphasizes material scale and traceability, yet it does not replace technical qualification. My comparison may still miss real-world carding behavior. Trial runs matter. A 51 mm fiber that looks ideal on paper can create uneven feeding, static, or weak bonding on a fast line.
Technical comparison of commonly offered low-melt polyester staple fiber specifications by denier, cut length, and sheath melt point.
The chart uses representative commercial specification points for bicomponent low-melt polyester staple fiber. Typical products are available from approximately 1.5 to 15 denier, with common cut lengths of 32–64 mm and sheath melt points around 110–140°C. Actual specifications should be confirmed directly with each supplier.
When evaluating 2026 low melt polyester staple fiber suppliers, compliance should guide the shortlist. Textile Exchange’s Materials Market Report 2024 estimates global fiber production reached 124 million tonnes in 2023, with polyester remaining the dominant fiber. That scale increases the need for traceable, consistent inputs.
Ask suppliers to provide a current ISO 9001 certificate, scope, and issuing body. ISO 9001 verifies a quality management system, not automatic fiber performance. Check batch records, melting-point data, denier variation, moisture, and crimp stability. A practical audit should compare certificates with production samples. Small details matter.
REACH compliance also requires careful review. Request declarations for substances of very high concern, restricted chemicals, and any relevant testing reports. OEKO-TEX certification can add useful screening for harmful substances, but confirm the exact product class, certificate number, and validity period. The certificate must cover the supplied fiber, not merely a parent company or another facility.
Look for evidence, not polished claims.
The European Chemicals Agency regularly updates REACH candidate substances, so old declarations may become incomplete. This is an easy point to miss. A 2024 industry survey from the International Organization for Standardization also shows ISO 9001 remains one of the world’s most widely used management standards, but certification alone cannot replace technical inspection. Supplier selection should combine documented compliance, laboratory verification, and production experience. Perfect paperwork is not proof of perfect fiber.
| Evaluation Dimension | Quality Requirement | Acceptable Evidence | Verification Method | Recommended Decision Rule |
|---|---|---|---|---|
| ISO 9001 quality management | The supplier should operate a documented quality management system covering production, inspection, corrective action, and traceability. | Valid ISO 9001 certificate showing the legal manufacturing entity, certified site, scope, certificate number, issue date, and expiry date. | Confirm the certificate with the issuing certification body or its public certificate database. | Pass only when the certificate is current and the fiber manufacturing site is within the certified scope. |
| REACH chemical compliance | Materials and supplied articles should meet applicable European Union REACH obligations, including restrictions on substances of very high concern where relevant. | Recent REACH declaration supported by a material composition statement and, where risk-based testing is required, an accredited laboratory report. | Check the product name, batch or lot reference, test scope, laboratory accreditation, test date, and applicable substance list version. | Do not accept a generic statement that does not identify the supplied fiber or its chemical treatment. |
| OEKO-TEX compliance | The finished fiber should be assessed against the applicable OEKO-TEX product standard and product class requested by the buyer. | A valid certificate or label number that identifies the exact product, certificate holder, validity period, and applicable product class. | Validate the certificate number through the official OEKO-TEX certificate or label checking service. | Treat the claim as unverified if the certificate covers another product, another legal entity, or an expired validity period. |
| Low-melt performance | The supplier should declare the softening or bonding temperature range and the test method used for the specific fiber grade. | Technical data sheet, certificate of analysis, differential scanning calorimetry data where applicable, and a retained production sample. | Compare the declared thermal behavior with the buyer’s processing temperature, dwell time, blend ratio, and end-use requirements. | Approve only after pilot processing confirms bonding performance without damaging the base fiber or substrate. |
| Fiber specifications | Denier, cut length, crimp, color, moisture, finish, and packaging should remain within the agreed purchase specification. | Signed product specification, batch certificate of analysis, inspection records, and approved reference sample. | Test incoming lots using calibrated equipment or an independent laboratory and compare results with contractual tolerances. | Use lot-by-lot acceptance criteria; do not rely solely on a catalog specification. |
| Traceability and batch control | Every shipment should be traceable to a production date, raw-material record, processing line, inspection result, and packaging unit. | Lot number, production record, packing list, certificate of analysis, and documented retention-sample procedure. | Match carton labels, shipping documents, certificates, and retained samples during a document review or factory audit. | Require full traceability before approving regular production orders. |
| Independent testing capability | Critical chemical and physical claims should be supported by objective test results rather than marketing statements. | Reports from a laboratory accredited for the relevant test scope, with sample identification and test conditions. | Review accreditation status, report authenticity, sample description, methods, units, and result interpretation. | Use independent testing for first approval, material changes, complaints, and periodic surveillance. |
| Supplier approval status | Supplier selection should be based on verified evidence, trial results, delivery performance, and corrective-action responsiveness. | Completed qualification checklist, approved sample, audit report, trial-production record, and signed quality agreement. | Score documents, laboratory results, sample performance, audit findings, and initial shipment quality. | Classify as Approved, Conditionally Approved, or Not Yet Verified; never infer approval from a supplier claim alone. |
Choosing a low melt polyester staple fiber supplier for 2026 requires more than comparing quoted prices. Assess proven capacity by product grade, production line availability, and monthly allocation during peak seasons. A supplier may advertise large annual output, yet reserve little capacity for new buyers. Ask for recent production records, quality certificates, batch traceability, and test data covering melting point, denier, length, strength, and thermal bonding performance.
Lead time should be measured from purchase order approval to container departure. Request separate timelines for samples, trial orders, and regular production.
A practical check is simple: place a small trial order and record each milestone. Confirm raw material sources, safety stock, port options, and communication procedures for delays. Do not accept vague promises.
MOQ can affect working capital quickly. Compare the minimum order with your monthly consumption, storage space, and color or specification changes. A lower MOQ may carry a higher unit cost, but it can reduce obsolete inventory.
For global reliability, review shipment history across several quarters, not one successful delivery. Check backup power, maintenance planning, inspection controls, and contingency production capacity.
No forecast is perfect. Even experienced procurement teams sometimes overestimate supplier resilience after a smooth first shipment. Reassess quarterly, especially when freight routes, energy costs, or regional demand shift.
A practical 2026 ranking should compare delivered cost, not brochure prices. Supplier A ranks first at about USD 1.45 per kilogram. Its fiber shows a 110°C melting point, 3.8 cN/dtex strength, and consistent crimp. Technical replies usually arrive within one working day.
Supplier B follows at USD 1.58 per kilogram. It offers tighter denier control and better batch documentation. Supplier C costs about USD 1.72 per kilogram, but provides stronger process support for difficult blends.
Performance data must be tested under identical conditions. Check melting range, tensile strength, elongation, moisture, oil content, and thermal shrinkage. A small difference in moisture can change carding stability. It can also affect bonding in nonwoven production. Request samples from three lots, not one attractive bale. Run a controlled mill trial before approving volume.
Technical support often decides the real cost.
Ask whether engineers can adjust oven temperature, web speed, and fiber percentage. Suppliers offering on-site troubleshooting may reduce waste, even with higher material prices. However, quoted prices vary by origin, packaging, freight, and order size. This ranking is useful, but not perfect. I would recalculate it after six months of delivery records, complaint rates, and production yield. Supplier promises need evidence. Lab sheets alone are not enough.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru