Choosing the right Mcb Riveting Machine can determine whether a production line runs smoothly or repeatedly stops for adjustments. Global buyers must examine more than price, catalog photographs, and claimed cycle speed. Rivet diameter, cabinet size, feeding accuracy, stroke control, and compatibility with miniature circuit breaker components all deserve close attention.
Manufacturing consultant Dr. Robert H. Todd states, “Process stability matters more than impressive machine speed.” That principle guides this review of the 10 Best MCB Riveting Machines for Global Buyers. A dependable machine should place each rivet consistently, even after thousands of cycles. Operators should also inspect the pressure regulator, sensor response, die design, and emergency-stop access. Small details matter. A loose feeder can create uneven heads, rejected assemblies, and costly downtime.
This guide compares practical performance, not marketing language alone. It considers automatic feeding, pneumatic or hydraulic operation, changeover time, noise, maintenance access, and after-sales support. International buyers should also confirm voltage requirements, documentation quality, spare-parts availability, and local service capability. These points are easy to overlook during a factory visit.
No machine is perfect. Some models offer excellent speed but limited flexibility. Others provide accurate riveting but require slower manual loading. That trade-off deserves honest reflection. Our recommendations are intended to help manufacturers match equipment with actual production volume, workforce skills, and quality targets. Before purchase, request sample riveting tests using your own breaker components. A polished demonstration may not represent daily factory conditions.
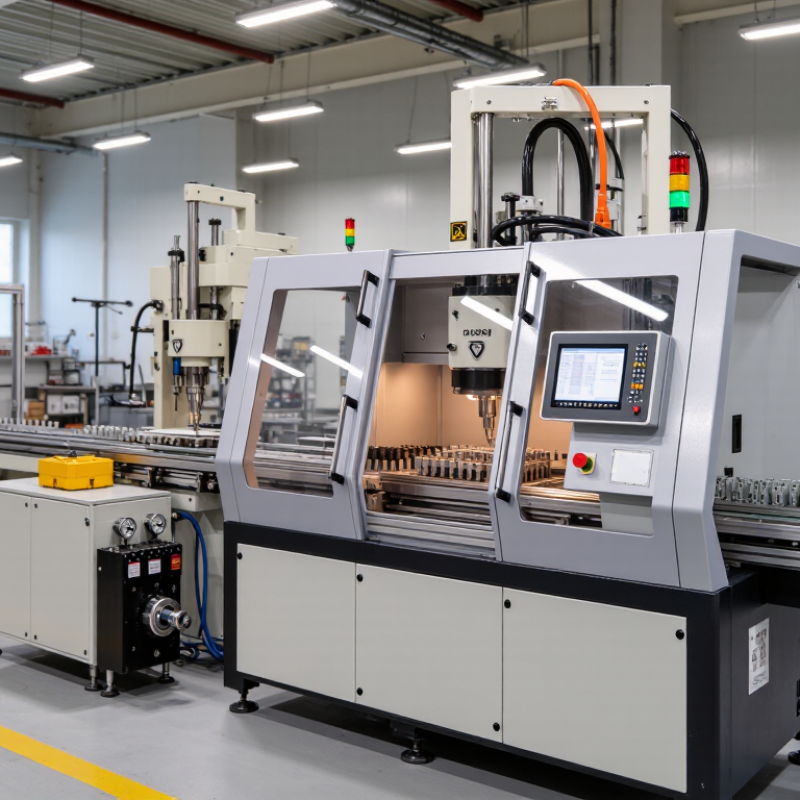
An MCB riveting machine assembles miniature circuit breaker parts with controlled pressure and repeatable alignment. MCBs protect low-voltage circuits from overloads and short circuits. Their internal parts require stable mechanical connections. A loose rivet can affect movement, contact pressure, or final inspection results.
The process usually begins with a fixture holding the breaker shell or metal component. A feeder places rivets into a guided position. The machine then lowers a punch and forms the rivet head against a support surface. Pneumatic, hydraulic, or servo-driven systems can provide the force. Sensors may check part presence, punch travel, and completed riveting height. Some machines also track production data for each cycle.
In practical factory work, tooling accuracy matters as much as machine speed. A strong frame cannot correct a poorly designed fixture. Operators should verify rivet height, joint tightness, and component movement during setup. Pull tests, visual checks, and electrical continuity tests help reveal hidden defects. Trip calibration still needs separate testing, because riveting alone does not confirm the breaker’s protective performance. Machine settings may drift after long production runs. That is easy to underestimate. Global buyers should compare compatible MCB sizes, feeding methods, force control, maintenance access, and available technical support before choosing among the ten best machines. Erotiske
MCB riveting machines join miniature circuit breaker components by inserting rivets and applying controlled force through a punch-and-die system. The indicative throughput benchmarks above are based on representative cycle times of approximately 30 seconds for manual bench riveting, 10 seconds for a single-station pneumatic machine, and 3 seconds for a multi-station automatic line. Actual output depends on rivet size, product design, feeding method, operator loading, and quality inspection requirements.
Selecting among the 10 best MCB riveting machines requires more than comparing purchase prices. The critical question is whether each machine maintains stable rivet quality across long production runs. Check riveting force, stroke control, spindle alignment, and cycle consistency. A reliable system should produce clean joints without cracked housings or loose terminals.
Ask suppliers for measured sample data, not general promises. Review force-displacement curves, reject rates, cycle times, and noise levels from realistic trials. Test your own MCB components, including different terminal thicknesses and material tolerances. Tooling should support quick changes, precise adjustment, and simple cleaning. Small errors matter.
Automation features deserve close attention. Sensors should detect missing parts, incorrect positioning, and incomplete riveting before products leave the line. Clear alarms help operators respond without guessing. Examine guarding, emergency stops, maintenance access, and electrical documentation during an on-site inspection. Compliance requirements vary by market, so technical files must be complete and traceable.
A strong evaluation also includes spare-part availability, training, remote support, and calibration procedures. Ask how quickly worn tooling can be replaced. Do not rely only on a polished demonstration. No scorecard is perfect. Real factory conditions may expose vibration, dust, or feeding problems that trials miss. Build acceptance criteria around documented results, then allow room for practical operator feedback.
Comparing the 10 best MCB riveting machines requires more than checking speed. I examine rivet consistency, frame rigidity, tooling access, noise, and operator safety. The ten options include pneumatic bench models, servo-driven units, rotary systems, four-head machines, modular lines, compact machines, high-speed models, vision-assisted equipment, semi-automatic units, and custom configurations. Pneumatic models usually cost less and suit stable, medium-volume work. Servo systems offer finer force control, especially for delicate components. Rotary designs reduce handling time, but their setup can be less forgiving.
In factory evaluations, I inspect rivet height across repeated samples. A practical target is stable output within a narrow tolerance. Four-head machines improve productivity, while compact units save floor space. Vision assistance can detect misalignment before rejection rates rise. However, lighting and software calibration need regular attention. That weakness is easy to underestimate. Modular machines adapt well to changing product sizes, though extra tooling increases maintenance demands. Semi-automatic equipment remains attractive for smaller plants because operators can correct feeding errors quickly.
Global buyers should compare electrical standards, spare-part availability, training support, and documentation quality. A machine with impressive cycle speed may perform poorly with inconsistent terminals. I also review emergency access, guarding, air consumption, and changeover time. My comparison favors balanced performance over headline numbers. Still, one judgment remains subjective: some operators prefer simpler controls, while others expect data tracking. A slightly slower machine can be the wiser purchase when local technicians can service it confidently.
| Rank | Machine Configuration | Recommended MCB Production Range | Compatible Rivet Diameter | Typical Setting Force | Automation Level | Typical Output | Power Requirement | Compressed Air | Approx. Footprint (L × W × H) | Approx. Net Mass | Best Suited For |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Servo-Electric Indexing Riveting Cell High precision | High-volume MCB assembly with repeatable contact and terminal riveting | 2.0–4.5 mm | 2–8 kN | Automatic feeding, indexing, riveting and part transfer | 25–45 units/min | 3-phase, 380–415 V, 50/60 Hz; 2–5 kW | 0.5–0.7 MPa; 150–300 L/min | 1,800 × 1,200 × 2,000 mm | 900–1,400 kg | Export-oriented factories requiring high repeatability and production traceability |
| 2 | Pneumatic Rotary-Table Riveting Machine Balanced output | Medium- to high-volume assembly of standard single-pole and multi-pole MCBs | 2.0–4.0 mm | 1.5–6 kN | Automatic rotary indexing with manual loading | 18–35 units/min | 3-phase, 380–415 V, 50/60 Hz; 1–3 kW | 0.5–0.7 MPa; 200–400 L/min | 1,500 × 1,000 × 1,850 mm | 650–1,000 kg | Manufacturers seeking a practical balance between investment, speed and flexibility |
| 3 | Servo-Pneumatic Two-Station Riveter Flexible | Mixed-model MCB production with two riveting operations in one work cycle | 1.8–4.5 mm | 1–7 kN | Automatic riveting; manual or bowl-fed component loading | 15–30 units/min | Single-phase or 3-phase, 220–415 V; 1.5–4 kW | 0.5–0.7 MPa; 120–250 L/min | 1,200 × 850 × 1,750 mm | 450–750 kg | Plants that need quick tooling changes for several MCB frame sizes |
| 4 | Automatic Bowl-Feed Contact Riveting Line High throughput | Continuous production of contact systems and current-carrying MCB assemblies | 1.5–3.5 mm | 1–5 kN | Automatic orientation, feeding, riveting and reject separation | 30–60 units/min | 3-phase, 380–415 V, 50/60 Hz; 3–7 kW | 0.5–0.7 MPa; 250–500 L/min | 2,200 × 1,400 × 2,100 mm | 1,100–1,800 kg | Large production lines where labor reduction and stable feeding are priorities |
| 5 | Programmable Electric Benchtop Riveter Low maintenance | Low- and medium-volume MCB assembly, pilot production and engineering trials | 1.5–4.0 mm | 0.8–5 kN | Operator-loaded with programmable force and stroke control | 8–20 units/min | Single-phase, 220–240 V, 50/60 Hz; 0.8–2 kW | Not required | 700 × 500 × 850 mm | 80–180 kg | Smaller factories and laboratories that need clean, quiet and repeatable operation |
| 6 | Pneumatic C-Frame MCB Riveting Press Cost effective | Manual assembly of terminals, arc-chute parts and internal MCB components | 2.0–5.0 mm | 1–4 kN | Manual loading with foot-pedal or two-hand control | 6–15 units/min | Single-phase, 220–240 V, 50/60 Hz; 0.2–0.8 kW | 0.5–0.7 MPa; 80–180 L/min | 600 × 450 × 1,250 mm | 60–130 kg | Cost-sensitive buyers, maintenance departments and small production batches |
| 7 | Hydraulic Precision Riveting Press High force | Heavy-duty riveting of thicker terminals and assemblies requiring elevated forming force | 3.0–6.0 mm | 5–20 kN | Operator-loaded with programmable pressure and dwell time | 5–12 units/min | 3-phase, 380–415 V, 50/60 Hz; 2–6 kW | Not required | 1,000 × 700 × 1,600 mm | 350–650 kg | Applications involving larger rivets, thicker copper parts or demanding forming loads |
| 8 | Vision-Inspected Riveting Workstation Quality focused | MCB assembly requiring rivet presence, position and head-form inspection | 1.5–4.0 mm | 1–6 kN | Semi-automatic riveting with camera inspection and automatic reject output | 10–25 units/min | Single-phase or 3-phase, 220–415 V; 1.5–4 kW | 0.5–0.7 MPa; 120–250 L/min | 1,300 × 900 × 1,900 mm | 500–850 kg | Global suppliers needing documented quality checks and reduced assembly defects |
| 9 | Compact Pneumatic Indexing Bench Cell Space saving | Small-footprint production of standard MCB components and subassemblies | 1.5–3.5 mm | 0.8–4 kN | Manual loading with automatic indexing and riveting | 12–24 units/min | Single-phase, 220–240 V, 50/60 Hz; 0.5–1.5 kW | 0.5–0.7 MPa; 100–220 L/min | 950 × 650 × 1,450 mm | 180–350 kg | Workshops and contract manufacturers with limited floor space |
| 10 | Modular MCB Assembly and Riveting Line Scalable | High-volume multi-pole MCB production with expandable assembly stations | 1.5–5.0 mm | 1–8 kN | Integrated feeding, assembly, riveting, testing and palletizing modules | 20–50 units/min | 3-phase, 380–415 V, 50/60 Hz; 5–15 kW | 0.5–0.7 MPa; 300–700 L/min | 3,000–6,000 × 1,500–2,200 × 2,100 mm | 1,800–3,500 kg | Established manufacturers planning phased automation and future capacity expansion |
Note: The specifications above represent typical ranges for commercially available MCB riveting equipment. Actual force, cycle rate, utility consumption, tooling and footprint vary according to MCB design, rivet material, feeding method and required inspection functions. Buyers should confirm the final configuration with the equipment supplier before purchase.
MCB riveting machines vary by production volume and assembly complexity. Pneumatic models suit stable, medium-speed lines. Servo-driven rotary machines offer tighter force control and better repeatability. Multi-station systems can rivet terminals, moving contacts, and trip-mechanism parts in one indexed cycle. According to the IEA’s Electricity 2024 report, global electricity demand may grow 3.4% annually through 2026. Its Renewables 2024 report also forecasts about 5,500 GW of renewable capacity additions from 2024 to 2030. These trends increase demand for dependable low-voltage protection equipment and consistent MCB assembly.
A capable machine should control riveting force, stroke, alignment, and feeding speed. Force-displacement monitoring helps detect loose joints or crushed components. Vision inspection can check rivet presence, head shape, and terminal position. Automatic reject units prevent defective parts from entering final testing. For production teams, traceability matters. Record the tool setting, batch number, cycle time, and failure code. IEC 60898-1 provides a useful technical reference for household and similar circuit breakers. Still, compliance cannot repair poor fixture design. A slight alignment error may change contact pressure.
Tips: Match the machine to rivet material, diameter, and daily output. Test real MCB samples before purchase. Ask for repeatability data, not only maximum speed. Leave space for maintenance access. A fast machine with difficult servicing becomes expensive. I would also review noise, compressed-air use, and spare-tool availability. These details seem minor, but factory experience often proves otherwise.
Selecting an MCB riveting machine starts with the product, not the catalog photograph. Check rivet diameter, material, stroke length, closing force, and cycle speed. Ask the supplier for tested samples using your actual components. A clean rivet head should form without cracks, loose joints, or damaged housings. Confirm compatibility with your assembly line, including electrical controls, air pressure, feeding systems, and available floor space. For global purchasing, request manuals, spare-parts lists, inspection records, and clear shipping terms. Compliance documents also matter.
Tips: Compare total ownership cost, not only the machine price. Review tooling costs, installation support, training, energy use, and expected maintenance intervals. A remote video test can reveal feeding problems before shipment. However, it cannot replace a physical sample inspection. That detail is often underestimated.
After installation, record force, stroke, vibration, and output quality during normal production. Operators should inspect rivet alignment at set intervals. Keep the feeder clean and lubricate approved moving parts according to the service guide.
Replace worn punches before they mark plastic housings or create inconsistent joints. Store critical tooling in labeled containers. Small errors grow quickly. No machine is perfect, and a cheaper model may become expensive when changeovers are frequent. Review performance after several weeks, not just during commissioning. This reflection helps buyers select equipment based on real production conditions.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru