What Is the Best Shrink Fit Tool Holder from China?
Choosing the best Shrink Fit Tool Holder from China requires more than comparing prices or polished product images. It demands practical judgment, verified specifications, and evidence from real machining environments. A reliable holder should grip the cutting tool evenly, maintain low runout, resist thermal fatigue, and support stable performance at high spindle speeds.
Andreas Haimer, a recognized tooling specialist and leader in precision toolholding, has stated, “The toolholder is the connection between the machine tool and the cutting tool.” That connection matters. A holder with 3-micron runout may produce cleaner walls, longer tool life, and fewer rejected parts. In contrast, poor heating control, inconsistent balancing, or inaccurate bore dimensions can quickly appear as vibration, chatter, and uneven tool marks.
China offers many capable manufacturers, but quality is not uniform. Some suppliers provide detailed inspection reports, balancing data, material certificates, and repeatable heating recommendations. Others provide attractive claims without enough testing. That gap deserves attention. A factory visit, sample trial, or independent measurement may reveal more than a catalog ever can.
This guide examines how to identify a dependable Shrink Fit Tool Holder from China. It considers steel quality, manufacturing precision, cooling design, compatibility, service support, and total operating cost. The best choice may not be the cheapest one. It may be the holder that stays accurate after months of daily cutting. Even then, no selection is perfect. Machining conditions, tool geometry, and operator habits can change the result. That is why careful testing remains essential.
How Shrink Fit Tool Holders Work
What Is the Best Shrink Fit Tool Holder from China?
How Shrink Fit Tool Holders Work
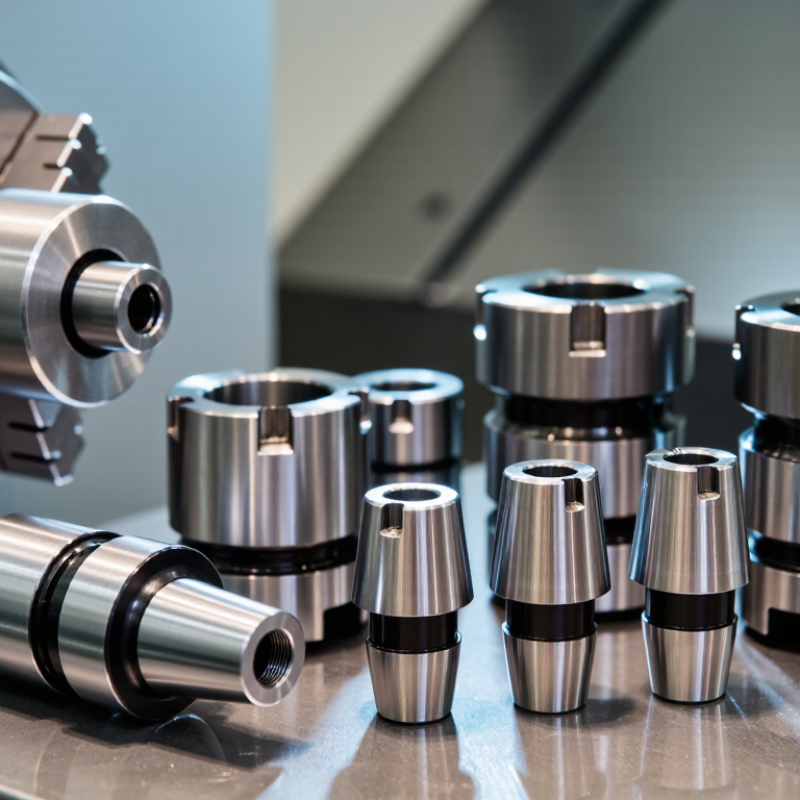
A shrink fit tool holder grips cutting tools through controlled thermal expansion. A heating unit enlarges the holder bore by a few microns. The operator inserts the shank quickly. During cooling, the bore contracts evenly around the tool. This creates strong 360-degree contact without collets, screws, or moving jaws. The result is usually better balance and lower runout. Many precision holders are specified at approximately 3 microns of runout, measured at 3×D. Actual performance depends on holder quality, heating control, tool shank accuracy, and cleaning.
The mechanism suits high-speed milling because it reduces protruding parts and supports stable rotation. The 2024 MarketsandMarkets CNC machine market report projects strong growth through 2029, reflecting wider demand for accurate automated machining. However, market growth does not prove every holder performs equally. Taper geometry, material hardness, cooling channels, and inspection records matter more than price alone. ISO 26623-1 is useful when checking polygonal taper interfaces. I would also question claims about “perfect” concentricity. Heat cycling and careless insertion can damage repeatability.
Tips: Clean the bore and shank before every setup. Use the recommended heating profile. Never force a cold tool into a hot holder. Check runout at the actual cutting length. Ask Chinese suppliers for balancing grades, inspection data, material certificates, and cycle-life testing. A trial cut reveals more than a catalog number.
How Shrink Fit Tool Holders Work: Thermal Bore Expansion
Heating the steel holder expands its bore so the cutting tool can be inserted. As the holder cools, the bore contracts and produces a uniform 360° clamping force. The values below are calculated for a 10 mm bore using steel’s typical thermal expansion coefficient of 11 × 10−6/°C, with 20°C as the reference temperature.
Materials and Designs Used in Chinese Shrink Fit Holders
What Is the Best Shrink Fit Tool Holder from China?
Chinese shrink fit holders commonly use alloy tool steel, such as 42CrMo or hardened high-carbon steel. The material must resist repeated heating, clamping stress, and cutting vibration. A dense, heat-treated body usually provides better dimensional stability. However, hardness alone does not guarantee performance.
Design details often matter more than appearance. A uniform wall thickness helps the holder expand evenly during heating. A short, accurately ground bore improves tool contact and reduces runout. Some designs include coolant passages, balanced geometry, or extended noses for deep cavities. These features should match the machine spindle and cutting application. A bright surface can look impressive. It proves very little.
In practical shop checks, measure runout near the tool tip after several heating cycles. Check whether the bore returns consistently after cooling. Inspect the heating zone for discoloration, cracks, or uneven wear. The holder should grip firmly without excessive heating time. Tool steel quality, heat treatment, grinding accuracy, and inspection records deserve equal attention. I would not choose solely by a catalog tolerance. Real cutting results may expose small errors. Even careful designs can fail when cleaning is poor, the tool shank is inconsistent, or the heating unit is unsuitable. Verify those details before regular production use.
How to Match a Holder with Your Machining Needs
The best shrink fit tool holder from China is not the same for every machining job. Matching the holder to your process matters more than choosing the lowest price. Start with the tool diameter, spindle interface, cutting speed, and required projection length.
For high-speed finishing, choose a holder with verified balance and low runout at the gauge line. A measured runout below 0.003 mm can support stable cutting, but the result depends on the tool, machine, and measurement method. Short reach helps. Deep cavities need extra length, although excessive projection can reduce rigidity and increase vibration. For hard materials, a strong thermal grip and accurate bore are important. For aluminum, chip evacuation and coolant access may deserve more attention.
Check the holder material, heat treatment, surface finish, and thermal expansion range. Ask for inspection records, balancing data, and sample measurements from the actual production lot. A reliable supplier should explain heating temperature, heating time, and cooling requirements clearly. I have seen buyers select a holder only by outside appearance. That is a costly mistake. However, specifications alone are not enough. Tool fit can change after repeated heating cycles, and some machines reveal vibration only under real cutting loads. Test the holder with your actual tool, workpiece, and cutting conditions before ordering in volume. A small trial may expose taper errors, unstable grip, or unexpected tool pullout.
How to Verify Supplier Quality and Compatibility
The best shrink fit tool holder is not chosen by price or polished photographs. It is verified through measurable quality and reliable supplier communication. In production trials, I inspect the holder’s material certificate, hardness data, and heat-treatment records. Ask for inspection reports covering bore size, taper accuracy, flange dimensions, and surface finish. Paperwork matters. However, a certificate alone does not prove consistent production quality.
Compatibility must be measured carefully. Confirm the machine spindle interface, tool diameter, heating system, coolant delivery, and approved operating speed. Match the exact interface, such as HSK or BT, with the applicable dimensional standard. Request detailed drawings before ordering samples. Measure bore tolerance and radial runout at the gauge line. Then repeat the measurement after several heating and cooling cycles. A holder can look perfect and still grip unevenly. Use calibrated instruments, not visual judgment.
Supplier reliability appears in small details. Ask whether each batch receives final inspection and traceable marking. Request a sample inspection report with actual values, not only tolerance ranges. I also prefer suppliers who explain rejected parts and corrective actions clearly. My checklist is not flawless. Batch variation can appear after a successful sample. A controlled trial with your cutters, spindle, and heating equipment reveals more. Record tool-change time, runout, clamping consistency, and holder temperature during testing. Small records often expose large problems.