Choosing the right Belt Annealing Furnace begins with process reality, not attractive catalog language. A reliable manufacturer should understand your alloy, strip thickness, line speed, and required surface condition. Stainless steel, copper, and nickel products may need different heating profiles and protective atmospheres. Small temperature variations can change hardness, color, and ductility.
Dr. George E. Totten, a recognized heat-treatment expert, said, “Without measured control, heat treatment becomes an assumption.” This principle remains highly relevant when evaluating a Belt Annealing Furnace for sale. Buyers should request temperature-uniformity records, atmosphere-control details, belt material information, and evidence from comparable production lines. They should also examine burner or electric-heating design, cooling-zone stability, exhaust handling, and maintenance access. Practical details matter. A clean inspection window helps operators see belt tracking and product movement. A responsive PLC helps them correct abnormal trends before quality problems spread.
A serious manufacturer does more than supply a heated chamber. It studies loading patterns, production targets, energy use, and future expansion. Factory testing can reveal problems that drawings hide. Still, no furnace is perfect. Belt wear, sensor drift, and uneven loading may appear after installation. That uncertainty deserves attention. Clear service terms, spare-parts planning, and operator training can reduce avoidable downtime.
This guide explores how to compare Belt Annealing Furnace manufacturers, verify technical claims, and select equipment that supports stable production. The best choice is not always the cheapest. It is the furnace that delivers measurable performance, practical maintenance, and dependable results over time.
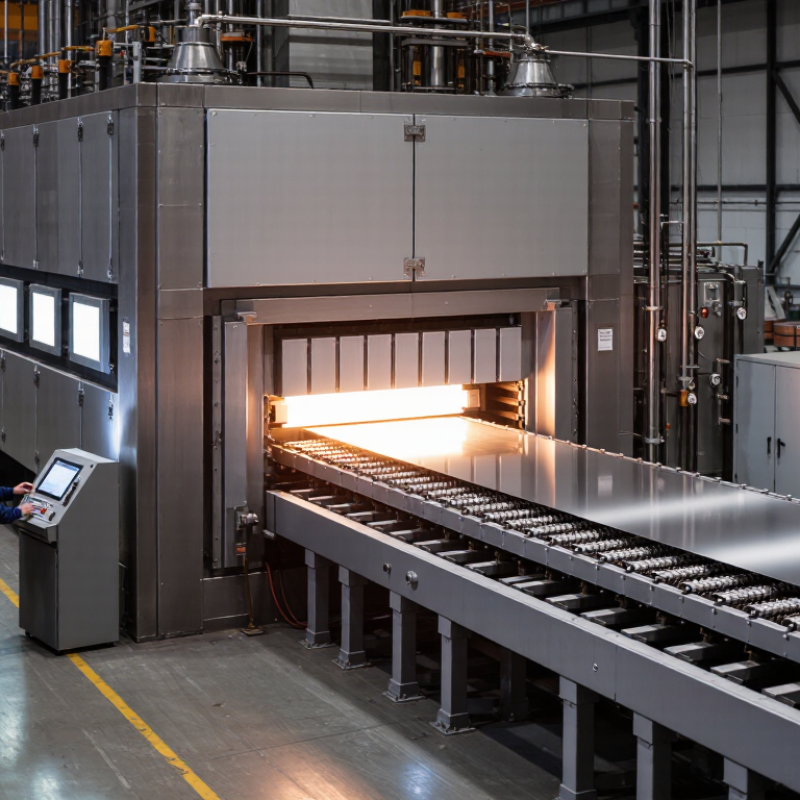
What Is a Belt Annealing Furnace?
A belt annealing furnace is a continuous heat-treatment system. It moves metal parts through heating, soaking, and cooling zones on a conveyor belt. The process reduces hardness and internal stress after forming, drawing, stamping, or sintering. Controlled temperature and atmosphere help prevent oxidation, discoloration, and unwanted surface scale.
Unlike batch furnaces, belt systems support steady production with less manual loading. They commonly process wire, fasteners, stainless-steel components, copper parts, and powder-metal products. The World Steel Association reported global crude steel production of about 1.89 billion tonnes in 2023. That scale highlights the need for repeatable thermal processing. The U.S. Department of Energy also identifies iron and steel among the most energy-intensive industrial sectors. Furnace efficiency therefore affects both operating cost and production reliability.
Tips: Check the useful belt width, temperature uniformity, atmosphere control, and cooling capacity. Ask for measured data, not only catalog claims. A furnace rated at 1,000°C may still fail to hold tight uniformity across a wide belt. In practice, the perfect temperature profile is uncommon. Product spacing, belt loading, and door openings can change results. Review trial data with your actual material and line speed before purchasing. Consider maintenance access, spare heating elements, and gas-monitoring systems. These details often decide whether a “low-cost” furnace remains economical.

A belt annealing furnace is a continuous heat-treatment system that transports parts through controlled heating, soaking, and cooling zones on a moving belt. The following chart shows a representative temperature profile for stainless-steel components processed in a continuous belt annealing line. Actual settings vary by alloy, part geometry, belt speed, and required mechanical properties.
Process interpretation: Components are gradually heated to reduce thermal shock, held near the alloy-specific annealing temperature, and then cooled in a controlled manner to improve ductility and relieve internal stress.
A belt annealing furnace continuously heats metal strip while it travels through a sealed, controlled atmosphere. The strip first unwinds from a coil. Rollers maintain alignment and tension. Heating zones then raise the material to its specified annealing temperature. For many stainless-steel grades, production lines commonly operate near 1,000–1,100°C, depending on chemistry and thickness.
The atmosphere matters as much as heat. Nitrogen or nitrogen-hydrogen mixtures reduce oxidation and help preserve a clean surface. Sensors monitor temperature, belt speed, oxygen level, and cooling conditions. Rapid cooling can restore the required structure, while excessive tension may create distortion. Small changes become visible at the exit: dull edges, waviness, or uneven color.
Industrial efficiency deserves attention. The International Energy Agency reports that steel production creates roughly 7%–9% of global energy-related carbon dioxide emissions. Better insulation, heat recovery, and accurate zone control can reduce furnace losses. World Steel Association data recorded about 1.89 billion tonnes of crude steel production in 2023, showing why continuous processing remains important. Still, one recipe cannot fit every alloy. Operators should verify hardness, surface quality, and dimensional stability through testing, rather than trusting display values alone. That practical caution is often overlooked.
China-made belt annealing furnaces are designed for continuous heat treatment of wire, strips, small components, and formed parts. In production trials, the mesh belt supports steady movement through controlled heating zones. This reduces handling between batches. It also improves process consistency.
A key feature is multi-zone temperature control. Independent sensors and PID controllers help maintain accurate heating across the furnace length. Many systems operate with protective gas to reduce oxidation and surface discoloration. Adjustable belt speed allows operators to match heating time with material thickness. Uniform airflow matters too. Poor circulation can create uneven hardness or color.
Cooling sections are equally important. Controlled cooling helps protect the required metallurgical structure. A reliable furnace should include emergency stops, over-temperature protection, gas monitoring, and insulated access doors. These details support safer operation and lower heat loss. Energy-saving insulation can reduce operating costs, although actual savings depend on loading and maintenance.
For buyers comparing a belt annealing furnace for sale, inspect the documentation, calibration records, spare parts access, and after-sales technical support. Ask for temperature uniformity data under real loading conditions. Empty-chamber results can be misleading. No furnace is perfect. Belt wear, sensor drift, and changing material loads still require attention. Regular cleaning and calibration remain necessary, even with advanced automation. A well-built China-made furnace should offer practical customization, clear controls, and stable performance rather than impressive specifications alone.
China Best Belt Annealing Furnace Manufacturer for Sale
Evaluating a belt annealing furnace manufacturer requires more than comparing prices. The International Energy Agency reports that industry consumes about 37% of global final energy. Therefore, heating efficiency should be a purchasing priority. Ask for measured energy consumption, temperature uniformity, belt life, and production capacity under real workloads. A reliable manufacturer should provide thermal mapping records, material certificates, control-system documentation, and references from comparable applications.
During a factory audit, inspect the furnace frame, atmosphere-sealing points, cooling zones, and belt tracking system. Request a witnessed factory acceptance test using your actual product dimensions. Check whether the manufacturer controls furnace design, electrical integration, and software support internally. The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies process heating as a major industrial emissions challenge. This makes combustion control, insulation quality, heat recovery, and standby energy data commercially important. A perfect brochure is not proof. I would still question unclear testing methods.
Tips: Compare guaranteed values with independently recorded results. Ask how often calibration occurs. Review spare-part availability and remote troubleshooting. Confirm operator training before shipment. Examine failure records, not only success stories. Also, evaluate after-sales response times across different time zones. The World Steel Association reported global crude steel production above 1.8 billion tonnes in recent years, showing the scale of continuous thermal processing. However, large output figures do not guarantee suitable engineering. Your strip thickness, alloy, line speed, atmosphere, and surface requirements must guide the final decision.
| Evaluation Dimension | What to Evaluate | Recommended Evidence | Practical Acceptance Guidance |
|---|---|---|---|
| Application Suitability | Whether the furnace is designed for the specific alloy, strip thickness, width, production rate, annealing atmosphere, and required metallurgical condition. | A written process specification, heat-treatment recipe, material list, and reference production samples. | The manufacturer should clearly identify operating limits rather than offering a generic furnace for every material. |
| Temperature Range | The controlled operating range and the maximum design temperature of the heating, soaking, and cooling zones. | Technical drawings, heater ratings, control-zone layout, and documented temperature test results. | The specified range should cover the actual annealing recipe with adequate control margin. |
| Temperature Uniformity | Temperature consistency across the working width and along the belt travel direction. | A temperature uniformity survey using calibrated instruments and a defined acceptance tolerance. | The tolerance must be agreed according to the product specification and any applicable standard, such as AMS2750 where relevant. |
| Atmosphere Control | The furnace’s ability to control oxygen level, dew point, gas flow, pressure, and atmosphere composition. | Gas-flow diagrams, sensor specifications, alarm settings, leak-test records, and atmosphere test data. | The system should maintain the atmosphere required to limit oxidation, discoloration, decarburization, or other surface defects. |
| Belt Design and Life | Belt material, belt width, load capacity, tracking system, drive arrangement, and resistance to thermal cycling. | Belt drawings, material certificates, load calculations, spare-parts list, and belt replacement procedure. | The belt should be selected for the operating temperature, product weight, surface requirements, and continuous-duty conditions. |
| Throughput and Line Speed | Actual production capacity at the required heating cycle, product spacing, belt loading, and line speed. | A capacity calculation based on product dimensions, mass, residence time, belt loading, and tested operating conditions. | Capacity should be stated at the required metallurgical result, not only at the highest possible belt speed. |
| Heating and Cooling Performance | Heating rate, soaking stability, cooling rate, cooling-zone temperature, and the effect of cooling on product properties. | Thermal profiles, cooling calculations, fan or water-system specifications, and sample test results. | The complete thermal cycle should match the required hardness, microstructure, dimensional stability, and surface quality. |
| Energy Efficiency | Electrical or fuel consumption, insulation performance, heat recovery options, standby settings, and exhaust-heat management. | A consumption estimate stated in relation to product throughput and operating temperature, together with insulation specifications. | Compare energy use per unit of processed material under equivalent production and temperature conditions. |
| Control and Data Logging | Number of control zones, programmable recipes, alarm functions, sensor calibration, trend recording, and data export. | Control-system architecture, sample process records, alarm list, user-access levels, and backup procedure. | The system should provide traceable records for critical parameters and protect recipes from unauthorized changes. |
| Safety Systems | Over-temperature protection, emergency stops, gas interlocks, door or access protection, exhaust control, and electrical safety. | Risk assessment, electrical schematics, safety-circuit description, operating instructions, and conformity documentation where applicable. | Safety functions should be independently testable and suitable for the installation country and site conditions. |
| Manufacturing Quality | Fabrication quality, insulation installation, welding quality, electrical assembly, component traceability, and inspection procedures. | Quality plan, inspection records, material certificates, welding documentation where relevant, and factory acceptance-test procedures. | Require documented inspections at defined stages instead of relying only on final visual inspection. |
| Testing and Acceptance | Whether factory and site acceptance tests confirm capacity, temperature performance, atmosphere stability, safety functions, and product results. | A signed FAT and SAT protocol containing measurable criteria, test instruments, tolerances, and corrective-action procedures. | Payment milestones should be linked to clearly defined and verifiable acceptance results. |
| Installation and Commissioning | Scope of installation support, utility requirements, foundation requirements, start-up procedures, and operator training. | Installation drawings, utility list, commissioning schedule, training plan, and responsibility matrix. | Responsibilities for transport, lifting, assembly, utilities, permits, and operator qualification should be stated in writing. |
| Maintenance and Spare Parts | Accessibility of heaters, thermocouples, motors, seals, bearings, burners, filters, belts, and control components. | Preventive-maintenance schedule, recommended spare-parts list, estimated replacement intervals, and service procedures. | Critical consumables and wear parts should have documented specifications and a realistic supply plan. |
| After-Sales Support | Response time, remote diagnostics, field-service availability, software support, warranty scope, and technical-document availability. | Warranty terms, service-level commitments, escalation process, training records, and examples of troubleshooting documentation. | Support obligations should include response times, exclusions, spare-parts responsibilities, and service rates. |
| Compliance Documentation | Compliance with applicable machinery, electrical, pressure, gas, environmental, and workplace-safety requirements. | Declarations, technical files, risk assessments, manuals, test reports, and country-specific conformity documents where required. | Verify that documents match the supplied furnace configuration and the regulations of the installation location. |
| Total Cost of Ownership | Purchase price, freight, installation, utilities, energy, maintenance, consumables, downtime, and end-of-life costs. | A five-year or ten-year cost model using stated assumptions for operating hours, energy prices, maintenance, and replacement parts. | Select the furnace using verified lifecycle cost and process performance, not the lowest initial quotation alone. |
When buying a belt annealing furnace for sale, start with the material, not the catalogue price. Define alloy, strip width, thickness, line speed, and target hardness. The IEA Energy Technology Perspectives 2023 reports that industry consumes about 37% of global final energy. Heat efficiency deserves serious attention. Ask for verified power consumption per processed tonne, not only installed heating capacity.
Temperature uniformity is equally important. Request temperature mapping across the usable belt width, including edge zones and loading changes. A practical factory trial should test real coils, protective atmosphere stability, and cooling response.
Check belt material, mesh design, replacement time, and spare-part availability. A furnace that runs hot but damages the belt is not economical. It is merely expensive equipment.
Control systems should record temperature, atmosphere, speed, alarms, and energy use. ISO 50001 guidance supports measured energy performance, although certification alone cannot prove furnace quality. Also examine insulation thickness, burner or heating-element maintenance, and emergency shutdown design. Ask for calibration records and service response times. Measure twice.
One overlooked issue is future production. A narrow belt may suit today’s orders but restrict tomorrow’s product range. I would also question optimistic capacity figures; they often assume ideal material and uninterrupted operation. Compare tested output, warranty terms, acceptance criteria, and operator training before purchasing from a China-based manufacturer. A lower quotation can hide commissioning delays, difficult controls, or unavailable components.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







