Choosing a China Best Roof Sheet Roll Forming Machine Manufacturer requires more than comparing prices. It requires practical judgment, technical evidence, and dependable communication.
A Roof Sheet Roll Forming Machine shapes galvanized steel through carefully aligned roller stations. Each station bends the strip gradually. This process reduces surface damage and supports consistent roof profiles.
George T. Halmos, author of Roll Forming Handbook, describes the process as “a continuous bending operation.” His explanation remains useful for evaluating machine design. A reliable manufacturer should understand material behavior, not only advertise production speed.
Experienced buyers inspect several details. They check frame rigidity, roller material, shaft diameter, drive configuration, and cutting accuracy. They also request trial production using the intended steel thickness. A sample roof panel can reveal poor alignment immediately.
Small errors matter.
A practical manufacturer should provide clear drawings, electrical specifications, installation guidance, and responsive after-sales support. Quality control records are valuable evidence. So are factory videos, customer references, and documented testing procedures.
However, no machine suits every project. A high-speed line may waste money for a small workshop. A compact machine may struggle with thick or wide coils. This is where careful consultation becomes important.
Some specifications can still be overlooked. I have seen buyers focus on forming speed while ignoring decoiler capacity and maintenance access. That decision often creates avoidable delays.
The strongest suppliers combine engineering experience with transparent recommendations. They explain limitations instead of promising perfection. For international buyers, this attitude supports trust, safer planning, and more stable long-term production.
China Best Roof Sheet Roll Forming Machine Manufacturer
Definition and Scope of Roof Sheet Roll Forming Machines
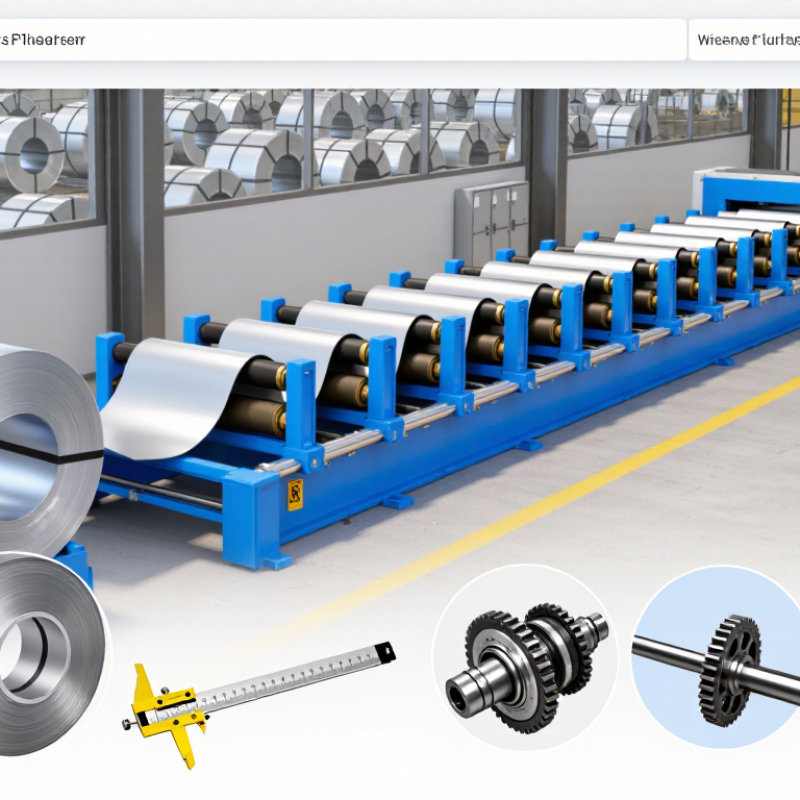
A roof sheet roll forming machine is a continuous production line for shaping metal coils into roofing panels. It usually includes a decoiler, leveler, forming stations, hydraulic cutter, and control cabinet. The coil moves through matched rollers, where each station adds a precise bend. The final profile may be trapezoidal, corrugated, or concealed-fix.
The scope is broader than roof production alone. These machines can process galvanized steel, pre-painted steel, and aluminum, depending on thickness, strength, and coating requirements. A practical specification review checks coil width, yield strength, forming speed, panel length, and cutting tolerance. Small errors become visible at the overlap.
According to the World Steel Association, global crude steel production reached about 1.89 billion tonnes in 2023. This large material base supports continued sheet-processing demand. UNEP’s 2023 Global Status Report states that buildings and construction consumed 32% of global energy in 2022 and produced 34% of energy-related carbon emissions. Lightweight, accurately formed roofing can reduce installation waste, but the machine itself still uses electricity and replacement tooling. That point is often overlooked.
Industry forecasts also connect metal roofing growth with faster construction and refurbishment. Yet forecast figures differ because reports define “roofing equipment” differently. This is a weakness worth recognizing. Buyers should compare technical data, sample panels, noise levels, and long-term maintenance records rather than trust market size alone. A clean edge matters. So does repeatable length control.
| Data Category | Technical Dimension | Typical Data or Standard | Definition and Application Scope |
|---|---|---|---|
| Machine Definition | Primary Function | Continuous cold roll forming | A roof sheet roll forming machine progressively bends a continuous metal strip through a series of shaped rollers to produce roofing profiles with a consistent cross-section. |
| Machine Definition | Finished Product | Trapezoidal, corrugated, tile-effect, or concealed-fix roof panels | The machine is intended for architectural roofing, wall cladding, industrial buildings, warehouses, workshops, agricultural structures, and commercial construction. |
| Input Material | Common Coil Materials | Pre-painted steel, galvanized steel, galvalume steel, and aluminum | Material selection depends on corrosion resistance, structural requirements, appearance, local climate, and compatibility with the selected roll-forming profile. |
| Input Material | Material Thickness | Approximately 0.30–0.80 mm for common roofing applications | The usable thickness range is determined by the profile geometry, material yield strength, roller design, drive capacity, and customer specifications. |
| Input Material | Coil Width | Approximately 900–1,250 mm, depending on the profile | The required coil width is normally greater than the finished cover width because part of the strip is consumed by bends, overlaps, and profile geometry. |
| Product Dimensions | Effective Cover Width | Approximately 750–1,100 mm | Effective cover width is the installed roofing width after side-lap or interlocking features are excluded. It is different from the total formed width. |
| Product Dimensions | Profile Height | Approximately 20–75 mm for many metal roof profiles | Profile height affects drainage performance, visual appearance, structural stiffness, lap design, and the amount of steel required for a specific span. |
| Forming System | Roller Stations | Approximately 8–24 forming stations | The number of stations varies with profile complexity, material thickness, bend radius, required surface quality, and the available machine layout. |
| Forming System | Roller Material | Machined steel rollers; hardened or treated surfaces may be used | Rollers must resist wear and maintain dimensional accuracy. Surface treatment can help reduce scratches and extend service life when correctly specified. |
| Production Performance | Typical Forming Speed | Approximately 8–30 m/min, excluding setup and cutting time | Actual output depends on profile complexity, material thickness, line configuration, cutting method, coil changes, operator settings, and quality-control requirements. |
| Production Performance | Length Tolerance | Commonly controlled to about ±1–2 mm per cut piece | The achievable tolerance depends on encoder accuracy, hydraulic or servo cutting control, material stability, machine calibration, and the specified production length. |
| Drive and Control | Drive Arrangement | Electric motor with gearbox and chain, gear, or cardan transmission | The drive system transfers torque to the forming stations. The appropriate arrangement depends on line speed, strip thickness, profile resistance, and maintenance preferences. |
| Drive and Control | Control System | PLC, touchscreen interface, encoder, and variable-frequency drive | The control system coordinates line start and stop, forming speed, automatic length measurement, batch quantity, fault alerts, and cutting operations. |
| Cutting System | Cutting Method | Hydraulic stop-to-cut or flying-cut configuration | Stop-to-cut systems pause the strip before cutting, while flying-cut systems can cut during movement and may support higher continuous production efficiency. |
| Line Components | Standard Equipment | Decoiler, leveling or guiding section, roll former, cutting unit, and run-out table | These components support coil unwinding, strip alignment, progressive forming, finished-length cutting, and safe collection of completed roof panels. |
| Decoiler | Typical Coil Capacity | Approximately 3–10 tonnes for common production lines | The required capacity depends on coil availability, material weight, loading equipment, production volume, and whether the decoiler is manual, hydraulic, or motorized. |
| Electrical Requirements | Common Power Supply | Three-phase 380–415 V, 50 Hz; other regional configurations are possible | Electrical specifications must be matched to the installation location. Actual total power depends on the motor, hydraulic station, control system, and auxiliary equipment. |
| Finished Products | Maximum Panel Length | Often limited by transport, handling, installation, and site logistics rather than forming capability | Long panels can reduce roof lap joints, but panel length should be selected according to coil length, building layout, transportation limits, lifting equipment, and thermal movement considerations. |
| Quality and Safety | Key Inspection Points | Profile width, height, straightness, cut length, surface finish, and interlocking accuracy | Routine inspection helps verify that formed sheets meet design drawings and can be installed without excessive gaps, distortion, coating damage, or dimensional mismatch. |
| Application Scope | Typical Building Uses | Factories, warehouses, workshops, agricultural buildings, retail facilities, and residential projects | Roof sheet roll forming machines are suitable for manufacturers and fabricators that need repeatable production of metal roofing panels in standard or customized profiles. |
| Customization Scope | Configurable Features | Profile geometry, cover width, thickness range, cutting length, automation level, and decoiler capacity | Customization should be based on approved profile drawings, material specifications, regional building practices, expected output, available floor space, and maintenance capability. |
Roof sheet roll forming depends on controlled movement, not one dramatic machine action. At the entry side, the decoiler supports the steel coil and releases it at a steady speed. Guide rollers center the strip before it reaches the forming stations. Each station uses shaped rollers to bend the sheet gradually. That gradual change protects the coating and reduces sharp stress marks.
Small errors matter. An uneven guide setting can create a wavering edge, poor overlap, or unstable panel length. Experienced operators check the strip with a square, tape measure, and visual inspection. These simple checks often reveal problems before production waste grows. During commissioning, I inspect the first panels for flange height, diagonal difference, and surface scratches.
Forming rollers are the core components, but the shaft system carries their accuracy. Precision shafts, bearings, spacers, and adjustable supports keep roller pressure consistent. The cutting unit usually works after forming, sizing each panel to the programmed length. A hydraulic or servo-driven system must cut cleanly without crushing the profile. The control cabinet coordinates feeding, speed, counting, and emergency stopping. Production is rarely perfect. Temperature, coil hardness, and rushed adjustments can change the result. Operators should record these deviations and refine alignment before the next coil enters.
China offers several roof sheet roll forming machine types, each designed for a different roof profile. Corrugated panel machines create deep, repeating ribs for warehouses and agricultural buildings. Trapezoidal machines produce wider load-bearing sheets with fewer overlaps. Tile profile machines imitate traditional ceramic tiles while using coated steel coils. Standing seam machines form concealed-joint panels for cleaner commercial roofs. Sandwich panel lines add insulation between two steel skins. They require more floor space and stricter alignment.
The World Steel Association reported China produced 1,019.1 million tonnes of crude steel in 2023. This large material base supports broad coil choices, including galvanized and pre-painted steel. A practical machine usually includes an automatic decoiler, leveling unit, roll stations, hydraulic cutting, and PLC control. The International Energy Agency notes buildings remain a major energy-use sector, supporting demand for better insulated roof systems. Yet insulation demand does not make every sandwich panel line suitable. Coil thickness, yield strength, panel length, and local voltage must be checked first. A test run matters. Small profile errors can become visible across a twelve-meter sheet. Some suppliers emphasize speed too much. That is a weakness worth questioning. Higher forming speed may reduce accuracy, increase noise, and shorten tooling life. Operators should inspect roll alignment, cutting tolerance, changeover time, and after-sales training before choosing a Chinese manufacturer.
China Best Roof Sheet Roll Forming Machine Manufacturer
How to Evaluate a Chinese Machine Manufacturer
Choosing a Chinese roof sheet roll forming machine manufacturer requires more than comparing prices. A credible supplier should explain forming tolerances, material grades, production speed, and machine capacity. Ask for detailed drawings, electrical layouts, and a clear list of included components. Details matter. Inspect the factory’s assembly area, welding quality, cable routing, and storage conditions. A polished showroom proves little without production evidence.
Evaluate technical capability through a real test run. Provide your roof profile, sheet thickness, steel type, and target output. The manufacturer should produce samples and measure width, rib height, cut length, and surface damage. Ask how operators adjust rollers and replace cutting blades. A test run should include startup, emergency stopping, and continuous operation. Do not accept samples made from unknown materials. I would record every measurement and compare it with your technical requirements.
Reliability appears in communication and after-sales support. Check response times before placing an order. Contact recent customers with similar profiles and production volumes. Read the warranty carefully, including exclusions, spare parts, remote support, and technician availability. Service speed matters. One weakness is often overlooked: small design changes can create long delays. Even a technically strong manufacturer may communicate poorly across languages and time zones. Leave room for clarification, inspection, and revision before final approval.
China Best Roof Sheet Roll Forming Machine Manufacturer
Production standards shape every stage of a dependable roof sheet roll forming machine. Engineers should match the machine design with coil thickness, sheet width, profile depth, and required production speed. Clear drawings and approved material specifications reduce misunderstandings before fabrication begins.
Customization must solve real production needs. A machine may include adjustable guide rails, reinforced forming stations, automatic cutting, and a user-friendly control system. For example, a galvanized coil entering at 1.2 meters per minute should remain aligned through every station. Small deviations can create uneven overlaps or visible panel waves. That detail matters.
Quality control needs evidence, not promises. Inspectors should check shaft alignment, roller hardness, electrical wiring, and cutting accuracy. Trial production can reveal vibration, noise, or unstable feeding. These issues should be recorded and corrected before shipment. No process is flawless. A rushed inspection may miss a loose fastener or minor roller mismatch. That is a weakness worth admitting, not hiding. Reliable manufacturers keep inspection reports, test finished panels, and explain maintenance requirements clearly. This approach supports safer operation, consistent output, and more informed purchasing decisions.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru