China Best Metal Stamping Parts Manufacturer?
Choosing China’s best Metal Stamping Parts manufacturer requires more than comparing quoted prices. A capable supplier turns sheet metal into consistent components for automotive, electronics, appliances, and industrial equipment. The real test appears in small details: clean edges, stable dimensions, and accurately positioned holes. A sample may look excellent. Production consistency matters more. This introduction examines how experience, engineering discipline, and transparent quality systems shape a dependable partnership. It also questions the word “best,” because one factory rarely fits every application.
Experienced manufacturers usually explain material selection before recommending a die design. They may discuss stainless steel, aluminum, copper, or coated steel according to strength, conductivity, and corrosion exposure. Their engineers should review drawings, bend allowances, part orientation, and expected production volume. Clear communication reduces expensive tooling changes later. Still, expertise is not proven by impressive machinery alone. Ask for process records, inspection methods, and examples of similar components. A reliable team can describe press capacity, tooling maintenance, and dimensional controls without hiding behind vague promises. That practical transparency builds trust.
Quality evidence should include first-article inspection, in-process checks, and final sampling. Useful records may show caliper readings, CMM reports, surface inspections, and material certificates. Supplier audits, traceable batch numbers, and corrective-action reports strengthen confidence. Certifications can help, but they never replace direct evidence. We will explore capability, communication, tooling, lead times, and after-sales support. Some decisions remain difficult. The lowest quote may create the highest total cost. The fastest response may conceal weak engineering. By examining these trade-offs carefully, buyers can identify a China-based partner that delivers safe, repeatable, and application-specific Metal Stamping Parts.
What Defines China’s Best Metal Stamping Parts Manufacturer?
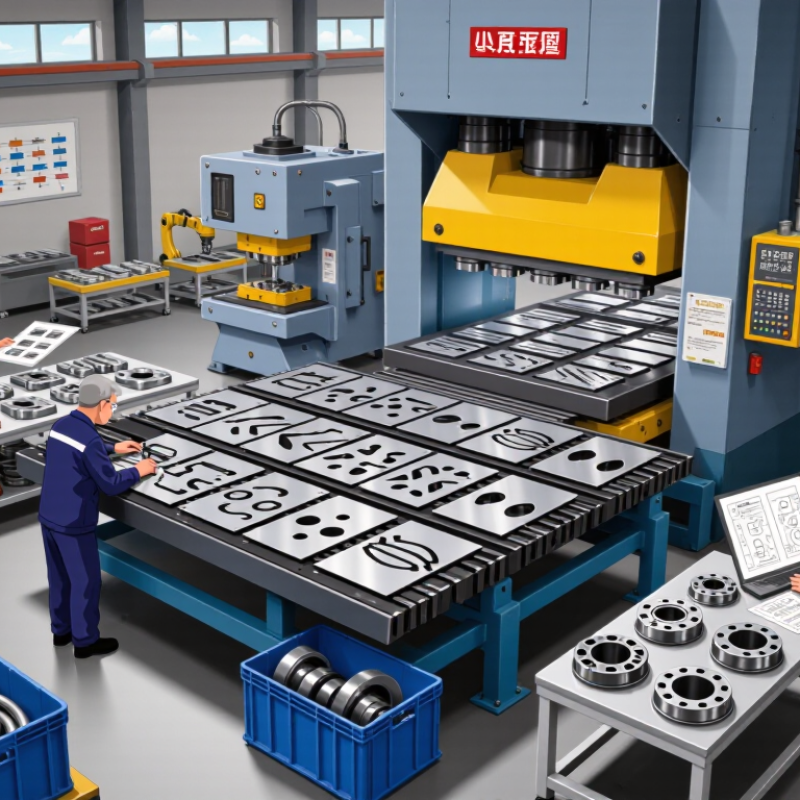
China’s best metal stamping parts manufacturer is defined by consistent performance, not attractive pricing alone. Experienced teams understand material behavior, tool wear, springback, and burr control. They review drawings before production and question unclear tolerances. That habit prevents expensive corrections later.
A reliable manufacturer provides traceable steel or aluminum records, inspection reports, and controlled production samples. Engineers should explain how progressive dies, blanking, bending, or piercing will affect the part. In one practical evaluation, a small trial run revealed uneven edges after repeated stamping. The issue was corrected through die adjustment, but it showed why pilot production matters. No supplier is perfect. Careful review still matters.
Tips: Request a sample inspection report, material certificate, and tooling maintenance plan. Check critical dimensions with calibrated equipment. Ask how nonconforming parts are isolated and recorded. Clear communication is also evidence of professionalism. Replies should include measurable details, not vague promises. A dependable partner discusses capacity, lead time, packaging, and corrective actions openly. Certifications can support credibility, but daily process discipline proves more. The strongest manufacturer combines engineering judgment with transparent records and stable output. That combination protects product fit, production schedules, and long-term purchasing decisions.
How Progressive Dies Deliver Production Speeds Above 500 Strokes per Minute
China Best Metal Stamping Parts Manufacturer?
How Progressive Dies Deliver Production Speeds Above 500 Strokes per Minute
Progressive dies can exceed 500 strokes per minute when the strip moves accurately between several forming stations. At this rate, each stroke lasts only 0.12 seconds. The die must pierce, bend, draw, and separate parts without disturbing the next position. Tight pitch control matters. So does consistent coil thickness.
Industry research supports this production model. A 2024 report from Grand View Research identifies automotive and electronics as major metal stamping applications, where high-volume output and repeatability remain essential. The U.S. Department of Energy also highlights material utilization and process efficiency as important cost factors in metal forming. Less scrap usually means more than faster presses.
In practical die trials, engineers check feed accuracy, pilot timing, shut height, and lubrication before increasing speed. Sensors can detect misfeeds or broken punches within milliseconds. A small alignment error may damage an entire die set. That part is easy to underestimate.
Above 500 strokes per minute is not automatically better. Tool wear, noise, heat, and inspection capacity can reduce real output. A line rated at 600 strokes may deliver fewer acceptable parts after stoppages. Experienced manufacturers therefore measure good parts per hour, not only press speed. Production records, material certificates, dimensional reports, and maintenance logs make the result more reliable. The unfinished lesson is simple: speed needs discipline.
Material Selection by Strength: Steel, Aluminum, and Copper Grades
China Best Metal Stamping Parts Manufacturer?
Material Selection by Strength: Steel, Aluminum, and Copper Grades
A reliable metal stamping process begins with the load, shape, and working environment. Steel remains a practical choice for brackets, clips, and structural panels. Mild steel grades such as 1008 or 1010 form easily and resist cracking during deep drawing. Higher-strength steel improves load capacity, but it can increase springback and tool wear. That trade-off is often underestimated.
Aluminum saves weight and offers useful corrosion resistance. Grade 5052-H32 suits formed covers, housings, and marine-related components. It bends well, although sharp corners may create cracks. Grade 6061-T6 provides higher strength, but its heat treatment can make stamping less forgiving. Copper and brass serve different priorities. C110 copper offers excellent electrical conductivity, while C260 brass balances conductivity, strength, and formability.
Material selection should include thickness, grain direction, edge condition, and coating requirements. A production review should test actual coils, not only rely on a datasheet. Small changes in hardness can alter burr height, dimensional accuracy, and tool life. Real experience shows that the “strongest” grade is not always the best grade. I have seen a stronger alloy fail because its forming window was too narrow. That result deserves reflection. A capable manufacturer should document mechanical properties, inspect incoming material, and validate parts through trial stamping and dimensional checks. Tacit assumptions create expensive surprises.
Quality Control Through ISO 9001, IATF 16949, and ±0.01 mm Tolerances
Choosing a reliable metal stamping parts manufacturer begins with measurable quality, not attractive promises. ISO 9001 provides a controlled framework for documented procedures, corrective actions, and continual improvement. In daily production, this means operators follow approved work instructions and record inspection results. Small errors matter.
For automotive components, IATF 16949 adds stricter expectations for risk control, traceability, process capability, and customer-specific requirements. Experienced teams review material certificates, tooling condition, press settings, and first-article samples before releasing production. Critical dimensions are checked with calibrated gauges, micrometers, and coordinate measuring equipment. A ±0.01 mm tolerance demands more than a final inspection. It requires stable tooling and disciplined process monitoring.
Statistical process control can reveal drift before parts leave the line. Lot identification also helps investigators trace material, machine, operator, and inspection data. These practices support dependable supply decisions. However, a certificate alone cannot guarantee consistent parts. Tool wear may develop between scheduled checks, and measurement methods can introduce their own uncertainty. That weakness deserves attention.
In practical work, quality engineers should compare drawings with real forming behavior, especially around bends, springback, and burr control. Samples may pass inspection yet create assembly problems later. Open communication between production and engineering reduces that risk. Honest reporting is better than hiding a variation. The strongest supplier is not flawless; it detects problems early, documents the response, and improves the process with evidence.
China Best Metal Stamping Parts Manufacturer?
Quality Control Through ISO 9001, IATF 16949, and ±0.01 mm Tolerances
ISO 9001:2015 A quality management system framework for consistent processes, documentation, and continual improvement.
IATF 16949:2016 An automotive quality management system standard focused on defect prevention, traceability, and process control.
Dimensional Control The chart visualizes a stated critical tolerance of ±0.01 mm around the nominal dimension.
How to Compare Tooling Cost, MOQ, Lead Time, and Total Value
China Best Metal Stamping Parts Manufacturer?
How to Compare Tooling Cost, MOQ, Lead Time, and Total Value
A low tooling quote can hide expensive compromises. Ask whether the die is progressive, transfer, or single-operation. Then confirm steel grade, expected tool life, maintenance responsibility, and ownership terms. A supplier quoting 20% less may use weaker tool steel or exclude engineering changes. I have seen “cheap” dies require repeated adjustments after the first trial. That delay can exceed the original saving. MOQ also needs context. Compare annual demand, batch size, storage cost, and scrap exposure, not only the unit price.
Lead time should include design review, die construction, sampling, corrections, and production approval. UNCTAD reports that more than 80% of global trade volume moves by sea, so shipping schedules can quickly affect launch dates. Request a milestone chart with buffer days. ISO’s 2023 survey recorded over 1.2 million ISO 9001 certificates worldwide, but certification alone does not prove stamping accuracy. Ask for capability studies, inspection records, material certificates, and sample approval data.
Tips: Build a landed-cost sheet. Include tooling, parts, packaging, freight, duties, inspection, rework, and inventory. Compare suppliers at the same specification and forecast. A supplier offering a higher unit price may reduce total value through stable tolerances and fewer disruptions. Still, do not trust polished spreadsheets blindly. Check several production lots, inspect burr height, and question unclear assumptions. Mistakes happen. Your comparison should expose them early.
Benchmark assumptions: Indicative ranges are based on common international purchasing conditions for carbon steel, stainless steel, aluminum, and copper-alloy stamped parts. Estimated first-year total cost includes one tooling charge plus the indicated unit price at the stated 10,000-piece reference volume, but excludes freight, taxes, surface treatment, secondary assembly, material surcharges, and special inspection requirements.