Choosing an Alloy Wheel Curing Oven is a production decision, not just a matter of buying a heated cabinet. The right system must deliver even temperatures across rims, support a steady line pace, and fit the coating process you actually use. Small details matter. A crowded rack, uneven airflow, or a slow recovery after the door opens can leave finish quality inconsistent and disrupt a shift.
As [verified alloy-wheel curing specialist’s name] puts it, “A reliable cure starts with consistent heat where the wheel sits—not just the temperature shown on the control panel.” That is a useful test when comparing ovens. Ask how temperature uniformity is measured, where sensors are placed, and whether the supplier can share data from a loaded oven. Then look closely at usable chamber dimensions, airflow design, controls, energy use, maintenance access, and after-sales support.
The seven tips in this guide turn those questions into a practical selection process. They help you compare equipment against real workshop conditions: wheel sizes, rack layouts, daily output, and available floor space. Not every specification tells the whole story. A brochure may promise precision, while your own trial reveals cold spots near a loaded rack. Check the evidence. Keep room for doubt, too; a technically capable oven may still be the wrong fit if it slows your line or complicates routine maintenance.
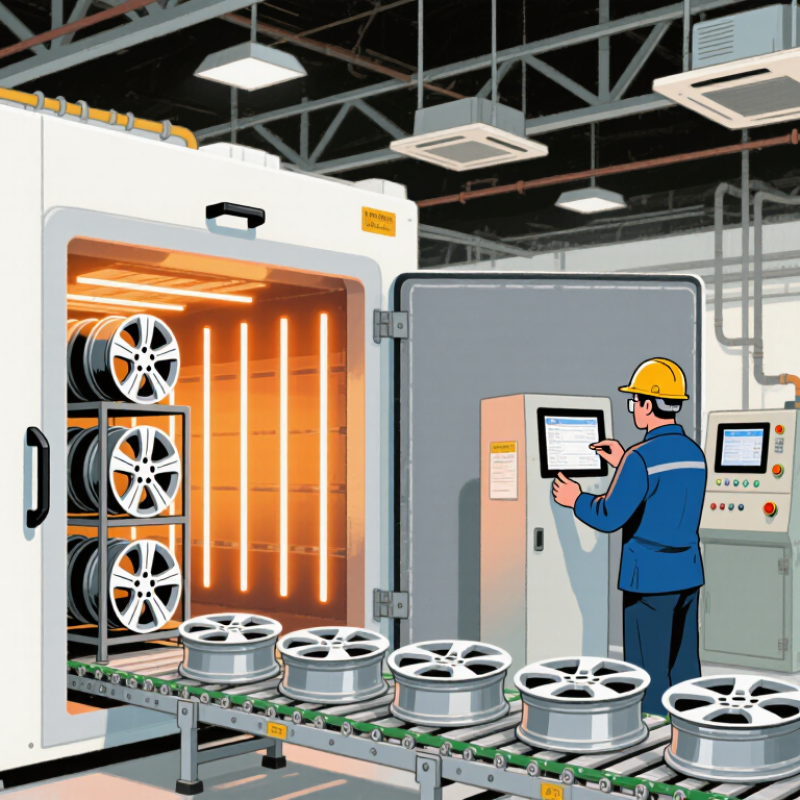
Alloy wheel curing begins with the coating’s chemistry, not a generic oven setting. Powder and liquid coatings can require different time-temperature schedules, so follow the coating supplier’s technical data sheet. The critical measure is usually the wheel’s metal temperature, not the oven’s displayed air temperature. Not just oven air. Thick hubs and spoke junctions heat differently from thin rim sections. A contact thermocouple on a representative wheel helps verify when the required metal temperature is reached and held.
The U.S. Department of Energy’s 2016 Improving Process Heating System Performance: A Sourcebook for Industry estimates that process heating accounts for about 36% of U.S. manufacturing energy use. That makes insulation, airflow, and sensible loading worth checking—not just maximum temperature. Leave space between wheels so heated air can circulate around the spokes and inner barrel. Record actual temperature curves across test cycles; an oven display alone cannot confirm a uniform cure. A minor weakness in many setup plans is testing only one wheel geometry. Different designs may heat unevenly, so validate the schedule with representative wheels before relying on it for routine production.
Match the oven to the wheels moving through it, not just the largest wheel in your catalog. Record wheel diameter, width, weight, and hourly output, then calculate how many wheels must be inside during the full cure cycle. For batch ovens, check usable rack area and loading clearance; for conveyor systems, set belt speed and spacing around the required dwell time. Leave room for uneven demand and future models. Small details matter.
The U.S. Energy Information Administration’s 2018 Manufacturing Energy Consumption Survey recorded 22.1 quadrillion Btu of energy use across U.S. manufacturing. That figure is not specific to wheel ovens, but it highlights why avoidable empty heating capacity deserves attention. Compare expected loads, warm-up time, door openings, and shift patterns before choosing a chamber. A tidy spreadsheet can still be wrong if it assumes every shift runs at full rate. Confirm the cure schedule against the coating supplier’s specifications, then use thermocouples on representative wheels to check actual metal temperature. A larger oven may ease loading, but it can also heat unused space; a smaller one may create queues. The right configuration depends on measured flow, not guesswork.
When comparing alloy wheel curing ovens, separate temperature uniformity from control accuracy. Uniformity describes temperature differences across the working space; control accuracy describes how closely the displayed value matches the actual temperature. An oven may hold its sensor reading steadily while a wheel near the door runs cooler. That matters.
Check temperature performance with a loaded oven, not just an empty chamber. Place calibrated probes near the upper and lower racks, at the center, and close to the door. Record readings during heat-up, the full cure period, and cooling. A smooth control-panel display is not enough. Look for repeatable results across several cycles, and compare them with the coating supplier’s specified cure window. The required tolerance depends on the coating and process, so avoid choosing a number by guesswork.
Ask how often sensors are calibrated and how the controller responds when readings drift. Review the actual temperature map, including the time needed to recover after loading. Small detail. A brief door opening can change conditions near the entrance, even when the central probe barely moves. Keep in mind that a single test can miss uneven loading or probe placement errors. It is worth questioning a perfect-looking chart; real production rarely behaves so neatly.
An alloy-wheel curing oven should be judged by energy used per loaded batch, not its empty-chamber rating. The U.S. Department of Energy’s Improving Process Heating System Performance sourcebook estimates that process heating consumes about two-thirds of manufacturing energy. Ask suppliers for measured consumption, warm-up time, and temperature uniformity under a realistic wheel load. Compare like with like. A low quoted cycle time means little if the oven needs long recovery periods between batches.
Safety details matter on the shop floor. Look for independent over-temperature protection, door interlocks, reliable airflow monitoring, and clear alarms. Verify that controls prevent heating when circulation fails, and check how operators can safely unload hot wheels. Small details count. A handle that stays cool is not a substitute for a documented safety procedure.
Build quality shows in insulation joints, door seals, welded seams, and fan access for maintenance. Inspect these areas, not just the exterior panels. I would not assume thicker sheet metal guarantees better performance; poor sealing can waste heat, and a strong specification can still be poorly assembled. Request temperature-mapping results and service records, then compare them with your wheel sizes and daily batch pattern. Real operating data beats a polished brochure.
| Tip | What to Compare | Evidence or Specification to Request | Why It Matters | Practical Buyer Check |
|---|---|---|---|---|
| 1. Match the oven to the coating process | Usable chamber dimensions, wheel capacity, loading method, and operating temperature range. | Internal dimensions, maximum load, temperature range, and the coating supplier’s required part-metal temperature and cure time. | Powder-coating cure schedules vary by coating formulation and are generally specified for the part itself, not just the oven-air temperature. | Confirm that the largest planned load fits with adequate space for airflow. Check the coating technical data sheet before selecting a temperature range. |
| 2. Compare energy use under the same conditions | Energy consumed per production cycle, heat-up time, insulation, and heat loss during operation. | Measured energy use for a defined cycle, including the load, starting temperature, setpoint, and hold time. Request insulation details and door-seal specifications. | Rated heater power alone does not show how much energy an oven uses to process a batch; cycle conditions and heat retention also affect consumption. | Compare kWh per cycle using equivalent loads and temperature schedules. Ask whether the quoted figure is measured or estimated. |
| 3. Check temperature uniformity with a loaded chamber | Temperature distribution throughout the chamber and repeatability between cycles. | A temperature-uniformity test report, including sensor locations, test conditions, and results with a representative load where available. | Even heating helps each wheel receive the intended cure. An accurate controller reading at one point does not, by itself, demonstrate uniform chamber temperature. | Ask how the oven is tested and where its control and monitoring sensors are placed. Verify the result against the coating process requirements. |
| 4. Review independent safety protections | Over-temperature protection, alarms, emergency stop, door or airflow interlocks where applicable, and safe shutdown behavior. | Electrical and control-system documentation, safety device list, operating instructions, and details of applicable local codes or standards. | Independent protective devices and clear operating procedures help reduce risks from overheating, equipment faults, and incorrect operation. | Confirm which protections are standard, how faults are indicated, and whether the equipment is designed for the installation jurisdiction and intended process. |
| 5. Assess ventilation and process separation | Air circulation, exhaust or ventilation requirements, and separation from powder application activities. | Airflow design information, installation clearances, ventilation requirements, and written guidance on permitted oven use. | A curing oven must be installed and operated for its intended purpose. Powder application and curing should follow suitable separation and process-safety controls. | Do not assume an oven is suitable for spraying or powder application. Have the proposed layout and ventilation reviewed for local requirements. |
| 6. Inspect construction and serviceability | Chamber materials, insulation installation, door construction, seals, structural frame, and access to service components. | Construction drawings or material specifications, maintenance schedule, replaceable-part list, and warranty terms. | Well-documented construction and accessible components can support reliable operation and make inspection and maintenance easier. | Inspect door alignment and seals, ask how heating elements and controls are serviced, and confirm the availability of replacement parts. |
| 7. Compare controls, records, and support | Programmable temperature settings, cycle monitoring, data logging, operator usability, and technical support. | Control-system functions, sample cycle records, training materials, commissioning scope, and response arrangements for service support. | Consistent settings and usable records help operators repeat approved cycles and investigate process deviations. | Ask for a demonstration using a representative cycle. Check whether operators can review setpoint, measured temperature, alarms, and cycle history. |
Note: Confirm curing schedules with the coating manufacturer and verify equipment, installation, ventilation, and safety requirements against applicable local regulations. Energy figures should be compared using equivalent cycle conditions and loads.
Before choosing an alloy wheel curing oven, check the installation conditions at your actual workshop. Measure doorways, ceiling height, and floor space, including room to load a wheeled rack safely. Confirm electrical capacity, ventilation needs, and the floor’s rated load with qualified site personnel. A layout drawing can catch problems early. It is easy to underestimate clearance.
Ask the supplier what installation includes: delivery, positioning, commissioning, and operator training. During handover, staff should learn how to set a cure schedule, verify temperature readings, and respond to an alarm. Request maintenance intervals and a list of wear parts, such as door seals, filters, and temperature sensors. Keep a simple log of inspections and temperature checks; small changes can reveal trouble before production is affected. Still, logs do not replace proper calibration.
Supplier support matters after commissioning. Ask how quickly technical staff respond, whether replacement parts are stocked, and what information they need to diagnose faults remotely. Get support terms in writing, including coverage hours and service costs. If possible, speak with a workshop using a similar oven and ask about downtime, not just performance. Some details may remain unclear until the oven is running in your space. That deserves attention.
Compare key buying considerations, including installation, maintenance, and supplier support.
Example planning scores on a 1–5 scale, where 5 indicates a higher priority. These are illustrative buyer-assessment scores, not survey results; adjust them to your production needs. Confirm oven capacity, temperature performance, site requirements, maintenance access, and service coverage with suppliers.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru