Choosing the right Ferrule Crimping Tool in 2026 requires more than comparing prices or counting advertised features. A reliable tool should create a firm, even connection without damaging the ferrule or conductor. In practical use, small details matter. The handle should remain stable in one hand. The ratchet should release only after a complete crimp. The die must match the ferrule size and profile.
This guide examines the factors professionals and careful installers should check before buying. These include wire-range compatibility, crimp geometry, frame strength, jaw alignment, grip comfort, and quality control. It also considers tools for control cabinets, electrical panels, machinery wiring, and occasional workshop repairs. Clear manufacturer specifications matter, but they should not be accepted blindly. Samples, test crimps, and consistent pull checks can reveal problems that product photographs hide.
No tool is perfect. A compact model may feel comfortable, yet struggle with larger ferrules. A heavy-duty tool may last longer, but tire the user during repetitive work. I have found that convenience can sometimes disguise poor adjustment or uneven pressure. That weakness deserves attention. The best Ferrule Crimping Tool is not always the most expensive option. It is the one that delivers repeatable results, fits the intended wire sizes, and supports safe, careful workmanship. This 2026 buying guide will help readers compare practical performance, durability, and long-term value before making a confident decision.
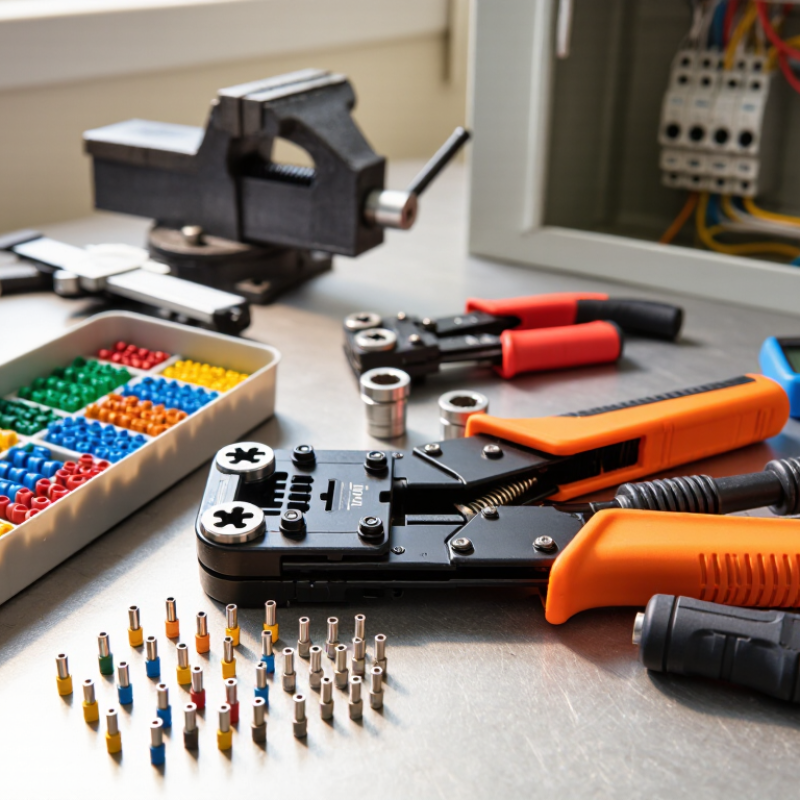
Selecting a ferrule crimping tool starts with the wire, not the handle. Check the conductor size, usually marked in square millimeters. A tool for 0.5 mm² wire may damage a 2.5 mm² ferrule. It may also leave a weak connection. Confirm the ferrule’s terminal type, including insulated, uninsulated, twin, or short-barrel designs. The crimp profile must match the terminal geometry.
IEC 60228 conductor class also affects tool selection. Class 1 solid conductors behave differently from Class 2 stranded conductors. Class 5 and Class 6 flexible conductors need careful compression. Their fine strands can spread during insertion.
I prefer tools with clear size ranges and repeatable ratcheting action. However, printed ranges are not enough. Test the actual wire and ferrule combination.
A practical check includes visual inspection, conductor insertion, and a gentle pull test. The ferrule should grip firmly without cutting through the sleeve. Keep the stripped length precise. Too much exposed copper looks untidy and may reduce insulation clearance. Too little wire can weaken the crimp.
I once trusted a smooth-looking connection that failed under vibration. That mistake changed my inspection routine. A perfect crimp is not proven by appearance alone.
Calibration records, clean dies, and consistent hand pressure matter.
Small details matter.
Choosing a ferrule crimping tool starts with the ferrule, not the handle. DIN 46228-1 covers tubular wire-end ferrules, while DIN 46228-4 generally includes ferrules with plastic collars. Check the conductor cross-section, sleeve length, and collar diameter before selecting a die. A 2.5 mm² ferrule is not automatically compatible with every 2.5 mm² tool setting.
Measure twice. Crimp once.
In practical assembly work, I compare the ferrule’s metal barrel with the tool’s stated capacity range. The range must cover both the conductor size and the ferrule construction. Some tools accept insulated and uninsulated ferrules, but their die shapes may differ. A square crimp, hexagonal crimp, or trapezoidal crimp can affect terminal entry and pull-out performance. Use the tool’s technical data, not only its printed scale. Markings can be surprisingly vague.
After crimping, inspect the conductor strands. They should remain inside the barrel, without exposed copper beyond the collar. The ferrule should hold firmly, but the insulation collar must not be crushed. A light pull test can reveal poor compression. For critical panels, a calibrated tensile test provides stronger evidence. I once trusted a familiar size marking and ignored the ferrule wall thickness. The connection looked acceptable, yet it fitted poorly in the terminal. That mistake changed my checking routine. Dimensions, die profile, and tool capacity must agree together. One measurement alone is not enough.
Choosing a ferrule crimping tool in 2026 requires more than selecting a square or hexagonal profile. DIN 46228 defines requirements for wire-end ferrules, including dimensions, materials, and suitability for stranded conductors. It does not simply approve one universal crimp shape. A reliable tool should match the ferrule size range and produce consistent compression without cutting strands.
IEC 60999-1 focuses on the performance of connecting devices for copper conductors. Its test approach examines clamping reliability, mechanical strength, temperature behavior, and electrical continuity. Therefore, a ferrule profile should support stable contact inside the terminal, not only look symmetrical. A tidy crimp can still fail.
Professional testing data matters. IEC 60999-1 evaluates connections under mechanical and thermal stress, while DIN 46228-based testing checks ferrule construction and crimp quality. Industry wire-processing reports also show that automated inspection and documented process control are becoming more common in high-volume assembly. That trend is practical, not decorative.
In field work, I compare a finished ferrule under magnification. I check for split sleeves, exposed strands, uneven compression, and conductor movement. Then I perform a controlled pull test using the applicable specification. The correct profile depends on the terminal geometry. Square crimps often suit cage-clamp terminals, while hexagonal or trapezoidal forms may perform better elsewhere. This is where selection becomes less certain. The tool must be validated with the actual ferrule and terminal combination.
How to Choose the Best Ferrule Crimping Tool in 2026?
Daily production exposes weaknesses quickly. Ratchet force should close the terminal fully without excessive hand pressure. A higher setting is not automatically better. It may improve compression, but it can also increase fatigue during repetitive work. The U.S. Bureau of Labor Statistics reported that overexertion and bodily reaction caused 27.2% of private-industry days-away-from-work cases in 2023. That figure supports careful force evaluation. Test the tool with your most common ferrule sizes, using a force gauge when possible. Inspect crimp height, conductor retention, and release smoothness.
Cycle life matters just as much. Request documented testing conditions, including ferrule material, conductor size, and number of cycles. A large cycle figure means little without those details. IEC 60999-1 provides useful guidance for screw-type connection performance, but it does not replace application-specific crimp validation. Check whether the ratchet maintains its release point after extended use. Small changes can create inconsistent crimps. This is easy to overlook.
Tips: Hold the tool near the center of its handles. Keep the wrist straight. Compare five operators, not one. Record hand force, completed crimps per minute, and failed crimps. Rounded handles may feel comfortable initially, yet comfort can change after several hours. I would also question perfect laboratory results. Real benches include dust, rushed movements, and uneven wire preparation. Choose the tool that stays predictable there.
Evaluate ratchet force, cycle life, and ergonomics for daily production.
Lower peak handle force reduces operator fatigue during repeated crimping.
Higher validated cycle life supports stable production and fewer tool replacements.
The ergonomic score combines handle force, grip comfort, and repeated-use suitability.
The production-readiness index is weighted as follows: 40% cycle life, 35% ratchet-force efficiency, and 25% ergonomic suitability. Lower force values are better; higher index values are better.
How to Choose the Best Ferrule Crimping Tool in 2026?
Verify Pull-Out Strength, Insulation Quality, and Calibration Traceability
A reliable ferrule crimping tool should produce a firm, repeatable connection. Do not judge it by appearance alone. A clean hex pattern can still hide weak compression. During evaluation, insert the ferrule into the specified conductor size. Then perform a controlled pull-out test with suitable equipment. Record the force, conductor condition, and crimp location. Repeated results matter more than one impressive sample.
Insulation quality deserves equal attention. The ferrule should grip the conductor without cutting strands or cracking its plastic collar. Check the entry point under bright light. Look for exposed copper, uneven sleeves, and crushed insulation. A smooth wire stop helps prevent inconsistent insertion depth. Small details matter. I once accepted a neat-looking crimp too quickly, then found loose strands beneath the collar. That mistake changed my inspection routine.
Calibration traceability separates a professional tool from an uncertain one. Ask for calibration records, reference standards, adjustment history, and the next verification date. The tool should also identify its rated wire ranges clearly. Storage conditions can affect performance, especially after heavy workshop use. In-house checks are useful, but they do not replace documented verification. My own process is not perfect; pull testing every connection is impractical. Still, scheduled sampling can reveal jaw wear before failures become routine. A tool with controlled force, clear markings, and traceable records supports safer, more consistent electrical assembly.
| Evaluation Dimension | Recommended 2026 Benchmark | Verification Method | Weight | Decision Result |
|---|---|---|---|---|
| Compatible conductor range | Must cover the required ferrule sizes; a broad professional range is typically 0.14–10 mm². | Check the tool marking, technical datasheet, and actual compatibility with the selected ferrule series. | 15% | Pass if all required sizes are covered |
| Ferrule standard compatibility | Suitable for insulated or non-insulated wire-end ferrules manufactured to the applicable DIN 46228 requirements. | Compare ferrule dimensions, conductor cross-section, sleeve length, and crimp profile with the tool specification. | 10% | Pass if profile and size match |
| Pull-out strength | No single pull-out value applies to every ferrule size. Results must be compared at the same conductor size, ferrule type, conductor material, and test speed. | Perform tensile testing on at least 10 samples per size; record minimum, average, and failure mode in newtons. | 25% | Select the tool with the strongest repeatable result |
| Crimp consistency | Crimps should be fully formed, centered, and free from cracks, loose strands, excessive deformation, or conductor damage. | Inspect 30 consecutive crimps across small, medium, and large ferrule sizes; measure crimp height where specified. | 15% | Pass with no visible defects |
| Insulation quality | The ferrule sleeve must remain intact and securely attached; the crimp must not cut, split, or loosen the insulation. | Use visual inspection and a retention check after crimping. If the tool is marketed for electrical safety work, verify the applicable insulated-tool rating separately. | 15% | Pass if sleeve and insulation remain undamaged |
| Calibration traceability | A current calibration record should identify the tool serial number, measurement uncertainty, calibration date, due date, and traceability to national or international standards. | Request a calibration certificate from an ISO/IEC 17025-accredited laboratory or an equivalent documented quality system. | 10% | Pass with complete traceable records |
| Calibration interval control | Use a risk-based interval; annual verification is a practical starting point for frequently used production tools. | Review usage frequency, overload history, failed inspections, and the organization’s documented calibration procedure. | 5% | Pass if interval is documented |
| Locking and release mechanism | The tool should complete the crimp cycle reliably and prevent premature release when the design requires a controlled full cycle. | Test the mechanism under repeated operation and confirm that incomplete crimps cannot be mistaken for completed crimps. | 3% | Pass if operation is repeatable |
| Ergonomics and maintenance | Low hand force, clear size markings, corrosion-resistant surfaces, replaceable wear parts, and accessible cleaning instructions. | Conduct an operator trial and review spare-part availability, lubrication requirements, and maintenance documentation. | 2% | Pass if suitable for planned workload |
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru