Choosing the best Pipe Swaging Machine begins with understanding the work, not browsing the highest-powered model. Tube diameter, wall thickness, material hardness, production volume, and end-form design all influence the decision. A machine that handles stainless steel beautifully may struggle with softer aluminum or thin-wall tubing. Small details matter, too. Inspect the tooling range, stroke control, motor capacity, cycle speed, and adjustment accuracy. Ask how quickly dies can be changed. In a busy workshop, ten lost minutes can become several lost hours.
Manufacturing quality expert W. Edwards Deming said, “Quality comes not from inspection, but from the improvement of the production process.” His principle applies directly to pipe swaging. A reliable machine should create consistent ends before defects reach final inspection. Look for repeatable pressure, stable alignment, guarded moving parts, and accessible maintenance points. Check the supplier’s technical support, spare-parts availability, training, and warranty terms. These practical factors often matter more than impressive brochure figures.
Do not choose by tonnage alone. That is an easy mistake. A larger machine may waste energy, floor space, and tooling budget when your components are modest. At the same time, an undersized unit can produce uneven shoulders, surface marks, or premature tool wear. Review sample parts, request a forming trial, and measure the finished dimensions. Your first choice may still need revision after testing. That is not failure; it is useful evidence. The right Pipe Swaging Machine should fit your material, workflow, operators, and long-term production goals.
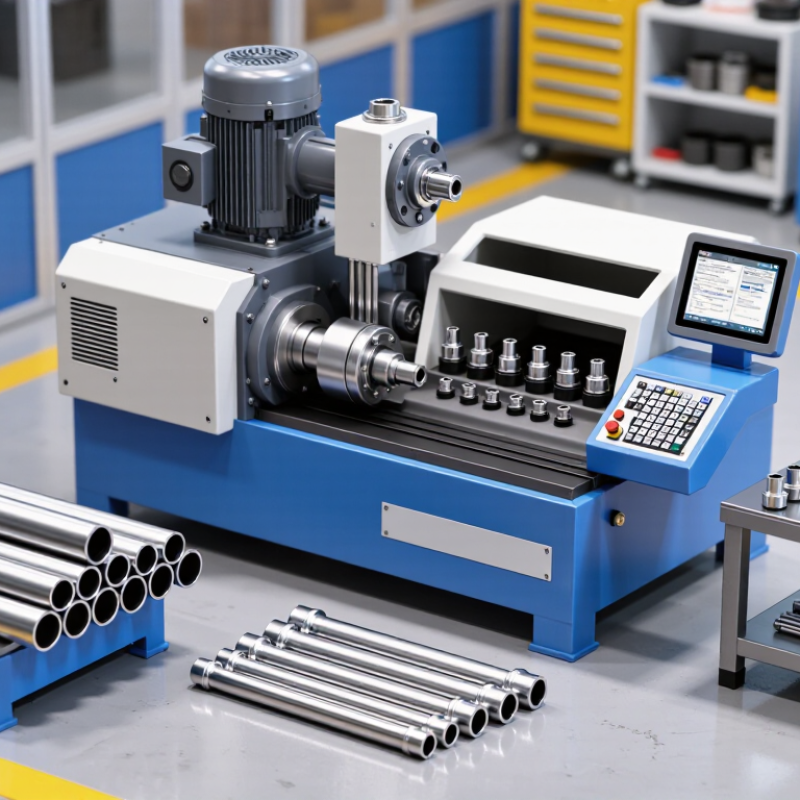
A pipe swaging machine reshapes a tube end by controlled radial pressure. It can reduce diameter, form shoulders, or prepare a clean joint. The process usually uses matched dies, hydraulic force, and measured closing strokes. Unlike cutting, swaging preserves a continuous surface with limited material waste.
These machines serve many industries. Plumbing workshops use them for fitting connections. Automotive fabricators form exhaust tubes and suspension parts. HVAC and heat-exchanger production depend on consistent tube ends. Structural manufacturers may swage thin-wall tubes before assembly. However, one machine cannot suit every application. Material hardness, tube diameter, wall thickness, and production volume all change the decision. A specification sheet may look impressive but still hide difficult setup requirements. That deserves checking.
Tips: Test actual tubes before buying. Measure the finished diameter at several points. Check die-change time, pressure control, guarding, and emergency stops. Ask whether standard tooling fits your common sizes. For stainless steel or high-strength alloys, confirm the required forming force. A trial run can reveal springback, surface marks, or uneven shoulders. These details often matter more than maximum machine capacity. Also examine maintenance access and operator training materials. A powerful machine is not automatically the best machine.
Choosing the best pipe swaging machine starts with the pipe, not the machine. Steel, stainless steel, aluminum, and copper respond differently under compression. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023. USGS estimated global primary aluminum output at about 70 million metric tons that year. These materials require different die pressures, lubrication methods, and deformation limits.
Record the pipe’s outside diameter, inside diameter, wall thickness, and length. Then identify whether the shape is round, oval, tapered, or irregular. A round tube may need simple radial dies. An oval tube can require guided tooling and tighter alignment. Also check the material’s yield strength, hardness, and temper. A thin aluminum tube may collapse before it swages correctly. That small detail is easy to miss.
Machine capacity should match the maximum diameter and wall thickness, not the average job. Ask for usable stroke, closing force, die range, and repeatability data. ASTM or ASME material certificates can support reliable selection, but certificates alone cannot predict every forming result. A practical trial remains valuable. I would inspect the first sample for wrinkles, cracks, ovality, and springback. The spreadsheet may look perfect. The pipe may disagree.
Choosing a pipe swaging machine starts with the forming task, not the machine price. Rotary swaging machines reduce pipe diameter through repeated die impacts. They suit precise ends, fittings, and moderate wall thicknesses. Hydraulic machines apply steady force and handle larger diameters or tougher alloys. Manual units remain useful for repair work and low production volumes. They demand more operator judgment, however.
Capacity must match the pipe’s outside diameter, wall thickness, length, and material hardness. A machine rated for 50 millimeters may perform poorly near its limit. Leave practical allowance for springback and tooling clearance. Check the manufacturer’s force chart, then test a sample. Steel can respond differently after heating, cutting, or previous forming. This detail is easy to miss.
Operating method also affects output quality. Manual control gives flexibility but can produce uneven lengths and inconsistent pressure. Semi-automatic models improve repeatability while keeping setup changes manageable. CNC systems support programmed cycles, force monitoring, and higher production rates. They also require trained technicians and careful maintenance. More automation is not always better. I have seen operators choose complex controls for simple jobs, then lose time during setup. Inspect dies for wear, verify pipe alignment, and record actual cycle results. A practical choice often comes from trial data, not a brochure.
Accuracy should be judged on finished pipes, not impressive specifications. Check diameter tolerance, repeatability, and alignment across several test pieces. A reliable machine should produce consistent swage depth without visible cracks, oval sections, or uneven edges. Request calibration records and inspect the measuring method. Small errors can become costly during assembly.
Safety features deserve direct inspection. Look for guarded moving parts, an emergency stop, pressure relief, and clear operating controls. Two-hand activation can reduce accidental contact during forming. However, safety depends on training and daily habits, not hardware alone. Operators should understand pinch points, safe loading, and lockout procedures. Never trust a familiar machine blindly.
Maintenance affects accuracy and service life. Ask whether dies, seals, and hydraulic fluid are easy to inspect or replace. A practical machine should allow quick cleaning around the tooling area. Keep a maintenance log with dates, wear observations, and pressure readings. That record often reveals problems before production quality changes. Durability also depends on frame rigidity, heat management, and protection from dust. A heavy frame helps, but it does not excuse poor alignment or careless setup. I have seen robust equipment deliver poor results after neglected lubrication. Test the machine under realistic workloads, then review the parts under proper measurement tools. The first trial may expose assumptions worth challenging.
Choosing a pipe swaging machine starts with production evidence, not catalogue promises. Record tube diameter, wall thickness, material hardness, daily volume, and required tolerances. Measure them across several shifts. One sample can mislead.
Deloitte’s 2024 Smart Manufacturing Survey reports that 86% of manufacturers expect smart manufacturing to become essential within five years. That supports choosing machines with usable production data, fault records, and compatible controls. However, automation only helps when operators can understand it. Request a live trial using your actual tube material. Check forming consistency, cycle time, changeover minutes, and tooling access. A ten-second saving may matter more than an impressive maximum force rating.
Budget beyond the purchase price. The U.S. Department of Energy notes that compressed-air systems can lose 20% to 30% of their output through leaks and inefficient use. Ask about hydraulic power, air consumption, heat generation, and standby energy. Calculate tooling, maintenance, training, installation, and rejected parts over five years. The machine with the lowest price may become expensive beside a noisy compressor and frequent die replacement. It happens. I would also leave capacity headroom, perhaps 15% to 20%, but not blindly; unused capacity still occupies floor space and capital. Compare documented test results, service response times, spare-part availability, and operator feedback before approving the purchase.
Selecting the best machine for your production needs and budget
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru