How to Choose the Best Ready Concrete Batching Plant
Choosing a Ready Concrete Batching Plant is not just a capacity decision. It affects delivery schedules, mix consistency, operating costs, and the space available on site. The Global Cement and Concrete Association estimates that the world uses around 14 billion cubic metres of concrete each year. That scale makes dependable production more than a purchasing detail. It is a practical requirement.
Start with the work your plant must actually handle. A small urban project may need a compact layout and quick setup. A large infrastructure job may require higher output, multiple aggregate bins, and reliable continuous operation. Check rated capacity against realistic hourly demand, not only the highest figure in a brochure. Look closely at weighing accuracy, mixer type, control systems, maintenance access, and spare-parts support. These details matter on a rainy morning, when wet aggregate can affect batch proportions and a delayed truck can disrupt placement.
Energy and material efficiency deserve attention too. The International Energy Agency identifies cement production as a significant source of global carbon emissions, so reducing waste and avoiding unnecessary idle operation can support more responsible production. Still, no plant is automatically efficient. Results depend on mix design, operator training, maintenance, and local conditions. A specification sheet cannot tell the whole story. Ask suppliers for documented performance data, references from comparable projects, and clear service terms. Then compare the plant against your site, workforce, and concrete demand. The best choice is rarely the biggest one; it is the one that performs reliably where you need it.
Define Ready Concrete Batching Plants: Stationary, Mobile, and Compact Models
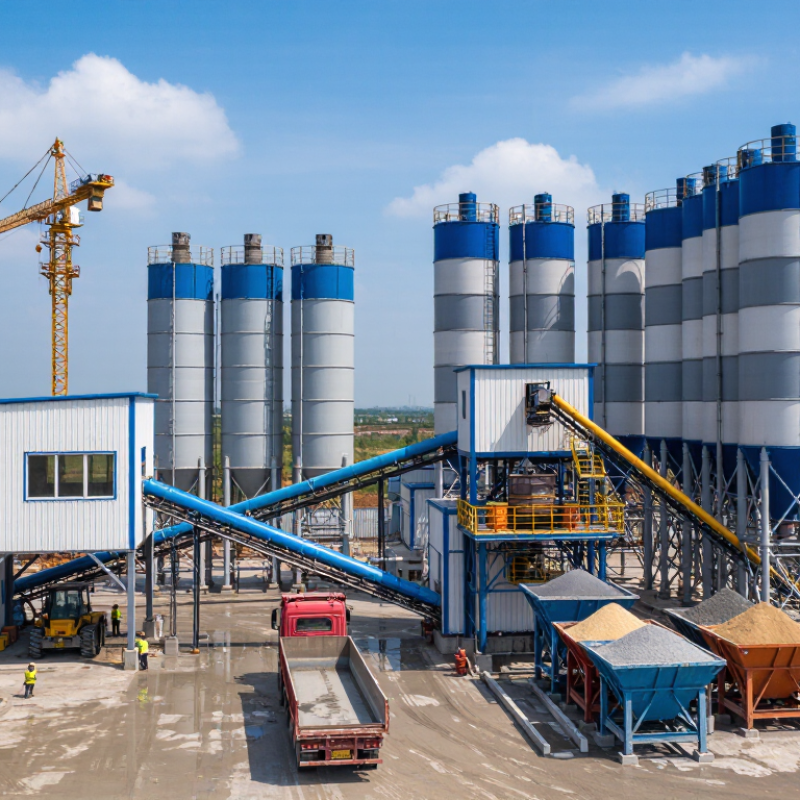
Ready concrete batching plants combine measured aggregates, cement, water, and admixtures to produce concrete for delivery to a project. The Global Cement and Concrete Association estimates that about 14 billion cubic metres of concrete are used worldwide each year. That scale makes plant choice practical, not cosmetic: transport distance, output demand, and site access all matter. A plant that looks efficient on paper may still struggle with narrow gates or uneven ground.
Stationary models suit long-term, high-volume production. Their fixed foundations and larger storage areas support steady operations, but they require space and substantial setup. Mobile plants can be relocated between projects and are useful where delivery routes are long or work sites change. Their real advantage depends on transport time and setup needs; “mobile” does not mean instant to deploy. Compact models fit restricted sites and smaller batches, though storage and throughput are limited.
The U.S. Environmental Protection Agency’s AP-42 Section 11.12 describes concrete batching operations and identifies dust-emission points such as aggregate handling and cement loading. Check enclosure, dust collection, and maintenance arrangements during selection.
A missed detail matters. Even a compact plant needs room for safe truck movement, material storage, and cleaning.
Match Production Capacity from 25–240 m³/h to Project Pouring Demand
How to Choose the Best Ready Concrete Batching Plant
Match Production Capacity from 25–240 m³/h to Project Pouring Demand
Choosing capacity starts with the pour schedule, not the plant brochure. A small foundation may need only 25–40 m³/h. A bridge deck can demand 90–120 m³/h during a narrow placement window. Large industrial slabs may require 180–240 m³/h to maintain a continuous pour.
Rated output is not always real output. Moist aggregates, longer loading paths, and truck shortages reduce performance. In field planning, allowing 15–25% capacity above average demand often protects the pouring rhythm. For example, a 70 m³/h requirement may suit an 85 m³/h plant. Small gaps matter. Concrete can begin setting while crews wait.
Review the complete delivery cycle. Check batching time, mixer truck turnaround, travel distance, and site access. A 25 m³/h plant may work well where trucks queue easily and pours remain intermittent. It may struggle on a large continuous slab. A 240 m³/h model can offer strong output, but it also needs steady aggregate supply, reliable power, trained operators, and enough trucks.
Do not guess. Use actual project data. Record hourly demand, not only the daily volume. Discuss moisture control and calibration with experienced technicians. I have seen plans fail because they measured plant capacity but ignored traffic delays. That mistake is preventable, although real sites rarely behave perfectly. Leave room for weather, maintenance, and uneven crew productivity.
How to Choose the Best Ready Concrete Batching Plant - Match Production Capacity from 25–240 m³/h to Project Pouring Demand
| Nominal Plant Capacity (m³/h) | Planning Output at 75% (m³/h) | Indicative Pouring Demand (m³/h) | Typical Project Fit | Selection Guidance |
| 25 | 18.75 | Up to 15 | Small building works, repairs, and low-volume site pours | Consider when demand is intermittent and a compact setup is important. |
| 35 | 26.25 | 15–22 | Small to medium construction projects | Allow for interruptions in aggregate loading, batching, and delivery. |
| 50 | 37.5 | 22–32 | Housing developments and regular commercial pours | Check that truck availability and site access can keep pace with production. |
| 60 | 45 | 32–40 | Medium-sized commercial and infrastructure projects | A practical choice for sustained pours with a dependable delivery cycle. |
| 75 | 56.25 | 40–50 | Larger building sites and steady ready-mix supply | Assess storage, batching schedule, and concrete delivery routes together. |
| 90 | 67.5 | 50–60 | High-volume commercial work and multiple active pour areas | Confirm that material replenishment and dispatch can support continuous operation. |
| 120 | 90 | 60–80 | Major infrastructure works and large construction programs | Plan for sufficient aggregate, cement, water, and admixture supply. |
| 180 | 135 | 80–120 | Large infrastructure projects and high-output supply operations | Evaluate transport capacity, site layout, and backup arrangements. |
| 240 | 180 | 120–160+ | Very large, sustained pours with coordinated logistics | Use only when the site, material supply, and fleet can support the required throughput. |
Planning figures are indicative: actual output varies with mix design, aggregate moisture, batching cycle, plant configuration, operator practice, maintenance, and delivery logistics. Compare the required sustained pour rate with realistic operating output, not nominal capacity alone.
Select Mixer Sizes from 0.5–4.5 m³ by Batch Volume and Cycle Time
Choosing a ready concrete batching plant starts with batch volume and cycle time, not advertised capacity. Mixer sizes from 0.5 to 4.5 m³ suit different project rhythms. A 0.5 m³ mixer can serve small foundations, repairs, and narrow urban sites. Larger 2–4.5 m³ mixers support continuous slab, road, and structural work.
Estimate practical output with this formula:
batch volume × 60 ÷ cycle time × operating efficiency.
A 2 m³ mixer with a 5-minute cycle theoretically produces 24 m³ per hour. Real output may fall to 17–20 m³ because of loading delays, moisture adjustments, truck queues, and cleaning. I once planned around ideal cycle times, and the schedule became too optimistic. Site access was the missing detail.
Tips:
Measure the actual travel distance between aggregate bins, mixer, and discharge point. Check whether trucks can arrive at the same pace as batches. Leave capacity for seasonal moisture changes and routine maintenance. A larger mixer is not automatically better; underfilled batches can waste cement and reduce consistency. For small pours, a 0.5–1 m³ unit may offer better control. For steady high-volume work, 3–4.5 m³ equipment can reduce loading frequency, provided the supporting system keeps pace. Record several trial cycles before final selection. Data beats assumptions.
Compare ASTM C94 Compliance, Dust Control, Energy Use, and Automation Features
When choosing a ready concrete batching plant, check ASTM C94/C94M requirements against actual production records, not a sales checklist. Ask to see calibrated scale certificates, batch tickets, water-addition logs, and procedures for correcting out-of-tolerance batches. The standard covers ready-mixed concrete production and delivery; it does not guarantee every mix will perform well. Your mix designs and local materials still matter. Small details matter. Watch an operator run a real batch: can they trace each ingredient and record a manual adjustment without losing the original data? Automation helps, but a poorly configured moisture probe can quietly skew water content.
Dust collection deserves the same scrutiny. OSHA’s silica rule sets a permissible exposure limit of 50 micrograms per cubic meter over eight hours, with an action level of 25. These are worker-exposure benchmarks, not equipment ratings. Inspect enclosed transfer points, silo vents, and filter-cleaning systems while trucks are loading.
For energy, request metered electricity and fuel use per cubic yard, then compare similar mixes and output rates. The IEA estimates cement production causes roughly 7% of global CO2 emissions; that figure concerns cement, not batching plants, but it makes material efficiency worth tracking. I would still question any “low-energy” claim without a defined measurement period. A dashboard cannot fix poor sampling.