Selecting a Chrome Plated Valve is not simply a matter of choosing the brightest finish. The wrong valve can develop pitting, leaks, or damaged threads under demanding service conditions. This guide introduces seven practical tips for comparing materials, pressure ratings, sealing systems, and maintenance needs.
Valve reliability engineer Daniel Mercer explains, “Chrome plating is valuable only when the base valve and service conditions are correctly matched.” That principle deserves attention. Chrome may improve surface hardness and corrosion resistance, but it cannot correct poor machining or unsuitable internal materials. A shiny body can distract us.
We will examine where the valve will operate, including fluid type, temperature, pressure, and cleaning exposure. A workshop technician should inspect plating uniformity, edge coverage, thread quality, and visible surface defects. A digital caliper can reveal inconsistent dimensions around the connection points. Product certificates and pressure-test records also support more dependable purchasing decisions.
The discussion will compare industrial, hydraulic, pneumatic, and general-purpose applications. It will also address seal compatibility, flow control, installation practices, and long-term inspection. Some choices remain imperfect. A lower-cost valve may appear efficient until replacement labor and unexpected downtime are included. Conversely, an expensive Chrome Plated Valve may offer little value in a mild environment.
These seven tips are designed to support careful judgment, not automatic selection. Always verify manufacturer data before installation. Reliability starts with evidence.
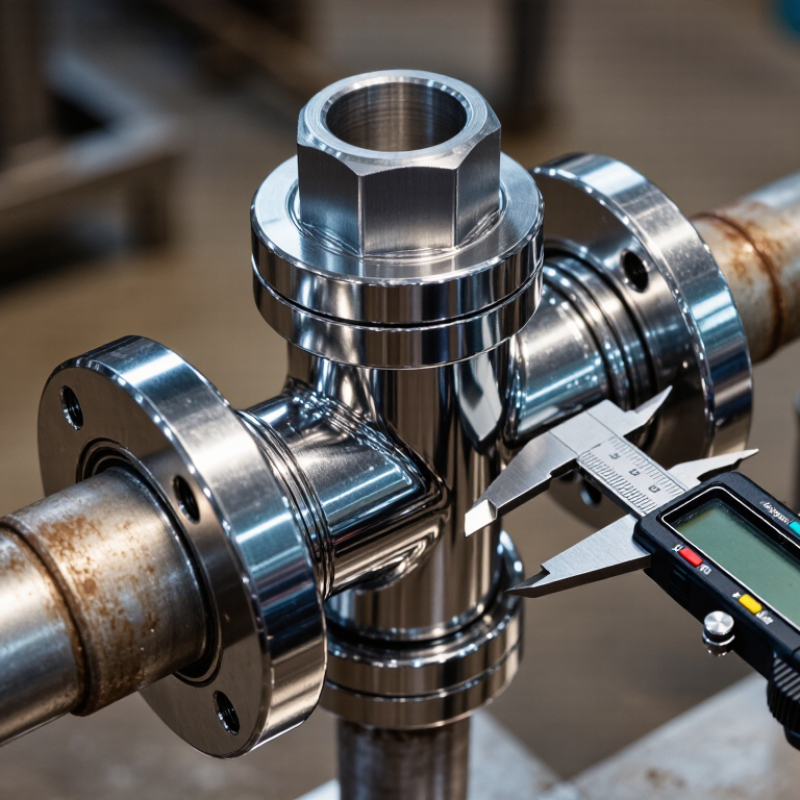
Choosing a chrome plated valve starts with service conditions, not appearance. ASME B16.34:2022 defines pressure classes from 150 to 2500, but Class 150 does not mean 150 psi. The allowable pressure changes with temperature, body material, and design details. A valve rated Class 600 at 38°C may handle far less pressure at elevated temperatures. Check the standard’s pressure-temperature tables carefully.
Tip 1: Record the maximum pressure, operating temperature, fluid, flow direction, and cycling frequency. Include upset conditions. A forgotten steam surge can damage trim quickly. Chrome plating may improve surface hardness and wear resistance, but it cannot correct an undersized body or unsuitable sealing material.
Tip 2: Match the valve class to the complete piping system. ASME B16.34 must be read with the applicable flange, welding, and inspection requirements. The 2024 industrial valve market report from Grand View Research estimated the global market above USD 70 billion in 2023, reflecting heavy use across energy, chemical, and water facilities. Market size is not proof of reliability. Test records matter more.
Tip 3: Request material certificates, pressure-test results, coating thickness data, and traceability documents. API 598 provides widely used valve inspection and testing practices, but project specifications may require stricter acceptance limits. One practical mistake is treating a shiny chrome surface as evidence of long service life. It is not. Confirm hardness, adhesion, porosity, and compatibility with the actual medium.
| No. | Selection Dimension | Relevant Service Condition | Recommended Evaluation | Chrome Plating Consideration | Applicable Standard or Reference | Practical Selection Guidance |
|---|---|---|---|---|---|---|
| 1 | Pressure class | Design pressure and maximum operating pressure | Select an ASME B16.34 Class 150, 300, 600, 900, 1500, or 2500 valve that exceeds the required pressure at the design temperature. | Chrome thickness does not increase the pressure class of the valve body or pressure boundary. | ASME B16.34 pressure-temperature ratings | Do not treat the class number as a universal pressure value. The allowable pressure depends on body material and temperature. |
| 2 | Design temperature | Minimum, normal, maximum, and upset temperatures | Use the pressure-temperature rating table for the exact valve material and the controlling temperature. | Confirm that the plating process, base material, seals, and lubrication system are suitable for the complete temperature range. | ASME B16.34; applicable material specifications | A rating acceptable at ambient temperature may be reduced at elevated temperature; low-temperature impact requirements may also apply. |
| 3 | Reference rating example | Approximate pressure at 100°F for carbon steel body material | Use the following values only as an initial reference for ASTM A216 WCB-type carbon steel; verify the certified material group and current standard edition. | The coating has no independent ASME pressure rating. | ASME B16.34 pressure-temperature tables | Illustrative ratings: Class 150: 285 psi; Class 300: 740 psi; Class 600: 1,480 psi; Class 900: 2,220 psi; Class 1500: 3,705 psi; Class 2500: 6,170 psi. Actual values must be confirmed from the selected material and standard edition. |
| 4 | Fluid compatibility | Water, oil, gas, steam, chemicals, abrasive or particle-laden media | Review fluid composition, concentration, pH, chloride content, velocity, solids content, and contamination risks. | Hard chrome can improve surface hardness and wear resistance, but it is not universally resistant to acids, chlorides, or aggressive chemicals. | Manufacturer chemical-compatibility data; ASTM coating test methods where specified | Specify the base metal, chrome type, coating thickness, substrate preparation, and chemical limits rather than requesting “chrome plated” alone. |
| 5 | Valve end connection | Flanged, threaded, socket-weld, or butt-weld piping system | Match the valve connection, nominal pipe size, facing, bore, wall thickness, and pressure class to the piping design. | Protect plated surfaces from impact, excessive tightening, welding heat, and installation damage. | ASME B16.5 for many flanges; ASME B16.25 for butt-weld ends; ASME B16.34 for valve requirements | Confirm dimensional compatibility and gasket selection before ordering, especially when changing pressure class or flange facing. |
| 6 | Leakage and testing | Required shutoff, shell integrity, and fugitive-emission performance | Define the valve test standard, seat leakage acceptance, test medium, duration, and documentation requirements. | Inspect the plating for pinholes, flaking, cracks, edge damage, and dimensional buildup that could affect sealing. | API 598 or the project-specified valve inspection and testing standard | Pressure testing must validate the complete assembled valve; coating inspection alone cannot demonstrate pressure-boundary integrity. |
| 7 | Operation and maintenance | Manual or automated operation, cycling frequency, accessibility, and maintenance interval | Check operating torque, actuator sizing, stem arrangement, installation orientation, drain or vent requirements, and spare-part availability. | Verify that repeated cycling, abrasive service, and contact with seats or packing will not prematurely wear the plated surface. | ASME B16.34; actuator and project maintenance specifications | Select plating for a defined wear or friction requirement, and establish repair or recoating limits before commissioning. |
Important: ASME pressure classes are designations rather than fixed pressure values. Final valve selection must be based on the applicable ASME B16.34 pressure-temperature rating for the exact body and trim materials, design temperature, fluid, end connection, and testing requirements.
7 Tips for Choosing a Chrome Plated Valve
Chrome plating can improve surface hardness, wear resistance, and cleaning performance. However, a bright finish does not prove adequate protection. In valve selection, verify the coating requirement against ASTM B650 and the intended service conditions. The standard addresses electrodeposited engineering chromium coatings on ferrous substrates. It does not replace a project specification or engineering review.
Tip 1: Request the exact ASTM B650 classification, not only the phrase “chrome plated.” Coating thickness can vary with sliding contact, corrosion exposure, and operating temperature. Confirm the required minimum thickness on the drawing or purchase specification. Tip 2: Ask for inspection records. They should identify the substrate, plating process, measured locations, and test method. A single reading may be misleading. Edges, threads, and sealing areas often plate differently.
Tip 3: Check thickness using a suitable, calibrated instrument. Compare several points across the valve, especially around the stem and sealing surfaces. Tip 4: Inspect adhesion and surface condition after plating. Blisters, cracks, pits, or uneven deposits may signal poor preparation or excessive process stress. Tip 5: Confirm dimensional control. Chrome adds material, and tight clearances can change after plating. This detail is easy to overlook. I have seen visually impressive coatings fail practical fit checks. A measured coating is more trustworthy than a polished appearance. Review the current ASTM B650 edition with a qualified inspector, because application requirements and acceptance criteria must match the valve’s actual duty.
7 Tips for Choosing a Chrome Plated Valve
Tip 1: Identify the actual fluid before choosing the valve. Chrome plating may resist wear, but it is not universally chemical-resistant. Check pH, chlorides, solvents, abrasives, and oxygen content. A clean-looking surface can hide damage beneath the coating.
Tip 2: Match every material to the operating temperature. Heat can weaken plating adhesion, seals, and valve seats. Confirm continuous and peak temperatures in the technical datasheet. Do not rely only on the temperature printed on a process diagram. Tip 3: Check whether the fluid touches the chrome, substrate, or lining. The underlying steel may control corrosion performance. Scratches, pinholes, and threaded areas deserve careful inspection. Tiny defects matter.
Tip 4: Assess galvanic-corrosion risks around connected equipment. Chrome-plated surfaces can contact stainless steel, brass, aluminum, or carbon steel. Conductive fluids may accelerate galvanic attack between dissimilar metals. Use compatible materials, suitable isolation, or protective design details. Tip 5: Consider pressure cycling and vibration. Repeated movement can expose the substrate at edges and sealing surfaces. Tip 6: Ask for coating thickness, adhesion testing, and inspection records. Reliable suppliers should explain their test methods clearly. Tip 7: Recheck the selection against real service conditions, not ideal laboratory data. This step is often skipped. I would also question assumptions made from appearance alone; a bright valve is not automatically a safe valve. Consult a qualified valve engineer when temperature, chemistry, or electrical conductivity changes during operation.
Temperature limits are approximate values commonly used for material selection. PTFE offers broad chemical resistance, EPDM is suitable for water and steam but performs poorly with oils, FKM handles oils and fuels but is not preferred for hot steam, and NBR is widely used for oils at lower temperatures. Chrome plating protects the valve surface, but the valve substrate, seal material, fluid chemistry, and galvanic contact must also be evaluated.
Confirm that seat leakage and shell tests meet API 598 acceptance requirements before choosing a chrome plated valve. Chrome plating can improve surface hardness and wear resistance, but it does not replace pressure testing. Ask for a test report that identifies the valve size, pressure class, test medium, duration, and calibrated equipment. Vague paperwork deserves caution.
The shell test checks the pressure boundary, including the body, bonnet joint, and stem sealing area. Under the applicable API 598 requirements, these areas should show no visible leakage during the specified test.
The seat test examines closure performance from the upstream and downstream sides. Acceptable leakage depends on the valve design, nominal size, and seating material. Metal seats may allow a defined leakage rate, while resilient seats generally require no visible leakage.
Check the actual acceptance table, not just a sales statement. Ask whether the test used clean water, air, or another approved medium. Air can reveal leakage differently from water. Confirm that pressure was stabilized before inspection. Small details matter. Record everything.
A practical inspection should also compare the report with the valve marking and purchase specification. Mismatched serial numbers, unclear test dates, or missing signatures weaken traceability. I have seen inspections focus heavily on chrome appearance while overlooking seat performance. That is an easy mistake. The coating may look flawless, yet the valve can still fail to isolate reliably. Personally, I would request retesting when records are incomplete, even if the exterior appears excellent.
Choosing a chrome plated valve starts with the actuator, not the finish. Start with the cycle. Match pneumatic, electric, or manual actuation to cycle frequency, fail-safe needs, available power, and control response. The U.S. Department of Energy reports that compressed-air leaks can waste up to 30% of compressor output. That makes pneumatic efficiency and leak testing important operating costs. Ask qualified suppliers for torque curves, cycle-test records, enclosure ratings, and actuator service intervals.
Maintenance evidence should be specific. Request chrome thickness, adhesion results, substrate details, and fluid-compatibility data. ISO 15848-1 provides a recognized framework for fugitive-emission testing, while pressure-test documentation should identify the actual test standard and acceptance criteria. A chrome finish is not a warranty. Poor preparation can still produce early flaking, especially near seats, stems, or threaded areas. I have seen comparison sheets overvalue purchase price and ignore access time. That is a costly mistake.
Use the life-cycle method described in NIST Handbook 135. Include valve price, actuator controls, installation, inspection, spare parts, energy, downtime, and disposal. The cheapest quotation may require longer maintenance outages. Compare at least three qualified suppliers using the same duty cycle and service conditions. Require lead times in writing. Require replacement-part pricing too. Price is entry cost. A spreadsheet can still lie. Review the assumptions before approval.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru