How to Choose an Industrial Mixing Machine? The answer starts with the material, not the catalog. A batch of thin liquid behaves differently from a sticky paste or powder blend. Viscosity, density, shear sensitivity, batch size, and cleaning needs all shape the choice. Small details matter. Dried residue on a tank wall may signal poor circulation; a slow-moving surface can hide uneven mixing below.
Edward L. Paul, co-editor of Handbook of Industrial Mixing: Science and Practice, offers a useful process-first perspective. A concise paraphrase of that approach is: define the process before selecting the mixer. For buyers, this means documenting ingredients, target consistency, mixing time, temperature limits, and production rate before comparing an Industrial Mixing Machine. Then assess impeller type, motor power, vessel geometry, seals, controls, and service access. Ask suppliers how they validate performance with materials similar to yours. Request test results, not just brochure claims.
There is no universal best machine. A high-shear mixer may improve dispersion but damage a delicate product. A simpler agitator may be easier to clean, yet leave stubborn dead zones. Trade-offs are real. This guide explains how to compare machine types, specify operating conditions, review maintenance features, and evaluate supplier evidence. Some choices remain uncertain until a trial run. Careful selection reduces that uncertainty, but cannot erase it. It begins with honest process data and clear priorities.
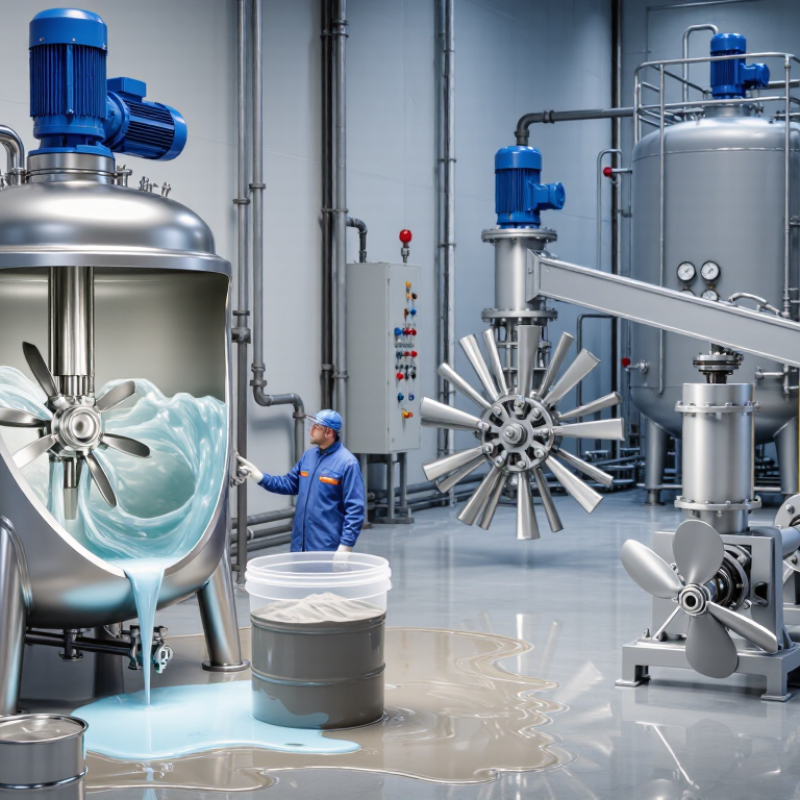
Before comparing industrial mixing machines, document what enters the vessel. Record each material’s physical form, particle-size range, bulk density, moisture, viscosity, abrasiveness, and temperature. Note whether these properties change during processing; a powder may cake when warm liquid is added. Small details matter. For powders, density differences can encourage segregation. For viscous pastes, wall scraping and heat buildup may be more important. A practical review of actual materials is more useful than choosing equipment from a product description alone.
Define the desired result in measurable terms. Specify the required uniformity, acceptable clump size, batch time, temperature limit, and whether ingredients must dissolve, disperse, or remain suspended. Avoid relying on “homogeneous” as the only target. Set a sampling plan, including where samples will be taken and which test will assess consistency. Then test a representative batch. I would not assume that a successful small trial guarantees the same result at full scale; vessel geometry and fill level can change mixing behavior.
Energy use also deserves attention. The International Energy Agency’s Energy Efficiency 2023 report estimates that industry accounts for about 37% of global energy use. That broad figure is not a mixer-performance benchmark, but it supports tracking energy alongside product quality. Record kilowatt-hours per batch, mixing time, and any temperature rise. Those measurements can reveal when an aggressive mixing objective is unnecessary—or when a gentler process is failing.
Choosing an industrial mixing machine starts with the process, not the machine’s advertised capacity. Identify the materials, batch size, target consistency, and any temperature or time limits. A thin liquid may blend well in a tank with a propeller or turbine. A thicker paste usually needs an anchor or other close-clearance agitator to move material near the vessel walls. For powders entering liquid, a high-shear mixer can help disperse clumps, but it may add heat or pull in air. That matters for heat-sensitive ingredients.
Match the mixer to the job it must repeat. A ribbon blender suits many dry powders, while a paddle mixer can handle gentle, even blending. For emulsions or fine dispersions, high shear may be appropriate; for fragile particles, gentler agitation can preserve their shape. Check cleanability, seals, and access for maintenance alongside mixing performance. A machine can look right on paper and still leave dead zones in a real vessel. Process trials are useful. They may also show that the original specification was incomplete.
Tips: Share a sample material and a realistic batch size with the equipment supplier. Ask how mixing time, temperature, and product uniformity will be checked. Watch for settling at the bottom and residue on the walls. Small details matter. Keep notes from each trial, even when results seem obvious.
01 Determine capacity from the batch you need to process, not the tank’s nameplate volume. Record working volume, fill level, and the smallest and largest batch sizes. A 1,000-liter vessel may not mix well at 200 liters if the impeller sits too high or loses submergence. Include headspace for foam and splashing. It matters.
02 Next, document operating conditions: viscosity at process temperature, density, solids content, and whether ingredients change during mixing. A thin liquid and a shear-thickening slurry can demand very different torque, even in the same tank. Ask suppliers to size for the hardest real condition, including startup with a settled or cold batch. Lab results help, but they do not perfectly predict scale-up. That is an uncertainty worth stating.
03 Check duty cycle, batch time, cleaning needs, and available power before choosing motor capacity. The U.S. Department of Energy’s 2002 U.S. Industrial Electric Motor Systems Market Opportunities Assessment estimated that motor-driven systems accounted for about 63% of industrial electricity use. That figure covers industry broadly, not mixers alone, but it underlines why oversizing deserves scrutiny. Compare expected torque and power across the operating range, then verify the proposed impeller and speed with a process trial where possible. A spreadsheet is useful. It is not proof.
Compare Construction, Controls, and Safety Features
Start with the material and batch size, then inspect the machine’s construction. A stainless-steel vessel may suit corrosive or washdown environments, but the grade, weld finish, and seal design matter. Check whether the impeller matches the task: a high-shear head disperses powders differently from a slow anchor blade. Look closely at the shaft and vessel wall. Small clearances can affect cleaning and mixing consistency. Capacity alone is not enough.
Controls should make operating conditions visible. A variable-speed drive helps operators adjust mixing without changing hardware; a timer and overload alarm can make repeat batches easier. Ask whether recipes can be locked or recorded. Safety features deserve the same scrutiny: guards, emergency stops, and interlocks should be easy to verify. OSHA estimates that effective lockout/tagout practices prevent about 120 fatalities and 50,000 injuries each year. That figure shows why service isolation matters, not just production speed. One detail is easy to miss: a control panel can be sophisticated yet awkward to clean or reach.
Tips: Before purchase, map how an operator loads, runs, cleans, and services the mixer. Test the emergency stop and confirm isolation points are accessible. Request drawings and maintenance instructions. Then review them with the people who will use the machine. Their feedback may challenge your first choice—and that is useful.
How to Choose an Industrial Mixing Machine?
Maintenance is part of the purchase price, even when it appears later on an invoice. Compare service access, wear-part availability, lubrication intervals, cleaning time, and the skills required for routine repairs. Picture a technician replacing a seal beside a warm vessel: can the job be done without dismantling half the assembly? Small design differences can mean hours of lost production.
A 2010 U.S. Department of Energy guide estimates that effective operations and maintenance programs can cut energy bills by 5–20%. That is a facility-level estimate, not a guaranteed saving for every mixer. Use it as a reason to measure motor energy, batch time, and unplanned stoppages before choosing equipment. NIST Handbook 135’s life-cycle cost method also supports comparing purchase, energy, operation, maintenance, and replacement costs over a defined period. Put those costs into one spreadsheet, using your own duty cycle.
Ask suppliers for maintenance schedules and realistic parts lead times, then price labor and downtime using your site’s figures. Include washdown water, seals, bearings, and disposal of worn parts. Keep assumptions visible. They are easy to overlook. Paper estimates may miss awkward access, sticky residues, or a seal that takes longer to change than expected. A short trial with your actual material can expose those gaps.
The figures below are indicative planning estimates in USD for representative, mid-sized equipment. Actual costs depend on material properties, duty cycle, construction materials, process requirements, and local service rates. The machine types may serve different processes, so compare them only after confirming that each can meet the required capacity and product quality.
| Evaluation dimension | Top-entry tank agitator | Inline high-shear mixer | Horizontal ribbon blender |
|---|---|---|---|
| Typical application | Liquid blending, suspension, and gentle-to-moderate agitation in a tank. | Rapid dispersion, emulsification, and particle-size reduction in a recirculating liquid stream. | Batch blending of powders, granules, and other dry or slightly moist solids. |
| Indicative purchase price | $15,000–$40,000 | $25,000–$80,000 | $30,000–$100,000 |
| Common wear or service items | Mechanical seal or packing, bearings, gearbox lubricant, coupling, and impeller. | Rotor–stator elements, mechanical seals, bearings, and elastomeric gaskets. | Bearings, gearbox lubricant, seals, discharge valve parts, and ribbon or shaft components. |
| Typical maintenance checks | Inspect for seal leakage, unusual vibration, and shaft alignment; check lubricant and fasteners according to the service schedule. | Inspect rotor–stator clearance and wear, seal condition, vibration, and pressure or temperature trends; clean product-contact areas as required. | Inspect bearings, drive, seals, and discharge gate; check for residue buildup, unusual vibration, and ribbon-to-trough contact. |
| Typical maintenance frequency | Operator checks each shift; planned inspection and lubrication typically monthly to quarterly, subject to the manufacturer’s instructions and operating conditions. | Operator checks each shift; inspect wear components and seals at intervals set by operating hours, product abrasiveness, and service guidance. | Operator checks each batch or shift; planned drive, bearing, seal, and fastener inspections typically monthly to quarterly. |
| Estimated annual maintenance labor | 8–24 hours | 16–40 hours | 12–32 hours |
| Illustrative annual maintenance budget | $1,000–$3,000, including routine labor and common service parts. | $2,000–$6,000; frequent abrasive or high-viscosity service can increase wear-part costs. | $1,500–$4,500, depending on batch frequency, dust exposure, and seal or bearing service. |
| Main cost or downtime risks | Seal failure, shaft or bearing wear, and downtime while the tank is opened or drained for repair. | Rotor–stator wear, seal replacement, and process interruption if the unit is a critical recirculation component. | Bearing or gearbox failure, product buildup, seal leakage, and downtime for cleaning or discharge-gate repair. |
| Best maintenance-fit indicator | Good access to the drive and seal, available lifting equipment, and a planned tank-cleaning window. | Quick access to replaceable wear parts, documented cleaning procedures, and spare seals or rotor–stator components on site. | Safe access to bearings and drive components, effective dust control, and a cleaning method suited to the product. |
| Cost item and modeling assumption | Top-entry tank agitator | Inline high-shear mixer | Horizontal ribbon blender |
|---|---|---|---|
| Representative purchase price | $25,000 | $45,000 | $55,000 |
| Estimated installation cost | $5,000 | $8,000 | $10,000 |
| Energy assumption | 7.5 kW motor; 70% average load | 15 kW motor; 70% average load | 11 kW motor; 65% average load |
| Modeled electricity use per year | 21,000 kWh | 42,000 kWh | 28,600 kWh |
| Electricity-cost assumption | 4,000 operating hours per year at $0.12 per kWh; 10 years of operation. | ||
| Modeled 10-year electricity cost | $25,200 | $50,400 | $34,320 |
| Modeled annual maintenance budget | $2,000 | $4,000 | $3,000 |
| Modeled 10-year maintenance cost | $20,000 | $40,000 | $30,000 |
| Illustrative 10-year total* | $75,200 | $143,400 | $129,320 |
*Total = purchase price + estimated installation + modeled 10-year electricity cost + modeled 10-year maintenance cost. This simplified comparison excludes operator labor, process materials, financing, taxes, major unplanned repairs, downtime losses, replacement equipment, and residual value. Use supplier quotations, site-specific energy rates, actual operating hours, and a maintenance plan to build a decision-grade total-cost model.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru