Choosing the right Oil Separator for industrial use is not a simple equipment purchase. It affects air quality, maintenance intervals, product protection, and operating costs. A separator that works well in a metalworking plant may perform poorly in a food-processing facility. The difference often comes from fluid type, flow rate, temperature, pressure, and contamination levels.
In practical installations, operators commonly compare stainless steel housings, coalescing elements, centrifugal designs, and high-efficiency filter systems. Each option has limits. A small separator may restrict airflow when oil mist increases. An oversized unit may waste space and provide little extra value. These details matter beside a compressor, CNC machine, or vacuum pump running continuously.
A reliable selection process begins with measured operating data. Record the oil concentration, inlet flow, particle size, and expected service temperature. Check pressure-drop ratings, drainage methods, replacement-element availability, and inspection access. Manufacturer test results can help, but field conditions deserve equal attention. Laboratory efficiency does not always match a dusty production floor.
Safety and compliance also require careful review. Confirm that the equipment suits the process and installation environment. Ask whether collected oil can be drained, reused, or disposed of through approved procedures. Material compatibility should not be assumed. Seals can swell, crack, or fail when exposed to unsuitable chemicals.
This guide explains how to compare Oil Separator technologies with practical criteria. It also highlights common selection mistakes, because even experienced teams occasionally overlook changing loads or neglected maintenance. The best choice is not always the most powerful model. It is the one that performs reliably under real operating conditions.
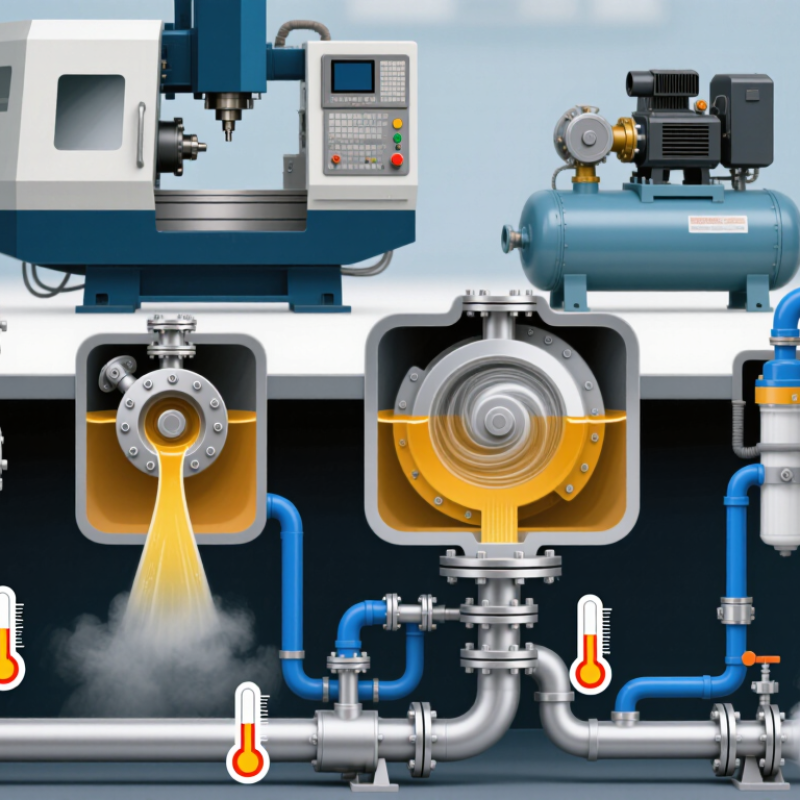
How to Choose the Right Oil Separator for Industrial Use
An industrial oil separator should be defined by its role, not its appearance. Start with the contamination problem. Is it removing free oil from wastewater, protecting a pump, or recovering reusable fluid? Each purpose requires a different separation method. Gravity units suit larger oil droplets and steady flow. Coalescing systems capture smaller droplets but need cleaner inlet conditions. Centrifugal equipment handles demanding separation tasks, although it can require more energy and maintenance.
Operating conditions determine whether the design will work reliably. Record the normal and peak flow rates, oil viscosity, temperature, pressure, and expected solids. An oily stream at 20°C behaves differently from one near 80°C. Emulsified oil may resist gravity separation and require chemical or mechanical treatment. Check tank capacity against actual retention time, not only the supplier’s nominal rating. Small details matter.
A practical inspection should include sampling during production, not only during a quiet shift. Observe sludge buildup, outlet clarity, drain frequency, and access for cleaning. One common mistake is selecting equipment from average flow alone. Peak surges can carry oil through the outlet. Another mistake is ignoring seasonal temperature changes. The specification may look correct on paper, yet performance can weaken in winter. I would also question any design that promises perfect removal without explaining testing conditions, maintenance limits, and the expected oil droplet size.
Choosing an industrial oil separator starts with measured fluid characteristics, not a catalog size. Identify whether the oil is free, emulsified, or carried as a fine aerosol. Viscosity, density, temperature, and droplet size directly affect separation performance. Compressor lubricants may also contain additives that change emulsification behavior. A practical survey should record inlet pressure, air temperature, flow rate, and operating hours.
Air purity requirements must guide the selection. ISO 8573-1:2010 classifies compressed-air oil content, with Class 1 allowing no more than 0.01 mg/m³ of total oil. The U.S. Department of Energy reports that compressed-air systems can consume 10–15% of industrial electricity. Excessive pressure drop therefore wastes energy. Select a separator using actual operating flow, not only the compressor’s nameplate capacity. Contaminants may include liquid water, rust, carbon particles, and degraded seal material. Coalescing units suit small aerosol droplets, while gravity systems work better with larger liquid drops. A neat calculation can still fail when the air warms or the load changes.
Tips: Take a fluid sample. Check viscosity and pH. Measure pressure drop before replacement. Inspect the drain during peak production. Do not assume a clear outlet means clean air; invisible oil vapor may remain. Laboratory analysis is worthwhile when discharge quality is critical. Reference data should come from ISO 8573-1:2010, ISO 12500 testing guidance, and current site measurements.
Choosing the right oil separator starts with contamination details, not catalog size. In industrial audits, I check oil viscosity, flow rate, temperature, and droplet size. These factors control filtration performance. A separator designed for heavy sludge may struggle with fine mist. It happens often.
Coalescing separators capture dispersed oil droplets by merging them into larger drops. They offer strong removal efficiency at moderate flow rates. However, dirty elements can raise pressure drop quickly.
Centrifugal separators use rotational force and handle changing loads well. Their performance may fall when droplets are extremely fine or fluids become very viscous.
Gravity chambers are simple and energy efficient, yet they need more space and settling time.
Membrane systems can achieve finer separation, but fouling and replacement costs need careful review. No technology wins every test.
For reliable selection, request test data under actual operating conditions. Ask for removal efficiency by micron range, pressure loss, drainage behavior, and service intervals. A claimed 99 percent rate means little without a defined droplet size. Inspect materials, seals, access clearance, and alarm points. I prefer a pilot trial using a real process sample. Laboratory oil can be too clean. One overlooked issue is startup flow; sudden surges may carry oil past the separator. Selection is rarely perfect on the first attempt. Record readings for several weeks, then revise the specification when evidence demands it.
Choosing an industrial oil separator starts with real operating data, not a catalogue headline. Measure peak flow, oil loading, temperature, and inlet pressure. A separator rated for average flow may flood during compressor start-up. Leave roughly 15–20% capacity margin, but avoid extreme oversizing. Oversizing can reduce capture efficiency at low flow. Check the manufacturer’s test conditions carefully. ISO 12500-1 provides a recognized method for evaluating compressed-air filter performance.
Pressure drop deserves equal attention. The U.S. Department of Energy’s Improving Compressed Air System Performance guide recommends keeping a clean filter below about 3 psi pressure loss. Replacement is commonly considered near 10 psi. That difference can create measurable energy waste across continuous operation. Use differential-pressure gauges near the inlet and outlet. Watch the trend weekly. A sudden rise may indicate oil carryover, blocked media, or excessive condensate. Small details matter.
Maintenance intervals should follow oil loading, not calendar habits. Drain systems before liquid reaches the element, inspect seals, and record pressure readings. Many separators last several years, but service life changes with temperature, aerosol concentration, and cycling. ISO 8573 testing helps define outlet air quality, yet field conditions remain less predictable. I have seen “long-life” elements fail early because drains were ignored. That is an uncomfortable lesson. Choose accessible housings, replaceable elements, and documented test results. A lower purchase price can become expensive when every inspection requires production downtime.
| Separator Type | Typical Application | Indicative Capacity Range | Typical Inlet Oil Load | Initial Pressure Drop | Oil Removal Performance* | Routine Maintenance | Expected Service Life | Best Selection Criterion |
|---|---|---|---|---|---|---|---|---|
| Coalescing Filter Separator | Compressed-air systems, vacuum equipment, hydraulic breather systems, and light oil-mist removal | 50–5,000 m³/h | Up to approximately 1,000 mg/m³ aerosol concentration | 0.05–0.20 bar when clean | Typically 95–99.9% for oil aerosols, depending on droplet size and element design | Inspect differential pressure monthly; replace the filter element when pressure drop reaches the manufacturer’s limit or performance declines | Filter element: 6–24 months; housing: 10–20 years with proper corrosion control | High-efficiency aerosol removal with moderate flow rates |
| Vane-Type Demister | Process-gas streams, separators, scrubbers, and large-volume oil mist removal | 1,000–100,000 m³/h | Approximately 0.1–10 g/m³ entrained liquid | 0.01–0.10 bar | Typically 90–99% for droplets above approximately 10–20 µm | Inspect and clean the vane pack during planned shutdowns; check for fouling, corrosion, and mechanical damage | 8–15 years; longer in clean, non-corrosive service | Low pressure drop and high gas throughput |
| Wire-Mesh Mist Eliminator | Oil vapor and mist removal from process vessels, air receivers, and gas-liquid separation equipment | 500–50,000 m³/h | Approximately 0.1–5 g/m³ entrained liquid | 0.005–0.05 bar | Typically 90–99% for droplets above approximately 5–10 µm | Clean or replace the mesh when fouling causes excessive pressure drop or liquid carryover; verify support grids | 5–15 years, depending on contamination, vibration, and material selection | Simple construction, low resistance, and easy vessel integration |
| Centrifugal Oil Separator | Machine-tool coolant systems, compressor systems, gearboxes, and high-liquid-load process streams | 100–20,000 m³/h | Approximately 0.5–50 g/m³ oil or liquid entrainment | 0.05–0.30 bar | Typically 80–98% for sufficiently large liquid droplets | Drain collected liquid regularly; inspect rotor or internal surfaces and clean deposits during scheduled service | 7–15 years; rotating components may require earlier replacement | High liquid loading and continuous self-draining operation |
| Cyclonic Separator | Heavy-duty gas cleaning, compressor discharge lines, and applications with dust or larger oil droplets | 500–30,000 m³/h | Approximately 1–100 g/m³ liquid or mixed contamination | 0.10–0.50 bar | Typically 85–98% for droplets above approximately 10–20 µm | Drain the collection chamber; inspect wear surfaces, inlet zones, and outlets for erosion or blockage | 10–20 years; lining or wear parts may need periodic renewal | Rugged operation with high contamination and liquid loading |
| Electrostatic Oil Mist Collector | Metalworking machines, machining centers, food-processing equipment, and fine oil-mist control | 500–15,000 m³/h per unit | Approximately 10–500 mg/m³ fine oil mist | 0.01–0.08 bar when clean | Typically 95–99% for fine particles, subject to electrical conductivity and particle loading | Clean collecting cells and prefilters regularly; inspect high-voltage components and safety interlocks | 5–12 years; collecting cells and power components may require replacement | Fine aerosol control where compact equipment and low airflow resistance are important |
| Activated-Carbon Oil Vapor Adsorber | Final-stage treatment for residual hydrocarbon vapor in compressed air or process exhaust | 50–5,000 m³/h | Usually below 100 mg/m³ after upstream liquid and aerosol separation | 0.05–0.25 bar when fresh | Typically 90–99% vapor reduction until the adsorption media approaches saturation | Monitor outlet concentration or hydrocarbon breakthrough; replace carbon media before saturation | Housing: 10–20 years; carbon media: approximately 3–12 months, depending on load | Removal of residual oil vapor after an upstream coalescing separator |
Choosing an oil separator starts with compliance, not catalogue capacity. Identify the oil type, flow range, temperature, and discharge destination. Then check applicable permits, safety rules, and ISO 8573-1 air-quality requirements. ISO 8573-1 defines contamination classes, but it does not approve a separator by itself. The selected unit must match the required outlet quality and documented test method.
Installation details often decide real performance. Confirm inlet and outlet sizes, maximum pressure, drain routing, ventilation, and maintenance clearance. A bypass may protect production, but it can also release untreated air or liquid. Use differential-pressure gauges and accessible sampling points. The U.S. Department of Energy reports that compressed-air leaks can waste 20–30% of compressor output, according to its Compressed Air System Performance guide. Excessive separator pressure drop can create similar operating waste. Small losses become expensive.
Calculate total cost of ownership before purchase. Include the separator, filters, valves, installation labor, disposal, energy, inspections, and replacement elements. Compare annual pressure-drop costs, not only the purchase price. A cheaper unit may need frequent element changes. That is easy to miss. The EU Joint Research Centre’s wastewater treatment BREF emphasizes application-specific design and operating control for oil removal systems. In practice, request verified efficiency data at your actual flow and viscosity. Recheck assumptions after commissioning, because real plant conditions rarely match the design sheet perfectly.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru