Choosing a Liquid Ring Vacuum Pump is rarely as simple as matching flow rate and vacuum level. The right decision depends on process gases, liquid compatibility, operating temperature, and installation conditions. A pump handling clean air may perform very differently with vapor, solvents, dust, or corrosive compounds.
This guide examines practical selection factors used by process engineers and maintenance teams. It explains how pumping speed, ultimate vacuum, seal-liquid consumption, motor power, and materials affect daily performance. For example, a stainless-steel pump may suit demanding chemical service, while cast iron can be more economical for general industrial applications. Small details matter. A poorly selected separator can increase liquid carryover, noise, and maintenance work.
Real operating experience also shows that catalog figures need careful interpretation. Rated capacity may change with seal-liquid temperature, atmospheric pressure, and gas composition. Ask for performance curves at your actual conditions, not only standard test points. Confirm the required vacuum range, because operating too close to the pump’s limit can reduce stability. It is an easy detail to miss.
Reliability should guide the final comparison. Review bearing design, mechanical seals, spare-parts availability, energy consumption, and supplier technical support. No selection method removes every uncertainty. Process data may be incomplete, and assumptions can be wrong. Therefore, validate the choice through calculations, manufacturer consultation, and, when possible, a controlled site trial. The best Liquid Ring Vacuum Pump is not always the largest or cheapest model. It is the one that delivers stable vacuum, manageable operating costs, and dependable service over time.
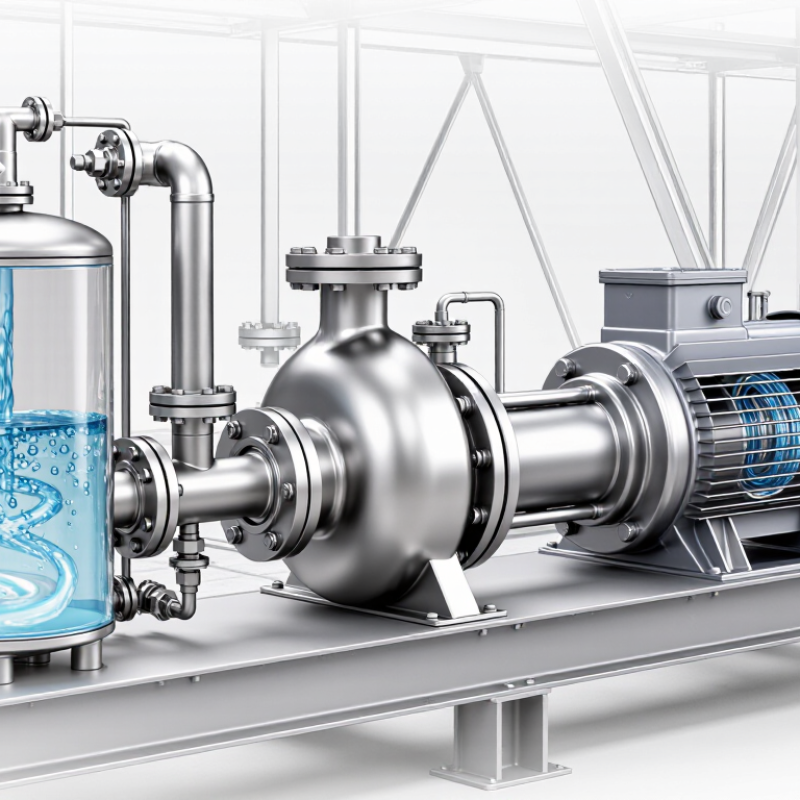
How to Choose a Liquid Ring Vacuum Pump?
Define the vacuum requirement before comparing pump sizes. State the target pressure as absolute pressure, not gauge pressure. A process requiring 100 mbar differs greatly from one requiring 20 mbar. Record the required pumping speed at that pressure, including leakage, vapor load, and non-condensable gases. ISO 21360-1 recommends standardized methods for measuring vacuum-pump performance, which improves supplier comparisons.
Operating conditions can change the result. Seal-liquid temperature is critical because higher temperature increases vapor pressure and reduces achievable vacuum. For example, water at 25°C has a vapor pressure near 31.7 mbar. At 40°C, it rises to about 73.8 mbar. The pump may appear correctly sized, yet fail to reach the target. Check liquid compatibility, inlet temperature, discharge pressure, altitude, and corrosion risks. Small details matter.
I often see energy treated as an afterthought. That is a mistake. The U.S. Department of Energy’s Industrial Motor Systems Market Assessment reports that motor systems used about 23% of U.S. electricity and roughly 70% of industrial electricity. The IEA’s Energy Efficiency 2023 report places industry near 37% of global final energy demand. Therefore, compare power at the actual duty point, not only rated motor power. My first shortcut was to prioritize ultimate vacuum. Field conditions proved otherwise. A slightly higher pressure with stable, efficient operation can serve the process better. Sometimes, imperfect data causes the largest sizing error.

How to Choose a Liquid Ring Vacuum Pump?
Material selection begins with the gas, sealing liquid, and process temperature. A pump handling humid chlorine gas needs different protection from one moving clean air. Corrosive vapors may dissolve into the sealing liquid and change its chemistry. That change can attack the casing, impeller, shaft, or mechanical seal. Stainless steel may suit mild service, but concentrated chemicals, high temperatures, or chlorides can require more resistant alloys. Confirm compatibility at the actual concentration and operating temperature. Generic charts are useful, but they are not enough.
The sealing liquid also affects vacuum performance. Its vapor pressure limits the achievable vacuum, especially in warm conditions. Process solids can score internal surfaces or block small passages. Elastomers deserve equal attention because an apparently suitable metal can still fail with the wrong seal material. In field assessments, teams often focus on the gas and overlook cleaning fluids or occasional process upsets. I have seen this assumption create premature corrosion. It is a useful reminder: normal operation is not the whole environment. Review startup, shutdown, washing, and contamination conditions too.
Tips: List every gas and liquid contacting the pump. Record concentration, temperature, pressure, solids, and cleaning chemicals. Ask the manufacturer for written compatibility guidance. Test uncertain combinations before full-scale installation. Do not guess. A small material mistake can become a large maintenance problem.
| Process Condition | Typical Gas or Vapor | Liquid-Ring / Seal Liquid | Recommended Wetted Materials | Why This Combination Is Used | Key Selection Checks |
|---|---|---|---|---|---|
| Clean, non-corrosive service | Air, nitrogen, dry process gas, water vapor with limited contaminants | Fresh or recirculated clean water | Cast iron casing with suitable stainless-steel shaft and impeller components | Cast iron is commonly used for economical service when the gas and seal liquid do not create significant corrosion risk. | Confirm water quality, dissolved oxygen, chloride level, operating temperature, and the risk of abrasive solids. |
| General industrial duty with moderate corrosion exposure | Moist air, mildly contaminated process gas, low concentrations of non-aggressive vapors | Water or a compatible process liquid | Austenitic stainless steel, commonly 304L or 316L, for wetted components | Stainless steel provides better resistance to general atmospheric and water-related corrosion than unalloyed cast iron. | 316L is generally preferred over 304L when chlorides, acidic condensate, or higher corrosion resistance are required; verify the exact chemistry. |
| Chloride-bearing or saline service | Humid air, brine vapor, seawater-related vapor, chloride-containing process gas | Low-chloride water, treated water, or seawater where specifically engineered | 316L for moderate exposure; duplex stainless steel or higher-alloy materials for more severe chloride duty | Chlorides can cause pitting and crevice corrosion in ordinary stainless steels, especially at elevated temperature or where deposits form. | Do not assume 316L is suitable for all seawater applications. Check chloride concentration, temperature, oxygen content, crevice design, and stress-corrosion risk. |
| Acidic gas or acidic condensate | Carbon dioxide with moisture, sulfur-containing gas, acidic vapors, or low-pH condensate | Water or a chemically compatible liquid maintained at a controlled pH | 316L, duplex stainless steel, nickel-based alloy, or lined construction selected from corrosion data | Acidic condensate can attack carbon steel and cast iron, while alloy selection must account for both the gas phase and the liquid phase. | Evaluate pH, acid concentration, temperature, oxidizing conditions, weld zones, and possible formation of sulfuric or carbonic acid. |
| Alkaline or caustic service | Ammonia-containing gas, alkaline vapor, or caustic process vapor | Water, dilute alkaline solution, or compatible process liquid | 316L or a higher-alloy material when concentration and temperature demand it | Many stainless steels tolerate selected alkaline solutions, but hot concentrated caustic liquids can cause corrosion or stress-corrosion cracking. | Check sodium hydroxide or potassium hydroxide concentration, temperature, residual stress, and compatibility of elastomers and mechanical seals. |
| Hydrocarbon vapor service | Solvent vapor, fuel vapor, light hydrocarbons, or refinery process gas | Water, hydrocarbon-compatible liquid, or another approved seal fluid | Carbon steel or stainless steel for metal wetted parts, with seals and elastomers selected for hydrocarbon compatibility | Metal corrosion may be manageable, but seal swelling, extraction, vapor pressure, and flammability often control the design. | Check flash point, lower explosive limit, vapor pressure, electrical classification, static control, seal material, and oxygen ingress. |
| Flammable or explosive gas | Hydrogen, methane, solvent vapor, or oxygen-enriched process gas | Non-reactive liquid selected for the process and ignition-risk assessment | Conductive metallic construction with suitable corrosion-resistant wetted alloys and a certified electrical/mechanical design | Material selection alone does not make a pump suitable for hazardous service; ignition prevention, bonding, sealing, and temperature control are essential. | Specify the hazardous-area classification, gas group, temperature class, oxygen concentration, maximum surface temperature, and required safety standards. |
| Oxygen-rich or oxidizing gas | High-purity oxygen, oxygen-enriched air, chlorine-containing gas, or other oxidizing vapor | Only a seal liquid and lubricant approved for the specific oxidizing service | Carefully selected stainless steel or compatible high-alloy materials; avoid unapproved oils, greases, and contaminated components | Oxidizing environments can greatly increase combustion and compatibility risks, even when the metal itself appears corrosion-resistant. | Confirm oxygen-cleaning requirements, ignition sensitivity, particle control, lubricant compatibility, temperature rise, and material certification. |
| Solids, crystals, or abrasive carryover | Gas containing dust, catalyst fines, salt crystals, or suspended process solids | Clean liquid with filtration or controlled blowdown | Wear-resistant metallic construction, often with stainless or hardened components, plus abrasion-resistant internal details where available | Solids can erode impeller surfaces, enlarge clearances, damage seals, and reduce vacuum performance regardless of corrosion resistance. | Specify particle size, concentration, hardness, filtration, separator design, flushing requirements, and allowable wear rate. |
| High-temperature process gas | Hot vapor, drying exhaust, sterilization vapor, or heated process gas | Water or another liquid maintained below its allowable temperature and vapor-pressure limit | Stainless steel or temperature-rated alloy construction with high-temperature seals and gaskets | Temperature affects corrosion rate, seal life, liquid vapor pressure, pump capacity, and the attainable vacuum level. | Use the actual gas inlet temperature, seal-liquid temperature, cooling capacity, thermal expansion, and materials temperature limits. |
| Sanitary or hygienic processing | Food, pharmaceutical, biotechnology, or clean-steam vapor | Potable, purified, or process-approved water | 316L stainless steel with smooth, cleanable wetted surfaces and hygienic seals | 316L and hygienic surface design support cleanability and resistance to many cleaning and process solutions. | Check surface finish, drainability, dead-leg control, elastomer approvals, cleaning chemicals, sterilization temperature, and validation requirements. |
| Seawater or high-salinity seal liquid | Marine air, humid gas, or process gas with salt entrainment | Seawater or concentrated saline water | Duplex stainless steel, super-austenitic stainless steel, nickel-based alloy, or non-metallic components where engineered | High salinity increases pitting, crevice corrosion, galvanic corrosion, and erosion-corrosion risks. | Assess velocity, stagnant zones, temperature, oxygen level, galvanic couples, biofouling, cathodic protection, and chloride concentration. |
| Process liquid must not contaminate the product | Pharmaceutical, food, electronic, or chemically sensitive process gas | Specified clean liquid or a compatible product-grade liquid | 316L stainless steel or another product-compatible alloy; use approved seals and surface finishes | The seal liquid can be carried over as entrained droplets or vapor, so its composition and cleanliness may affect product quality. | Define allowable contamination, carryover limits, liquid purity, seal-material extractables, cleanability, and separation requirements. |
Engineering note: Material recommendations are starting points, not a substitute for a corrosion-compatibility review. Final selection should use the actual gas composition, liquid chemistry, concentration, temperature, pressure, contaminants, solids content, and applicable safety requirements.
Choosing a liquid ring vacuum pump starts with the real gas load, not the catalogue headline. Record flow at the operating pressure, temperature, and altitude. ISO 21360-1:2020 recommends standardized vacuum-pump performance measurements, helping buyers compare capacity under consistent conditions. A pump rated at 1,000 m³/h may deliver much less at deep vacuum.
Vacuum level depends strongly on seal-liquid temperature. At 20°C, water vapour pressure is about 2.34 kPa absolute, limiting practical vacuum performance. Cooler liquid can improve the ultimate pressure, while warmer liquid reduces it. Check whether the process needs 200 mbar, 50 mbar, or below 30 mbar. Those are very different duties. Do not size from pressure alone. Gas composition matters too.
Energy consumption deserves equal attention. The U.S. Department of Energy reports that pumping systems can represent about 25% of industrial electricity use in some facilities, although this figure covers broader pumping applications. Measure motor input against actual throughput, using kWh per 1,000 m³ as a working comparison. A smaller pump may consume less power, but it can run continuously at its limit. A larger pump may waste energy through throttling. That trade-off is easy to miss. ISO test conditions also differ from plant conditions. In practice, temperature, leaks, and partial-load operation often change the result more than expected. Temperature control and leak testing should be included in the selection sheet.
Choosing a liquid ring vacuum pump starts with the process, not the catalog size. Compare single-stage and two-stage configurations against the required vacuum level, gas load, and operating hours. A single-stage pump may suit filtration or vapor handling near moderate vacuum. Two-stage designs can reach deeper vacuum, but they often require more power and closer seal-water control.
Features deserve practical attention. Check the separator, recirculation arrangement, materials, shaft sealing, and drain access. Seal-water temperature changes performance noticeably. For example, warm water can reduce capacity during a long production shift.
I have also seen oversized pumps cycle poorly, wasting energy without improving vacuum. Bigger is not always better. That assumption needs testing.
Tips: Record inlet pressure, gas temperature, seal-water temperature, and flow during real operation. Compare these measurements with the supplier’s certified performance curve. For control options, a pressure transmitter and automatic valve can stabilize vacuum when demand changes. A variable-frequency drive may reduce energy use, but it is not automatically the best choice. Minimum speed limits, motor cooling, and control response must be checked. Simple on/off control can be reliable for steady loads, while staged operation suits fluctuating demand. Leave room for manual operation during sensor faults. It matters. My preference is to automate gradually, because poorly tuned controls can create more instability than they remove.
Choosing a liquid ring vacuum pump starts with the installation, not the catalog capacity. Confirm suction pressure, gas temperature, vapor load, and required operating hours. Keep suction piping short, straight, and properly supported. Undersized piping can increase pressure loss and reduce actual vacuum performance. Verify seal-water temperature and flow at the pump inlet. Warm water can quietly reduce capacity.
Maintenance planning should include water-quality checks, separator inspection, corrosion monitoring, and scheduled mechanical-seal reviews. ISO 1607 provides recognized methods for measuring vacuum-pump performance. Use comparable test conditions when checking supplier data. The U.S. Department of Energy’s Motor Systems Market Assessment reports that motor-driven systems represented about 70% of manufacturing electricity use. Energy efficiency deserves attention. Still, water consumption and wastewater treatment can change the result.
Safety verification should follow a documented machinery risk assessment under ISO 12100. Check guarding, isolation points, discharge routing, noise, and protection from hot seal water. Total cost includes electricity, water, spares, labor, downtime, and disposal. I have seen a low purchase price become expensive after repeated seal failures. That assumption may be incomplete. Recheck lifecycle calculations with measured flow, operating pressure, and local utility rates. Leave room for uncertainty.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







