7 Tips for Choosing the Right Precast Magnet?
Choosing the right Precast Magnet can determine whether a formwork setup feels secure or quietly becomes a production risk. A small magnet may look efficient on a sales sheet, yet fail against vibration, uneven steel, or repeated handling. The real choice depends on holding force, surface contact, dimensions, release design, and daily working conditions.
“Magnet selection should begin with the mould, not the catalogue,” says Markus Reiter, a precast-formwork specialist. His advice is practical. A 450-kilogram holding rating does not guarantee performance on dusty, painted, or slightly curved steel. Contact quality matters. So does the magnet’s position beneath the form. This guide examines seven useful tips, from calculating realistic loads to checking corrosion resistance and maintenance access. It also considers safety margins, production speed, and long-term replacement costs.
Details matter.
I have seen teams choose the strongest available unit and still struggle with removal. Excessive force can slow workers, damage equipment, or encourage unsafe shortcuts. A weaker model may be suitable for a light divider, but not for a vibrating table producing heavy wall panels. The “best” Precast Magnet is rarely the largest one. It is the model that matches the mould, concrete process, steel condition, and operator routine. No checklist is perfect. However, a careful comparison can expose weak assumptions before they become expensive defects. When specifications seem unclear, request test data, installation guidance, and a realistic demonstration using your own formwork.
What Is a Precast Magnet and How Does It Work?
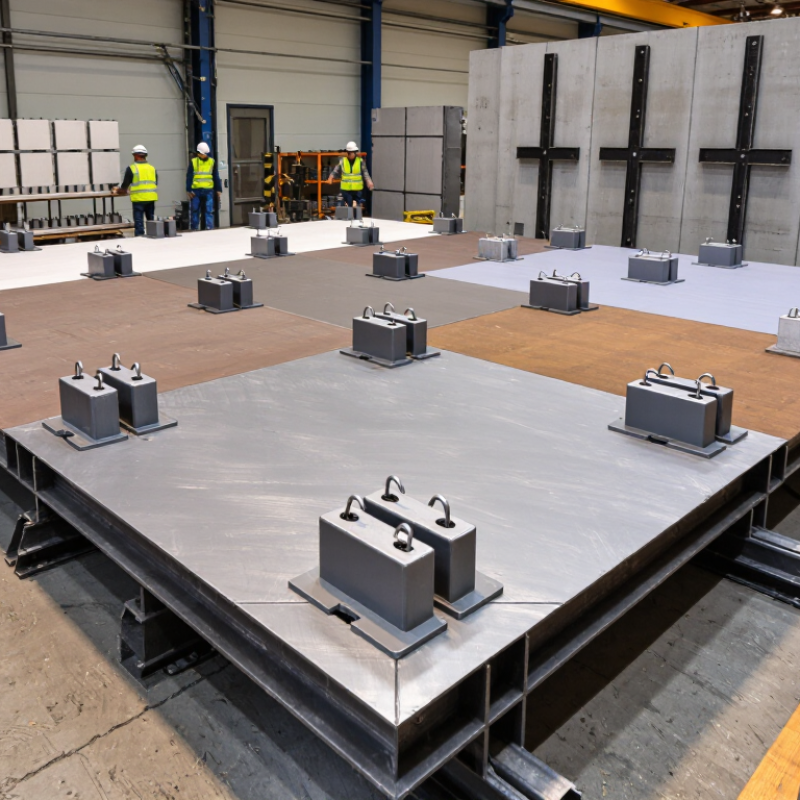
A precast magnet is a reusable fixing device for concrete molds. It usually contains permanent magnets inside a steel housing. A lever activates or releases the magnetic force. When the magnet touches a steel form table, its force travels through the base plate and creates a firm hold. This keeps threaded inserts, edge forms, and lifting anchors stable during concrete placement and vibration.
The right magnet depends on seven practical checks: holding capacity, contact area, mold thickness, insert size, vibration level, release method, and surface condition. A clean, flat steel surface gives better magnetic contact. Dust, rust, paint, or small gaps can reduce the holding force sharply. Do not judge strength by appearance alone. Check the rated capacity and leave a sensible safety margin. A site pull test is useful, but it should not replace the manufacturer’s technical data or your workplace procedure.
During use, keep the magnet aligned and fully seated. Remove concrete residue before it hardens. Inspect the lever, housing, and contact plate for damage. I once underestimated how quickly thin residue could weaken contact. That mistake is easy to repeat. Magnets can also shift when workers drag reinforcement across the mold. Marking their positions helps, although marks alone are not enough. Regular inspection, careful handling, and suitable storage make the working system more reliable.
How to Evaluate Magnetic Holding Force and Load Capacity
7 Tips for Choosing the Right Precast Magnet
How to Evaluate Magnetic Holding Force and Load Capacity
Choosing a precast magnet starts with understanding its real holding force. A rated value is not always the usable load capacity. Test results may assume clean, flat steel with perfect contact. In a precast plant, form oil, rust, weld marks, and concrete dust can create an air gap. Even a small gap can reduce magnetic performance. Ask for pull-off data, test conditions, and temperature limits. Do not guess.
Separate vertical pull from shear and peel forces. A magnet may resist direct lifting well but slide under sideways pressure. Vibration, form movement, fresh concrete pressure, and repeated use also affect performance. Use a suitable safety factor based on the application and applicable engineering requirements. Never treat holding force as the safe working load. A calibrated force gauge can provide useful site evidence.
I once focused too much on a laboratory rating and overlooked dried concrete on the steel plate. The magnet shifted during a positioning check. It was a useful warning. Inspect contact surfaces before every pour, confirm full seating, and check the locking mechanism. Record test results and unusual movement. If failure could cause injury or damage, add an independent restraint. Real conditions are often less perfect than the brochure.
7 Tips for Choosing the Right Precast Magnet
Compare nominal magnetic holding force with the recommended working load. The working-load values below apply a 3:1 safety factor to representative pull-test results on clean, flat steel surfaces. Actual capacity can be reduced by air gaps, rust, paint, thin formwork, concrete vibration, and uneven contact.
Evaluation guidance: Select a magnet whose working-load capacity exceeds the required formwork load, then verify the result with site-specific testing and the manufacturer's technical documentation.
What Environmental and Design Factors Should You Consider?
7 Tips for Choosing the Right Precast Magnet
What Environmental and Design Factors Should You Consider?
Precast magnets work best when their surroundings and design loads are understood together. Tip 1: Check moisture exposure. Wet production areas, standing water, and repeated washing can accelerate corrosion. Tip 2: Review temperature changes. Extreme heat may weaken some components, while freezing moisture can damage poorly protected parts. Tip 3: Consider dust and concrete residue. Fine particles can prevent full contact with the steel formwork. Small gaps matter.
Tip 4: Match the magnet’s holding force to the form design, panel weight, and vibration level. Too little force may cause movement during casting. Too much force can complicate removal and increase handling risks. Tip 5: Measure the formwork thickness and contact area. Uneven surfaces, coatings, and curved edges can reduce magnetic performance. Tip 6: Allow practical access for positioning and release. Workers should not need awkward tools or excessive force. Good design saves time.
Tip 7: Check compatibility with reinforcement, embedded parts, and planned recesses. Crowded steel layouts may limit placement options. I have seen magnets selected correctly but installed too close to an edge. The result was avoidable shifting. Recheck drawings on the production floor, not only on a screen. Test one assembly under real vibration, cleaning, and temperature conditions before wider use. Field experience can expose assumptions that specifications miss.
How to Compare Quality, Safety, Cost, and Supplier Support?
Choosing a precast magnet requires more than checking its price. Compare seven points: rated pull force, steel contact, load direction, coating, release mechanism, documentation, and support. A useful test records performance on clean, flat steel, not only the supplier’s strongest laboratory result. PCI MNL-116 stresses controlled production and reliable handling practices for precast components, but magnet specifications still need careful verification.
Safety deserves practical attention. OSHA recorded 93 construction struck-by fatalities in 2022, while the U.S. Bureau of Labor Statistics reported 1,075 construction deaths in 2023. Inspect the housing for cracks, confirm the locking action, and check whether workers can release the magnet without placing fingers beneath a panel. Ask for inspection intervals and replacement criteria. Small details matter.
Cost comparison should include cleaning, downtime, damaged forms, and replacement parts. A lower purchase price may become expensive after repeated failures. Request test reports, material details, warranty terms, delivery records, and training support. Supplier response time also matters when a production line stops. My checklist is not perfect. Real site conditions can expose weaknesses that paperwork misses. A short trial under normal temperature, dust, lifting angles, and concrete cycles often reveals more than a sales sheet.