Choosing a Spray Gun in 2026 requires more than comparing prices, nozzle sizes, and online ratings. The right tool must match the coating, compressor, surface, workspace, and operator’s technique. A glossy automotive panel demands different atomization from a cabinet, wall, or industrial frame. Small details matter. Tip size, cup position, air consumption, and cleaning time can change the final finish.
Industry data supports a careful approach. The U.S. Environmental Protection Agency identifies high-volume, low-pressure technology as a practical method for improving coating transfer efficiency. Several U.S. air-quality rules use approximately 65% transfer efficiency as a benchmark for compliant spray application. That figure does not guarantee a perfect finish, but it highlights the value of controlled atomization. MarketsandMarkets also reported continued growth in the global paints and coatings sector, driven by automotive, construction, and industrial demand. More coatings mean more equipment choices, not automatically better decisions.
This guide examines the evidence behind those choices. It considers HVLP, LVLP, and conventional Spray Gun designs, while comparing air requirements, overspray, pattern control, and maintenance. Professional experience still matters. A specification sheet cannot show how a gun feels after three hours, or how quickly its passages clog. I would not claim one model suits everyone. That would be convenient, but inaccurate. Even strong industry reports often combine very different applications. Your material data sheet, compressor performance, and test panel should therefore remain decisive. A controlled test on scrap metal can reveal more than a confident product description.
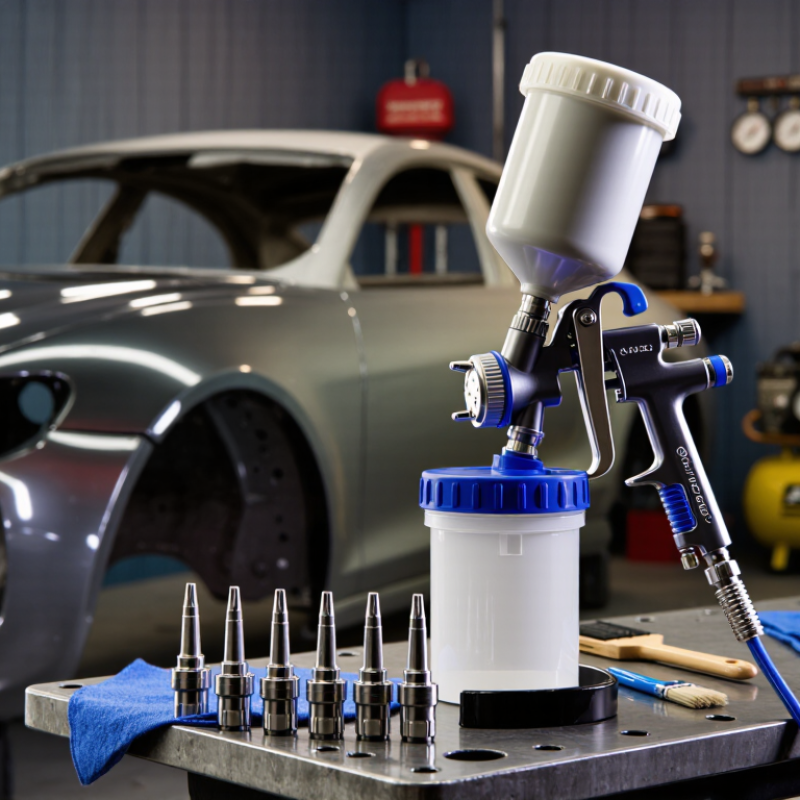
Define the project before choosing the gun. A kitchen cabinet needs controlled atomization and a clean finish. A steel frame may need faster coverage and thicker materials. Record the coating type, viscosity, surface size, target film thickness, and daily spray time. Do not choose by pressure range alone. Tip size, fluid delivery, air consumption, and operator comfort must work together.
The U.S. EPA’s AP-42 surface-coating data estimates conventional air spray transfer efficiency at roughly 20–40%. HVLP systems can reach about 40–65%, depending on setup and technique. That difference affects material waste, cleanup, and production cost. Check your compressor’s actual output, not its advertised peak rating. A small compressor may sound adequate, then struggle after two minutes. I have seen uneven fan patterns caused by poor air supply, not a defective gun. That mistake is easy to make.
Tips: Test the coating on scrap material first. Measure viscosity with a simple flow cup. Start with the lowest workable pressure. Watch the fan edges for dry spray. Keep notes on nozzle size, pressure, distance, and passes. The U.S. EPA data is useful, but real transfer efficiency changes with technique, booth airflow, coating solids, and gun adjustment. A perfect specification can still fail in an inexperienced hand. Test, record, and revise.
How to Choose a Spray Gun in 2026?
In 2026, choosing a spray gun starts with the coating, not the tool’s appearance. The right match improves finish quality, material control, and working speed. Thin stains, dyes, and clear finishes usually suit HVLP or LVLP guns with smaller fluid tips. They provide gentle atomization and help reduce excessive overspray. Medium coatings, including many primers and lacquers, need adjustable air pressure and a suitable nozzle size. Thick paints may require an airless or air-assisted airless gun. These systems handle higher viscosity, but they can create more overspray. Surface protection remains essential.
Tips: Check the coating label and technical data sheet before selecting a tip. Stir the material thoroughly, then strain it if recommended. Test one small panel first. Watch the fan pattern, wetness, and edge coverage. Keep the gun perpendicular and move at a steady speed. Measure twice.
Application conditions also influence the best choice. A cabinet in a workshop may benefit from HVLP control and a fine fan pattern. A large wall or exterior surface may need airless speed and fewer refills. For detailed furniture, a smaller cup can improve balance and reduce wrist fatigue. I have sometimes chosen a fine nozzle for a thick coating, expecting a smoother finish. It only caused dry spray and extra cleaning. That mistake still reminds me to test viscosity, pressure, and distance together. Read the spray gun’s instructions carefully, record successful settings, and adjust them when temperature or humidity changes.
Choosing a Spray Gun in 2026
Choosing a spray gun starts with the work, not the price. I measure the coating’s viscosity, surface size, and desired finish before adjusting the air controls. A small nozzle around 1.0–1.3 mm suits thin finishes and controlled detail. For primers or heavier coatings, 1.5–2.0 mm usually provides better fluid flow. The exact size still depends on the coating instructions. That detail matters.
Air pressure needs measured adjustment, not a guess. I begin near the recommended range, then spray a test pattern on cardboard. Too little pressure creates spits and uneven edges. Too much air wastes material and can dry the surface before leveling. A clean, oval pattern with soft edges is a useful target. Keep the gun about 15–20 cm from the surface. Move before pulling the trigger. I sometimes move too quickly. That mistake creates thin bands.
Fluid delivery should match the job’s speed and shape. Open the fluid control gradually for broad panels, but reduce it around narrow corners. A slower pass may improve coverage, although it can also cause runs. Watch the wet edge under angled light. This is practical evidence, not a perfect rule. Temperature, humidity, and thinning can change the result. Record the nozzle, pressure, and pass speed after each test. My notes are often incomplete, but they reveal repeatable settings over time.
| Spray Gun / Use Case | Recommended Nozzle Size | Typical Air Pressure at Gun | Typical Fluid Delivery | Suitable Materials | Best Starting Adjustment |
|---|---|---|---|---|---|
| Detail and touch-up work | 0.8–1.0 mm | 15–25 psi / 1.0–1.7 bar | 50–150 mL/min | Thin coatings, stains, dyes, small repair areas | Use a narrow fan and low fluid flow to limit overspray. |
| General-purpose HVLP finishing | 1.2–1.4 mm | 20–30 psi / 1.4–2.1 bar | 100–250 mL/min | Clear coats, basecoats, sealers, thin-to-medium paints | Begin near 25 psi and increase air only until the pattern is fully atomized. |
| Low-pressure LVLP finishing | 1.3–1.5 mm | 15–25 psi / 1.0–1.7 bar | 100–300 mL/min | Automotive coatings, furniture finishes, general maintenance paint | Keep the gun close to the recommended distance and use steady passes. |
| Conventional high-pressure spraying | 1.4–1.8 mm | 35–50 psi / 2.4–3.4 bar | 150–400 mL/min | General industrial coatings and larger surfaces | Use adequate ventilation and avoid excessive pressure that increases overspray. |
| Primer and surfacer application | 1.7–2.2 mm | 20–35 psi / 1.4–2.4 bar | 200–450 mL/min | High-build primer, surfacer, filler primer, thick protective coatings | Strain the material carefully and apply several controlled coats instead of one heavy coat. |
| Thick latex or water-based paint | 1.8–2.5 mm | 25–40 psi / 1.7–2.8 bar | 250–600 mL/min | Wall paint, acrylic coatings, thicker water-based finishes | Follow the coating manufacturer’s thinning instructions; do not rely on pressure alone. |
| Large-area production spraying | 1.6–2.0 mm | 25–40 psi / 1.7–2.8 bar | 250–500 mL/min | Furniture panels, machinery, doors, broad flat surfaces | Choose a wider fan, maintain consistent overlap, and verify compressor airflow capacity. |
How to Choose a Spray Gun in 2026?
Compare Power Sources, Transfer Efficiency, and Material Use
Choosing a spray gun starts with its power source. Pneumatic models offer fine control, but they need a clean, stable air supply. Electric models are easier to move and set up. Battery-powered options improve mobility, though runtime can limit larger projects. I check the compressor’s delivered airflow, not only its advertised pressure. That number reflects real working conditions better.
Transfer efficiency shows how much coating reaches the surface instead of becoming airborne mist. High-volume, low-pressure systems can reduce overspray when the operator keeps the correct distance. A practical starting point is 15 to 20 centimeters from the surface. Move steadily, and overlap each pass by about half. Too much pressure creates waste. Too little pressure may produce an uneven finish.
Material use also depends on nozzle size, viscosity, and preparation. I measure the coating before and after a test panel. This reveals consumption more honestly than relying on specifications. My first comparison was flawed because I ignored cleanup material and test losses. That mistake changed the final cost. Thin coatings may need a smaller nozzle, while thicker materials often require more flow. Test first. Small adjustments matter. A reliable choice balances finish quality, portability, air demand, and measurable material savings.
Check Ergonomics, Maintenance Needs, Compatibility, and Budget
A spray gun should feel balanced after several minutes of use. Hold it with your normal grip, then test the trigger travel. Fit matters. A heavy front end can strain your wrist, especially during overhead work. Look for reachable controls and a handle that does not pinch your fingers. In workshop trials, small comfort problems often become major fatigue problems.
Maintenance affects both finish quality and service life. Check how easily the air cap, nozzle, and fluid passage can be removed. A gun that needs specialized tools may discourage proper cleaning. That mistake creates uneven spray patterns. Keep it simple. Use the cleaning method recommended for the coating and gun materials. Inspect seals regularly, because softened seals can cause leaks and inconsistent pressure.
Compatibility requires more than matching a nozzle size. Confirm the gun suits your coating thickness, compressor output, working pressure, and container connection. Water-based and solvent-based materials may require different cleaning routines. Read the technical data sheets carefully. Budget for filters, replacement seals, cleaning tools, and occasional nozzle wear. The cheapest purchase is not always the lowest cost. Still, expensive features can be unnecessary for light, infrequent projects. I would reconsider my choice after each job, because real handling often reveals weaknesses that specifications hide.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru