A Die Cutting Machine turns flat materials into repeatable shapes with controlled pressure and a precisely engineered cutting tool. It may process paper, labels, cartons, foam, rubber, leather, or thin plastic. In a typical flatbed system, a die board carries sharp steel rules. The machine presses this tooling against the sheet, creating cuts, creases, perforations, or embossing in one controlled cycle.
The process looks simple. It is not. Material thickness, grain direction, die clearance, pressure, and waste removal all influence the final result. Rotary machines use cylindrical dies and continuous web feeding, while flatbed machines suit many short and medium production runs. Operators still inspect edges, registration marks, and stripped waste beside the press. Small setup errors can produce crushed corners, incomplete cuts, or expensive material loss.
Industry research shows why this equipment remains important. Smithers’ report, The Future of Die-Cutting to 2028, examines demand across packaging, labels, and converting applications. Grand View Research’s Die Cutting Machine Market Size, Share & Trends Analysis Report also identifies automation, digital controls, and packaging demand as major market influences. These reports provide useful direction, but they cannot replace production-floor testing. Every substrate behaves differently. A paperboard carton may cut cleanly at one setting, while recycled stock needs another. This article explains what a Die Cutting Machine is, how its tooling and drive systems work, and which operating factors affect accuracy, speed, safety, and cost. The goal is practical understanding, not a perfect shortcut.
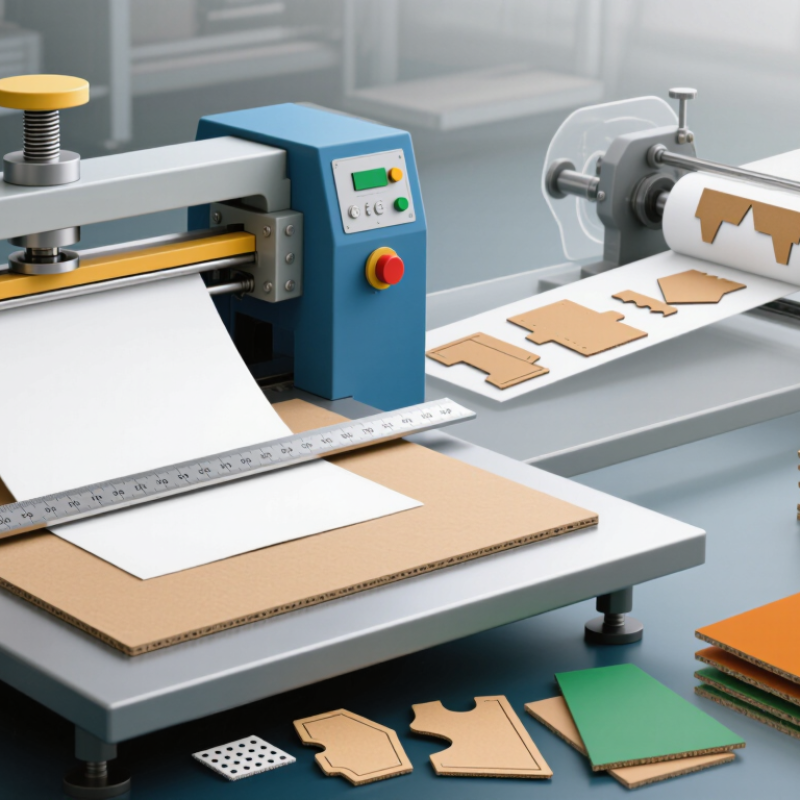
A die cutting machine is industrial equipment that cuts, creases, or perforates sheet materials into repeatable shapes. It uses a shaped die, pressure, and controlled feeding. Common materials include paperboard, corrugated board, labels, foam, and thin plastics. The die may be flat or cylindrical, depending on the production line and material thickness.
The process is precise. A sheet enters the machine, aligns against guides, and passes beneath the cutting station. Pressure pushes the die through the material, while creasing rules form fold lines without cutting completely through. Waste stripping can then remove the surrounding material. In practical production, poor alignment can leave rough edges or incomplete cuts. Small changes in pressure matter.
According to Grand View Research, the global packaging machinery market was valued at approximately USD 52.83 billion in 2023, with continued growth expected through 2030. Smithers also reports sustained demand for printed packaging and more efficient converting processes. These trends help explain why die cutting remains important in packaging production. It supports consistent shapes at higher volumes and reduces manual handling.
Yet, the machine is not automatically efficient. Tooling cost, setup time, material grain, and operator skill affect real output. A technical data sheet may promise high speed. Actual performance can be lower. That gap deserves careful measurement.
A die cutting machine shapes paper, film, foam, or thin board with a prepared die. Its main parts work together under controlled pressure. The frame supports the entire machine and keeps the cutting area stable. A flatbed platen presses the material against the die. Rotary models use two cylinders instead. The die contains sharp raised rules for cutting and creasing. Some dies also include rubber strips that lift the material after each stroke.
The feed table guides sheets into position. Rollers or grippers control movement and reduce shifting. A pressure adjustment system sets the force for different materials. Too little pressure leaves incomplete cuts. Too much pressure can damage the cutting plate or crush delicate stock. The cutting plate sits beneath the material and protects the platen. Sensors and a control panel help operators manage speed, alignment, and safety stops. In daily production, even a clean machine can produce uneven results when the die is slightly worn.
Tips: Check alignment before running a full batch. Use a small test sheet first. Examine corners, fold lines, and small openings closely. Keep the cutting plate flat and replace it when grooves become deep. Do not ignore unusual noise. It may indicate loose hardware or uneven pressure. I have found that careful setup often saves more material than increasing machine speed. Still, results can vary with humidity, material thickness, and operator judgment. Record successful settings, but question them when the material changes.
What Is a Die Cutting Machine and How Does It Work?
A die cutting machine shapes paperboard, labels, foam, or thin plastic with a formed cutting tool. The process resembles a powerful cookie cutter, but registration must stay extremely precise. Smithers reports that the global packaging market may grow from about $1.17 trillion in 2023 to $1.33 trillion by 2028. That growth increases pressure for faster, repeatable converting.
The die cutting process starts with artwork preparation and material testing. Operators check grain direction, thickness, moisture, and surface coating. A feeder then places each sheet or web into the cutting area. Side lays and sensors align the material before the die closes. Pressure forces the blade through the substrate, while creasing rules create controlled folding lines. The machine may then strip waste and separate finished pieces.
Keep it flat.
Flatbed systems suit short runs and detailed work. Rotary systems support continuous production at higher speeds. Grand View Research values the global packaging machinery market at roughly $52.8 billion in 2023, with continued growth forecast through 2030. The figure reflects broad machinery demand, not die cutting alone. That distinction matters.
Quality staff inspect cut edges, fold accuracy, and registration. Small errors matter. A crushed edge can weaken a carton during packing. In practice, the first sheet is rarely perfect, especially after a tool change. Experienced operators adjust pressure gradually instead of forcing one setting. They record waste, downtime, and dimensional results, although production records are sometimes incomplete. That weakness deserves attention. Consistent measurement remains the safest way to improve the next run.
| Step | Process Stage | What Happens | Main Equipment or Tool | Typical Output or Control Point |
|---|---|---|---|---|
| 1 | Material Selection | The operator selects a sheet, roll, or web material according to the required thickness, flexibility, surface finish, and product function. | Material specification sheet, caliper, weighing scale | Consistent material thickness and suitable tensile strength; common materials include paperboard, corrugated board, foam, rubber, gasket sheet, film, and thin plastic. |
| 2 | Artwork and Tooling Design | The product outline is converted into a cutting layout. Cutting lines, crease lines, perforations, stripping areas, and registration marks are defined. | CAD software, die layout, steel-rule die, rotary die, or digital cutting file | The cutting path matches the final dimensions, grain direction, material thickness, and required fold or tear behavior. |
| 3 | Machine Setup | The die, cutting plate, anvil, feed system, guides, sensors, and waste-removal components are installed and aligned. | Flatbed press, rotary die cutter, digital cutter, registration system | Correct tool alignment, safe clearances, stable feeding, and accurate registration before production begins. |
| 4 | Material Feeding | The material is positioned beneath the die or passed continuously through the rotary cutting station. Guides or optical marks help maintain alignment. | Feeder, conveyor, unwind unit, nip rollers, side guides, registration sensor | Stable feed rate and repeatable positioning; misalignment can cause dimensional errors or incomplete cuts. |
| 5 | Cutting, Creasing, or Perforating | Pressure forces the cutting rule through the material. Creasing rules compress a fold line, while perforation rules create a controlled series of cuts and bridges. | Cutting die, press platen, rotary cylinder, anvil, cutting mat, or oscillating knife | Clean edges, correct cut depth, consistent crease depth, and no unwanted deformation of the finished part. |
| 6 | Waste Removal | The surrounding matrix, trim, and internal waste pieces are separated from the usable shapes. | Stripping pins, stripping board, ejector system, vacuum, waste conveyor | Finished pieces remain intact and free from excess material, while waste is collected for disposal or recycling. |
| 7 | Inspection and Adjustment | Samples are checked for dimensions, edge quality, registration, crease position, perforation performance, and surface damage. | Ruler, caliper, optical inspection system, test-fold fixture, sample checklist | Press pressure, cutting depth, feed alignment, speed, and stripping settings are adjusted if defects are found. |
| 8 | Production and Quality Control | Approved settings are used for the production run, with periodic sampling to detect tool wear, material variation, or registration drift. | Die cutting machine, production log, inspection tools, counting and stacking system | Uniform parts, controlled scrap rate, accurate counts, and documented quality results. |
| Machine Type | Operating Method | Suitable Materials | Typical Strengths | Typical Limitations |
|---|---|---|---|---|
| Flatbed Die Cutter | A flat platen presses a stationary die against the sheet or substrate. | Paperboard, corrugated board, foam, rubber, gasket materials, and laminated sheets. | High cutting force, accurate registration, and flexibility for complex shapes. | Generally slower than continuous rotary systems for very high-volume web production. |
| Rotary Die Cutter | A cylindrical die cuts material continuously as it passes between rotating cylinders. | Labels, films, tapes, flexible packaging materials, paper, and thin board. | Continuous operation, high throughput, and efficient web processing. | Tooling can be more specialized, and setup may be less economical for short runs. |
| Digital Knife Cutter | A computer-controlled knife, wheel, or scoring tool follows a programmed path without a physical die. | Foam, corrugated board, textiles, films, leather, and prototype materials. | Fast design changes, low tooling cost, and suitability for prototypes or short runs. | Cutting speed and force may be lower than a dedicated press for some thick or high-volume applications. |
| Laser Die Cutter | A focused laser beam removes or separates material along a programmed path. | Paper, film, textiles, wood-based sheets, and selected polymers compatible with laser processing. | No physical die, intricate patterns, and rapid digital changeovers. | Heat-affected edges, fumes, ventilation requirements, and material compatibility constraints. |
Note: Actual production speed, maximum material thickness, cutting force, tolerances, and scrap rates vary according to machine configuration, die design, substrate properties, part geometry, and operating conditions.
A die cutting machine uses a shaped steel rule, rotary cylinder, or flatbed press to cut repeated forms. The die presses through a sheet with controlled pressure. It can also crease, perforate, kiss-cut, or emboss the surface. The real question is not only machine capacity. Material behavior matters more.
Common substrates include paper, cardstock, corrugated board, adhesive films, thin plastics, foam, felt, rubber, and textile layers. Thin aluminum foil may also be processed, but it needs careful pressure control. PlasticsEurope reported 400.3 million tonnes of global plastic production in 2022, showing the scale of film and sheet conversion. Smithers’ The Future of Global Packaging to 2028 also identifies paperboard, corrugated materials, and flexible films as major packaging substrates. In practice, thick board can crack at folds, while soft foam may compress before cutting. Static can also pull lightweight film away from the die. Material charts can mislead. Testing is still necessary.
Tips: Check thickness, density, coating, and grain direction before production. Run a small sample first. Inspect cut edges under bright light. A clean edge should not show tearing, burrs, melted film, or crushed fibers. Reduce pressure when the backing liner shows marks. Remember, one setting rarely suits every batch. Source data: PlasticsEurope, Plastics – the Fast Facts 2023; Smithers, The Future of Global Packaging to 2028.
A die cutting machine uses a shaped tool to cut, crease, or perforate sheets and rolls. Its main types differ by motion, material handling, and production volume. The choice affects speed, waste, setup time, and finished-edge quality.
Flatbed die cutters use a reciprocating platen. They suit folding cartons, labels, foam, and short-to-medium runs. Operators can change tooling relatively easily, which helps during product testing. Rotary die cutters use cylindrical dies and continuous web feeding. They run faster and support long production cycles, especially for labels and flexible packaging. However, cylinder tooling can cost more, and poor web tension may create registration errors.
Digital die cutters use computer-controlled blades instead of traditional dies. They work well for prototypes, variable designs, and small batches. Laser systems cut without physical tooling, but heat can discolor some films or melt sensitive materials. According to Smithers’ The Future of Packaging to 2028, worldwide packaging demand is expected to exceed US$1 trillion by 2028. That growth increases pressure for faster, more flexible converting equipment.
Speed is not everything. A rotary machine may waste less material on a long run, while a digital cutter may reduce setup waste on a short run. The best selection depends on substrate thickness, tolerances, order frequency, and operator skill. Real factory results can differ from catalog figures. Humidity, worn blades, and imperfect artwork still matter. Sometimes, the cheaper process becomes expensive later.
A die cutting machine presses or rolls a shaped cutting tool through sheet or web material to produce repeatable forms. The general process is material feeding, die alignment, cutting or creasing, waste removal, and finished-part collection.
The chart compares common machine configurations. A value of 1 means the feature is typical of that machine type, while 0 means it is not typical. Flatbed machines use a reciprocating flat die and are commonly sheet-fed. Rotary and semi-rotary machines use cylindrical dies for continuous web production. Digital cutters use a programmable blade or tool instead of a physical die and are suited to short runs, prototypes, and variable designs.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru