Choosing the right Wear Plate in 2026 requires more than comparing hardness numbers or low quotations. Global buyers face different operating conditions, supply risks, and inspection requirements. A plate used in a quarry truck differs from one installed inside a cement chute. Abrasive stone, wet slurry, heat, and impact can change performance quickly.
This guide introduces practical ways to evaluate Wear Plate for international purchasing decisions. It considers abrasion resistance, impact toughness, plate thickness, welding behavior, and service temperature. It also explains why chemical composition and heat treatment deserve careful review. A high-hardness grade may resist sliding wear well, but it can crack under repeated impact. That detail is easy to miss.
Reliable selection begins with real working data. Buyers should record material size, drop height, contact pressure, operating temperature, and expected service hours. Supplier experience also matters. Ask for mill certificates, test reports, traceability records, and previous project references. A clear report is useful, but it should not replace independent verification. Samples and small trial sections often reveal problems before a full shipment arrives.
There is no universal best grade. Sometimes, a slightly softer plate performs better because it tolerates impact and repairs. In other cases, a premium alloy reduces shutdown time enough to justify its cost. I have seen specifications look perfect on paper, yet installation revealed distortion or difficult welding. That is why buyers should challenge assumptions, compare field evidence, and review results after service. This approach supports dependable sourcing, safer maintenance, and more predictable lifecycle costs across global markets.
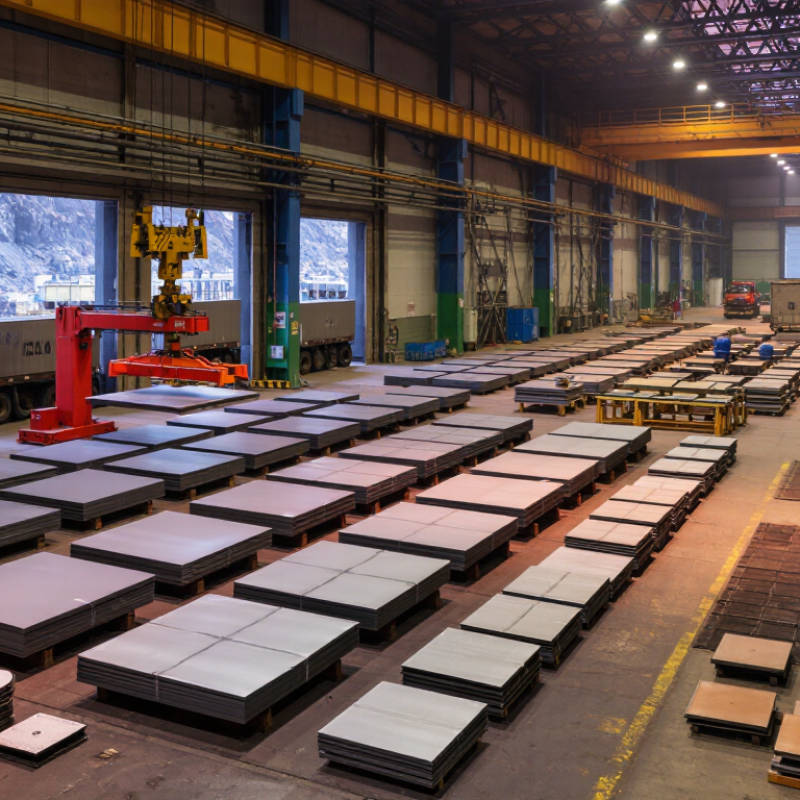
Wear plate is steel designed to resist surface loss from abrasion, impact, or sliding materials. Manufacturers strengthen it through alloying, heat treatment, or a hardened surface layer. It is commonly used in mining chutes, quarry hoppers, conveyor liners, dump bodies, and recycling equipment. The plate does not prevent wear completely. It slows damage and protects the supporting structure.
For global buyers, wear plate matters because material failure can stop an entire production line. A cracked liner may release sharp fragments, damage nearby parts, or require urgent replacement. Plate selection should match the actual wear pattern. Abrasion-resistant plate suits sliding rock, while impact-heavy service may require a tougher grade. Hardness alone can mislead. A harder plate may perform poorly when repeated impact causes cracking.
Buyers should review thickness, hardness range, chemical composition, impact data, weldability, and test certificates. Ask how samples were tested, not only for a stated value. Check tolerances carefully. A small thickness variation can affect bending and installation. Shipment distance also matters. Moisture protection, packing strength, and document accuracy reduce receiving problems. Regional standards may differ, so technical teams should confirm requirements before ordering. A common mistake is choosing the longest advertised service life without examining operating conditions. Dust, temperature, loading speed, and maintenance habits can change results. No selection is perfect. Good decisions come from measured conditions, traceable data, and honest review after use.

2026 How to Choose Wear Plate for Global Buyers?
How to Match Wear Plate Grades to Operating Conditions
Global buyers should match wear plate grades to the wear mechanism, not a catalog hardness number. The USGS Mineral Commodity Summaries 2024 recorded about 2.5 billion metric tons of mined iron ore worldwide in 2023. That scale reflects severe handling in chutes, hoppers, and transfer points. Yet abrasion is only one variable. Impact, moisture, temperature, and plate support can change service life dramatically.
For sliding abrasion, compare certified ASTM G65 volume-loss results. Lower loss is generally better. For impact-heavy loading, prioritize toughness and weldability. Hardness alone can mislead. Worldsteel reported 1.89 billion tonnes of crude steel production in 2023. Recycled feed can vary sharply. A crusher receiving oversized rock needs a different balance than a conveyor carrying damp fines.
Start with particle size, drop height, moisture, temperature, liner thickness, and failure photographs. A field trial beside the current plate is often more honest than a brochure. It may show a 500-Brinell-class plate cracking around bolt holes, while a slightly softer grade bends and lasts longer. That finding is inconvenient. Require heat numbers, test certificates, and welding guidance. Review wear loss after a defined tonnage. ASTM G65 helps, but it cannot reproduce every mine’s impact pattern.
When global buyers compare wear plate, hardness is only the starting point. A harder plate may resist sliding abrasion, but it can crack under impact or during welding. Compare the hardness range, not one attractive number. Ask for the test method, sampling location, and certified results. These details expose weak comparisons.
Impact toughness matters when rocks, scrap, or frozen material strike the surface. Check impact data at the service temperature, especially for outdoor equipment. Chemistry also deserves attention. Carbon equivalent affects weldability, while alloy balance influences toughness and heat-affected zones. In my field experience, a plate that survives the first month can still fail after poor repair welding. That lesson is easy to forget.
Compare thickness tolerance, flatness, and surface condition before ordering large quantities. A rough surface may hide laminations, grinding marks, or localized soft spots. Check through-thickness consistency when the plate becomes a liner. Formability is another practical property. A plate may meet hardness targets yet resist bending around a small radius. Ask for recommended preheating, cutting limits, and welding procedures. Do not rely only on a catalog table. Supplier traceability, batch records, and independent inspection improve confidence. Still, inspection is not magic. A few test coupons cannot represent every corner of a large plate. Match the test plan with actual load, temperature, impact angle, and maintenance conditions.
Typical comparison of commonly specified wear-resistant steel plate categories
| Wear Plate Category | Typical Hardness | Typical Yield Strength | Typical Tensile Strength | Typical Elongation | Relative Abrasion Resistance | Fabrication Characteristics | Recommended Applications |
|---|---|---|---|---|---|---|---|
| AR400-class quenched and tempered plate | Approx. 360–440 HBW | Approx. 900–1,100 MPa | Approx. 1,200–1,400 MPa | Approx. 10–14% | Good | Good weldability and formability compared with higher-hardness grades; preheating may be required depending on thickness, carbon equivalent, and hydrogen control. | Dump bodies, chutes, hoppers, truck beds, structural wear liners, and general material-handling equipment. |
| AR450-class quenched and tempered plate | Approx. 420–480 HBW | Approx. 1,100–1,250 MPa | Approx. 1,350–1,550 MPa | Approx. 8–12% | Very good | Moderate cutting and bending difficulty; fabrication procedures should be based on plate thickness and the manufacturer’s carbon-equivalent calculation. | Mining equipment, excavator buckets, crushers, feeders, conveyor transfer points, and high-impact liners. |
| AR500-class quenched and tempered plate | Approx. 470–530 HBW | Approx. 1,200–1,400 MPa | Approx. 1,450–1,700 MPa | Approx. 6–10% | Excellent | Limited cold forming compared with AR400; requires careful heat input, suitable consumables, controlled preheating, and hydrogen management during welding. | Severe sliding abrasion, rock-handling equipment, wear liners, impact screens, recycling machinery, and heavy-duty buckets. |
| AR600-class ultra-high-hardness plate | Approx. 560–640 HBW | Approx. 1,400–1,600 MPa | Approx. 1,800–2,100 MPa | Approx. 4–8% | Outstanding against sliding abrasion | Difficult to cut, drill, bend, and weld; normally requires specialized tools, strict heat control, and detailed fabrication procedures. | Extreme abrasion applications where long service life is more important than ease of fabrication or impact toughness. |
| Austenitic manganese steel | Approx. 180–220 HBW as supplied; may work-harden to approximately 450–550 HBW | Typically not specified as a conventional yield-strength grade | Approx. 800–1,000 MPa | Approx. 25–40% | Very good under high impact and compressive loading | Excellent toughness; difficult to machine; welding and heat treatment require procedures designed for manganese steel. | Jaw crushers, gyratory crushers, railway crossings, impact zones, and applications with repeated high-energy impact. |
| Chromium-carbide overlay plate | Overlay typically approx. 550–700 HV; base plate hardness varies | Not normally specified for the brittle overlay layer | Not normally specified for the overlay layer | Overlay is not evaluated like ductile structural steel | Outstanding against severe sliding and low-to-moderate impact abrasion | Cutting and forming are limited; overlay may contain transverse checks that relieve welding stress and are not automatically defects. | Cement plants, coal handling, steel production, power generation, dredging, and high-abrasion liners with limited impact. |
How to Choose Wear Plate for Global Buyers?
Supplier evaluation should begin with traceable evidence, not attractive brochures. The ISO Survey 2022 recorded 1,265,216 valid ISO 9001 certificates worldwide. Yet certification alone does not prove consistent wear plate performance. Ask for the certificate scope, issuing body, audit date, and manufacturing site. Confirm whether the supplier produces the plate or only trades it. A reliable supplier should provide heat numbers, mill test certificates, chemical composition, hardness results, and production records. EN 10204 Type 3.1 documentation is useful for linking each plate to its test results.
Product quality requires practical checks. Compare nominal hardness with measured values across several points. Review impact toughness, tensile strength, thickness tolerance, flatness, and ultrasonic testing when internal defects matter. The World Steel Association reported global crude steel production above 1.8 billion tonnes in 2024. This huge supply base creates choice, but also uneven process control. Request samples from different heats, not only one perfect plate. I would also inspect cut edges and surface repairs. Small defects can become large failures.
Tips: Use an independent inspection agency before shipment. Check ISO 9001, ISO 14001, and ISO 45001 certificates directly with the certification body. Ask for recent failure records and corrective actions. Do not accept “equivalent grade” without written comparison. A lower price may reflect thinner actual thickness or weaker traceability. Still, even third-party reports can miss field conditions. Review your own load, impact, temperature, and welding assumptions. That part is often overlooked.
Use nominal Brinell hardness grades as an initial product-quality screen: higher HBW values generally indicate greater resistance to abrasive wear, but may reduce formability and weldability. Buyers should verify the applicable material standard, mill test certificate, heat number traceability, chemical composition, hardness test method, and independent inspection records. Supplier quality systems such as ISO 9001 should support—not replace—product testing and certification review.
Global buyers should calculate more than the quoted price of wear plate. A practical landed-cost model includes plate price, freight, insurance, duties, cutting, machining, inspection, and installation. For a 20-ton order, a low unit price can disappear after urgent air freight or port storage charges. Use a spreadsheet with three scenarios: planned delivery, delayed delivery, and emergency replacement. My first estimate is often too optimistic. A second review catches hidden charges.
Delivery risk deserves a separate calculation. Check production capacity, material certificates, thickness tolerance, packing quality, and previous shipment performance. Ask how many days the supplier needs before loading, not only the advertised transit time. A missed shutdown window may cost more than the entire plate order. Keep a small safety stock when the equipment is critical, but avoid excessive inventory that ties up cash. Weather, customs checks, and vessel changes remain real variables.
Long-term value depends on wear life, not hardness alone. Compare expected service hours, plate thickness loss, repair frequency, and replacement labor. A plate costing 15% more may reduce downtime by 30%, if its toughness matches the impact conditions. Request test reports and verify samples through an independent inspection when the application is severe. Do not trust a perfect forecast. Abrasive type, moisture, impact angle, and operator habits can change results. Record actual wear after three months, then update the purchasing model with field data.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







