How to Buy 200x1800mm Graphite Electrode in 2026?
Buying a 200*1800mm Graphite Electrode in 2026 takes more than comparing prices. This size may suit a particular furnace setup, but the designation alone does not confirm fit. Ask suppliers to clarify the diameter, length, tolerances, and connection details before requesting a quote. Small differences matter.
This guide explains how to assess product quality, supplier capability, and total purchasing cost. It covers key specifications, including bulk density, electrical resistivity, flexural strength, and machining requirements. Request current test data and confirm which standard or grade the supplier uses. Check that the documents match the product being offered, not simply a similar item in a catalogue.
Details count. A clear product drawing can prevent confusion. So can a written inspection plan. Review packaging, transport arrangements, lead time, and replacement terms alongside the unit price. If possible, ask for recent production records or arrange an inspection before shipment. These steps do not eliminate risk, but they make decisions easier to explain and verify.
There is no single best supplier for every buyer. Furnace conditions, operating goals, delivery location, and order volume can change what matters most. A low quote may still cost more if the electrode arrives late or fails to match the agreed specification. I would not judge quality from a polished brochure alone. Compare evidence, ask direct questions, and record the answers. The process is not perfect, but careful checks can reduce avoidable surprises.
Define the 200 mm × 1,800 mm Electrode Size, Taper, and Nipple Connection
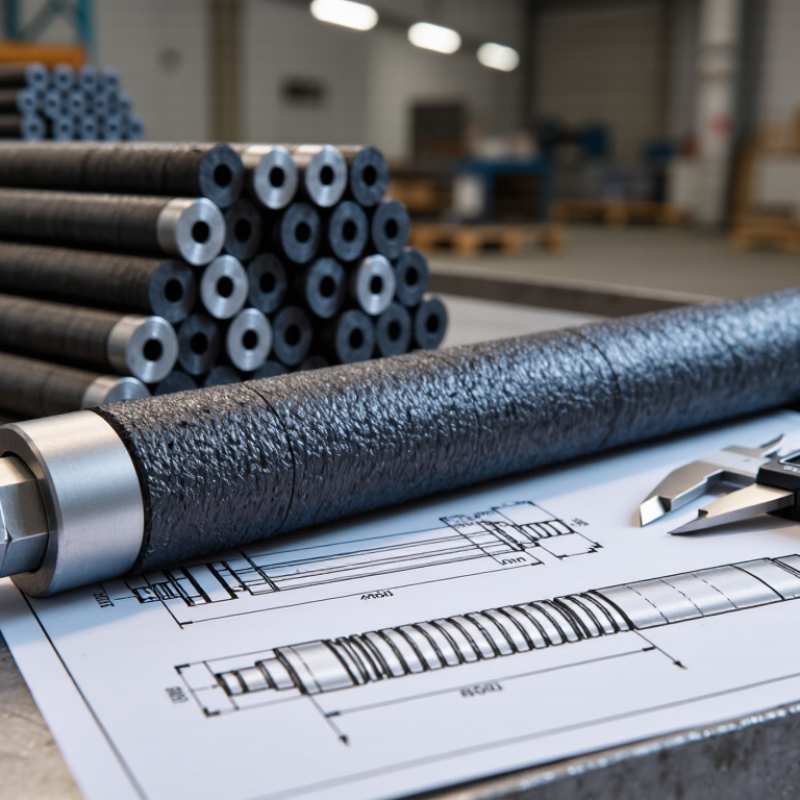
For a 200 × 1,800 mm graphite electrode, confirm what each dimension means before requesting a quotation. The 200 mm figure is the nominal diameter; clarify whether 1,800 mm means total length or usable length. Ask for the supplier’s dimensional drawing and tolerance values. Small differences matter. IEC 60239 provides dimensional designations for graphite electrodes and nipples used in steelmaking, but the purchase drawing should define the actual connection.
Specify the taper and nipple connection together. Record the taper form, thread pitch, nipple diameter, and engagement length; do not assume that similar-looking parts will fit. Check that the nipple seats without rocking and that the joint closes evenly during a trial assembly. A mismatch can cause poor contact or damage at the connection. I would not treat “200 × 1,800 mm” as a complete specification. It leaves too much open to interpretation.
There is a real industrial context for careful ordering: the World Steel Association’s World Steel in Figures 2025 reports global crude steel production of about 1.88 billion tonnes in 2024, with electric arc furnaces accounting for roughly 29%. For procurement, request material grade, bulk density, electrical resistivity, and test documentation alongside dimensions. Verify packaging and end protection on arrival. One detail is easy to miss: confirm whether the nipple is included or ordered separately.
Select RP, HP, or UHP Grade by Furnace Load: Typical 200 mm Currents of 5–12 kA
How to Buy 200x1800mm Graphite Electrode in 2026?
For a 200 × 1800 mm graphite electrode, select the grade according to the furnace’s actual electrical load, not the label alone. A 200 mm diameter commonly operates around 5–12 kA, but this is a working range, not a guarantee. Furnace design, power-on time, transformer settings, cooling, and electrode condition all affect operating limits. That matters.
RP may suit lighter-duty or intermittent operation where current and thermal shock stay modest. HP is often considered for steadier, higher loads, while UHP is intended for demanding, high-current operation. However, a higher grade cannot compensate for poor connections or unstable furnace control. Ask for verified grade data, including resistivity, bulk density, flexural strength, and current guidance for the exact diameter. Compare the 1800 mm length with holder clearance and the furnace’s required working length. Check the fit. Confirm nipple dimensions, thread type, machining tolerances, and packing protection before ordering. A small mismatch can cause delays or uneven contact. Check the 5–12 kA estimate against furnace records and technical data; actual practice varies. I would not choose UHP solely because it sounds safer.
How to Buy a 200 × 1800 mm Graphite Electrode in 2026?
Indicative operating-current ranges by grade for a 200 mm electrode
RP: 5–7 kA · HP: 6–9 kA · UHP: 8–12 kA. These are indicative ranges, not guaranteed ratings. Select a grade to suit furnace load and operating conditions; confirm allowable current with the electrode supplier’s technical data and your furnace specifications.
Compare Grade-Specific Resistivity, Bulk Density, and Flexural-Strength Data
How to Buy 200x1800mm Graphite Electrode in 2026?
When comparing 200x1800mm graphite electrodes, check the grade before comparing prices. Resistivity, bulk density, and flexural strength can differ substantially between grades. A lower resistivity generally helps reduce electrical losses, but it does not guarantee better performance in every furnace. Ask for the supplier’s current technical data sheet and batch-specific test results. Check that reported values use the same test methods.
Bulk density offers another useful comparison. Higher density can indicate a less porous structure, but density alone cannot predict service life. Flexural strength matters during lifting, installation, and operation, when electrodes face mechanical stress. Look for values stated for the exact grade, not a general product family. Small differences count.
The awkward part is that tidy tables can hide differences in testing or tolerances. Ask how the 200 mm diameter and 1,800 mm length are measured, and confirm permitted dimensional variation. Review the electrode’s end finish and connection details against your equipment. Request packaging information too; damaged edges can complicate handling. Compare like with like. If a quotation lists impressive figures without a grade or test method, ask for clarification before ordering.
How to Buy 200x1800mm Graphite Electrode in 2026? - Compare Grade-Specific Resistivity, Bulk Density, and Flexural-Strength Data
Comparison for a nominal 200 mm diameter × 1,800 mm length electrode. The figures below are commonly published grade-level specification benchmarks; confirm the applicable standard, tolerances, and test results with the supplier before ordering.
| Grade | Electrical Resistivity
(μΩ·m, maximum) | Bulk Density
(g/cm³, minimum) | Flexural Strength
(MPa, minimum) | Typical Selection Consideration | Checks for a 200 × 1,800 mm Order |
RP
(Regular Power) | 9.0 | 1.58 | 8.0 | Lower electrical and mechanical performance benchmark; consider only where furnace conditions and operating requirements are compatible. | Confirm the electrode is rated for the intended furnace duty, current, and connection system. |
HP
(High Power) | 6.5 | 1.65 | 10.5 | Intermediate grade commonly considered for higher-power operation than RP; compare operating conditions and total consumption cost. | Verify nominal diameter and length, dimensional tolerances, machining, and nipple compatibility. |
UHP
(Ultra-High Power) | 5.5 | 1.68 | 11.0 | More demanding electrical and mechanical benchmark; suitability depends on furnace design and operating practice. | Request grade-specific inspection results and confirm that the complete electrode-and-nipple assembly matches the application. |
Verify Lot Test Reports, Dimensional Tolerances, Packaging, and Breakage Terms
For a 200 × 1,800 mm graphite electrode, request a lot-specific test report—not a generic catalogue sheet. Check resistivity, bulk density, flexural strength, and the test method, sampling date, and batch number. ASTM C611 describes a method for measuring electrical resistivity in manufactured carbon and graphite articles; a reported value is useful only when its method and specimen details are clear. Small sentence. Confirm the report matches the goods being shipped.
Put dimensional limits in the purchase specification. Ask the supplier to measure diameter at several points and record total length, end-face condition, and any machining or thread details. State the permitted tolerances in millimetres; “standard tolerance” leaves room for disagreement. worldsteel reported 1.88 billion tonnes of crude steel production in 2024, a reminder that electrode supply serves a high-volume industry where repeatability matters. Still, one industry-wide figure cannot predict the quality of a particular lot.
Before dispatch, request photos showing each electrode, protective end caps, separators, and the loading arrangement. Packaging should prevent rolling, impact, and contact between threaded ends. Agree in writing how visible damage, concealed breakage, inspection timing, and replacement or credit will be handled. Specify who records damage at delivery and what evidence is required. Keep it practical. I would also retain the packing list and receiving photos, even when the supplier seems reliable; paperwork can be imperfect, and memory is worse.
Evaluate 2026 Quotes by Cost per Tonne, MOQ, Lead Time, and Incoterms
When comparing 200x1800mm graphite electrode quotes in 2026, start with cost per tonne, not the headline unit price. Confirm whether the quoted weight is net product weight and whether packaging, inland transport, and ocean freight are included. A low price can look less attractive once delivery costs are added. Check the electrode grade and dimensional tolerances too; matching only the size may leave important performance differences unclear.
Ask each supplier to state the minimum order quantity (MOQ) and whether mixed lots are possible. A smaller trial order may cost more per tonne, but it can reduce inventory risk while you verify quality. Request a lead-time breakdown: production, inspection, packing, and transport are separate stages. Clarify when the clock starts, such as after deposit receipt or final specification approval. Delays happen.
Incoterms can change the real cost and the point where transport risk transfers. Compare quotes on the same basis, such as FOB or CIF, and name the destination port. Confirm who handles export clearance, insurance, and unloading-related charges. Get these details in writing, along with quote validity and packing requirements. One often-missed point: a short lead time is useful only if the shipment schedule fits your production plan.