How to Choose an Industrial Air Compressor?
Selecting an Industrial Air Compressor is a practical engineering decision, not a simple price comparison. The wrong unit may cause pressure drops, overheating, product contamination, or unnecessary energy costs. A compressor that looks powerful on paper can still fail during a busy production shift.
Begin with the air demand. Record each tool, cylinder, valve, and process using compressed air. Check required pressure, flow rate, duty cycle, and future expansion plans. A workshop using intermittent tools needs different equipment than a factory running pneumatic machinery continuously. Receiver size matters too. It can reduce short cycling and stabilize pressure during sudden demand.
The installation environment deserves equal attention. Dust, heat, moisture, and limited ventilation can shorten compressor life. Oil-free models may suit food, pharmaceutical, or electronics production, while oil-lubricated designs often provide efficient industrial performance. However, “oil-free” does not remove every maintenance requirement. Air treatment, filtration, drying, and condensate management remain important.
Energy efficiency should guide the purchase. Electricity may cost more than the compressor itself over several years. Compare motor efficiency, control systems, service intervals, and part availability. Variable-speed drives can reduce waste under changing demand, but they are not automatically the best choice. A steady production line may benefit from another configuration.
Reliable selection requires measured data and honest assumptions. Speak with qualified suppliers, request performance curves, and verify operating conditions. Do not trust impressive brochure numbers alone. They may reflect ideal testing conditions. A perfect choice does not exist. The best Industrial Air Compressor balances air quality, capacity, reliability, maintenance access, and total ownership cost.
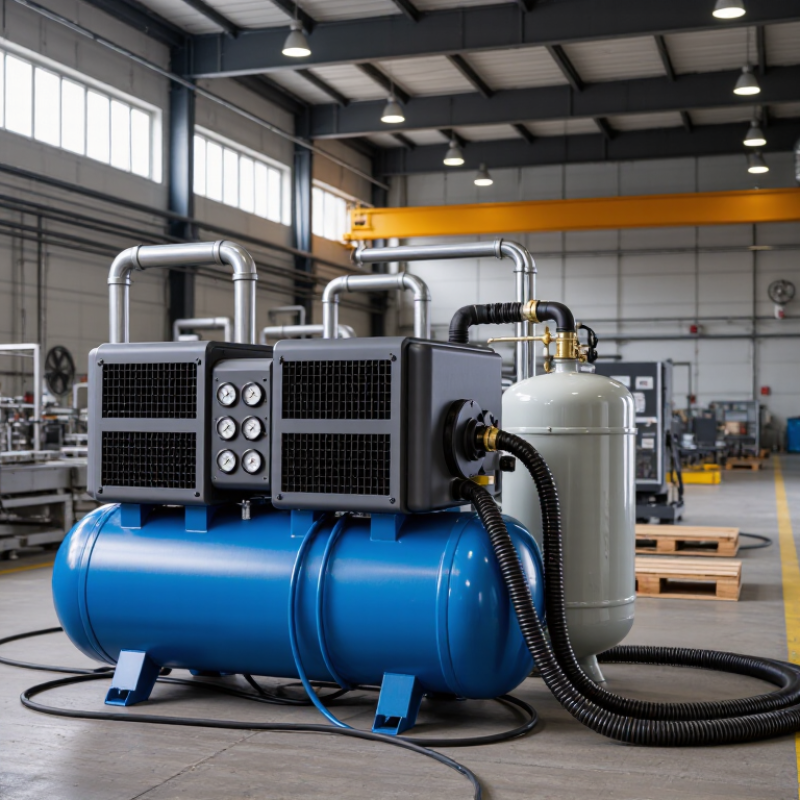
Define Air Demand: Match FAD, Pressure, and a 20–30% Capacity Margin
Choosing an industrial air compressor starts with measured air demand, not the largest motor available. List every pneumatic tool, valve, cylinder, and cleaning point. Record each unit’s required FAD and operating pressure from manuals or field tests. FAD means the volume of free air delivered under stated reference conditions. It is more useful than comparing tank size alone. A pressure gauge showing 7 bar does not prove adequate flow at the outlet. Measure during the busiest production cycle. Watch the gauge. Note pressure drops across filters, dryers, hoses, and long pipe runs. Small restrictions can become expensive surprises.
Add the demands of equipment that may run simultaneously, then apply a 20–30% capacity margin. For example, a line using 1,000 l/min at 7 bar should normally be matched with roughly 1,200–1,300 l/min FAD at the required pressure. Check whether the quoted FAD uses the same test standard and inlet conditions. Otherwise, two attractive data sheets may not describe equal performance. Keep peak and average demand separate; a compressor sized for an occasional blast may cycle poorly during quiet hours. In my experience, operators often overestimate tool consumption and underestimate leaks. A weekend leak survey can reveal a faint hiss near a coupling. That finding may change the selection more than another calculation. Recheck the estimate after production expands.
Compare Compressor Types: Rotary Screw, Reciprocating, and Centrifugal
How to Choose an Industrial Air Compressor?
Choosing an industrial air compressor starts with the work cycle, not the machine’s advertised horsepower. Rotary screw compressors suit factories needing steady airflow throughout long shifts. Their two rotating screws deliver smooth, low-pulsation air with fewer vibration problems. They also operate efficiently under continuous demand, although part-load performance can disappoint if controls are poorly matched.
Reciprocating compressors fit workshops with intermittent air use and higher pressure requirements. A piston compresses air inside a cylinder, making the design familiar and relatively accessible to maintain. However, expect more noise, vibration, and heat near the discharge line. I once underestimated receiver size on a small production line. The compressor then started too often, increasing wear. That mistake changed how I evaluate duty cycles.
Centrifugal compressors are different. They use high-speed impellers and work best when a facility needs large, stable air volumes. They can provide clean compressed air with suitable system design, but they need careful installation, skilled monitoring, and consistent operating conditions. A sudden flow reduction may create control challenges. Check pressure, flow, humidity, ambient temperature, and available floor space before choosing. Ask how much air the plant uses during the quietest hour, not only during peak production. Maintenance access matters too. A compact machine can become expensive when technicians cannot safely reach filters, coolers, or valves.
Assess Energy Use: Compressed Air Can Consume 10–15% of Plant Electricity
How to Choose an Industrial Air Compressor?
Compressed air can consume 10–15% of a plant’s electricity. This figure is reported by the Compressed Air Challenge in its industrial best-practice guidance. The U.S. Department of Energy also notes that leaks may waste 20–30% of compressor output. These losses can hide behind a stable production schedule. A compressor running after shifts still draws power. Listen near fittings. Feel for escaping air during a quiet inspection.
Choose capacity from measured demand, not installed motor size. Record pressure, flow, operating hours, and peak loads for several production cycles. A 75 kW compressor may look adequate, yet a short demand spike can force inefficient loading. Oversizing creates another problem. It can increase unloaded running and maintenance costs. The DOE publication Improving Compressed Air System Performance: A Sourcebook for Industry recommends evaluating controls, storage, pressure, and end-use requirements together.
Ask suppliers for specific energy consumption, expressed as kW per cubic metre per minute. Request test conditions and correction factors. Numbers can shift with inlet temperature, altitude, and pressure. A spreadsheet alone can mislead. Check the compressor room yourself. Hot air, clogged filters, and poor ventilation increase energy use. Variable-speed control may help with changing demand, but it is not automatically efficient. If demand stays steady, another control strategy may perform better. That judgment requires measurements, and sometimes the first estimate is simply wrong.
Specify Air Quality and Lifecycle Needs with ISO 8573-1 and VSD Control
How to Choose an Industrial Air Compressor?
Specify Air Quality and Lifecycle Needs with ISO 8573-1 and VSD Control
Start with the air, not the compressor. ISO 8573-1:2010 classifies particles, water, and oil by purity level. A food-contact process may need a much stricter class than a pneumatic workshop. Define the required class at the point of use, then check dryers, filters, drains, and pipework together. A clean compressor cannot correct a dirty distribution system. In field assessments, this detail is often missed.
Demand patterns matter just as much. A fixed-speed compressor can suit stable, full-load production. Variable-speed drive (VSD) control is more useful when demand rises and falls during shifts. The U.S. Department of Energy’s Improving Compressed Air System Performance guidance identifies leakage as a major waste source, often representing 20–30% of compressor output. VSD cannot repair leaks. It only follows the changing load more efficiently. That distinction is easy to overlook.
Tips: Record pressure, flow, and running hours for at least one production week. Compare the profile with the compressor’s efficient operating range. Ask for specific power data at several loads, not only the headline rating. Review filter pressure loss and dryer energy. DOE compressed-air guidance also stresses lifecycle analysis because energy usually outweighs the purchase price. My practical caution is simple: predicted savings can look perfect on paper, yet poor controls, oversized equipment, or neglected drains can quietly weaken them.