Choosing the best polyimide tape is rarely as simple as selecting the highest temperature rating. Real performance depends on the application, surface, adhesive, and working environment. A tape used for circuit-board masking may need clean removal, while one wrapped around a motor coil must resist heat, voltage, and mechanical stress. The right choice begins with understanding what the tape must endure every day.
Experienced technicians usually examine temperature exposure, dielectric strength, thickness, tensile strength, and adhesive behavior. They also consider whether the tape will contact silicone, metal, plastics, or rough insulation. A thin film can fit tight spaces, but it may tear during installation. A thicker grade offers better handling, yet it can affect clearances. Small details matter.
Do not trust one specification alone. Test a sample on the actual surface whenever possible. Leave it under expected heat, then inspect the edges, residue, and bond strength. This practical step often reveals problems that a product sheet cannot show. Certification and supplier traceability also support safer decisions, especially in electrical and aerospace-related work. Still, product claims require careful verification. Even experienced buyers can overlook humidity, repeated movement, or rushed application. There is no universal best tape. There is only the most suitable choice for a clearly defined need.
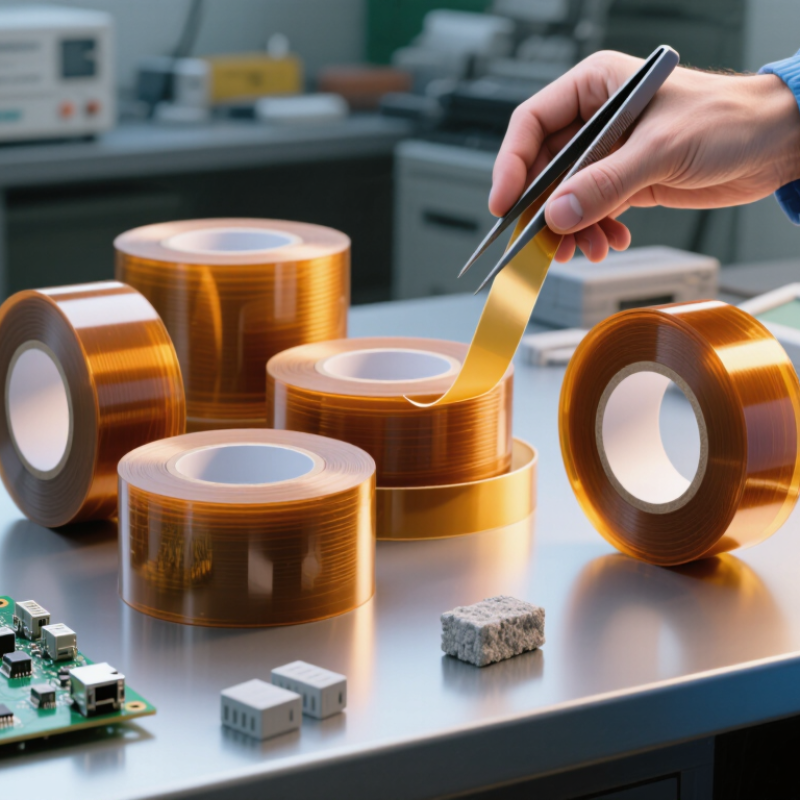
Polyimide tape is a thin adhesive tape built around a polyimide film. This amber-colored film stays stable under heat, electrical stress, and repeated handling. Its adhesive layer bonds to surfaces without greatly changing the tape’s shape. When wrapped around wires or placed over circuit areas, the tape creates insulation and protects against solder splashes, abrasion, and short-term heat exposure.
The tape does not work by heat resistance alone. The adhesive must remain attached without leaving heavy residue. Its performance depends on temperature, pressure, surface cleanliness, and exposure time. A clean metal or polymer surface usually gives better bonding. In practical work, I press the tape firmly with a smooth tool and inspect the edges for lifting. A common mistake is choosing the thickest tape automatically. Thick tape can reduce flexibility and create unwanted steps around small components. I also check whether the adhesive is silicone-based or acrylic-based, because removal behavior may differ.
Tips: Match the tape to the real working temperature, not the equipment’s advertised maximum. Test a small piece first. Check insulation needs, thickness, width, and residue after heating. If the tape will bend repeatedly, evaluate flexibility after installation. I have found that quick visual checks can miss weak corners, so gentle pull testing is useful. Still, this test is not a substitute for documented technical data. Temperature ratings can be misunderstood. Always confirm the film and adhesive limits separately.
When choosing polyimide tape, temperature rating is only the starting point. The adhesive must survive your real process, including heating speed, dwell time, pressure, and removal. A 2023 reliability review from the U.S. National Renewable Energy Laboratory reports that power-electronics components may experience operating temperatures near 150–200°C. That range can quickly expose weak adhesive systems.
Electrical insulation also deserves close attention. Check dielectric strength, insulation resistance, and thickness consistency. ASTM D1000 provides recognized methods for measuring adhesion, tensile strength, and elongation. These tests help compare samples under controlled conditions. However, laboratory values may not match a dusty assembly line. I would test the tape on the exact substrate, especially textured plastics or powder-coated metal.
Mechanical performance matters during cutting and masking. A tape that stretches too easily may wrinkle around sharp corners. Excessive adhesion can leave residue after a long thermal cycle. For circuit protection, verify flame behavior and insulation requirements against the applicable safety standard, such as UL 510. Do not rely on a single headline value. A 2024 industry analysis of high-temperature electrical materials links demand growth to electrification and compact electronics, but market forecasts cannot replace application testing. Small details matter. Test peel strength after heat exposure, humidity conditioning, and repeated removal. My own practical mistake would be choosing the strongest adhesive first; clean release can be more valuable than maximum grip.
How to Choose the Best Polyimide Tape for Your Needs?
Choosing polyimide tape starts with the real temperature at the bond line, not the oven setting. A nearby metal surface can be 20°C cooler or hotter. Many industrial tapes use silicone adhesives for intermittent service near 200°C, while acrylic systems often suit moderate heat and stronger long-term adhesion. Check the supplier’s tested range. Film temperature ratings alone can mislead.
Chemical exposure changes the decision. Polyimide film generally resists oils, solvents, and dilute acids, but the adhesive may soften, swell, or leave residue. For cleaning agents, test a taped sample after 24, 72, and 168 hours. Observe edge lifting. Then measure peel strength. ASTM D1000 provides methods for adhesion, tensile strength, and electrical performance. These tests are useful, but they do not reproduce every factory environment.
Thermal aging deserves careful attention. IEC 60216 uses a 20,000-hour reference when establishing thermal endurance, while UL 746B evaluates long-term heat performance of polymeric materials. Those figures are not automatic guarantees for a finished tape assembly. I would not trust a single temperature number. Humidity, pressure, cycling, and contaminated surfaces matter too. A tape that survives 180°C dry air may fail beside hot alkaline wash water. Test the actual substrate, pressure, dwell time, and chemical concentration. Results can be imperfect, but they reveal more than a catalog headline.
When evaluating polyimide tape, begin with adhesion rather than appearance. A smooth roll can still fail on a dusty or uneven surface. Clean the substrate with a compatible solvent, then apply a small test strip. Press it firmly with a roller. After a short dwell time, check peeling, lifting, and adhesive transfer. Test at the actual operating temperature, because heat can soften some adhesives while making others brittle. A tape that sticks well at room temperature may perform poorly near a soldering area.
Thickness also deserves careful attention. Thinner tape usually follows sharp corners and narrow gaps more easily. However, it may tear during installation or offer less mechanical protection. Thicker tape can resist abrasion better, but it may create unwanted height around connectors and windings. Measure the tape with a calibrated gauge, not only the package label. Tolerances matter in compact assemblies. I have seen a small thickness difference interfere with a cover fit.
Electrical insulation requires more than a high voltage number. Review dielectric strength, volume resistivity, temperature rating, and the test method used. Ask whether the value applies to new tape or aged samples. Test a sample after heat exposure, bending, and humidity when the application is demanding. Keep sharp edges away from the tape whenever possible. One overlooked detail is contamination from handling. Finger oils can reduce adhesion and create unpredictable insulation results. Small tests reveal weaknesses early. They are worth the extra time.
Choosing polyimide tape starts with the application, not the lowest quotation. Check temperature, voltage, insulation needs, and surface condition. In production, I have seen tape fail because its adhesive softened near a heater. Ask for measured data, including continuous temperature ratings, dielectric strength, thickness tolerance, and peel adhesion. Request samples. Apply them to the actual substrate, then inspect the edges after heating and cooling. A clean release matters. So does residue.
Cost comparison should include labor, waste, and replacement risk. A cheaper roll may have uneven coating or inconsistent winding. That creates wrinkles, torn liners, and slower assembly. Compare the price per usable meter, not the price per roll. Review batch records and certificates before approval. Independent test reports can support supplier claims, but they do not replace your own trial. Check packaging, storage guidance, lead times, and response speed. A supplier who answers technical questions clearly is easier to trust. Still, friendly emails do not guarantee reliability. Keep evidence.
Tips: Build a simple scorecard. Give quality, cost, and delivery separate weights. Test at the highest realistic temperature. Record lot numbers and failure photos. Ask how complaints are investigated and corrected. Avoid choosing from one sample alone. That was my mistake once. Do not ignore details like roll telescoping or adhesive transfer. They often become expensive during full-scale production.
Compare quality, cost, and supplier reliability by first matching the adhesive system to the required operating temperature.
The chart shows representative continuous-use temperature limits commonly published for generic polyimide tapes: silicone adhesive up to about 200°C, acrylic adhesive up to about 150°C, and rubber adhesive up to about 80°C. Actual performance depends on tape thickness, adhesive formulation, dwell time, pressure, substrate, and test method. For purchasing decisions, verify technical data, request samples and lot certificates, compare total cost per usable roll, and assess supplier reliability through lead-time consistency, quality-control records, and production capacity.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru