Choosing the right Ppgi Coated Coil supplier affects appearance, durability, production speed, and long-term project costs. A low quotation may look attractive beside a busy purchasing spreadsheet. However, weak coating adhesion, uneven color, or hidden gauge variations can create expensive problems later.
Quality consultant W. Edwards Deming offered a useful principle: “Quality comes not from inspection, but from the improvement of the production process.” That idea fits coated steel purchasing closely. A dependable supplier should control cleaning, chemical treatment, paint application, curing temperature, and recoiling conditions. Ask for measurable details, not polished promises. Review the substrate grade, zinc coating mass, paint system, coating thickness, gloss, color tolerance, and protective film. Request recent inspection reports and traceable mill certificates. Samples should show clean edges, consistent tension, and no visible scratches.
Experience matters here. Visit the production site when possible. Watch how coils are stored. Moisture trapped between tightly packed coils can cause premature white rust. It is a small detail. It can become a serious claim.
Industry knowledge also means checking whether the supplier understands your environment. Coastal buildings require stronger corrosion resistance. Roofing panels need stable forming performance. Interior applications may require different paint chemistry and surface protection.
Price still tempts buyers. It should not lead alone. Compare total value, delivery reliability, technical support, packaging quality, and claim handling. No supplier is perfect. Even a trusted partner may miss a detail. The best choice is one that documents risks honestly, responds quickly, and improves after problems appear. That is the real test behind selecting a PPGI Coated Coil supplier.
How to Choose the Best PPGI Coated Coil Supplier?
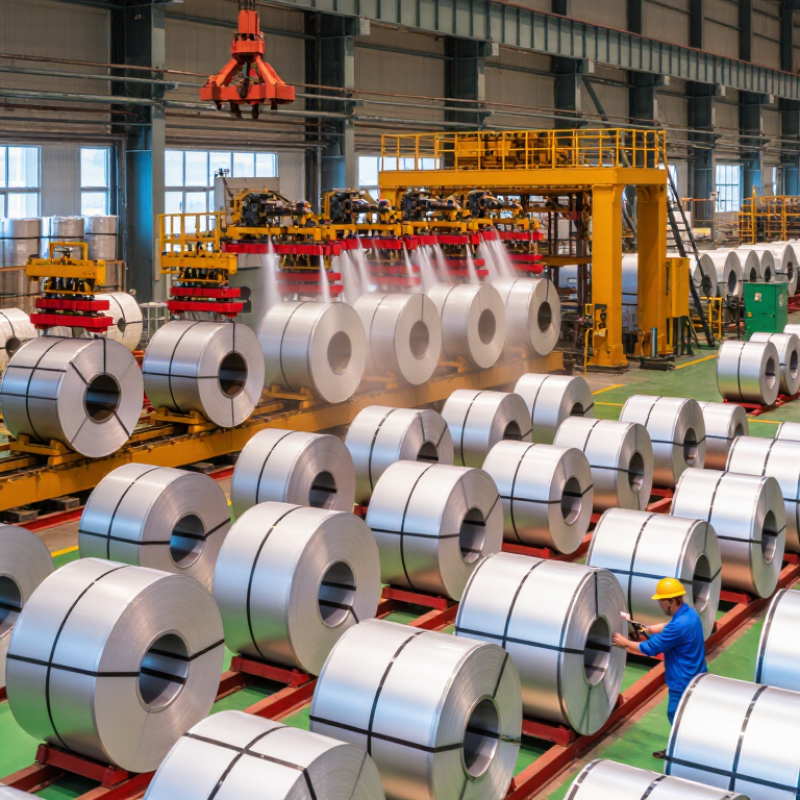
PPGI starts with the correct EN 10346 substrate. DX51D suits general roll forming, while S250GD and S350GD provide higher structural strength. The grade is not the coating. Z100, Z140, Z200, and Z275 describe zinc mass, measured in grams per square metre across both surfaces. Z275 therefore contains 275 g/m² of zinc, not 275 microns. That difference prevents costly specification errors.
A reliable supplier should provide mill certificates, coating test results, paint-system details, and traceable coil numbers. EN 10346 controls metallic-coated flat steel, but it does not define every paint performance requirement. Ask about primer type, topcoat thickness, gloss, colour tolerance, and forming limits. Check the coil edge and surface under warehouse lighting. Small scratches often become visible after profiling.
Scale also matters. The World Steel Association’s World Steel in Figures 2024 reports approximately 1.89 billion tonnes of crude steel production in 2023. Such volume makes documentation essential, not decorative. A supplier should connect each PPGI coil to its heat number, substrate grade, zinc mass, and paint batch. Sampling matters too. One certificate cannot represent every delivery perfectly. I have seen specifications accepted too quickly, especially when Z275 was chosen without considering cutting edges, humidity, or forming damage. The safer decision combines EN 10346 compliance, realistic exposure conditions, and independent verification before production.
| Evaluation Dimension | Reference Option | Technical Data | Typical Application or Selection Meaning | What to Verify with the Supplier |
|---|---|---|---|---|
| Product Definition | PPGI coated coil | Pre-painted galvanized steel coil consisting of a steel substrate, metallic zinc coating, chemical treatment or primer system, and organic topcoat. | Used when appearance, corrosion protection, forming performance, and consistent color are required. | Substrate grade, zinc coating designation, paint system, nominal thickness, width, color, gloss, and applicable standard. |
| Forming Grade | DX51D | Commercial-quality galvanized steel grade specified in EN 10346 for general forming and profiling. | Roofing sheets, wall panels, flashings, trims, and relatively simple roll-formed components. | Whether the forming operation is suitable for the requested bend radius and profile depth. |
| Deep-Forming Grade | DX52D | Deep-drawing quality galvanized steel grade under EN 10346. | More demanding formed parts where improved ductility is needed compared with commercial forming quality. | Mill certificate values, forming test results, and suitability for the final part geometry. |
| Extra-Deep-Forming Grade | DX53D | Extra-deep-drawing galvanized steel grade under EN 10346. | Complex pressed or formed parts requiring higher formability than DX51D and DX52D. | Minimum inside bend radius, surface quality, and compatibility with the paint system after forming. |
| Structural Grade | S250GD | Structural galvanized steel grade with a specified minimum yield strength of 250 MPa. | Light structural profiles, purlins, framing members, and panels requiring defined structural strength. | Yield strength, tensile strength, elongation, and design calculations for the finished component. |
| Structural Grade | S350GD | Structural galvanized steel grade with a specified minimum yield strength of 350 MPa. | Higher-strength roofing, wall, framing, and roll-formed structural components. | Strength certificate, profile design requirements, and forming limits. |
| Structural Grade | S550GD | High-strength structural galvanized steel grade with a specified minimum yield strength of 550 MPa. | High-strength cold-formed sections where reduced material weight is important. | Tooling capability, springback control, minimum bend radius, and structural compliance. |
| Zinc Coating | Z100 | Nominal zinc coating mass of 100 g/m² total for both surfaces, approximately 50 g/m² per surface when evenly distributed. | Lower coating mass for controlled indoor or relatively mild exposure conditions. | Actual coating test results, intended environment, cut-edge protection, and warranty requirements. |
| Zinc Coating | Z140 | Nominal zinc coating mass of 140 g/m² total for both surfaces. | General-purpose corrosion protection for many interior and moderately exposed applications. | Coating uniformity, surface treatment, paint adhesion, and exposure classification. |
| Zinc Coating | Z180 | Nominal zinc coating mass of 180 g/m² total for both surfaces. | Enhanced corrosion protection for more demanding building and industrial environments. | Coil availability, coating mass tolerance, and compatibility with the selected paint system. |
| Zinc Coating | Z200 | Nominal zinc coating mass of 200 g/m² total for both surfaces. | Higher corrosion-resistance requirement where additional zinc protection is justified. | Environmental exposure, forming behavior, edge quality, and documented coating measurements. |
| Zinc Coating | Z225 | Nominal zinc coating mass of 225 g/m² total for both surfaces. | Heavy-duty galvanized substrate selection for exposed building or industrial applications. | Whether the additional coating mass is supported by the project specification and delivery capability. |
| Zinc Coating | Z275 | Nominal zinc coating mass of 275 g/m² total for both surfaces, approximately 137.5 g/m² per surface when evenly distributed. | Common high-coating option for demanding exterior exposure and longer corrosion-protection requirements. | Minimum coating results, paint adhesion after forming, delivery consistency, and storage protection. |
| Paint System | Polyester | Common organic coating system for general exterior and interior applications; performance depends on resin, coating thickness, and environment. | Cost-effective roofing, wall cladding, panels, and formed building products. | Topcoat and back-coat thickness, gloss, color tolerance, adhesion, and stated durability class. |
| Paint System | PVDF | Fluoropolymer-based coating system selected for higher resistance to weathering, ultraviolet exposure, and color fading than many standard coatings. | Architectural façades and applications requiring enhanced appearance retention. | Resin composition, dry-film thickness, color and gloss limits, adhesion, and project-specific performance requirements. |
| Dimensional Control | Thickness and Width | Coil thickness is normally specified in millimetres and width in millimetres; tolerances depend on the applicable standard and purchase specification. | Accurate dimensions reduce profile variation, material waste, and production stoppages. | Measured thickness basis, width tolerance, flatness, camber, coil inside diameter, and coil weight. |
| Quality Documentation | Inspection Certificate | A complete certificate should identify the grade, coating designation, dimensions, mechanical properties, coating results, paint details, heat or batch reference, and inspection basis. | Traceability allows the buyer to confirm that delivered PPGI coil matches the purchase specification. | Certificate traceability, independent testing options, sample approval, and nonconformance procedure. |
| Storage and Delivery | Moisture and Handling Control | PPGI coils should be protected from water ingress, condensation, impact, and prolonged storage in humid conditions to reduce staining and coating damage. | Proper packaging and transport handling help preserve surface appearance and edge integrity. | Packaging method, corrosion protection during shipment, loading photos, delivery schedule, and claim handling. |
How to Choose the Best PPGI Coated Coil Supplier?
Paint thickness deserves more than a supplier’s neat certificate. For PPGI coils, verify the specified 5–35 μm dry film thickness against ASTM A755/A755M requirements and your purchase agreement. The standard covers prepainted, metallic-coated steel sheet, but the exact thickness depends on the coating system, paint type, and agreed tolerance. Confirm whether the value includes primer, topcoat, or both. This detail is often overlooked.
Ask for batch-specific inspection records, not generic brochures. A qualified inspector should use a calibrated dry-film gauge suited to the metallic substrate. Measurements should cover the coil length, width, exposed face, and reverse side where applicable. Check several points near the edges and center. One reading can mislead. Small variations may result from line speed, surface preparation, or paint viscosity. A supplier should explain these variations clearly instead of hiding behind an average value.
Compare measured results with the ordered target, tolerance, and ASTM A755/A755M-based documentation. Also review surface defects, adhesion tests, color consistency, and traceability records. I would request a retained sample from the same production batch. It is a simple safeguard. However, thickness alone cannot prove long-term performance. Humidity, forming, transport damage, and installation conditions still matter. A reliable supplier admits these limits and supports independent verification when results seem uncertain.
ASTM A755/A755M provides requirements and guidance for steel sheet coated by the coil-coating process, but it does not define one universal paint-thickness limit for every product. The agreed coating thickness, coating system, test method, and acceptance criteria should be confirmed in the purchase specification. The chart shows neutral quality-control readings across common nominal dry-film thickness targets.
A capable supplier should provide test records identifying the nominal thickness, measured values, measurement method, substrate condition, and acceptance range. Confirm whether the quoted 5–35 μm value refers to one side, both sides, the primer plus topcoat, or total dry-film thickness.
A reliable PPGI supplier must prove capacity across 0.12–1.20 mm thickness, not merely list it. Ask for recent production records showing thickness, width, steel grade, coating mass, and delivered tonnage. The 0.12 mm gauge needs stable tension control and precise leveling. The 1.20 mm gauge demands stronger rolling capacity and reliable furnace control.
Width capability also matters. Confirm the minimum and maximum widths, trimming tolerance, coil inner diameter, and maximum coil weight. A supplier offering 1,250 mm width may not consistently produce your required 1,220 mm finished width.
The World Steel Association reported 1,882.6 million tonnes of global crude steel production in 2023, according to World Steel in Figures 2024. Large output alone proves little. PPGI quality depends on line configuration, inspection discipline, and process records.
Request mill test certificates, coating-weight results, paint-system details, and sample cross-sections. Check whether inspection follows relevant requirements, such as EN 10346 or ASTM A755/A755M.
Also review three months of production evidence for thin gauges. One isolated sample can look perfect. Production history is harder to disguise. I would test width variation across the coil, because edge waviness often appears after forming.
Suppliers sometimes state broad ranges without explaining restrictions. That is a warning sign. Capacity should be demonstrated with repeatable data, although no supplier’s record is flawless.
Choosing a PPGI coated coil supplier requires more than comparing price and colour cards. EN 10169 provides a practical framework through corrosion resistance classes, RC, and ultraviolet resistance classes, RUV. These classifications help match the coating system to the building’s real exposure.
PE coatings often suit sheltered buildings and controlled budgets, but their resistance can be limited in harsh sunlight or industrial atmospheres. SMP coatings usually offer stronger colour retention and weather resistance. PVDF systems are commonly selected for demanding façades, coastal areas, and projects requiring long-term appearance stability. However, the resin type alone does not prove performance. Coating thickness, steel substrate, pretreatment, forming quality, and application method also affect results. Testing beats promises.
A reliable supplier should provide EN 10169 classification data, coating thickness records, substrate specifications, and batch traceability. Ask whether the quoted RC and RUV classes apply to the complete coil system, not only the topcoat. Request independent test reports when the project has severe exposure. The supplier should also explain edge protection and expected performance after cutting, bending, and installation. Details decide.
In project reviews, a lower-cost PE coil can be sensible for an indoor warehouse. It may be a poor choice beside salt spray or persistent humidity. PVDF can reduce repainting concerns, yet its higher purchase cost may not suit every building. SMP sits between these options, although its performance still depends on formulation and manufacturing control. I would question vague warranties, because warranty wording can hide exclusions, maintenance duties, and untested assumptions. Supplier transparency matters as much as the coating label.
A reliable PPGI coated coil supplier should provide more than an ISO 9001 certificate. During a supplier audit, ask to see the current quality manual, inspection procedures, and corrective action records. Check whether these documents match actual production practices. A clean certificate alone proves little.
Review testing records for coating thickness, paint adhesion, gloss, hardness, yield strength, and zinc coating weight. Each report should identify the coil number, testing date, equipment, and responsible inspector.
Traceability matters. Request a sample from production, not only a prepared presentation. Compare its results with the approved specification. Small gaps can become expensive problems.
Warranty terms need careful reading. Confirm coverage for peeling, color fading, corrosion, and manufacturing defects. Ask about exclusions, claim evidence, response time, and replacement procedures. Delivery terms deserve the same attention. Clarify production lead time, loading photos, packaging standards, shipping documents, and responsibility for transport damage. I once focused too heavily on price and overlooked weak packaging. That mistake delayed a project. Supplier promises also need written records. Verbal assurances are easy to misunderstand. A short trial order may reveal more than a long sales meeting.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru