Choosing an Aluminum Extrusion Die is not a small tooling decision. It shapes profile accuracy, surface quality, production speed, and the amount of scrap on the press floor. The International Aluminium Institute has projected that global aluminium demand could grow by nearly 40% by 2030 compared with 2020 levels. That growth raises the stakes for manufacturers: a die must support reliable output, not merely produce one acceptable sample.
Start with the profile itself. Wall thickness, hollows, corners, and dimensional tolerances all affect die design. Alloy, billet temperature, press capacity, and target production volume matter too. A thin-walled channel may need different bearing lengths and metal flow control than a solid bar. Small details count. Even a sharp transition can create uneven flow, die wear, or visible surface marks.
This guide explains how to match die type and design to the job, then weigh material, lead time, cost, and maintenance. Experienced die makers can help interpret drawings and flag difficult features before tooling begins. Ask for evidence from similar profiles, including trial results and expected die life. Numbers help, but they do not tell the whole story. Real production conditions can expose assumptions that looked sound on paper. Choosing well takes technical review, clear requirements, and a willingness to revise the design when the first trial reveals a weakness.
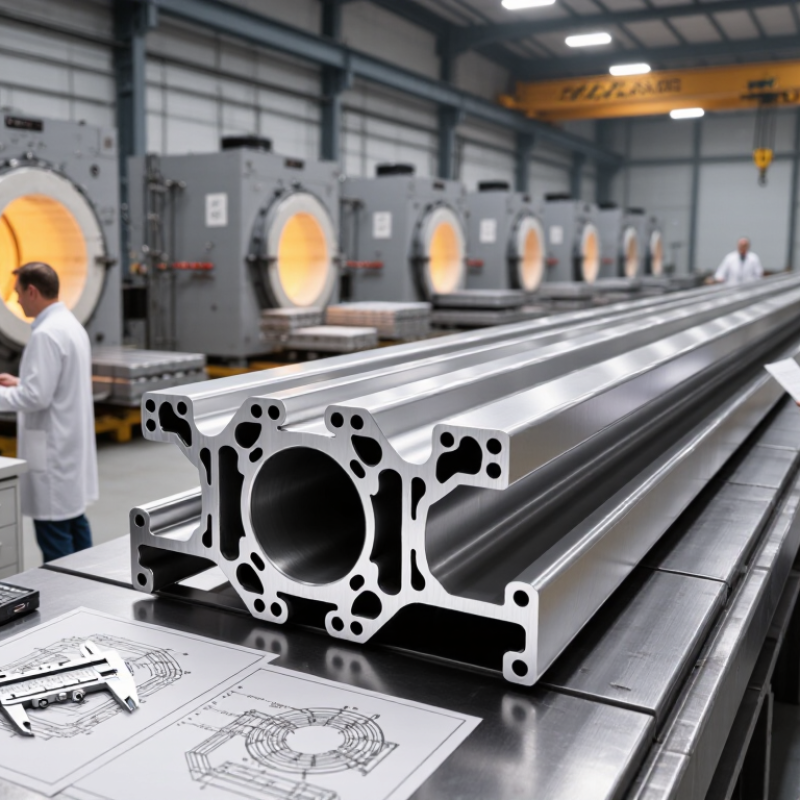
Before selecting an aluminum Extrusion Die, study the profile drawing rather than judging the outline alone. Note the overall width and height, wall thickness, corner radii, and any grooves or narrow slots. These details affect metal flow through the die. A thin wall beside a heavy section may fill unevenly, even when the outside dimensions look simple. Small features matter.
Mark which dimensions are critical for assembly and which allow normal production variation. A sliding channel may need tighter control than a concealed trim edge. Specify tolerances clearly, and check whether they apply across the full profile or only at certain points. For hollow shapes, identify internal openings and the bridges that form them. These can influence die design and require careful review of strength and flow. A clean, dimensioned drawing helps the die maker assess feasibility before tooling begins.
It is tempting to perfect every measurement on paper. That can be misleading. Compare the drawing with the part’s actual use, mating components, and finishing process. Anodizing or coating may affect fit, so include those requirements early. If a dimension is uncertain, flag it instead of guessing. A physical sample or prototype review can reveal interference that a drawing misses. Revise the specification when needed; a small correction now is usually easier than adjusting a production die later.
| Profile Geometry or Requirement | Details to Identify | Typical Die Consideration | Why It Matters |
|---|---|---|---|
| Solid profile | One continuous cross-section with no enclosed internal voids; record overall width, height, wall thickness, and corner radii. | A solid die is commonly used. Check bearing lengths and metal flow around thick and thin regions. | Uneven section thickness can cause different flow rates, twisting, or dimensional variation. |
| Hollow profile | One or more enclosed cavities, including the number, shape, and minimum size of each void. | A porthole or bridge die is often used; assess mandrel support, weld chambers, and metal flow balance. | The die must form the cavity while maintaining adequate support and sound pressure welds. |
| Semihollow profile | A partially enclosed opening with a narrow gap; specify the opening width and surrounding wall thickness. | Determine whether a solid-die approach is feasible or whether a hollow-style die design is needed. | The opening-to-depth relationship affects die strength, flow, and the risk of distortion. |
| Wall thickness | Define nominal, minimum, and maximum thicknesses, including local transitions and thin webs. | Review die strength and flow balance; avoid abrupt thickness changes where the design permits. | Very thin or uneven walls can be difficult to fill consistently and may increase scrap or correction work. |
| Overall dimensions | Specify the outside envelope, critical internal dimensions, and measurement locations. | Check whether the profile fits the press and die limits, including billet size and container capacity. | Profile size influences press selection, die layout, and achievable production rate. |
| Dimensional tolerances | State the required tolerances for width, height, wall thickness, openings, and functional interfaces. | Set die dimensions with allowance for process effects, including elastic recovery and thermal conditions. | Clear, measurable tolerances help prevent over-specification and ensure the part fits its assembly. |
| Corner radii and edges | Identify internal and external radii, sharp-edge requirements, and any edge breaks. | Include practical radii in the die design where possible; very sharp corners may be difficult to maintain. | Radii can improve metal flow, reduce stress concentration, and support more consistent production. |
| Asymmetry and section balance | Mark off-center features, one-sided projections, unequal wall thicknesses, and long unsupported legs. | Balance flow using suitable bearing design and die layout; plan for trial measurements and adjustment. | Unbalanced flow can cause bow, twist, or uneven exit speed across the profile. |
| Material and temper | Specify the aluminum alloy, temper, and applicable material specification. | Confirm that the die design and press conditions are appropriate for the selected alloy and production requirements. | Alloy and temper affect extrusion behavior, achievable properties, and downstream processing. |
| Length, straightness, and twist | Define cut length and acceptable limits for bow, twist, and straightness, along with inspection methods. | Consider die exit balance and the planned stretching, straightening, and cutting operations. | Profile dimensions may change during cooling and finishing, so final acceptance should reflect the finished condition. |
Choose the alloy before finalizing the die, because each grade moves differently under heat and pressure. Common 6xxx alloys, such as 6063, generally extrude smoothly and suit profiles with thin walls or fine details. Their magnesium and silicon content still affects flow, so the exact grade matters. A small change in wall thickness can alter how quickly metal fills a narrow pocket.
Check billet temperature, extrusion speed, and press capacity together. If the billet is too cool, the alloy may resist flow and leave incomplete corners. Too much heat or speed can create surface marks, uneven dimensions, or unwanted grain changes. Watch the exit temperature and inspect the profile along its length, not just at the first cut. Small details count. Higher-strength 7xxx alloys can demand tighter control and may call for simpler die features than an easy-flowing 6xxx grade. A die that works well for one alloy is not automatically suitable for another.
Trial runs help reveal what calculations miss. Record the actual billet temperature, ram speed, and profile dimensions, then adjust bearing lengths or flow balance when evidence supports a change. It is tempting to blame the die immediately. Sometimes the process settings are the real issue, and sometimes both need revision. Recheck assumptions after each run.
A die must match both the profile and the way aluminum can flow through it. A simple solid bar usually needs less flow balancing than a section with thin legs, deep channels, or uneven wall thickness. Small details matter. A narrow tongue in the die can face high stress, while a thick region may draw metal faster than nearby thin walls. Review the profile with the extrusion alloy, billet temperature, and press capacity in mind.
For hollow shapes, bridges divide the incoming metal and direct it into a weld chamber, where pressure brings the streams together. The chamber and bearing lengths need careful design. Bearings help regulate local flow: a longer bearing generally slows metal, while a shorter one allows it to move faster. But adjustments are not isolated fixes. Changing one area can shift flow elsewhere. Even a tidy drawing can mislead.
A practical die review should flag sharp corners, thin webs, and abrupt changes in section thickness. Ask where metal may hesitate, accelerate, or leave the profile uneven. Trial runs can reveal issues that calculations alone miss, including distortion or inconsistent wall thickness. Record those results and revise the die with measured evidence. Perfect balance is not always realistic. The useful goal is a stable process that produces a profile within its specified tolerances.
An extrusion die must resist heat, pressure, and repeated contact with moving aluminum. Match the steel to alloy abrasiveness, profile complexity, and production volume. ASTM A681’s H13 tool-steel composition specifies 4.75–5.50% chromium, 1.10–1.75% molybdenum, and 0.80–1.20% vanadium. These alloying elements support hot-strength and wear resistance, but chemistry alone does not guarantee a durable die. Heat treatment, surface condition, and machining quality matter too. Hardness is not the whole story.
Check the expected operating temperature and press conditions before choosing a grade. European Aluminium’s extrusion guidance places many billet processes near 450–500°C, though alloy and setup change the target. Repeated heating and cooling can fatigue a die, while abrasive alloys can wear bearing surfaces faster. Ask the die maker for hardness records and comparable run data, not just a promised service-life figure. Track press hours, profile dimensions, and repair intervals. That evidence is useful. It may still be imperfect: operators, lubrication, and maintenance can change die life substantially, so one shop’s result may not transfer directly.
Compare key alloying elements in two commonly used hot-work tool steels. Values are typical nominal compositions by weight; exact specifications vary by standard and supplier.
How to interpret: H13 and H11 have similar chromium and molybdenum levels, while H13 typically contains more vanadium, which contributes to wear resistance. Chemistry alone cannot predict die service life: heat treatment, die design, nitriding, extrusion conditions, and maintenance also matter. Confirm the grade and heat-treatment requirements with the applicable material specification.
Choosing an aluminum extrusion die involves more than comparing the initial tooling price. Ask what each quote includes: die steel, machining, nitriding, sample runs, and possible corrections. A simple, open profile may need less complex tooling than a hollow shape with tight dimensional tolerances. Still, low cost can hide exclusions. I have seen estimates look similar until trial charges appeared.
Lead times depend on profile complexity, die-shop capacity, and how quickly drawings are approved. Confirm whether the schedule includes die design, first extrusion, and sample delivery. Trial requirements matter, too. Specify the alloy, temper, cut length, and critical dimensions before production. A short trial can reveal wall variation, twist, or surface marks that a drawing alone will not show. Allow time for adjustments; the first sample may not be perfect.
Tips: Request a written breakdown of tooling and trial costs. Ask how many trial rounds are included, what measurements will be recorded, and who approves revisions. Share a marked-up drawing with critical tolerances highlighted. One detail I sometimes overlook is packaging for samples, so confirm how parts will arrive for inspection.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru