How to Choose a CCD Inspection Machine?
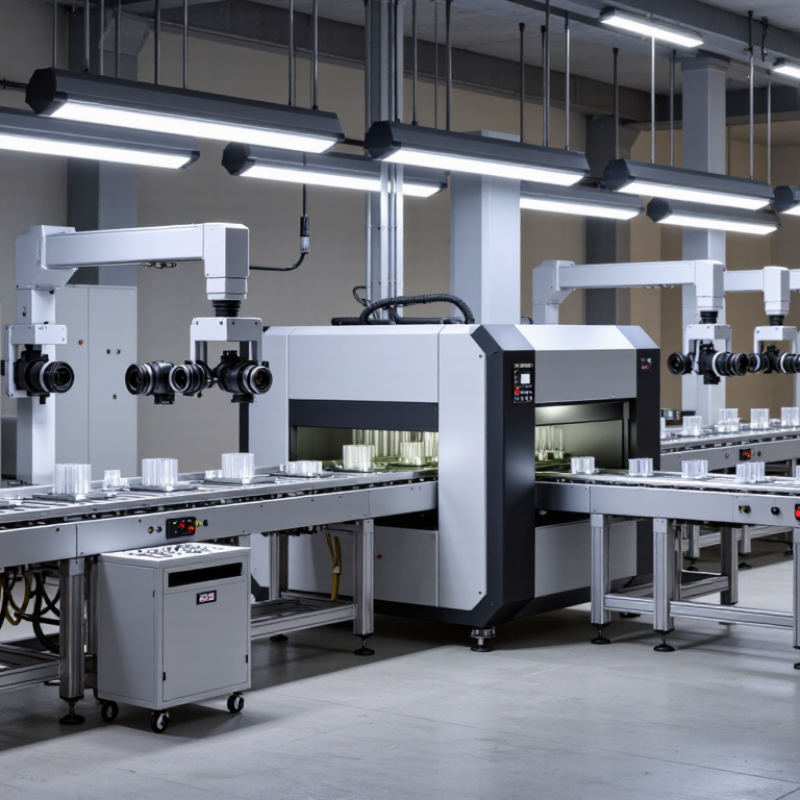
Choosing a Ccd Inspection Machine requires more than comparing camera resolution or purchase price. The right system must match your product, defect types, production speed, and inspection environment. A machine that performs well on metal parts may struggle with transparent plastic, reflective surfaces, or uneven textures. Practical evaluation starts with real samples, not attractive brochures.
Experienced engineers examine image stability under changing light, vibration, dust, and temperature. They check whether the camera can detect scratches, missing components, incorrect dimensions, or surface contamination consistently. Lighting often matters as much as the CCD sensor. A small change in angle can reveal a hidden edge defect. It can also create a misleading shadow. That is where careful testing matters.
Ask for repeatability data, sample inspection videos, and clear information about software settings. Confirm how the Ccd Inspection Machine connects with conveyors, PLC systems, reject units, and production records. Operators should understand the interface without relying on constant specialist support. Maintenance access also deserves attention. A difficult lens adjustment can quietly reduce inspection quality over time.
No machine is perfect. Some suppliers may demonstrate only ideal samples. Your own products may expose weaknesses later. Run trials with good parts, borderline parts, and known defects. Measure false rejects and missed defects separately. A reliable decision balances technical performance, operator experience, future service, and total operating cost. The best choice is not always the most advanced model. It is the system that delivers dependable results in your actual factory.
Define Defect Limits: Capture Each Critical Feature in 2–3 Pixels
When choosing a CCD inspection machine, start with the defect limit, not the camera format. Define the smallest critical feature and make it cover at least 2–3 pixels. A 0.15 mm crack therefore needs a pixel scale of roughly 0.05–0.075 mm per pixel. This calculation must include lens distortion, vibration, and inspection tolerance.
The EMVA 1288 standard separates spatial resolution, signal-to-noise ratio, and dynamic range. A sharp image can still miss a low-contrast defect. ISO 12233 testing also evaluates spatial frequency response, which helps reveal whether the optical system preserves fine edges. In production trials, I check a real sample under the fastest planned conveyor speed. Static images can mislead.
Use more pixels when defects have soft edges, changing reflectivity, or irregular shapes. Two pixels may show presence. Three or more pixels support classification. That rule is useful, but not sacred. I have seen a calculated 2-pixel defect disappear after exposure time changed. Lighting matters.
Leave practical margin. If the defect limit is 0.10 mm, designing for 0.10 mm per two pixels is fragile. A 0.033 mm pixel scale gives about three pixels across the feature. Review the EMVA 1288 camera data, ISO 12233 chart results, and measured samples together. Do not trust resolution figures alone. The final decision should reflect contrast, motion blur, lens performance, and the cost of a missed defect.
Match CCD Resolution and Optics: Balance FOV, Pixel Size, and MTF
Choosing a CCD inspection machine starts with the smallest defect, not the camera’s headline resolution. According to EMVA 1288 Release 4.0, sensor evaluation should include sensitivity, signal-to-noise ratio, and dynamic range. These measurements matter when polished metal creates glare or dark cavities lose contrast. A larger sensor may capture more area, but its pixels can become too large for tiny defects.
Consider a 100 mm field of view with a 2,448-pixel sensor. One pixel represents about 40.8 micrometres. A 0.1 mm defect covers roughly 2.45 pixels. That meets basic sampling, but it leaves little tolerance for vibration, focus errors, or weak contrast. In production, three to four pixels across a defect is safer. This is a practical rule, not a guarantee.
Optics must match the pixel size. Lens MTF should remain strong near the required spatial frequency, rather than only looking sharp at the image centre. ISO 12233 testing practices can help compare resolution and contrast consistently. Check the corners too. FOV, working distance, aperture, and distortion interact. A wider aperture may improve brightness but reduce depth of field. I have seen systems pass laboratory tests and fail after a small fixture change. Recheck calibration under real lighting, because theoretical resolution often overstates usable resolution.
Verify Throughput: Calculate Required FPS from FOV and Line Rate
Choosing a CCD inspection machine starts with throughput, not camera resolution. Let conveyor speed be 600 mm/s and the vertical field of view be 50 mm. The basic requirement is 600 ÷ 50 = 12 frames per second. Add a 20% overlap margin, and the camera should deliver at least 14.4 FPS. Real production lines need headroom for vibration, encoder error, and trigger delays.
This calculation is often underestimated. A larger field of view lowers the required FPS, but it may reduce defect detail. A smaller field of view improves sampling, yet demands faster imaging and processing. The Association for Advancing Automation reported continued growth in machine vision adoption across manufacturing, while MarketsandMarkets estimated the machine vision market could grow from about 13.7 billion dollars in 2024 to 20.9 billion dollars by 2029. Faster inspection is valuable, but only when image quality remains stable.
Check the full chain: exposure time, transfer time, processor capacity, storage, and reject response. For a 1,200 mm/s line with a 40 mm field of view, the base rate is 30 FPS. With 25% margin, specify at least 37.5 FPS. That number may still be optimistic if lighting flickers or products arrive unevenly. I have seen systems pass a bench test and fail beside a vibrating conveyor. The calculation needs a factory trial.
How to Choose a CCD Inspection Machine? - Verify Throughput: Calculate Required FPS from FOV and Line Rate
Frame-rate planning examples based on the vertical field of view and production line speed
| Inspection Scenario | Vertical FOV
(mm) | Line Rate
(mm/s) | Minimum Required FPS
(frames/s) | Recommended Camera FPS
(20% Safety Margin) | Maximum Frame Interval
(ms) |
| Low-Speed Web Inspection | 100 | 500 | 5.0 | 6.0 | 166.7 |
| Standard Conveyor Inspection | 75 | 750 | 10.0 | 12.0 | 83.3 |
| Medium-Speed Surface Inspection | 50 | 1,000 | 20.0 | 24.0 | 41.7 |
| High-Speed Component Inspection | 40 | 1,500 | 37.5 | 45.0 | 22.2 |
| Very High-Speed Web Inspection | 25 | 2,000 | 80.0 | 96.0 | 10.4 |
Calculation method: Minimum required FPS = Line Rate (mm/s) ÷ Vertical FOV (mm). The recommended camera FPS includes a 20% operating margin to accommodate triggering variation, processing overhead, and short-term speed changes. Maximum frame interval (ms) = 1,000 ÷ Recommended Camera FPS.
Validate Measurement Quality: Target Cpk ≥1.33 and Gauge R&R ≤10%
How to Choose a CCD Inspection Machine?
A CCD inspection machine must prove measurement quality, not only produce sharp images. Set a practical target of Cpk ≥1.33 for critical dimensions. The NIST/SEMATECH e-Handbook identifies 1.33 as a widely used capability benchmark for stable processes. Record repeated measurements across operators, shifts, lighting conditions, and representative parts. A polished sample can hide weak performance.
Measurement variation needs equal attention. The AIAG Measurement Systems Analysis reference commonly classifies Gauge R&R below 10% as acceptable, 10–30% as conditional, and above 30% as unacceptable. For demanding CCD applications, keep Gauge R&R at or below 10%. Use at least ten parts, multiple operators, and repeated trials during validation. Check edge contrast, lens distortion, vibration, and fixture seating. Small setup errors can become large pixel errors.
Do not accept a supplier’s single demonstration. Ask for raw data, control charts, and the calculation method. I would also challenge the test design. Were the parts truly varied? Was the lighting fixed unrealistically? These questions matter. A machine may reach Cpk 1.40 in a controlled trial, then fall below 1.33 on the factory floor. Revalidate after software changes, lens replacement, or camera relocation. The target is useful, but the evidence must remain believable.