Bend Wpc safely in 2026 requires more than warming a board and forcing it around a form. Wood-plastic composite combines wood fibers, polymers, additives, and sometimes hollow internal structures. Each formulation reacts differently to heat, pressure, moisture, and cooling. A curve that looks smooth outside may hide crushed fibers or internal separation.
Professor Michael P. Wolcott, a recognized wood-plastic-composites researcher, offers a useful principle: “Processing conditions determine composite performance.” That warning matters during bending. Use the manufacturer’s recommended temperature range, bending radius, heating time, and cooling method. Never guess from appearance alone. A digital thermometer, stable bending jig, gloves, eye protection, and controlled ventilation provide a safer working setup. Keep the workpiece supported across its full length. Local pressure can leave pale marks, dents, or permanent distortion.
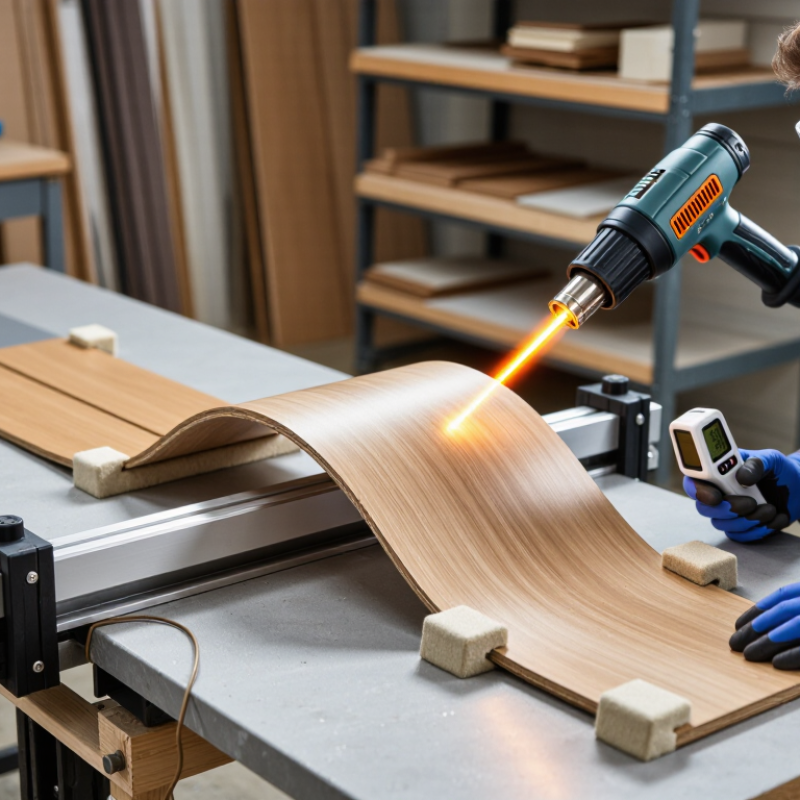
The practical method begins with a small test piece from the same production batch. Heat gradually and check flexibility at short intervals. Do not use an open flame. Uneven heating can scorch the surface while the core remains rigid. Secure the softened WPC against a smooth former, then hold it until fully cooled. Rushing this stage is a common mistake.
Some guides promise sharp curves with simple tools. That advice can be misleading. A successful bend once does not prove long-term stability. Temperature changes, sunlight, and repeated loading may reveal weaknesses later. Record the material grade, heating conditions, radius, and cooling time. If cracks, whitening, bubbling, or spring-back appear, stop and reassess. Safe results depend on patience, tested limits, and honest inspection.
WPC combines wood fiber, thermoplastic resin, and additives. Recent reviews in Polymers report wood content commonly ranging from 50% to 70% by weight. The remaining resin controls heat response and flexibility. This structure creates a key limitation: WPC is not naturally elastic like solid plastic. Wood particles interrupt polymer flow. Sharp bending can cause whitening, surface cracks, or hidden delamination.
The USDA Forest Products Laboratory notes that wood-based materials respond strongly to moisture and temperature changes. ASTM D7031 also recommends evaluating flexural performance under controlled conditions. In practice, many profiles need gradual heating within the resin supplier’s approved softening range. Uneven heat is risky. The outer surface may scorch while the core remains rigid. A large bending radius is safer, but no universal radius exists. Profile thickness, fiber loading, moisture, and extrusion quality all matter. A clean curve can still fail later through creep.
Tips: Measure the profile temperature, not only the heater setting. Use a wide jig and continuous support. Heat slowly and evenly. Avoid open flames. Make a small trial bend first, then inspect both surfaces after cooling. Leave the piece clamped until fully stable. ASTM D790 flexural testing can help compare samples, but it cannot predict every field condition. I would not trust appearance alone. Humid storage, repeated loading, and summer heat may expose weaknesses weeks later.

Before heating, identify the WPC formulation, thickness, moisture condition, and reinforcement. Different polymers soften at different temperatures. Do not guess. Check the supplier’s technical sheet and safety data sheet for softening limits, ventilation needs, and decomposition warnings. The USDA Forest Products Laboratory’s Wood Handbook reports that wood-based materials respond to changing moisture and temperature. WPC can also expand unevenly, especially across thick sections. Measure twice.
Inspect the surface for cracks, voids, trapped water, or metal fasteners. ASTM D7031 evaluates WPC density, moisture absorption, and mechanical performance, while ASTM D6109 measures flexural properties. These standards do not provide one universal bending temperature. Use them to understand material behavior, not to replace a controlled trial. Clamp the piece gently, support both sides, and record the heating time, surface temperature, and bending radius. A thermocouple is more reliable than touching the panel.
Use local extraction and keep ignition sources away from the heating area. Wear heat-resistant gloves, eye protection, long sleeves, and suitable respiratory protection when the safety data sheet requires it. OSHA heat guidance emphasizes monitoring exposure, hydration, and recovery during hot work. The advice is relevant, but imperfect for WPC fabrication. Polymer fumes and hot surfaces create different hazards. Stop immediately if the material darkens, bubbles, smokes, or smells sharply. Let the sample cool under restraint, then inspect the inner curve for whitening, splits, and permanent distortion.
How to Bend WPC Safely in 2026?
Bending WPC safely starts with the heat source, not the bending jig. WPC formulations differ widely, so one temperature cannot suit every board. Check the technical sheet and test a small offcut before touching the finished piece. An infrared oven gives even heating. A controlled heat gun can work for short sections. Keep its nozzle moving. Never use an open flame. It can scorch the polymer surface and create irritating fumes.
Use a contact thermometer or infrared thermometer, but verify its reading on a cool sample. Heat both faces gradually when access allows. Uneven heating often causes whitening, ripples, or hidden cracks. Wear heat-resistant gloves, eye protection, and respiratory protection when required by the safety data. Ventilation matters. Set the board in a clean bending form with a generous radius. Do not force a sharp corner while the core remains stiff. Hold the shape with clamps until the material cools completely.
In practical trials, a test coupon saves more material than confidence does. Mark the heated zone, record heating time, and inspect both surfaces after cooling. A dull finish may signal overheating, even when the bend looks smooth. I have seen rushed setups fail because the jig was ready, but the board was not evenly softened. That mistake is easy to repeat. Adjust slowly, and reject any piece with bubbles, deep discoloration, or a burnt odor.
The chart shows typical starting surface-temperature windows for forming common thermoplastic WPC profiles. Steam is limited by atmospheric boiling temperature, while hot air, infrared, and heated platens provide higher and more localized heat. Measure the actual WPC surface temperature, heat gradually, and confirm the polymer type, profile thickness, bend radius, and supplier processing limits before production.
Indicative engineering ranges only: WPC formulations vary significantly. Do not exceed the material supplier’s recommended processing temperature.
Forming WPC safely starts with identifying its wood-to-polymer ratio, moisture content, and reinforcement. These properties change how the profile softens and bends. Do not copy a heating temperature from another product. Check the technical datasheet first, then test a short sample.
Secure the profile on a clean workbench. Mark the bend zone and measure the planned radius. Use a controlled oven or guarded hot-air system, never an open flame. Heat gradually and rotate the piece when practical. The surface should soften evenly, not blister or darken. Place the warm profile into a rounded forming jig. Apply steady pressure, without sudden force. Hold it until fully cooled. ASTM D790 and ISO 178 provide useful flexural testing methods, but they do not replace product-specific forming trials. A 2024 Grand View Research report projects strong WPC market growth through 2030, increasing the need for repeatable fabrication practices. Still, market growth does not prove that every WPC grade bends well.
Tips: Wear heat-resistant gloves, eye protection, and suitable ventilation. Keep a thermometer near the profile, not only inside the oven. Inspect for whitening, cracks, odor, and spring-back. My early assumption was that a longer heating time would improve flexibility. It instead damaged the outer layer. Smaller test pieces are cheaper than correcting a full-length mistake. Record temperature, heating time, radius, and cooling time for every trial. If the profile resists bending, stop and reassess. Forcing it usually creates hidden fractures.
How to Bend WPC Safely in 2026?
Cooling, Securing, and Inspecting the Finished Shape
Bending WPC is not simply a heating exercise. Cooling controls the final geometry. After forming, keep the material inside a rigid jig until it reaches room temperature. Use broad clamps, not narrow metal edges. Narrow pressure points can leave pale marks, dents, or hidden stress lines. A practical working rule is to cool gradually and avoid water shocks unless the product guidance allows them.
Hold it longer than expected.
ASTM D7032 and ASTM D6662 emphasize product-specific performance testing for WPC decking and related components. Their requirements show why one universal bending temperature is unreliable. The USDA Forest Products Laboratory’s Wood Handbook also documents how heat and moisture influence composite dimensions. Measure the part at three points: the center, both ends, and the bend radius. Record the temperature, cooling time, and visible movement. These simple records improve repeatability, although they cannot replace the product’s technical data sheet.
Inspection should continue after release from the jig. Look for whitening, surface ripples, open edges, and spring-back during the next 24 hours. A 2024 industry analysis from Freedonia reported continued growth in WPC applications, increasing the need for consistent fabrication controls. I have found that small spring-back often appears only after overnight storage. That detail is easy to miss. If the curve changes, reduce the load and investigate rather than forcing it tighter. A neat shape is not proof of a sound part.
| Process Stage | Control Dimension | Practical Target or Range | Safe Working Method | Inspection Record |
|---|---|---|---|---|
| Material preparation | Moisture and surface condition | Use clean, dry profiles; avoid bending material with visible water, ice, cracks, or delamination. | Store flat on level supports and allow the profile to reach the workshop temperature before heating. | Record profile size, batch condition, and visible defects before processing. |
| Heating | Surface temperature | Use the profile supplier’s specified range; a common trial window for many WPC profiles is approximately 80–120 °C. | Heat gradually and evenly with a controlled oven or moving hot-air system. Confirm temperature with a calibrated infrared thermometer or contact probe. | Log heating method, measured temperature, and heating time. Do not rely only on heater-set temperature. |
| Temperature control | Temperature uniformity | Keep the difference between measured points as low as practical; a trial limit of about 10 °C or less helps reduce uneven bending. | Measure at the center and both ends of the heated zone. Avoid direct flame and concentrated hot spots. | Record the lowest and highest readings before forming. |
| Forming | Bend radius | Begin with a generous radius, such as 15–20 times the profile thickness, then reduce only after successful trials and specification approval. | Use a smooth, continuous former. Do not force a cold profile or make a sharp single-point bend. | Measure the former radius and compare it with the approved drawing or trial standard. |
| Securing | Fixture contact and restraint | Support the profile continuously or at closely spaced points; prevent twisting, sliding, and local crushing. | Use padded clamps, straps, or a shaped jig. Apply pressure progressively and keep fasteners clear of unsupported edges. | Check for clamp marks, compression, surface whitening, and movement during forming. |
| Cooling | Cooling while restrained | Keep the profile in the fixture until it is stable and near room temperature, typically below about 35–40 °C for handling. | Allow gradual air cooling unless the approved process specifies another method. Avoid cold-water shock, which can cause distortion or surface stress. | Record restraint time, release temperature, and any spring-back observed after release. |
| Dimensional inspection | Shape, radius, and twist | Compare the cooled part with the approved template or drawing; use project tolerances rather than an assumed universal limit. | Measure with a template, radius gauge, straightedge, calipers, or a coordinate measurement system as appropriate. | Record final radius, end-to-end dimensions, twist, bow, and spring-back. |
| Surface and structural inspection | Defects after bending | Reject or review parts showing cracks, splits, permanent whitening, blistering, resin bleed, severe marks, or exposed reinforcement. | Inspect under even lighting and check both the tension side and compression side of the bend. | Photograph defects, identify their location, and retain samples for process review. |
| Process safety | Operator protection | Control hot surfaces, fumes, sharp edges, and stored energy in clamps and fixtures. | Use ventilation, heat-resistant gloves, eye protection, guarded fixtures, and a controlled release procedure. Follow the material safety data sheet. | Document equipment checks, operator training, ventilation status, and any incident or near miss. |
Note: WPC formulations, profile geometry, fillers, and reinforcement vary significantly. The temperature and radius values above are practical starting points for controlled trials, not universal design limits. Always confirm the approved processing window and dimensional tolerances for the specific profile.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru







