Top Custom Zinc Alloy Die Casting Manufacturers?
Choosing among the top Custom Zinc Alloy Die Casting manufacturers requires more than comparing glossy websites or low quotations. A reliable partner must convert a practical design into stable, repeatable parts. Look for experience with zinc alloys, complex tooling, thin walls, threaded features, and tight dimensional requirements. Ask how engineers review drafts before mold production. Small changes in draft angles can prevent expensive delays.
This guide examines manufacturers through evidence, not marketing claims. Useful proof includes sample parts, inspection reports, material certificates, and clear production records. A serious supplier should explain die life, filling behavior, porosity control, trimming, polishing, plating, painting, and secondary machining. Factory visits or live video audits can reveal details photographs hide. Check the inspection area. Check the molds. Check how operators handle rejected parts.
Cost matters, but the lowest quote may not be the lowest project cost. Tooling revisions, unstable cycle times, poor surface finishes, and late shipments can quickly damage a launch schedule. Communication matters too. Can the manufacturer answer technical questions without vague promises? Can it provide measurable corrective actions?
No supplier is perfect.
Even experienced buyers miss small risks during urgent sourcing. A strong manufacturer may still need improvement in documentation or response speed. Therefore, compare verified capabilities, quality controls, delivery history, and after-sales support together. The best choice is not simply the biggest factory. It is the partner that consistently delivers suitable zinc alloy components, explains limitations honestly, and improves when problems appear.
What Is Zinc Alloy Die Casting and Why Is It Used?
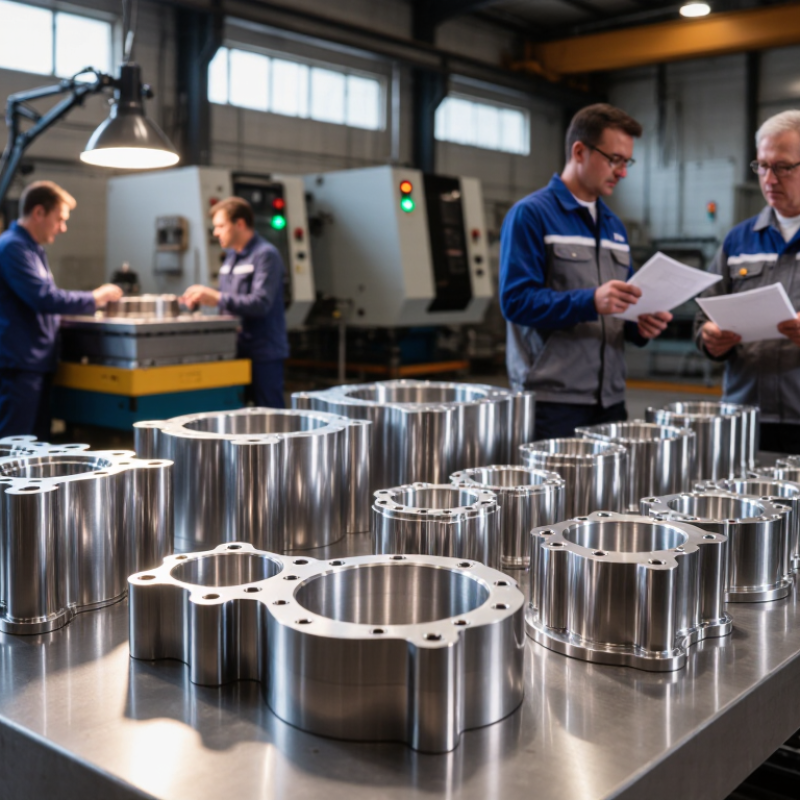
Zinc alloy die casting is a manufacturing process that forms metal under high pressure. Molten zinc enters a reusable steel die and fills its designed cavity. The metal cools quickly, then the solid part is ejected. It sounds simple. In practice, temperature, pressure, venting, and lubrication need close control.
Manufacturers choose this process for small and medium-sized components with detailed shapes. Zinc flows into thin ribs, bosses, slots, and textured surfaces more easily than many metals. This detail can reduce drilling, trimming, and other secondary machining. It also creates a smooth surface that accepts plating, painting, or protective coating. Common parts include handles, housings, brackets, connectors, and decorative hardware. Tight dimensions help components align during assembly.
The process also offers good repeatability and efficient material use. Zinc alloys have useful strength, wear resistance, and dimensional stability. However, die casting is not automatically the best choice. Tooling can require substantial investment, especially for low-volume production. Poor venting may trap air inside the casting. Excessive injection speed can create flash or surface defects. In production reviews, engineers often discover that overly thin walls cause weak areas. A prototype review helps. Wall thickness, alloy selection, cooling design, and inspection methods should be evaluated together. Recycling runner metal can reduce waste, but energy use and coating requirements still deserve careful review.
Key Criteria for Evaluating Custom Die Casting Manufacturers
When choosing a custom zinc alloy die casting manufacturer, examine process evidence rather than polished promises. Grand View Research estimated the global die casting market at about USD 87 billion in 2023. That scale increases competition, but it does not prove quality. Ask for recent sample parts, dimensional reports, alloy certificates, and documented corrective actions. A serious supplier should explain die life, filling simulation, porosity control, and secondary machining limits in practical terms.
Quality systems need measurable proof. Review ISO 9001 certification, inspection equipment calibration, and lot-level traceability. For critical components, request capability studies for key dimensions, including Cpk results where available. Some suppliers may show impressive averages while hiding unstable production. That deserves scrutiny. Production records should connect the zinc ingot, furnace batch, die number, operator, and inspection results. The U.S. Geological Survey reported global zinc mine production of roughly 12.3 million metric tons in 2023, so material availability still requires responsible planning and verified sourcing.
Visit the facility, if possible. Watch how workers monitor melt temperature, remove flash, and separate rejected parts. Ask how defects are classified and contained. The International Zinc Association confirms that zinc can be recycled repeatedly without losing its essential properties, making scrap handling an important evaluation point. However, recycling claims can be vague. Request actual recovery records, not general statements. Compare quoted cycle times with machine tonnage, annual volume, tooling ownership, and realistic maintenance schedules. A low initial price may conceal unstable tooling or excessive post-casting labor.
Leading Custom Zinc Alloy Die Casting Manufacturers by Capabilities
Top Custom Zinc Alloy Die Casting Manufacturers?
Leading Custom Zinc Alloy Die Casting Manufacturers by Capabilities
Leading custom zinc alloy die casting manufacturers are judged by capabilities, not catalog size. Their teams translate drawings into mold-flow checks, draft angles, gate locations, and ejector plans. A practical supplier asks about wall thickness, annual volume, joining methods, and target finish before quoting. That conversation can prevent expensive tooling changes. Tooling capability matters. Experienced engineers balance cycle time, filling behavior, and die life. Still, no simulation replaces a physical trial.
Material control separates dependable production from inconsistent output. Skilled manufacturers select zinc alloys according to strength, dimensional stability, corrosion exposure, and finishing requirements. They monitor melt temperature, injection pressure, and holding time during production. Small process shifts can affect thin ribs or visible surfaces. Sample parts should be checked with coordinate measuring equipment, gauges, and documented inspection plans. Results need traceability, not vague assurances.
Strong suppliers also manage secondary operations. These may include trimming, CNC machining, tapping, polishing, plating, painting, and assembly. Their capabilities should match the product’s real use, not only its appearance. A pilot run can reveal burrs, sink marks, or thread damage before full production. That step may feel slow. It is usually cheaper than correcting thousands of parts. Honest manufacturers also explain limitations, revise designs when necessary, and report defects without hiding them.
How to Compare Quality, Materials, Tooling, and Production Services
Choosing a top custom zinc alloy die casting manufacturer requires more than comparing quoted prices. Ask for inspection records, process capability data, and traceability from batch to shipment. Experienced teams should explain porosity control, dimensional tolerances, surface defects, and corrective actions clearly. A sample housing should show clean edges, stable wall thickness, and consistent plating.
Material selection affects strength, weight, finish, and cost. Common zinc alloys offer different balances of hardness, ductility, and casting performance. Request the alloy grade, chemical composition report, and recycled content details. Do not accept “zinc alloy” as a complete specification. It is too vague. A reliable manufacturer can connect your load requirements to a suitable material and explain trade-offs without hiding limitations.
Tooling quality often reveals production maturity. Review mold steel, expected tool life, cooling layout, venting, and maintenance responsibility. A detailed tool trial should include first-article measurements, not only attractive photographs. Production services matter equally. Check die casting capacity, trimming, CNC machining, polishing, coating, assembly, packaging, and inspection equipment.
Visit the factory when possible, or request a live video audit. I have seen promising samples fail during volume production because process controls were weak. That risk deserves attention. Even strong suppliers may miss a cosmetic defect occasionally, so their response speed, root-cause analysis, and replacement policy matter.
Questions to Ask Before Choosing a Die Casting Manufacturer
Choosing among top custom zinc alloy die casting manufacturers requires more than comparing prices. Ask how many years they have handled similar parts, especially thin walls, deep cavities, or visible surfaces. Request sample parts from comparable projects. A polished sample proves little if the alloy, tooling, and finishing process differ.
Ask which zinc alloy grades they recommend and why. A professional manufacturer should explain strength, corrosion resistance, dimensional stability, and surface appearance in practical terms. Confirm the die casting machine range, mold design process, and expected tolerance. Also ask how they control porosity, flash, burrs, and warpage. These small defects can disrupt assembly. Ask to review inspection records, material certificates, and calibration practices. Certifications matter, but current evidence matters more.
Tips: Request a written production timeline, including tooling trials and approval stages. Clarify who owns the mold and who pays for modifications. Ask how rejected parts are handled and whether corrective reports are shared. Do not accept vague answers. No supplier is perfect. A manufacturer that admits a limitation may be more reliable than one promising everything. I would also ask for references from projects with similar volume and finishing needs. Sometimes the cheapest quote excludes secondary machining, coating, packaging, or inspection. Read every line carefully.
Top Custom Zinc Alloy Die Casting Manufacturers: Material Capability Comparison
Before choosing a die casting manufacturer, ask whether its process can consistently meet the mechanical requirements of your selected zinc alloy. The chart shows representative room-temperature tensile and yield strengths for commonly used zinc die casting alloys; actual values vary by standard, casting design, and testing method.
Values shown in MPa. Confirm alloy certification, testing procedures, dimensional capability, surface finishing, and quality controls with each manufacturer.