Buying a Mechanical Flange for an international project involves more than comparing prices. A flange may look correct in a product image, yet fail during installation because its bore, pressure class, or facing type is wrong. Small differences matter. A few millimeters can disrupt an entire piping connection.
Global buyers must examine material grades, dimensions, tolerances, temperature limits, and corrosion resistance. They should also compare the supplier’s drawings with the project specification. Reliable manufacturers can provide inspection reports, material certificates, dimensional records, and traceable batch information. These documents support confidence, but they should not replace physical verification. A polished datasheet can still hide an unsuitable product.
Ask specific questions early. Confirm whether the flange matches the pipe schedule and connection standard. Check how the supplier protects machined faces during transport. Wooden crates, sealed surfaces, and moisture-resistant wrapping can prevent costly damage at a busy port. Delivery terms, export packaging, and inspection responsibilities also deserve attention. They often cause avoidable delays.
No checklist catches everything. In practice, buyers may overlook gasket compatibility or assume that similar standards are interchangeable. That assumption can become expensive. The ten tips in this guide focus on practical checks, supplier evidence, technical accuracy, and purchasing risks. They are designed for engineers, distributors, and project teams sourcing Mechanical Flange products across borders. Careful review may feel slow, but replacing an incorrect flange after shipment is far slower.
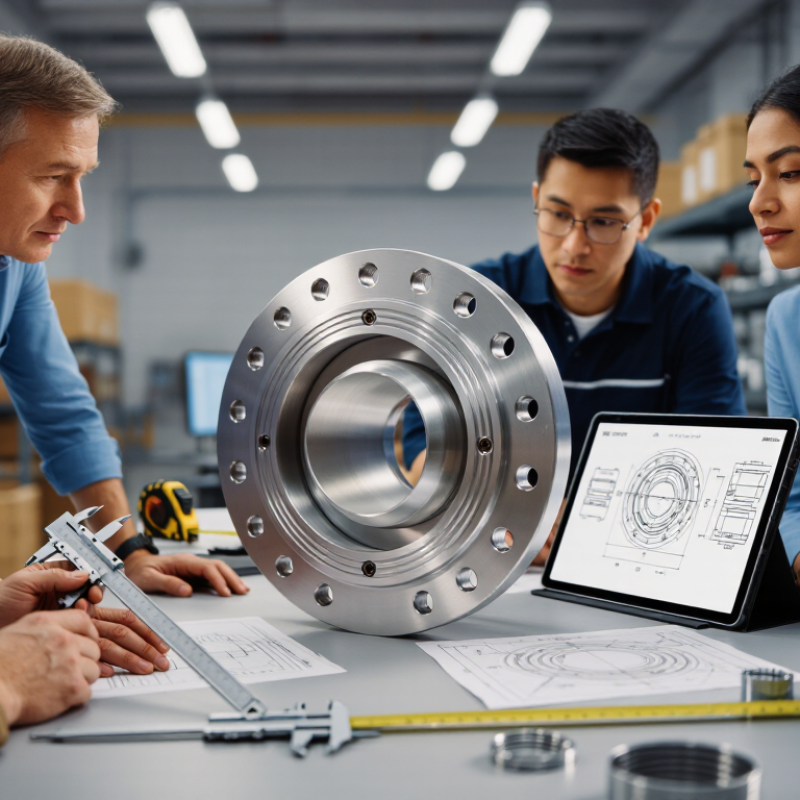
Before requesting quotations, define the flange type for the actual connection. Weld neck, slip-on, threaded, socket weld, and blind flanges serve different purposes. A blind flange closes a pipeline, while a weld neck flange supports demanding pressure and temperature conditions. Choosing by appearance alone is risky.
Record the nominal pipe size, outside diameter, bore, bolt-hole pattern, and flange thickness. Confirm the pressure class and facing type, such as raised face or flat face. Small dimensional differences can prevent assembly. Ask for dimensional drawings before production starts. Do not rely only on a familiar catalog description.
Application details matter just as much. State the fluid, operating temperature, pressure range, corrosion exposure, and installation environment. A flange handling seawater may require better corrosion resistance than one used for dry air. Check the material certificate, inspection records, and applicable manufacturing standard. Request traceable marking on each piece. This improves receiving control.
A common mistake is treating the flange as an isolated component. The gasket, bolts, pipe wall, and mating flange must work together. I would also question unclear specifications, even when the delivery deadline is tight. Speed can hide expensive errors. Recheck the data with the installer or engineer before purchase. Five minutes of review may prevent a shipment that cannot be fitted.
When buying mechanical flanges across borders, material grade is not a line to accept blindly. Ask for the heat number, chemical analysis, mechanical test results, and traceability documents. A certificate should match the stamped grade on the flange. Check carbon, chromium, nickel, and molybdenum when corrosion or temperature matters. Small differences can change welding behavior and service life. I have seen paperwork list one grade while the marking showed another. That mistake was caught before installation. Not every shipment is checked so carefully.
Confirm the governing standard and its edition. Dimensions may look similar, while bolt holes, facing, and thickness differ. Compare the flange drawing with the mating pipe, gasket, bolts, and valve. Do not mix standards because the parts appear to fit. Verify the pressure class or PN rating at the actual design temperature. A rating table should show allowable pressure, material group, and temperature limits. Ask the supplier to identify the calculation basis. “High pressure” is not a technical rating.
Use an independent inspection plan for critical service. Measure outside diameter, bore, thickness, bolt-circle diameter, and face finish. Photograph markings before packing. Review impact tests when low-temperature service is possible. I once treated a familiar standard as sufficient evidence; it was not. Recheck assumptions, especially when translated documents use vague terms. Keep the approved drawing, certificates, inspection report, and packing list together. This record makes disputes easier to investigate.
| No. | Buying Checkpoint | What to Verify | Practical Reference or Example | Recommended Evidence |
|---|---|---|---|---|
| 1 | Confirm the flange standard | Identify the dimensional standard before ordering, including outside diameter, bolt circle, bolt-hole quantity, bore, thickness, and facing dimensions. | ASME B16.5 covers flanges and flanged fittings from NPS 1/2 through NPS 24. ASME B16.47 covers larger nominal sizes. EN 1092-1 uses DN sizes and PN pressure designations. | Approved dimensional drawing, purchase specification, and applicable standard edition. |
| 2 | Verify the material grade | Check that the flange material matches the process fluid, design temperature, corrosion conditions, and piping material specification. | ASTM A105 is commonly used for forged carbon-steel flanges. ASTM A182 F304/F304L and F316/F316L are common stainless-steel forging grades. Grade selection must follow the project specification. | Material test certificate, heat number, chemical analysis, mechanical test results, and marking photographs. |
| 3 | Check pressure class or PN rating | Confirm the required pressure designation and ensure it is suitable for the selected material and operating temperature. Do not treat different designation systems as automatically interchangeable. | ASME B16.5 includes Class 150, 300, 400, 600, 900, 1500, and 2500. EN 1092-1 commonly uses PN 6, PN 10, PN 16, PN 25, PN 40, PN 63, PN 100, and PN 160. | Design pressure and temperature sheet, pressure-temperature rating table, and engineering approval. |
| 4 | Match the flange face and gasket | Confirm the facing type, surface finish, gasket style, and gasket dimensions. The flange face and gasket must be compatible with the service and bolting method. | Raised Face (RF), Flat Face (FF), and Ring-Type Joint (RTJ) are common face configurations. RTJ flanges require the correct ring-groove dimensions and ring type. | Facing drawing, gasket specification, surface-finish report where required, and gasket certificate. |
| 5 | Validate nominal size and bore | Check nominal pipe size, outside diameter, wall thickness or bore, schedule, and whether the flange is weld neck, slip-on, socket weld, threaded, blind, or lap joint. | A weld-neck flange bore should be compatible with the connected pipe inside diameter and wall profile. A blind flange must be rated for the required pressure and have the specified thickness. | Pipe data sheet, flange dimensional drawing, bore measurement report, and line class specification. |
| 6 | Review bolting requirements | Confirm bolt diameter, length, quantity, thread form, nut grade, coating, washer requirements, and tightening method. Bolting must be selected for the temperature and service environment. | ASTM A193 B7 studs with ASTM A194 Grade 2H nuts are common in many carbon-steel applications, but sour service, low-temperature service, or high-temperature service may require different requirements. | Bolting material certificates, thread inspection report, coating certificate, and approved tightening procedure. |
| 7 | Assess corrosion and service conditions | Consider chloride exposure, sour gas, seawater, chemicals, cyclic loading, erosion, low temperature, and high temperature. Confirm whether impact testing, hardness limits, or special corrosion controls apply. | Stainless grades such as 316/316L may offer improved resistance to chlorides compared with 304/304L, but material suitability depends on concentration, temperature, exposure time, and design requirements. | Process-fluid composition, corrosion study, NACE or project compliance statement where applicable, and hardness test results. |
| 8 | Confirm manufacturing and inspection controls | Verify forging or manufacturing route, heat treatment, dimensional tolerances, visual condition, surface quality, and any required nondestructive examination. | Typical inspection requirements may include visual inspection, dimensional inspection, hardness testing, and, when specified, ultrasonic testing or liquid penetrant testing. The purchase specification determines the applicable inspection scope. | Inspection and test plan, dimensional inspection report, heat-treatment chart, NDE reports, and final inspection release. |
| 9 | Require traceability and correct marking | Ensure each flange remains traceable to its material heat, grade, size, pressure class or PN rating, face type, and applicable standard throughout production and shipment. | Typical permanent or low-stress markings include manufacturer identification, material grade, nominal size, rating, standard designation, and heat number, subject to the applicable standard and project requirements. | Heat-number traceability map, marking photographs, packing list, material certificates, and certificate of conformity. |
| 10 | Check testing, packaging, and delivery details | Define required pressure tests, test medium, acceptance criteria, preservation, end protection, labeling, export packaging, and documentation before production begins. | Flanges are not automatically interchangeable or pressure-tested under identical rules. Testing and acceptance should follow the applicable standard, project specification, and service requirements. Protect machined faces and RTJ grooves from impact and corrosion during transport. | Approved quality plan, test reports, certificate of conformity, packing photos, inspection release note, and shipping marks. |
When buying mechanical flanges globally, verify the manufacturer before reviewing price. Request legal registration, production scope, quality certificates, inspection procedures, and recent audit records. The ISO Survey 2023 reported 1,265,216 ISO 9001 certificates worldwide. However, certification confirms a management system, not every flange’s quality. Ask whether the certificate covers the actual facility producing your order.
Product traceability should follow each flange from steel receipt to final inspection. Check heat numbers, material test reports, forging records, machining dates, dimensions, pressure ratings, and non-destructive testing results. The heat number on the flange should match the mill certificate and inspection report.
Small mismatches matter. They can expose weak document control.
The World Bank’s 2023 Logistics Performance Index collected responses from 4,090 trade professionals in 139 countries. Its findings highlight the practical importance of reliable logistics information across borders. Require digital records with revision control, but do not trust software alone. A barcode can be scanned incorrectly. During supplier audits, compare random flange markings with original production records. Photograph the marking, packaging, and certificate set. A clean document package may still conceal an incomplete process. That possibility deserves attention.
10 Mechanical Flange Buying Tips for Global Buyers
A low flange price can hide costly delays. Compare offers by material grade, pressure class, machining tolerance, and inspection scope. UNCTAD’s Review of Maritime Transport reports that over 80% of global trade moves by sea. Therefore, ocean freight terms can change your landed cost sharply. Ask for separate prices under FOB, CIF, and DDP terms. Confirm insurance, destination charges, customs responsibilities, and currency risks.
Tip: Request a shipment timeline with production, inspection, packing, and port dates. The World Bank’s 2023 Logistics Performance Index shows major differences in customs efficiency and shipment reliability worldwide. A supplier promising seven days may mean seven production days only. I have seen buyers miss project deadlines by overlooking inspection queues. Build a practical buffer, even when the factory resists it.
Packaging deserves equal attention. Flanges need rust protection, sealed bags, timber crates, edge guards, and clear heat-number labels. Ask for crate dimensions, gross weight, stacking limits, and photographs before dispatch. Compare air, sea, and multimodal shipping using total delivered cost, not freight alone. UNCTAD also highlights how maritime disruptions can extend routes and increase uncertainty. My imperfect rule is simple: cheap freight is useful only when the delivery remains predictable.
Inspecting a physical sample is more reliable than approving a polished product photograph. Ask the supplier to send one flange from the planned production process. Measure the outside diameter, thickness, bolt-hole spacing, and bore with calibrated tools. Compare every result with the approved drawing and required standard. Small defects matter.
Check the sealing face under bright light. Look for scratches, dents, uneven machining, rust, or damaged threads. Test the gasket fit without forcing it. Confirm the material grade through heat numbers and traceable mill certificates. For pressure service, review the pressure class, temperature range, and test records. An independent inspection can verify hardness, dimensions, and surface quality before shipment.
I have learned that visual checks alone can mislead. My earlier inspections focused too heavily on machining marks. That was a weak assumption. Request sample photos from several angles, but do not treat them as final evidence. Record measurements in a signed inspection report, including acceptable tolerances and rejected features. Keep a retained sample when possible. It helps resolve disputes later. Before finalizing the order, confirm that production parts will match the approved sample, material documents, packaging method, and marking details. Vague promises create avoidable risk.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru