A Puree Pouch Filling Machine is built for a deceptively difficult task: moving thick, smooth food into flexible pouches without splashing, leaking, or trapping air. Fruit puree, baby food, sauces, and yogurt-like products behave differently from free-flowing liquids. Their viscosity changes with temperature, fiber content, and processing conditions.
PMMI’s 2024 State of the Industry report identifies automation, labor availability, and flexible packaging as important machinery investment pressures. Smithers’ flexible packaging research also points to continued demand for lightweight, convenient formats. These trends help explain why pouch systems now appear across food, beverage, and nutrition production lines. The machine usually feeds empty pouches, opens them, doses a measured volume, seals the top, and removes finished packs. Some systems add nitrogen flushing, cleaning-in-place circuits, checkweighers, or vision inspection.
“It is a product-handling problem before it is a speed problem,” says Jorge Izquierdo, Vice President of Market Development at PMMI, describing a principle widely applied in automated packaging design. The wording is simple. The engineering is not.
A reliable Puree Pouch Filling Machine must control pump pressure, filling temperature, nozzle movement, and seal-jaw heat together. Even a small puree smear can weaken a seal. A few trapped air bubbles may distort the pouch. Minor errors become expensive at high output.
Still, the picture is not perfect. Reported machine speeds often depend on product flow, pouch material, and operator discipline. Laboratory results may not survive a busy factory floor. This guide examines how the equipment works, where failures begin, and which specifications deserve closer questioning before purchase.
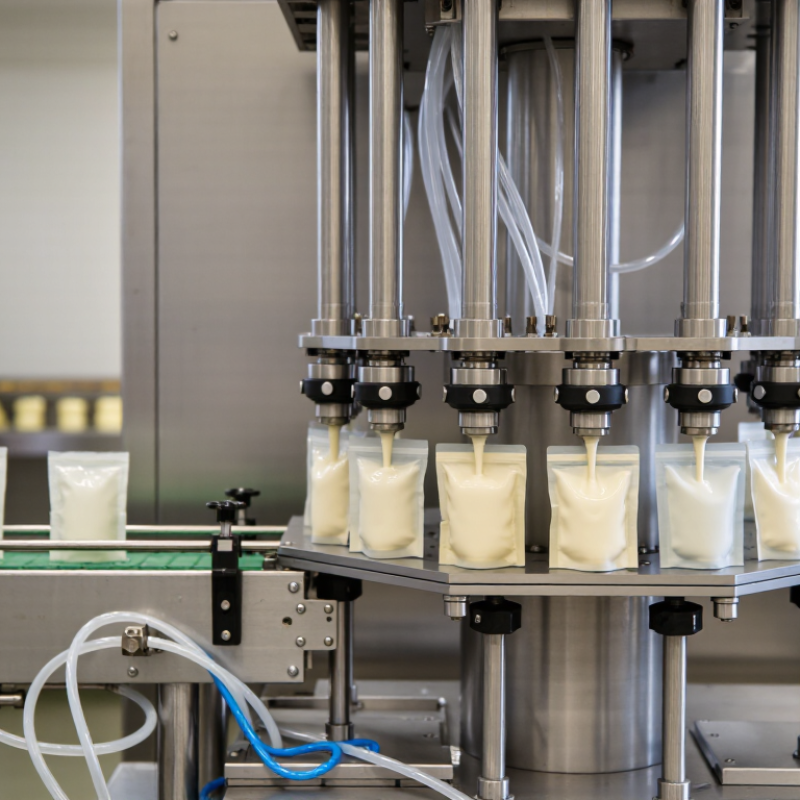
A puree pouch filling machine is industrial equipment designed to measure and seal smooth foods inside flexible pouches. It handles products such as fruit puree, vegetable blends, sauces, and baby food. Its main purpose is controlled packaging. Each pouch should receive a consistent amount with minimal product loss.
The process usually begins with a food-grade hopper holding the prepared puree. A pump or piston system moves the product toward the filling nozzle. Sensors help position each pouch before filling starts. The machine then dispenses a measured volume and seals the opening with heat or pressure. Sealing temperature, dwell time, and film condition must match the packaging material. Small errors can cause leaks.
Cleanability is equally important. Product-contact parts should be removable or easy to wash and inspect. Operators typically check fill weight, seal strength, temperature readings, and pouch appearance during production. These checks support traceability and reliable quality control. A machine may run quickly, but speed alone does not prove good performance. That matters.
The definition sounds simple, yet real operation is less predictable. Puree viscosity can change with temperature, fiber content, and recipe variation. A setting that works in the morning may need adjustment later. This is where practical experience becomes valuable. Operators must watch for dripping nozzles, uneven seals, trapped air, and underfilled pouches. Automation reduces repetitive work, but it does not remove the need for trained judgment. Mistakes still happen.
| Data Dimension | Typical Information | Practical Purpose |
|---|---|---|
| Definition | A puree pouch filling machine is packaging equipment that doses fruit, vegetable, baby-food, sauce, or other semi-liquid puree into preformed flexible pouches and seals them. | Automates accurate filling and closure while reducing manual handling. |
| Primary Packaging Format | Common formats include spouted pouches, flat pouches, stand-up pouches, and pouches with fitments or caps. | The machine configuration depends on pouch shape, opening design, material, and closure type. |
| Main Product Types | Smooth purees, pulpy purees, fruit preparations, vegetable blends, baby food, dessert fillings, and thick sauces. | Product texture and particle size determine the filling valve, pump, and piping requirements. |
| Typical Filling Principle | A pump or volumetric dosing system transfers a measured quantity of puree from a hygienic product hopper into each pouch. | Controlled dosing supports consistent net weight and reduces product giveaway. |
| Basic Operating Sequence | Pouch loading → pouch opening → optional pouch detection → puree dosing → headspace control → spout or top sealing → discharge. | A programmed sequence coordinates each station to maintain repeatable production. |
| Product Contact Materials | Food-contact stainless steel, commonly grades such as 304 or 316, along with food-compatible seals, hoses, and gaskets. | Smooth, corrosion-resistant surfaces support hygienic production and easier cleaning. |
| Typical Fill Volume | Approximately 50–2,000 mL per pouch, depending on the pouch format and machine design. | The actual range must be matched to the pouch size, product viscosity, and dosing system. |
| Typical Production Capacity | Small and medium systems commonly operate from about 10 to 60 pouches per minute; higher outputs require specialized multi-lane or rotary designs. | Actual throughput varies with pouch size, filling volume, sealing method, product properties, and operator loading speed. |
| Dosing Accuracy | Well-adjusted volumetric systems may commonly achieve approximately ±1% to ±2% of the target fill, subject to product and equipment conditions. | Accuracy depends on calibration, temperature, viscosity, air entrainment, particle content, and pump selection. |
| Suitable Viscosity Range | Suitable products may range from pourable liquids to thick, shear-sensitive purees; exact viscosity limits depend on the pump and valve design. | High-viscosity or particulate products may require larger passages, a positive-displacement pump, or agitator. |
| Pouch Handling | Pouches can be loaded manually or supplied from an automatic magazine; grippers, guides, sensors, and clamps position each pouch. | Reliable positioning prevents misfills, wrinkles, open seals, and pouch jams. |
| Sealing Methods | Common methods include heat sealing for flexible laminates and cap or spout sealing for reclosable pouches. | Seal temperature, pressure, dwell time, and cleanliness must be controlled to achieve leak-resistant closures. |
| Temperature Control | Puree may be filled cold, ambient, or hot, depending on the product process and packaging material; heat-sensitive products require controlled conditions. | Stable temperature helps maintain viscosity, dosing consistency, product quality, and seal performance. |
| Common Controls and Sensors | PLC or controller, touch interface, pouch-presence sensor, fill-level or dosing feedback, temperature controller, and fault alarms. | Controls synchronize machine actions and help identify missing pouches, low product levels, or sealing faults. |
| Cleaning and Sanitation | Product-contact parts should be accessible for cleaning; systems may use removable components, flush ports, or clean-in-place arrangements. | Effective sanitation reduces residue buildup and microbiological contamination risk. |
| Quality Checks | Typical checks include fill weight, seal integrity, pouch appearance, leakage, cap placement, and foreign-particle control. | Routine inspection helps verify package safety, compliance, and consistent consumer presentation. |
| Key Advantages | Consistent portioning, reduced labor, compact packaging, lower product exposure, faster changeovers, and improved production repeatability. | Useful for producers seeking scalable and hygienic pouch packaging operations. |
| Main Limitations | Performance can be affected by pulp size, fiber content, viscosity changes, trapped air, pouch variability, and inadequate cleaning. | Product trials and equipment adjustment are important before full-scale production. |
| Best-Fit Applications | Shelf-stable, refrigerated, or frozen puree products packaged in flexible pouches, subject to the required thermal process and food-safety controls. | The filling machine handles packaging; pasteurization, sterilization, refrigeration, or freezing must be designed separately as required. |
A puree pouch filling machine transfers prepared food into flexible pouches with controlled accuracy. The hopper holds the puree and keeps it moving through gentle agitation. This reduces settling when the mixture contains fruit fibers, vegetable pieces, or starch. A sanitary pump then pushes the puree toward the filling nozzles. Pump speed and valve timing affect both portion weight and splashing.
The filling nozzles dispense measured amounts into opened pouches. Sensors check pouch position before filling begins. A sealing unit then applies heat and pressure to close each pouch securely. The control panel coordinates these actions through programmed settings. Temperature sensors monitor the sealing bars, while pressure controls help produce consistent seals. In real production, puree viscosity can change during a shift. That variation may require slower pumping or wider valve timing. The machine is precise, but it is not magically self-correcting. Operators still need to inspect seals, weights, and product buildup. Cleaning features, such as removable contact parts, also support hygiene and maintenance.
Tips: Keep the hopper level stable during filling. Check nozzle alignment before a production run. Do not ignore small drips; they can become sealing defects. Test a few pouches after every major setting change. A short inspection often prevents a costly batch problem.
A puree pouch filling machine is a controlled system that portions thick food products into flexible pouches. It combines product feeding, pouch handling, filling, sealing, and inspection. Puree behaves differently from water because its viscosity can change with temperature, fiber, and recipe consistency.
The process starts when empty pouches enter the machine and are positioned under the filling nozzle. Sensors confirm their location before the pump delivers a measured volume. A piston or servo-driven pump usually controls the dose. The nozzle must move smoothly to reduce splashing and trapped air. A small error matters. Operators often check the first filled pouches by weight, appearance, and seal condition.
After filling, heated sealing jaws close the pouch opening under controlled pressure and temperature. The machine then releases the sealed pouch for trimming, coding, or packaging. Sensors can detect missing pouches, weak seals, and incorrect filling levels. In real production, settings need adjustment. Puree may flow slowly during a cool shift and quickly after warming. Even experienced operators can overlook residue near the seal area. Regular cleaning, calibration, and documented checks help maintain reliable results. The exact sequence also depends on pouch design, product texture, and required output.
A puree pouch filling machine doses smooth food into flexible pouches before sealing them. Its main parts include a hopper, dosing system, pouch holder, sealing jaws, and control panel. Common machine types serve different production needs.
Piston fillers handle thick products, such as fruit puree, vegetable blends, and baby food. They deliver accurate volumes with limited product damage. Servo pump fillers suit thinner purees and frequent recipe changes. Premade pouch machines work well for medium production runs and many pouch shapes. Form-fill-seal machines create pouches from film rolls. They support higher output and lower packaging costs, but setup requires more technical control.
Smithers’ report, The Future of Global Flexible Packaging to 2028, forecasts flexible packaging demand above 300 billion dollars by 2028. This growth increases pressure for cleaner dosing, faster changeovers, and reliable seals. Yet, bigger output is not always better. A small producer may waste more material with an oversized line. I would review pouch size, puree viscosity, filling accuracy, and cleaning time before choosing equipment. Operators should also test pulpy recipes, because fruit fibers can interrupt valves and create uneven fills.
Tips: Keep the hopper level stable. Check seal temperature during every shift. Use water trials before product trials. Record foaming, dripping, and pouch deformation. These details often expose problems earlier than final inspection.
A puree pouch filling machine measures, dispenses, and seals fruit, vegetable, baby-food, and sauce purees in flexible pouches. The chart compares typical nominal throughput levels for common machine types.
How to read the chart: Manual and semi-automatic systems suit small batches and frequent product changes. Intermittent rotary machines are commonly used for medium-scale production, while continuous rotary and inline systems are better suited to high-volume applications. Actual output depends on pouch size, puree viscosity, filling accuracy, sealing method, and the number of filling lanes.
A puree pouch filling machine portions soft foods into flexible pouches with controlled speed and accuracy.
It usually draws puree from a sanitized hopper through a pump or dosing system. The pouch opens, receives the measured product, and passes to heated sealing jaws. Sensors monitor pouch position, fill volume, and seal timing. The process looks simple. Small errors can spread quickly.
Hygiene begins with the product-contact path. Operators should dismantle nozzles, valves, hoses, and hopper surfaces according to a documented cleaning procedure. Use approved detergents, suitable water temperatures, and verified rinsing steps. Visual inspection alone is not enough. Tiny puree residues may remain inside seals or narrow fittings. Drying is also important because trapped moisture can support microbial growth. Clean hands, protective clothing, and controlled product exposure reduce handling risks. In practice, rushed cleaning remains a common weakness.
Quality control should include fill-weight checks, seal-strength tests, and inspections for wrinkles, leaks, or trapped puree. Record samples from the beginning, middle, and end of each run. Maintenance teams should inspect gaskets, pumps, sensors, and sealing bars at scheduled intervals. Replace worn parts before they cause inconsistent filling. Food-safe lubricants must stay away from product-contact areas. Calibration records help identify gradual drift. Records reveal patterns. Yet no checklist replaces trained judgment; procedures may need revision when real production conditions change.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru