Seamless Pipe is made without a longitudinal weld, using processes such as piercing a heated billet and reducing it into a hollow tube. The result is not automatically stronger in every application. Performance depends on steel grade, dimensions, manufacturing quality, and operating conditions. A pipe destined for a refinery needs different checks from one carrying water through a building.
The World Steel Association reported 1,892.2 million tonnes of crude steel production worldwide in 2023. That figure shows the scale of steelmaking, not seamless-pipe demand; it should not be mistaken for a market-size estimate. For design context, materials scientist Michael F. Ashby writes in Materials Selection in Mechanical Design: “Design is the process of translating a new idea or a market need into the detailed information from which a product can be manufactured.” His point applies here: choosing a pipe means matching material and form to a real service, not relying on the word “seamless.”
This guide explains how seamless pipe is produced and how common types differ. Carbon-steel, alloy-steel, and stainless-steel grades each serve distinct conditions. Hot-finished and cold-drawn pipes also differ in dimensions and surface finish. Small details matter. A temperature range, corrosion exposure, or pressure requirement can change the appropriate choice. Standards such as ASTM A106 and API 5L help define requirements, but the applicable specification must be checked against the project. That step is easy to rush. It deserves a closer look.
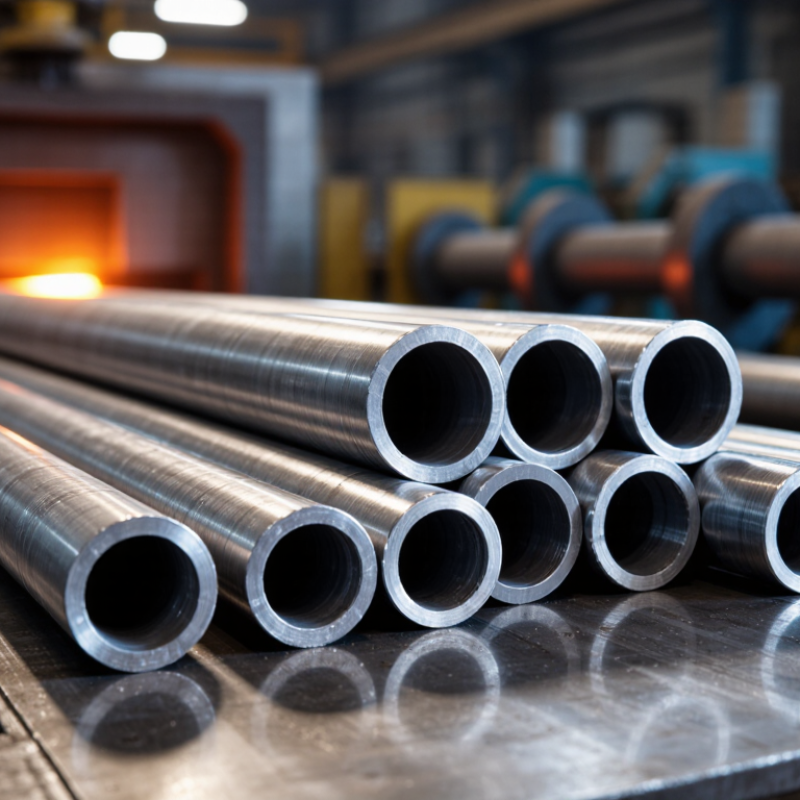
A seamless pipe is a tubular product made without welding together a strip or plate. It usually begins as a solid steel billet, heated and pierced to create a hollow center. The hollow is then rolled or drawn to reach the required diameter and wall thickness. No weld seam runs along its length. That is the defining feature.
The process can produce pipes for high pressure, heat, or demanding service, but “seamless” does not mean flawless. Manufacturing may leave variations in wall thickness, surface finish, or straightness, so inspection and specifications still matter. A pipe’s material grade, dimensions, and test results help determine whether it suits a particular system. It is tempting to assume seamless always means stronger; that claim is too broad. Welded pipe can also perform reliably when properly specified. The right choice depends on operating conditions, not on the label alone. Details matter. A careful buyer should compare documented requirements with the actual pipe, rather than relying on appearance or a single manufacturing term.
Seamless pipe production starts with a solid steel billet, inspected for surface defects and heated until it can be formed. A piercing mill presses a pointed plug into the billet while rolls rotate and stretch it. The metal opens into a hollow shell, with no welded seam. It is a loud, forceful stage. Temperature matters: an unevenly heated billet may deform inconsistently.
The hollow shell then passes through rolling equipment that reduces its wall thickness and adjusts its diameter. A mandrel supports the inside as the pipe lengthens. Sizing rolls refine the outside dimensions. Some products are made by cold drawing after cooling; this can improve dimensional accuracy and surface finish, but adds processing steps. The pipe is then cooled, straightened, and cut to length.
Manufacturing does not end when the pipe looks round. Workers may check dimensions, surface condition, and material properties, with inspection methods selected for the grade and intended service. Ultrasonic testing can help reveal internal flaws. A smooth exterior is not proof of sound internal quality. Pipe specifications and process controls matter, and no single manufacturing route suits every size or application. Details deserve a second look.
Seamless pipe is made by piercing a solid billet, leaving no longitudinal weld seam. Available types are often grouped by manufacturing process and material. These categories describe different things, which can make product listings confusing.
Hot-finished seamless pipe is shaped at high temperatures and is common in general industrial service. Cold-drawn or cold-finished pipe is processed further at lower temperatures. It often offers tighter dimensional control and a smoother surface. Carbon-steel types are used in many pressure and structural applications. Alloy-steel types can be selected for elevated temperatures or demanding mechanical conditions. Stainless-steel types provide better resistance to corrosion in suitable environments. No single type fits every job.
Tips: Compare the specified grade, outside diameter, wall thickness, and required tolerances before choosing. Check the applicable product standard and service conditions with a qualified supplier or engineer. A polished surface does not automatically mean better performance; it depends on the application.
Seamless pipe is made without a welded seam. It is commonly produced by piercing a solid billet and then rolling or drawing the hollow shape to the required dimensions. Available options vary by manufacturing process, material, and intended service.
| Type | How It Is Classified or Made | Typical Characteristics | Common Applications |
|---|---|---|---|
| Hot-finished seamless pipe | The pierced billet is formed and finished while hot. | Suitable for a broad range of sizes and wall thicknesses; dimensional tolerances and surface finish depend on the product specification. | General industrial piping, structural uses, and high-temperature service when specified for the application. |
| Cold-drawn or cold-finished seamless pipe | Hot-worked pipe is further drawn or sized at a lower temperature. | Often offers closer dimensional tolerances and a smoother surface than hot-finished pipe; cold working can increase strength and hardness. | Precision components, hydraulic systems, instrumentation, and mechanical applications. |
| Carbon steel seamless pipe | Classified by its carbon-steel composition; supplied in hot-finished or cold-finished forms. | A widely used, economical steel option. Corrosion resistance is limited without suitable protection or service conditions. | Water, oil, gas, and general process lines, subject to the applicable grade and design requirements. |
| Alloy steel seamless pipe | Steel containing specified alloying elements, such as chromium or molybdenum, in addition to carbon. | Selected grades can provide improved strength or resistance to elevated-temperature service; performance depends on composition and heat treatment. | Power generation, boilers, refineries, and other high-temperature or pressure applications. |
| Stainless steel seamless pipe | Made from stainless steel grades containing at least 10.5% chromium by mass. | Chromium helps form a passive surface layer that provides corrosion resistance; resistance varies by grade and environment. | Food processing, chemical processing, water systems, and corrosive-service piping when the grade is appropriate. |
| Duplex stainless steel seamless pipe | A stainless-steel family with a mixed austenitic-ferritic microstructure. | Many duplex grades combine higher strength than common austenitic stainless grades with good resistance to chloride stress-corrosion cracking; exact performance is grade-specific. | Marine, offshore, chemical, and other demanding chloride-containing environments. |
Selection should account for the required dimensions, pressure and temperature, corrosion environment, applicable product standard, and material grade. “Seamless” describes the manufacturing form; it does not by itself specify a pipe’s strength or suitability for a particular service.
Seamless pipe is formed by piercing a solid steel billet, leaving no longitudinal weld seam. That matters. But “seamless” does not mean defect-free or automatically suitable for every pressure and temperature. Grade, heat treatment, dimensions, and inspection also shape performance. ASTM A106 covers seamless carbon-steel pipe for high-temperature service, while ASTM A335 covers seamless ferritic alloy-steel pipe. ASTM A312 covers stainless pipe in both seamless and welded forms, so the standard number alone does not confirm the manufacturing method.
Material chemistry changes corrosion resistance and service limits. Type 304 stainless steel suits many general environments; Type 316 adds molybdenum, which improves resistance to certain corrosive conditions. The World Stainless Association’s 2024 production statistics report 58.4 million tonnes of global stainless crude-steel output in 2023. That figure describes steel production, not pipe supply. For dimensions, ASME B36.10M and B36.19M define pipe sizing conventions; design codes address different requirements. A specification can still leave room for confusion. Buyers should verify grade, manufacturing route, schedule, test requirements, and intended service together—not rely on “seamless” as a quality guarantee.
Seamless pipes are used where pressure, temperature, or cyclic loading makes reliable wall performance important. Common settings include boiler lines, heat exchangers, hydraulic systems, and oil and gas facilities. A pipe carrying hot steam through a plant, for example, must withstand both operating pressure and repeated temperature changes. The lack of a longitudinal weld can be useful, but it does not make every seamless pipe suitable for every duty.
Selection starts with the service conditions. Engineers check the fluid, operating temperature, design pressure, corrosion risk, and expected loads. They then specify the material grade, outside diameter, wall thickness, and required tolerances. For corrosive service, the fluid’s chemistry matters; for high heat, strength at operating temperature matters. Details matter. A pipe that fits the drawing may still be wrong for the process.
Applicable product standards and inspection requirements should also be confirmed before purchase. Depending on the application, checks may include dimensional inspection, mechanical testing, and nondestructive examination. Review material certificates and traceability records, too. These steps help verify what was supplied, though paperwork alone cannot replace competent engineering review. In practice, selection can involve trade-offs between corrosion resistance, availability, weight, and cost. It is easy to focus on pressure ratings and miss installation conditions, so the full operating picture deserves a second look.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru