A Shuttle Rotomolding Machine is a practical system for producing strong, hollow plastic parts with consistent wall coverage. It uses two or more mold stations that move between heating and cooling areas. While one mold heats, another can be opened, loaded, or unloaded. This reduces idle time and supports steady production.
The process begins with measured polymer powder inside a hollow mold. The shuttle carries the closed mold into an oven, where controlled heat softens the material. Two-axis rotation spreads the molten polymer across every internal surface. The mold then moves to a cooling station. Air, water mist, or both lower the temperature before the finished part is removed. Simple in principle. Not always simple in practice.
Glenn Beall, a respected rotational-molding consultant and author, describes the method as “a process for producing hollow plastic parts without using pressure.” That observation explains the machine’s main advantage. Low pressure can reduce tooling costs and support complex shapes, but it also demands careful powder control, mold design, and cycle management. The Association of Rotational Molders emphasizes these factors in its technical guidance and training materials. Recent market reviews from Grand View Research and Mordor Intelligence also identify growing demand for rotationally molded tanks, containers, playground equipment, and industrial housings. Their estimates differ because market definitions vary. That limitation matters. A machine’s value cannot be judged by market growth alone. Operators must examine cycle time, energy use, cooling control, labor access, and part quality. This article explains those working principles, with attention to the details visible on a real factory floor.
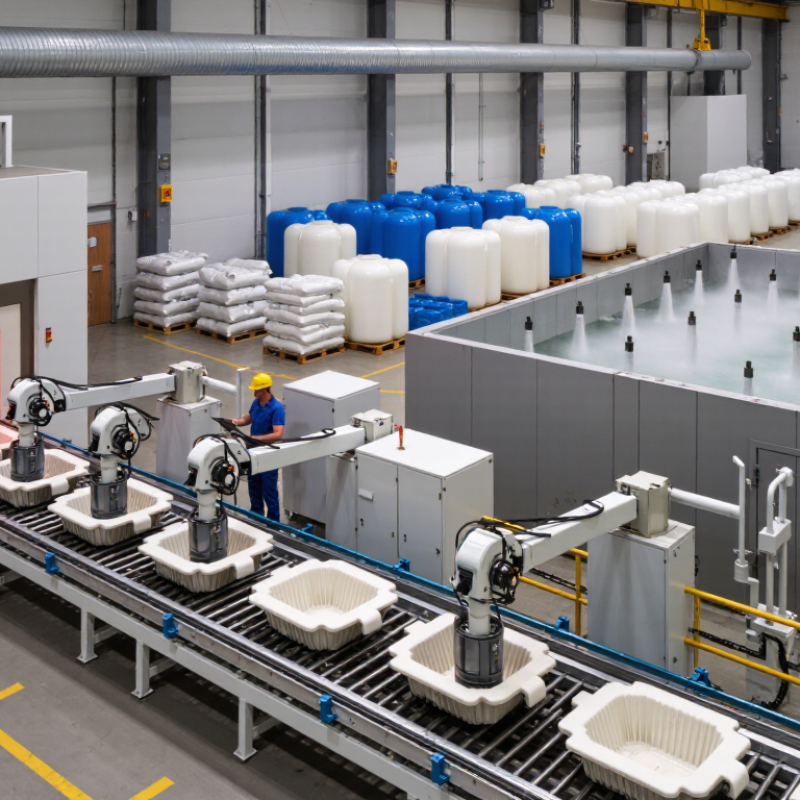
A shuttle rotomolding machine is a thermoplastic molding system with movable mold platforms. Its core purpose is producing hollow plastic parts with controlled wall thickness. The shuttle moves a mold into a heated oven, then returns it to a cooling or loading area. During heating, the mold rotates on two axes. This motion spreads softened plastic across the internal surfaces.
The machine usually serves two or more stations. One platform may remain in the oven while another is unloaded, inspected, or prepared. This arrangement supports flexible production without requiring a separate oven for every mold. Operators can manufacture tanks, containers, housings, and other large hollow components. The process also avoids weld lines created by joining several molded sections.
In practical operation, results depend on more than oven temperature. Mold condition, resin quantity, rotation speed, cooling airflow, and cycle timing all influence the final part. An experienced operator checks corners, seams, and wall thickness after demolding. Small changes can prevent distortion or trapped stress. It is not automatically the best machine for every factory. Shuttle systems need floor space, careful scheduling, and disciplined mold handling. A weak cooling setup may still produce warped parts. That detail is easy to overlook. Improvements often come from reviewing actual cycle data rather than relying only on standard settings.
A shuttle rotomolding machine uses controlled heat and rotation to form hollow plastic products. Its shuttle carriage moves a mold between the oven, loading area, and cooling station. During heating, the mold rotates on two axes, spreading plastic powder across its inner surface. The material melts gradually and builds a consistent wall.
The oven supplies controlled heat through gas burners or electric heating elements. Air circulation helps reduce hot and cold zones inside the chamber. The shuttle carriage supports the mold and travels along rails between working stations. Its drive system controls rotation speed, direction, and movement during each cycle. Small adjustments matter here. Uneven motion can create thin corners or unwanted material buildup.
The mold defines the product’s shape and usually includes vents for releasing trapped air. A vent that is too small may increase internal pressure. A vent that is too large can affect surface quality. The cooling station uses air, water mist, or both to solidify the molded part without causing severe distortion. Operators monitor mold temperature, oven temperature, rotation speed, and cooling time through the control system.
Loading and unloading equipment also affects production reliability. Clean mold surfaces support better release and more stable dimensions. In practical operation, temperature sensors are not perfectly accurate, so experienced operators check parts instead of trusting displays alone. Wall thickness, warping, and surface texture reveal problems quickly. Some cycles still need adjustment, especially when product geometry changes.
A shuttle rotomolding machine uses movable mold carts for heating, cooling, loading, and unloading. Each cart carries a mold into a heated chamber. The operator first measures polymer powder and places it inside the clean, open mold. Correct material weight matters because it controls the final wall thickness.
The mold closes and moves into the oven. It rotates on two axes while heated air surrounds its surfaces. As the powder melts, it spreads across the inner walls through continuous rotation. There is no internal core pressing the plastic outward. The machine depends on heat, gravity, rotation speed, and timing.
When the material has fully fused, the cart leaves the oven and enters the cooling area. Air, water mist, or a controlled combination lowers the mold temperature. Cooling must be gradual. Fast cooling can create distortion, stress, or uneven shrinkage. Not perfect every time.
After cooling, workers open the mold and remove the hollow part. They trim flash, check dimensions, and inspect the surface for bubbles, thin areas, and warping. Experienced operators also review cycle records before changing settings. A small adjustment in oven temperature or cooling time may improve one part but harm another. That is why process control requires measurement, patience, and practical judgment.
A shuttle rotomolding machine uses separate heating and cooling stations to produce hollow plastic parts. A mold is clamped onto a shuttle carriage, which moves between these work areas. During loading, technicians measure resin carefully and inspect the mold for damaged seals or blocked vents. Small mistakes here can affect wall thickness later.
Inside the heating chamber, the mold rotates around two axes. This movement spreads the resin across the internal surfaces as heat melts it. Air temperature, rotation speed, and heating time must match the resin and mold design. Operators often check temperature records and part samples, rather than trusting one setting. The process is not perfectly uniform. Corners and deep ribs may heat more slowly.
The shuttle then carries the mold into the cooling zone. Fans or controlled air systems remove heat while rotation continues. Stopping rotation too early may cause sagging, uneven walls, or distortion. Cooling too quickly can create stress, so experienced operators adjust airflow gradually. When the part is stable, the carriage returns for mold opening and part removal. Simple handling matters. A warm part can still deform under careless gripping. After demolding, technicians trim flash, inspect surfaces, and compare dimensions with production specifications. Even reliable cycles need review, because ambient temperature, resin moisture, and mold condition can quietly change the result.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru