What Is Solvent Free Lamination and How Does It Work?
Solvent Free Lamination joins two or more flexible packaging webs without using liquid solvents. Instead, a two-component adhesive is metered, mixed, and applied in a very thin layer. Heat and pressure then help the films bond as the adhesive cures. The process may look simple. It is not.
Dr. Luca Bianchi, a flexible-packaging adhesive specialist, describes the principle clearly: “Control the adhesive film, and you control the final laminate.” This practical view explains why operators monitor coating weight, mix ratio, web tension, nip pressure, and curing temperature. A small imbalance can create tunnels, wrinkles, weak seals, or visible haze. On a production line, these defects may appear slowly, several hours after lamination. That delay makes troubleshooting less obvious.
Solvent Free Lamination can reduce solvent handling, drying energy, and factory emissions. It also supports thinner adhesive layers and efficient material use. Yet it is not automatically the best choice for every structure. High-speed lines demand disciplined maintenance and accurate metering. Some films need careful surface treatment before bonding. Cure time also matters, especially when packaging requires strong chemical resistance or low odor.
A clean-looking roll is not enough. Experienced teams test bond strength, appearance, residual odor, and seal performance. They also inspect samples after aging, not only immediately after production. This is where the process becomes more demanding than its name suggests. Solvent-free does not mean risk-free. It means the risks have moved into formulation, equipment control, and process discipline. A little uncertainty remains, and honest quality checks must expose it.
What Solvent-Free Lamination Is and How Its Core Principle Works
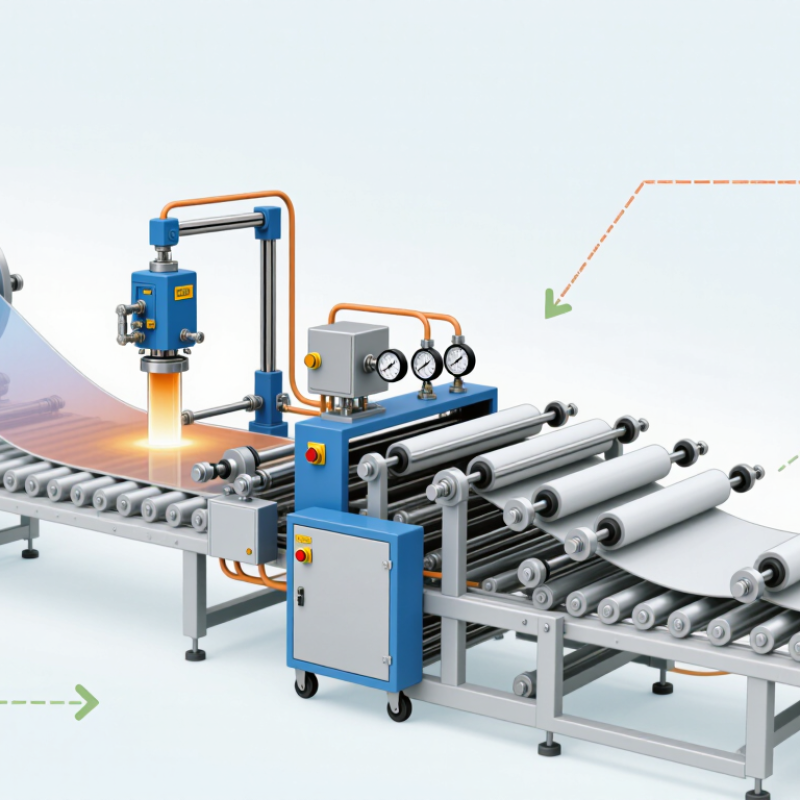
Solvent-free lamination bonds flexible films without evaporating liquid solvents. Its core principle is chemical reaction. Two adhesive components are metered, mixed, and applied as a thin layer between substrates. The adhesive contains nearly 100% solid material, so little or no drying energy is needed. After coating, the films pass through a pressure nip. Heat may improve flow, but curing mainly occurs through a controlled reaction.
In production, accurate dosing matters greatly. A mixing unit must maintain the correct component ratio throughout the run. The coated film should look even, without streaks, pinholes, or dry areas. Clean surfaces help the adhesive spread and bond properly. Operators also monitor web tension, coating weight, nip pressure, and curing temperature. These details often decide whether a pouch feels smooth or develops wrinkles at the edges.
The process is not automatically flawless. Poor mixing can create weak zones, while excessive adhesive may cause blocking or curling. A small temperature change can also alter viscosity and coating behavior. In practical work, early bond tests can be misleading because full strength may require several days. That delay deserves attention. Solvent-free lamination reduces solvent emissions and drying requirements, yet it still demands disciplined equipment control, verified formulations, and careful inspection.
Materials and Equipment Used in a Solvent-Free Lamination System
What Is Solvent Free Lamination and How Does It Work?
Solvent-free lamination bonds flexible materials without evaporating liquid solvents. A two-component polyurethane adhesive usually creates the bond. The system meters, mixes, and coats the adhesive onto one web. Typical materials include plastic films, aluminum foil, paper, and barrier laminates. Each material affects coating weight, tension, and curing time. The adhesive may look simple, but small setting errors can cause wrinkles or weak bonding.
A solvent-free lamination line uses unwinders, tension controls, heated adhesive tanks, precision metering rollers, and a mixing unit. A coating roller applies a very thin adhesive layer. The laminating nip then presses two webs together under controlled pressure. Rewinders form the finished roll. Temperature sensors and inspection tools help operators monitor coating stability and surface defects. Curing often continues after winding, sometimes for several days. Rushing this stage can damage performance.
Tips: Check film surface treatment before production. Confirm adhesive ratios regularly. Keep rollers clean and aligned. Store materials in stable conditions. A useful lesson from production is that “more adhesive” does not always mean stronger bonding. Excess coating can increase cost, extend curing, and create uneven rolls. I have found that careful tension control often matters more than speed. Still, every structure behaves differently, so trial runs and documented adjustments remain essential.
What Is Solvent-Free Lamination and How Does It Work?
Solvent-free lamination bonds two or more flexible substrates with a two-component polyurethane adhesive. The adhesive is metered, mixed, applied by a heated coating unit, pressed together in a laminating nip, and then cured without using a solvent carrier.
Typical Adhesive Coat-Weight Ranges by Lamination Duty
The ranges shown are representative industry process targets in grams per square metre (g/m²). Actual settings depend on substrate surface energy, film structure, barrier requirements, adhesive viscosity, coating temperature, nip pressure, and curing conditions. A typical system includes adhesive tanks, precision metering pumps, a static mixer, a heated coating head, a laminating nip, web-tension controls, and a curing area.
How Adhesive Application and Film Bonding Take Place
What Is Solvent-Free Lamination and How Does It Work?
Solvent-free lamination bonds two flexible films without using a solvent carrier. A two-component polyurethane adhesive is mixed immediately before coating. A metering unit applies a thin, even layer to the first web. The coated film then enters a heated nip roller. Pressure and controlled heat spread the adhesive across the surface. The second film joins it there. The laminate later cures as the adhesive chemically reacts.
The process is precise, but not foolproof. Adhesive ratios, coating weight, web tension, and roller temperature must remain stable. A small mixing error can create bubbles, weak edges, or curling. Operators often inspect the bond after curing, not only directly after the nip. The Flexible Packaging Association’s 2024 State of Flexible Packaging Report valued the United States flexible packaging market at about $40.9 billion in 2023. That scale increases pressure for faster, cleaner converting. Solvent-free systems can help because they contain nearly 100% solids and usually need no solvent-drying oven.
Curing still takes time. Do not confuse “dry” with “fully bonded.” Some structures require hours or days before final bond strength develops. Smithers’ flexible packaging market research identifies sustainability, material reduction, and production efficiency as continuing industry drivers. In practice, solvent-free lamination supports these goals by reducing oven energy and solvent emissions. Yet thinner adhesive layers demand better surface treatment and cleaner films. A glossy roll may look perfect. It can still delaminate later. That is where process records, peel testing, and experienced adjustment matter.
Benefits, Limitations, and Typical Industrial Applications
What Is Solvent-Free Lamination and How Does It Work?
Solvent-free lamination joins flexible film, foil, or paper without evaporating liquid solvents. A metering system applies a two-component adhesive in a very thin layer. The adhesive components react after coating and form a durable bond during curing. Pressure helps remove air and maintain contact between the webs. Curing may continue for several days, depending on chemistry, temperature, and substrate structure.
Its main benefits include low emissions, reduced drying energy, and efficient material use. The process also supports high production speeds and clean working areas. Typical applications include snack packaging, medical pouches, household product packs, and industrial laminates. However, precise mixing and coating control are essential. Small ratio errors can cause weak bonds, bubbles, or uneven curing. Some structures also need longer aging before filling or converting. It is not automatically better for every product. A supplier’s laboratory trial and real production test remain important.
Tips: Check adhesive weight across the full web width. Monitor mix ratio, line speed, pressure, and curing temperature. Test bond strength after realistic storage conditions. Operators should record defects, because minor wrinkles can reveal larger alignment problems. In my experience, early trials sometimes look excellent but fail after aging. That lesson is easy to overlook.