Choosing a supplier for Sand Casting Parts is not just a price comparison. The right partner should understand your drawings, production needs, and the conditions each part must withstand. A housing used near heat, for example, may need different alloy guidance and inspection checks than a decorative component. Details matter.
This guide presents ten practical tips for evaluating potential suppliers. It covers casting experience, material knowledge, tooling capabilities, quality checks, communication, lead times, and after-sales support. Ask how a supplier handles dimensional inspection, defect review, and changes to a drawing. Request clear examples, such as sample inspection records or a production schedule. Not every supplier will share the same format, so compare the evidence carefully.
Look beyond the quoted unit price. A low quote can look convincing. It may not include tooling, finishing, packaging, or the cost of delayed delivery. Clarify what the estimate covers before comparing offers. If possible, begin with a sample order and check the casting against your actual requirements. Useful checks may include dimensions, surface condition, and documentation for the specified material. A checklist helps, but it is not a substitute for technical discussion. Some details may still be missed. Review them openly. Supplier selection involves trade-offs, and the best fit depends on part complexity, order volume, and risk tolerance. These tips are a starting point, not a guarantee; verify claims and confirm requirements with your engineering and quality teams.
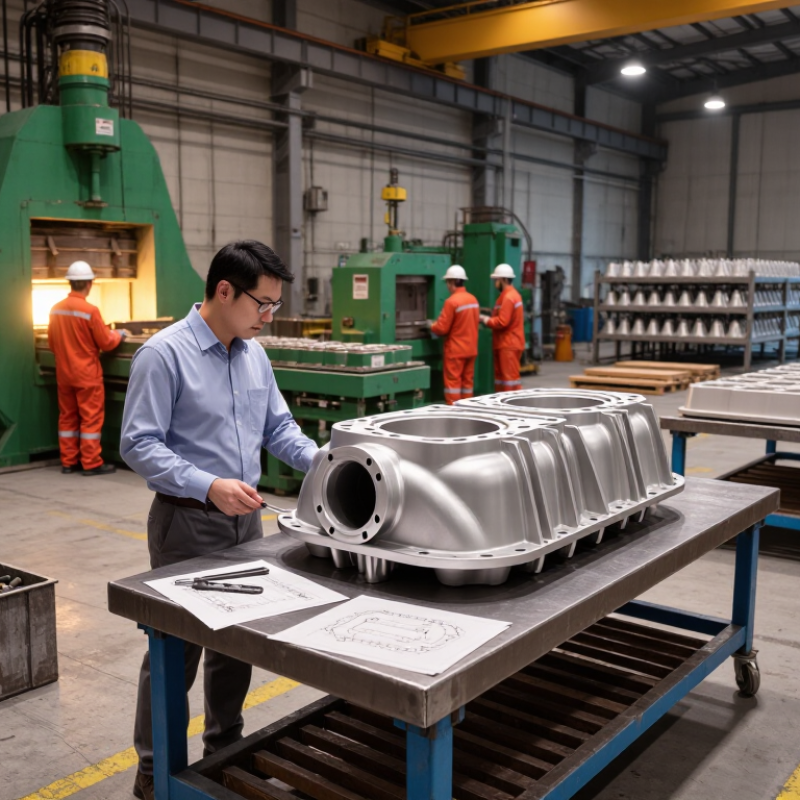
Before comparing sand casting suppliers, define the part in measurable terms. State the alloy, finished weight, annual volume, and maximum envelope. Add critical wall thicknesses, machining allowances, and required surface finish. A drawing showing 280 × 160 × 90 mm is more useful than “medium-sized housing.”
Specify tolerances by function, not habit. ISO 8062-3 provides casting tolerance grades that help suppliers quote consistently. The 2023 World Foundry Census reported global casting production of about 110 million tonnes in 2022. That scale reflects intense process variation, so vague requirements create avoidable price differences. Identify datum surfaces, hole locations, thread details, and areas requiring inspection. Include acceptable limits for porosity, cracks, distortion, and inclusions. If pressure tightness matters, define the test method and pressure.
I have seen projects fail because the buyer requested a smooth surface without naming a measurement method. Use a recognized roughness value where possible. Ask for sample approval, inspection records, and traceability for each batch. Confirm whether the supplier owns the pattern, maintains it, or charges separately for repairs. A perfect specification may be unrealistic for early prototypes. That is worth admitting. Mark uncertain dimensions clearly, then review them with an experienced foundry engineer. Share photographs of the assembly, especially where tools or fixtures contact the casting. Small details can change feeding design, machining time, and final cost.
Choosing a sand casting parts supplier requires more than comparing prices. Assess practical experience, equipment, and proven casting capabilities. The 2023 World Foundry Census reported global casting production above 100 million tonnes in 2022. That scale makes process discipline essential, especially for suppliers handling repeat orders.
Ask how long the supplier has produced similar alloys, geometries, and annual volumes. Request sample inspection reports, not only attractive photographs. Review furnace capacity, temperature monitoring, sand testing, core-making equipment, and pattern storage. A capable foundry should explain its control points clearly. Ask for proof.
Check whether the supplier can manage thin walls, deep cavities, complex cores, and machining allowances. The American Foundry Society’s industry data consistently identifies quality control, skilled labor, and equipment investment as major foundry challenges. Therefore, verify operator training and maintenance records. A modern furnace cannot repair poor mold preparation.
Request traceable material certificates, dimensional reports, and nonconformance records. Independent testing may include chemical analysis, hardness checks, radiography, or pressure testing, depending on the part. Visit the production floor if possible. Look for labeled sand batches, organized tooling, and clean inspection areas. I have learned that a polished tour can still hide weak process control. Supplier claims need evidence, and even experienced buyers sometimes overlook lead-time risks. Review capacity during peak months, because the best technical fit may still fail commercially.
Choosing a sand casting parts supplier requires more than comparing prices. Quality controls should be visible on the production floor, not only described in a sales document. Ask how patterns, molds, pouring temperatures, and dimensional checks are recorded. Request sample inspection reports for similar castings.
A reliable supplier should hold relevant quality certifications and provide current certificates upon request. Verify the certificate number, scope, and expiration date independently. Certification alone is not proof of daily discipline. Audit records, nonconformance reports, and corrective actions reveal more about actual performance. I once reviewed a supplier with impressive paperwork but inconsistent inspection logs. That gap deserved attention.
Material traceability must continue from raw stock to finished parts. Each heat or batch should have a clear identification code. That code should connect material certificates, furnace records, test results, and shipment documents. Check whether labels remain readable after cleaning and machining. Small gaps matter. During an audit, follow one part backward through the records. If the trail stops at the melting stage, traceability is incomplete. Ask how mixed returns, rework, and leftover metal are controlled. These details can expose risks that a polished factory tour misses.
Speak with the quality engineer, not only the account manager. Ask for evidence, and allow time for uncomfortable questions. Some suppliers may need improvement. That is not automatically a rejection. What matters is whether they recognize weaknesses, document actions, and verify that fixes work.
Choosing sand casting parts suppliers requires more than selecting the lowest quote. In my sourcing reviews, cheap estimates often excluded pattern adjustments, machining, inspection, or export packing. Ask each supplier to separate tooling, casting, finishing, testing, and shipping costs. A useful quote names the alloy grade, weight tolerance, quantity assumptions, and payment milestones. If one line says “miscellaneous,” request clarification. Small omissions become expensive later.
Compare calendar dates, not vague phrases. Request dates for drawing review, pattern completion, first samples, corrective work, and production release. A supplier promising 14 days may mean only melting and pouring. Check capacity during holidays and ask how they handle furnace maintenance or rejected samples. I once treated a short lead time as proof of efficiency. It was not. The sample arrived quickly, but dimensional corrections added three weeks. That mistake changed my review checklist.
Test communication before placing an order. Send a drawing question and observe response speed, technical accuracy, and willingness to document assumptions. Clear replies should mention draft angles, shrinkage allowance, core placement, and inspection records when relevant. Keep one shared revision log, because phone promises fade. Ask who owns urgent decisions and how delays are reported. Silence is data. Still, perfect communication is unrealistic. A capable supplier may miss one message, then recover with a specific action and date. Judge the recovery, not only the first reply.
| # | What to Compare | Questions to Ask | Evidence to Review | Why It Matters |
|---|---|---|---|---|
| 1 | Quote scope and assumptions | Does the quotation cover pattern or tooling, casting, machining, inspection, finishing, and packaging? | An itemized quotation with inclusions, exclusions, and stated assumptions. | A low headline price may exclude services or costs included in another quote. |
| 2 | Material and casting requirements | Can the supplier meet the specified alloy, mechanical properties, and applicable material requirements? | A material specification, applicable test plan, and sample material documentation. | Material and process choices affect part performance and acceptance. |
| 3 | Lead time and schedule detail | What are the estimated dates for tooling, samples, approval, production, and shipment? | A milestone schedule that identifies dependencies and the date the lead time begins. | A breakdown makes competing delivery estimates easier to compare and monitor. |
| 4 | Tooling and pattern ownership | Who owns the pattern or tooling, how is it maintained, and what happens if production moves? | Written terms covering ownership, storage, maintenance, and transfer. | Clear terms help avoid uncertainty about future access and replacement costs. |
| 5 | Machining and tolerance plan | Which features are cast, which are machined, and how will critical dimensions be verified? | A drawing review, inspection plan, and sample measurement report for agreed critical features. | Casting and machining requirements should be evaluated together against the part drawing. |
| 6 | Quality controls and traceability | How are incoming material, production stages, nonconformities, and finished parts controlled? | Relevant quality procedures, inspection records, traceability examples, and corrective-action process. | Documented controls help assess how issues are detected, recorded, and addressed. |
| 7 | Finishing and secondary operations | Are cleaning, heat treatment, coating, machining, or other required operations included or subcontracted? | A process flow showing operation responsibility, inspection points, and quoted charges. | Additional operations can affect cost, quality responsibility, and overall schedule. |
| 8 | Quantity, pricing, and payment terms | How does unit pricing change by order quantity, and are setup, packaging, or other charges separate? | A price breakdown by requested quantity, with currency, validity period, and payment terms. | Comparable assumptions reveal the likely total cost for the planned order. |
| 9 | Communication and issue handling | Who is the project contact, how are updates shared, and how are drawing questions or delays escalated? | A named role or contact, agreed update frequency, and a clear escalation path. | Responsive, organized communication supports faster decisions and clearer accountability. |
| 10 | Packaging, shipping, and delivery terms | How will parts be protected, who arranges transport, and where does the quoted delivery responsibility end? | Packaging details, shipping assumptions, destination, and clearly stated delivery terms. | Packaging and transport responsibilities affect delivered cost and the risk of transit damage. |
A sand casting sample shows more than surface quality. Ask for a part similar in size, alloy, and shape to your own. Compare key dimensions with the drawing, then inspect edges, draft angles, and machining allowance. Small details matter. A clean surface can still conceal uneven wall thickness or a difficult-to-machine area. If possible, review a cut section or inspection report alongside the sample.
References reveal how a supplier performs after the first order. Speak with customers who have bought comparable parts, not only easy, low-volume castings. Ask how the supplier handled a late design change, a rejected batch, or inconsistent dimensions. One reference is not enough. A glowing comment may reflect one unusually smooth project, so look for patterns across several conversations.
Long-term support includes clear communication, stable process records, and practical help when specifications change. Confirm who will answer technical questions and how quickly inspection results can be shared. Request written details for tooling maintenance, sample approval, and corrective actions. These points can feel tedious before production begins. They matter later. Even a strong supplier may need reminders, so define review dates and keep agreed drawings and measurements accessible. I would still leave room for reassessment; early samples cannot predict every production issue.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru